
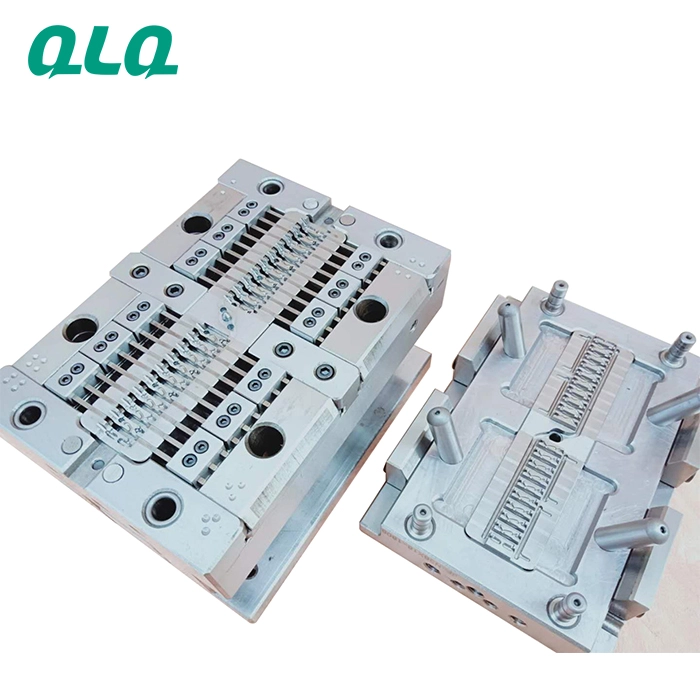
Slider Mould Daily Care: Cavity Cleaning, Release Agent and Storage.
A working reference for slider mould care. Numerical values in the process diagram are illustrative, not universal operating limits. Set cleaning methods, tool materials and service intervals from the mould maker instructions and the validated mould history. Scenarios below illustrate checks, not verified customer results.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Cleaning cavities with hard metal scrapers | Scratches copy into every shot | Use approved non-damaging tools and compatible cleaning agents |
| 2. No shot counter | Maintenance timing becomes guesswork | Counter log per mould; act at set thresholds |
Best Practices
- Approved non-damaging tool kit at the press
- Shot counter threshold alerts
- Mould storage register with dates
Mould Change Care
- Clean cavities - Approved tools and compatible cleaner (No hard metal scrapers)
- Log shot count - Against threshold (Missed logs hide due dates)
- Coat and store - Boxed and dated (Bare storage rusts cavities)
Register per mould | Threshold alerts to setter
Mould Care Reference
Care points for slider moulds in production.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Cavity cleaning | Every mould change | Residue copies into shots |
| Release agent | Thin, even, logged | Heavy coats build residue |
| Shot counter threshold | Per mould history | Act before wear shows in parts |
| Storage | Coated, boxed, dated | Prevents corrosion damage |
Illustrative check: shot counts and maintenance planning
Scenario. Moulds were serviced after failures, not before.
Action. Per-mould shot counter logs with threshold alerts.
Check. Review whether service can be planned before wear defects appear; confirm the result from your own records.
Frequently Asked Questions
Why avoid hard metal scrapers in cavities?
Scratches can transfer to cast parts. Use only mould-maker-approved tools and compatible cleaning agents.
What is a shot counter threshold?
The shot count at which history says maintenance is due set per mould, not per calendar.
How should moulds be stored?
Coated, boxed and dated. Bare storage corrodes cavities and costs the first production run.
Implementation Roadmap
| Step | Frequency |
|---|---|
| Cavity care live | Every change |
| Shot counter logs live | Week 1 |
| Life economics model | Month 1 |
What Would You Like to Solve?
If you would like this checklist or template adapted to your own line and part mix, contact QLQ we supply the full equipment and chemistry package along with the working documents that make it run.
FAQ - Slider Mould Daily Care: Cavity Cleaning, Release Agent and Storage
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.