
Scope of this guide
This management guide translates the process into cost, risk and throughput: what to measure, what to audit and where the money leaks.
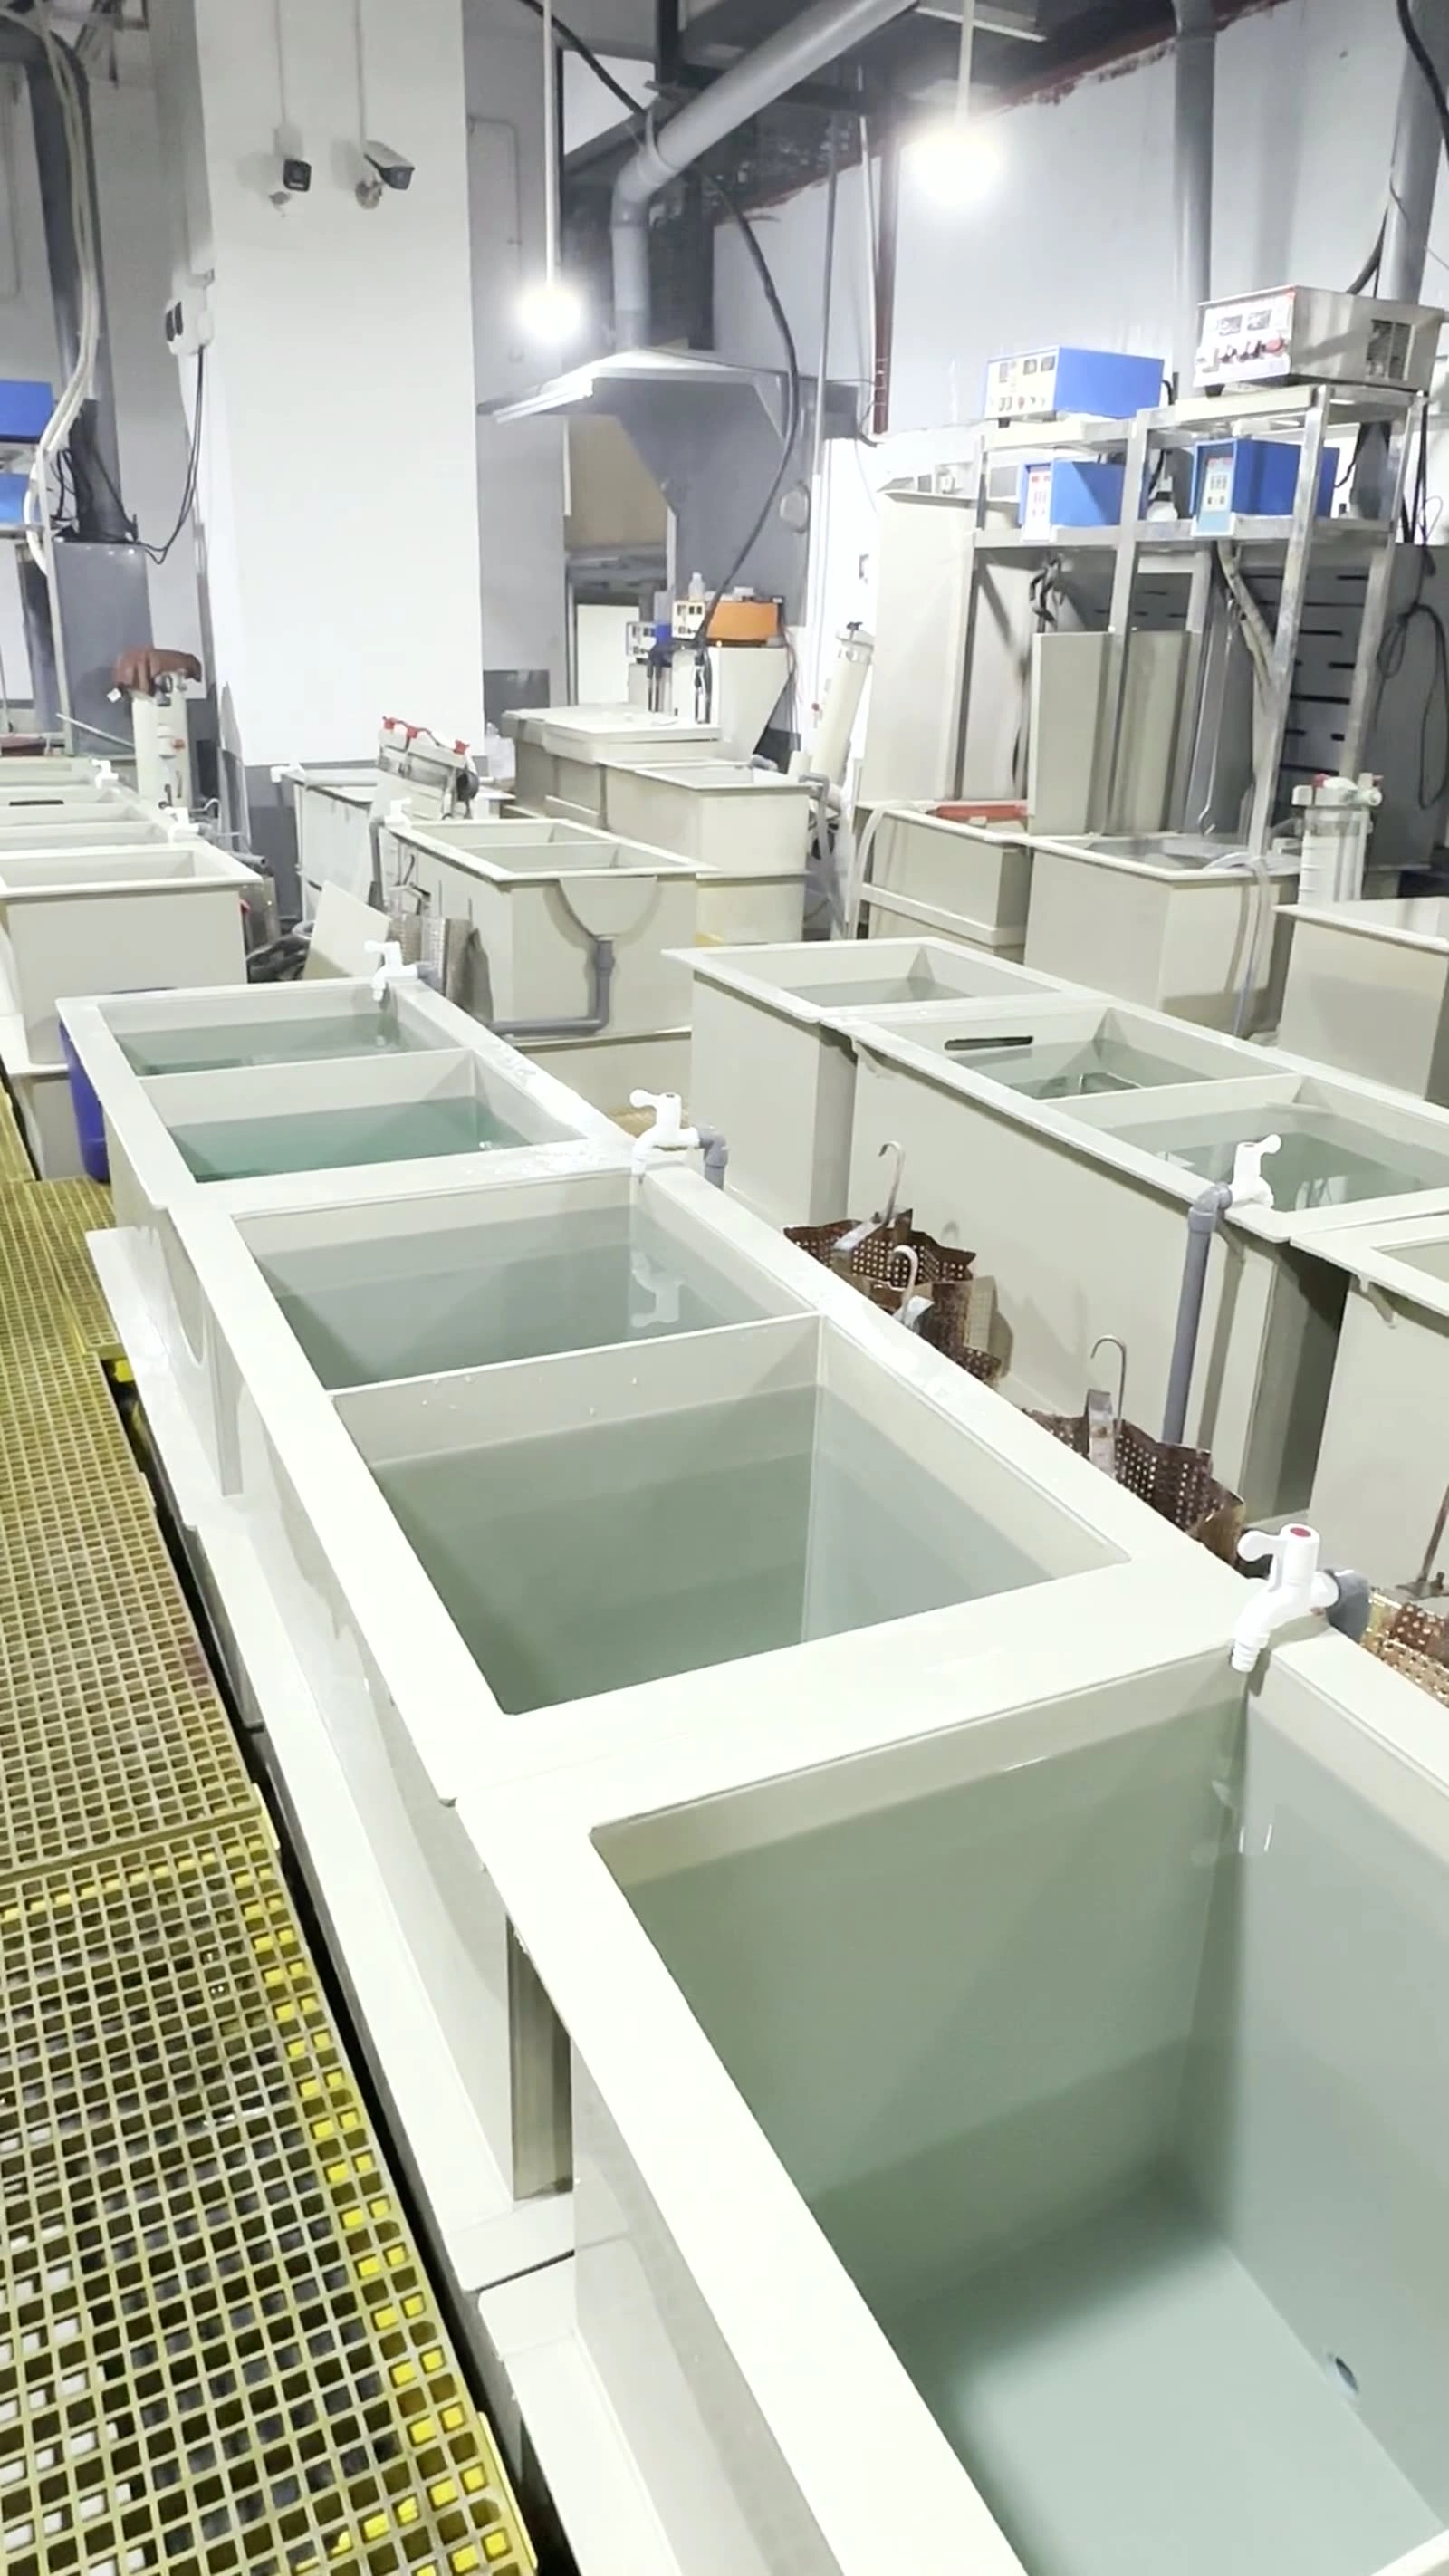
Process: Electrocoating (E-coat). Figures in this guide are industry-standard starting ranges; confirm against your supplier TDS before locking settings.
Working ranges and control points
The table below is the daily reference for a line. Set by the card, verify by the control point column.
| Parameter | Typical range | Control point | Watch out |
|---|---|---|---|
| Bath solids | 14–18% | Solids check daily | Low solids thin films |
| Bath temperature | 28–32 °C | Chiller loop logged | Warm bath ruptures film |
| Voltage | 180–280 V by part | Ramp curve per family | Too high = cratering |
| Conductivity | 1200–1800 µS/cm | UF permeate control | High conductivity rough films |
| Cure | Object temp 160–180 °C, 20 min | Data logger per batch | Under-cure soft film |
Run It As A Business: the management view
Beyond the basic card, this is the layer that matters at your level:
| Cost line | What drives it | Metric to track | Typical lever |
|---|---|---|---|
| Chemicals | Drag-out and bath dumps | Cost per 1000 parts | Rinse counter-flow, drip bars |
| Rework | First-pass yield losses | FPY by defect family | Fix top family first |
| Energy | Heated tanks and idle time | kWh per 1000 parts | Covers, night setback |
| Claims | Escape rate | PPM by customer | Ship gate on FPY |
Standard routine
- Check solids and pH before the first load
- Verify anode cell condition weekly
- Ramp voltage per part family, not one curve for all
- Log object temperature, not oven air
- Rinse ultrafiltrate before bake; never let bath dry on film
Engineer notes
- Craters trace to oil — check pre-clean before blaming the bath
- Anode cells exhaust like filters; log their hours
- Film build follows voltage curve area, not peak voltage
- Rupture voltage falls as conductivity climbs
- Cure verification uses a part thermocouple, oven gauge lies
Safety: E-coat baths and UF permeate irritate skin and eyes. Splash protection and eyewash access are mandatory at load and unload.
FAQ
Why do craters appear after a holiday shutdown?
Oil films settle on racks and parts; re-clean first loads and skim the bath surface.
What controls film thickness most?
The voltage-time curve; solids set the ceiling, the curve sets the build.
How do I know cure is complete?
Solvent rub test plus logged object temperature reaching the cure window.
Which single metric should I start reporting weekly?
First-pass yield by defect family; it exposes rework cost and points at the largest lever.