

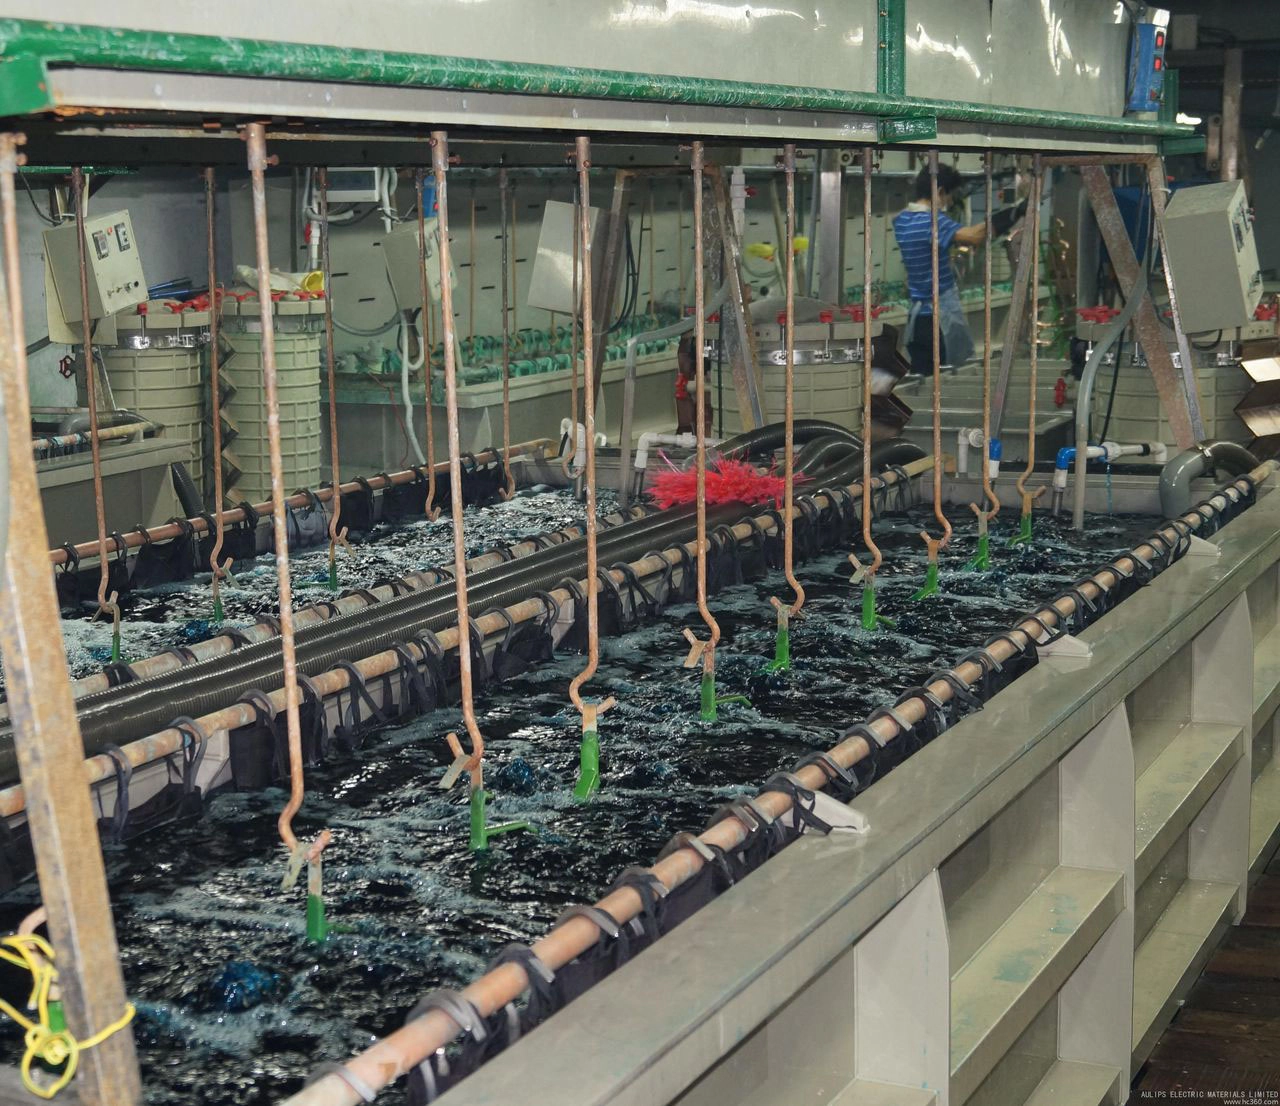
An anodizing bath treats the alloy, not the part description. A rack of parts loaded with the wrong alloy code can etch, smut or come out the wrong shade because the schedule was built for a different metal.
This junior guide covers load tickets for anodizing: verifying alloy codes, checking surface condition, matching the load to the bath schedule, and the gates that stop a wrong-alloy rack before it enters the tank.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Racking without the ticket | Wrong alloy enters the bath | Read the ticket first |
| 2. Misread alloy code | Etch or smut follows | Verify the alloy mark |
| 3. Oily surface missed | Patchy oxide and dye | Surface check before racking |
| 4. Wrong schedule for alloy | Wrong film or shade | Match schedule to alloy |
| 5. Loose contacts | Thin film at contact | Tighten and check |
| 6. Mixed alloys on one rack | One schedule cannot fit | Separate alloys by rack |
| 7. Signed by memory | No real check happened | Gate: inspect then sign |
| 8. Dirty gloves on parts | Stains under the film | Handle parts clean |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Read and verify the load ticket before racking
- Confirm the alloy code on every part family
- Check surface condition before the rack moves
- Match the bath schedule to the alloy
- Sign the ticket only after the real checks
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Load ticket flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- The load ticket connects the part to the correct bath schedule.
- Alloy verification is the cheapest protection against a ruined rack.
- Never mix alloys on one rack unless the ticket allows.
- Never sign a ticket without inspecting the load.
Working Data & Formula Notes
Load ticket reference
Example fields for an anodizing load ticket; adapt to your product range.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Alloy code | From part mark | Drives the schedule |
| Part area | dm2 or m2 | Drives current and time |
| Surface | Clean and oil-free | Gate before racking |
| Contact | Tight and bright | Secure film at contact |
| Schedule | Per alloy | Voltage, acid and time |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Alloy schedule quick table
| Alloy family | Bath response | Ticket note |
| Pure series | Fast film, clear dye | Lower alloying control |
| Common cast alloy | Etch risk | Check acid and time |
| High-copper alloy | Smut risk | Special pre-treatment |
| Mixed load | Not allowed | Separate by ticket |
Implementation Cases
Case 1 - the misread alloy that smutted
Situation. A batch of parts was racked with a ticket for a different alloy series. The parts smutted in the tank because the etch schedule was too strong for the actual metal.
Approach. The load ticket process was changed to require verification of the alloy mark before racking and a second check at the tank.
Outcome. Smutted racks stopped and the ticket check is now part of the handover.
Case 2 - oil that hid under the film
Situation. Parts with a light oil film were racked without surface inspection. After anodizing the finish was patchy and the dye did not take evenly.
Approach. A surface gate was added to the load ticket, checking for oil and water-break before the rack leaves the loading bench.
Outcome. Patchy finishes stopped and surface checks now protect every load.
Frequently Asked Questions
Why verify the alloy before racking?
The bath schedule follows the alloy; a wrong code etches or smuts the part.
What does the load ticket show?
Alloy, part area, surface condition and the bath schedule.
Why check for oil?
Oil blocks the oxide film and shows as patchy finish and dye.
Can I mix alloys on one rack?
Only if the schedule allows; most racks stay to one alloy family.
Why check contacts?
Loose contacts give thin or missing film at the contact point.
When should I sign the ticket?
Only after the alloy, surface and contact checks are real.
What happens with a high-copper alloy?
It needs special pre-treatment; the ticket must flag the risk.
Who owns the load ticket?
The junior loads and signs it; the shift lead spot-checks the gates.
What Would You Like to Solve?
If wrong-alloy or surface faults reach your anodizing tanks, send us your product alloys and current load ticket format. We can help set the verification gates that stop the fault at the loading bench.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.