

Get a Free Quote Today
Send us your samples or drawings — our engineers reply within 24 hours with pricing and technical advice.
Workshop Planning Data
Color Paint — Data Zinc Alloy Finishing Managers Need
The painting line applies primer and topcoat by barrel spraying, rack spraying or cold spraying, then bakes to a durable finish with 100+ h salt spray, covering zinc alloy hardware in any RAL color.
600 m²Workshop Area
20 peopleTeam Size
220 kWInstalled Power
400-900k pcs/dayDaily Output (10 h)
Quality Inspection & Control
| Check item | Method | Acceptance standard |
|---|---|---|
| Film thickness | Coating thickness gauge | Primer 15-25 μm; topcoat 20-35 μm total 40-60 μm |
| Color match | Colorimeter ΔE | ΔE ≤ 1.0 vs approved RAL master |
| Adhesion | Cross-cut + tape | ISO 2409 rating 0-1 |
| Salt spray | NSS chamber | ≥ 100 h (with phosphating) |
| Bake cure | MEK rub test | No paint lift after 50 rubs |
| Appearance | Angle-light inspection | No orange peel, sagging, pinholes or overspray |
Workshop Layout & Floor Area
| Zone | Area |
|---|---|
| Pretreatment / phosphating | 110 m² |
| Spray booths (barrel + rack + cold) | 180 m² |
| Flash-off & curing ovens | 120 m² |
| Paint mixing / store | 60 m² |
| QA & color lab | 40 m² |
| Utility / compressed air | 50 m² |
| Packaging | 40 m² |
| Total workshop | 600 m² |
Manpower & Shift Plan
| Role | Headcount |
|---|---|
| Spray operators | 10 |
| Pretreatment operators | 3 |
| QC inspectors | 2 |
| Paint mixing technician | 1 |
| Oven / conveyor monitor | 1 |
| Supervisor | 1 |
| Maintenance | 1 |
| Packaging | 1 |
| Total (2 shifts × 10 h) | 20 |
Power & Utility Demand
| Equipment | Demand |
|---|---|
| Spray booths + extraction | 40 kW |
| Curing ovens (2 × 60 kW) | 120 kW |
| Air compressor | 22 kW |
| Conveyor / barrel drives | 15 kW |
| Paint pumps + mixer | 8 kW |
| Lighting & auxiliary | 15 kW |
| Installed total | 220 kW |
| Typical running load | ≈ 175 kW |
Production Flow Chart
PretreatmentDegrease → phosphate → dry
Load & MaskBarrel / rack / cold painting load
Primer CoatElectrostatic or air spray
Flash-off5-10 min solvent flash
TopcoatColor coat per RAL
Cure & QCBake 120-160 °C, inspect, pack
Daily Capacity — 10-Hour Operating Day
| Parameter | Value |
|---|---|
| Coating cycle | 40-70 min |
| Load per batch | 60-120 kg |
| Batches per 10 h day | 10-14 |
| Daily output | 400,000-900,000 pcs |
| Monthly output (26 days) | 10-23 million pcs |
Output Value Estimate
| Parameter | Value |
|---|---|
| Painting fee per piece | USD 0.008-0.02 |
| Daily output value (10 h) | USD 4,000-10,000 |
| Monthly output value | USD 104,000-260,000 |
| Annual output value | USD 1,250,000-3,120,000 |
Related Products — Complete Color Paint Solution
Machines, chemicals and consumables selected from the real QLQ product range for this process. Every product page is live and ready to quote.
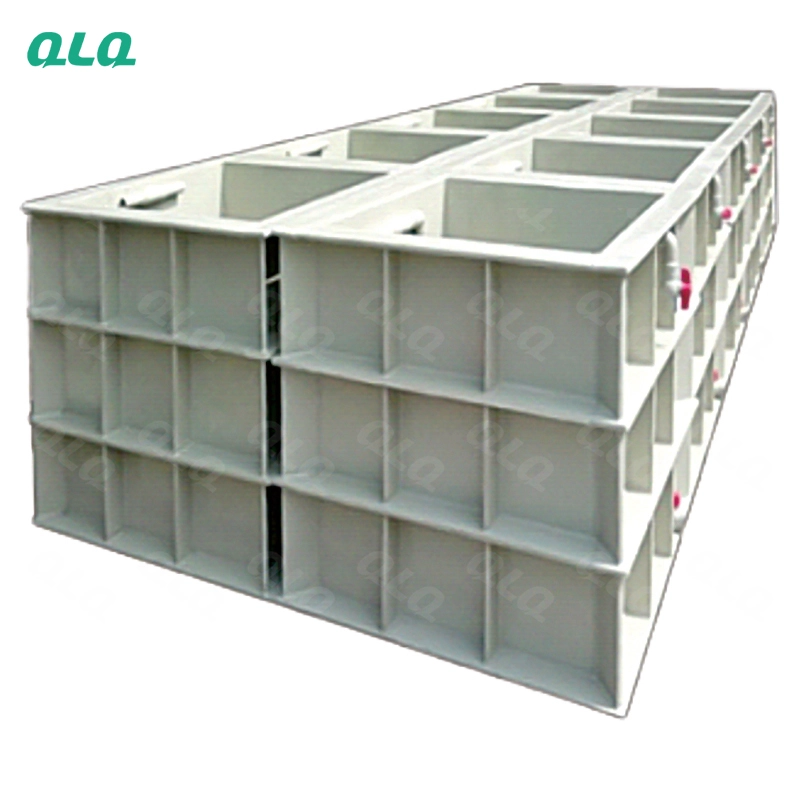
Automatic washing tank is suitable for rack plating, electrophoresis, and pretreatment.
Machine & Equipment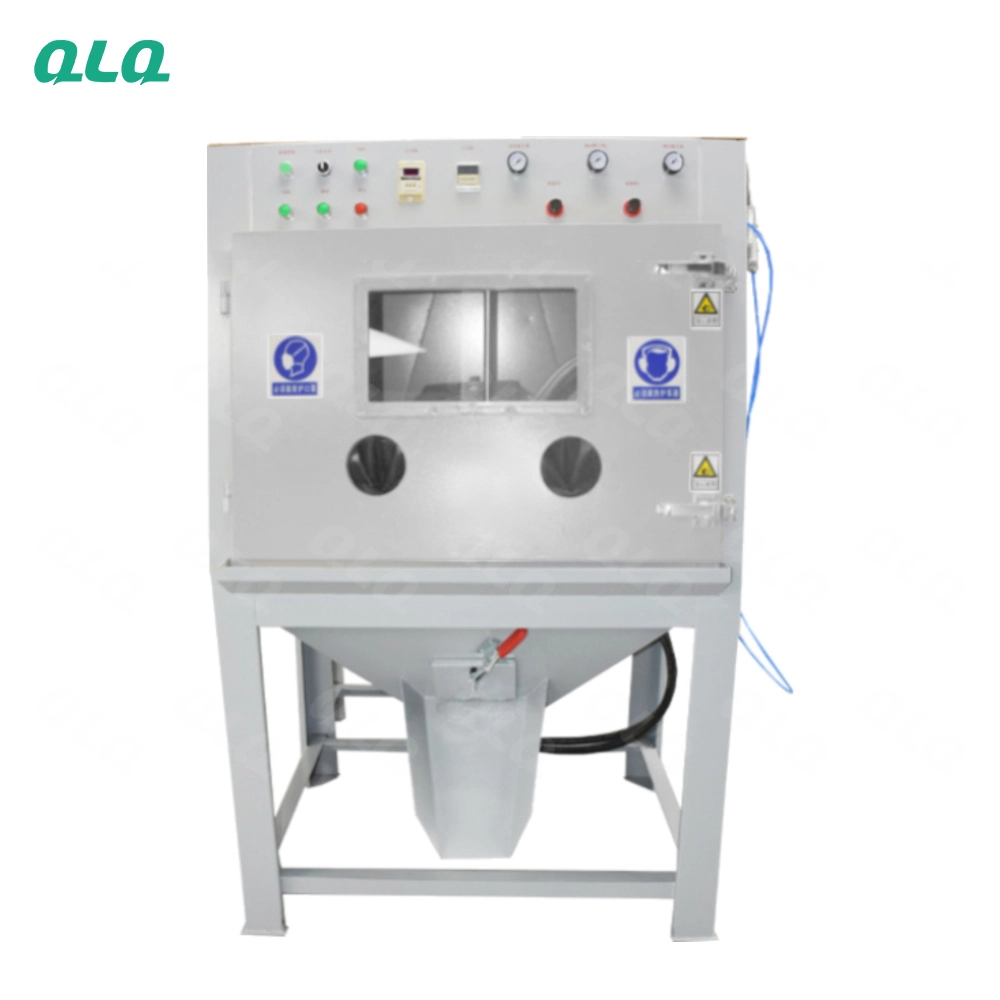
QLQ-ASBM Automatic Sand Blasting Machine
Machine & Equipment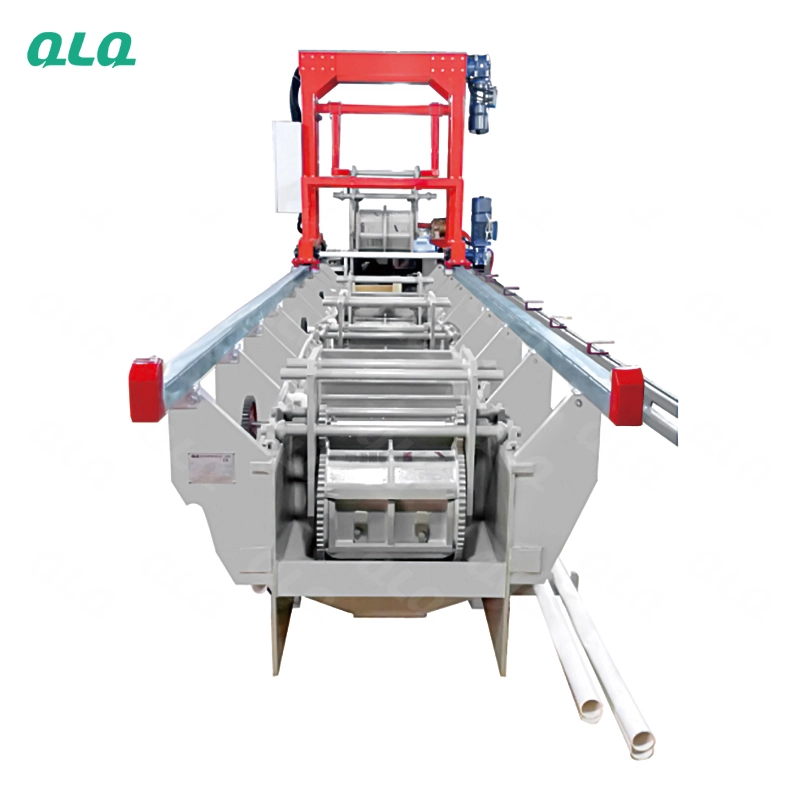
QLQ-APM Automatic phosphating machine
Machine & Equipment
Tea Seed Powder
Chemical & Coating
Porcelain Refined Polishing Stone
Consumable & Accessory
Aluminum and Porcelain Oblique and Round Column Refined Polishing Stone
Consumable & Accessory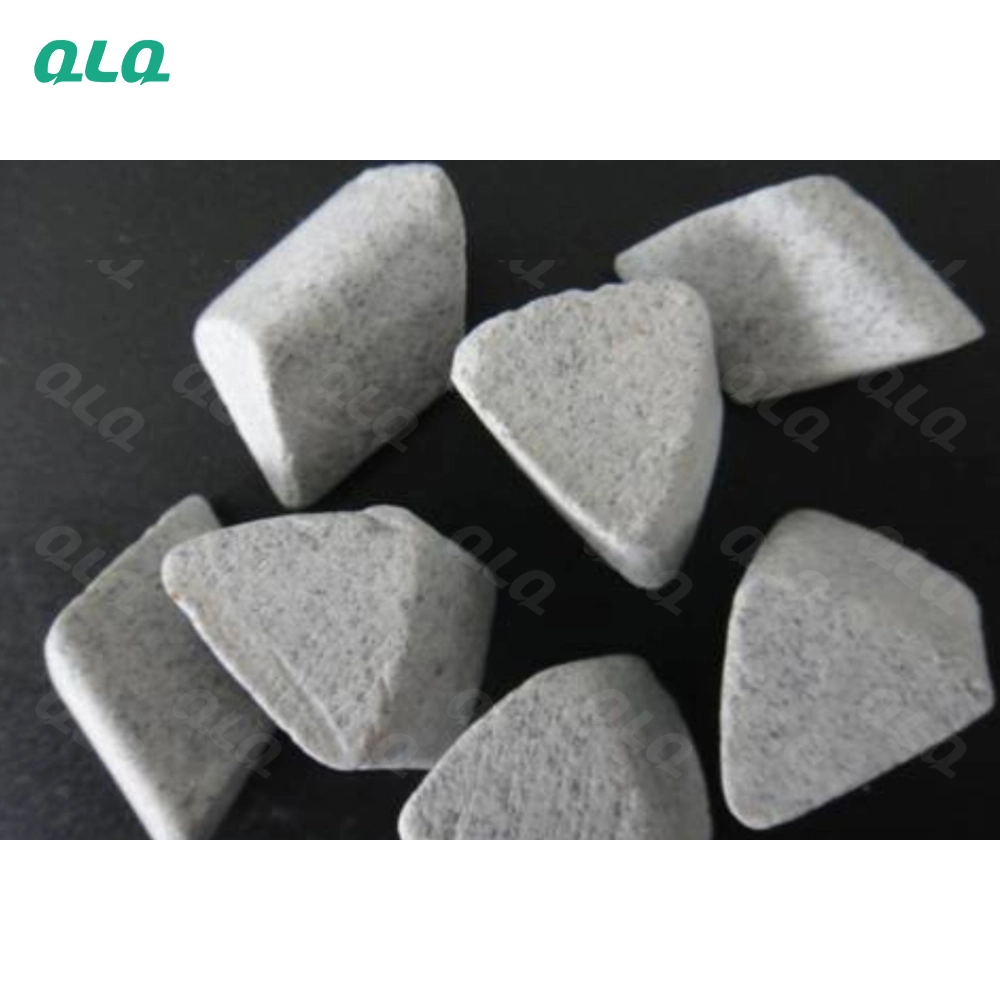
Triangle Shape Rough Polishing Stone
Consumable & Accessory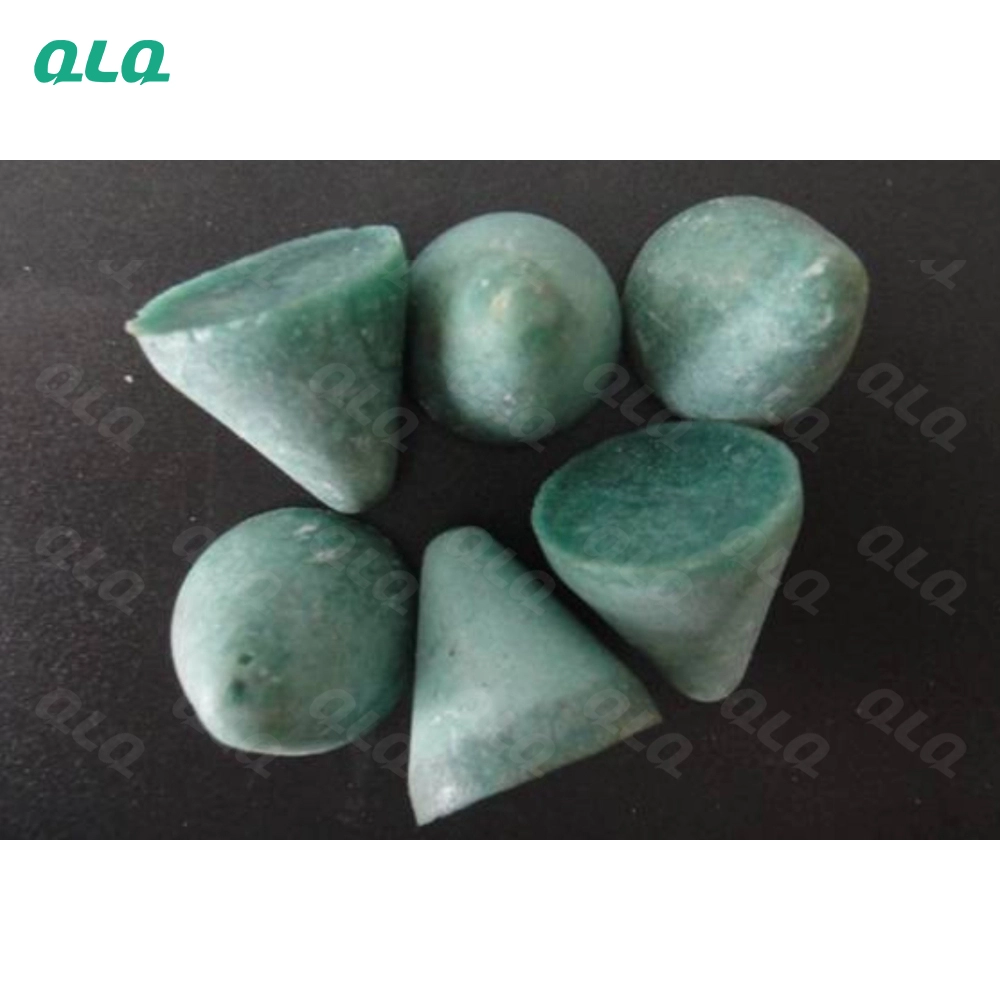
Derlin Coniform Shape Fine Polishing Stone
Consumable & AccessoryView Full Product Range
Colour matching workflow
| Step | Action | Output |
|---|---|---|
| 1. Target | Approve a physical chip, not a photo | Signed chip with base layer spec |
| 2. Base | Lock base layer and film build | Recorded thickness range |
| 3. Trial | Spray 3 panels at different film builds | Visual + gloss readings |
| 4. Confirm | Compare under D65, indoor and shade | L*a*b* values stored |
| 5. Production | Check first part each shift | Batch record |
FAQ
Why do we need three panels?
Film build changes perceived colour. One panel only proves one thickness works.
Can we match a PMS number exactly?
PMS describes ink on paper. On plated metal, the base layer shifts the result - match the physical chip, not the code.
What causes colour drift mid-batch?
Paint viscosity, booth temperature or film build. Log all three, then compare batches.