
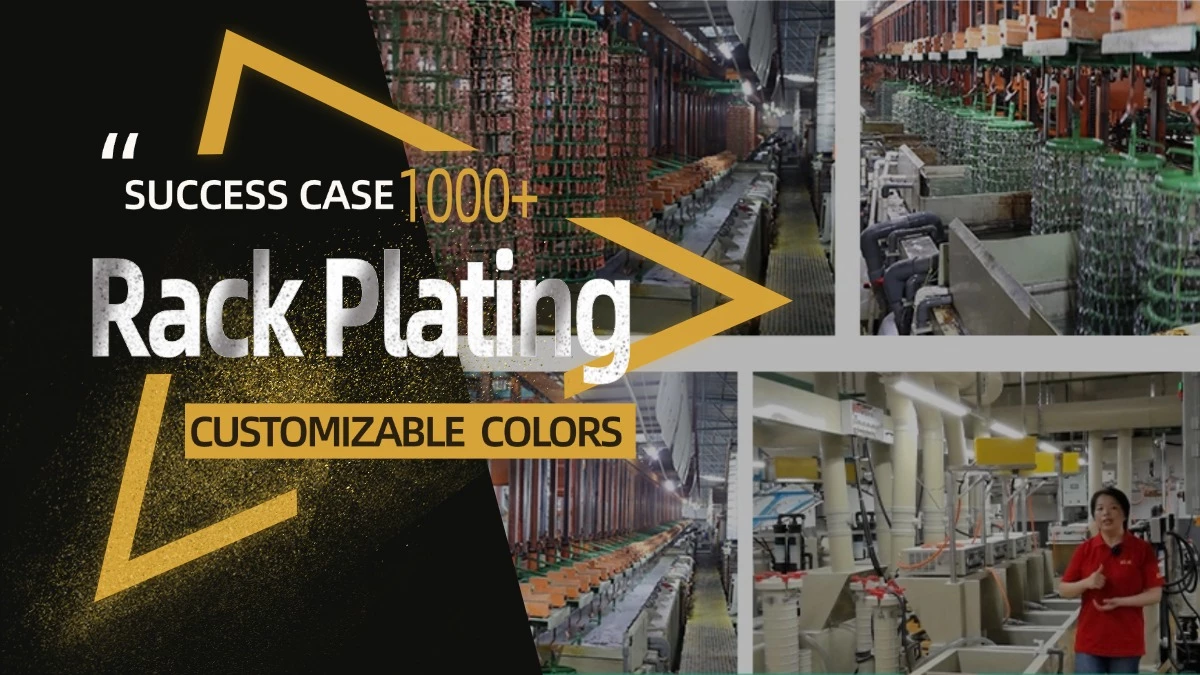
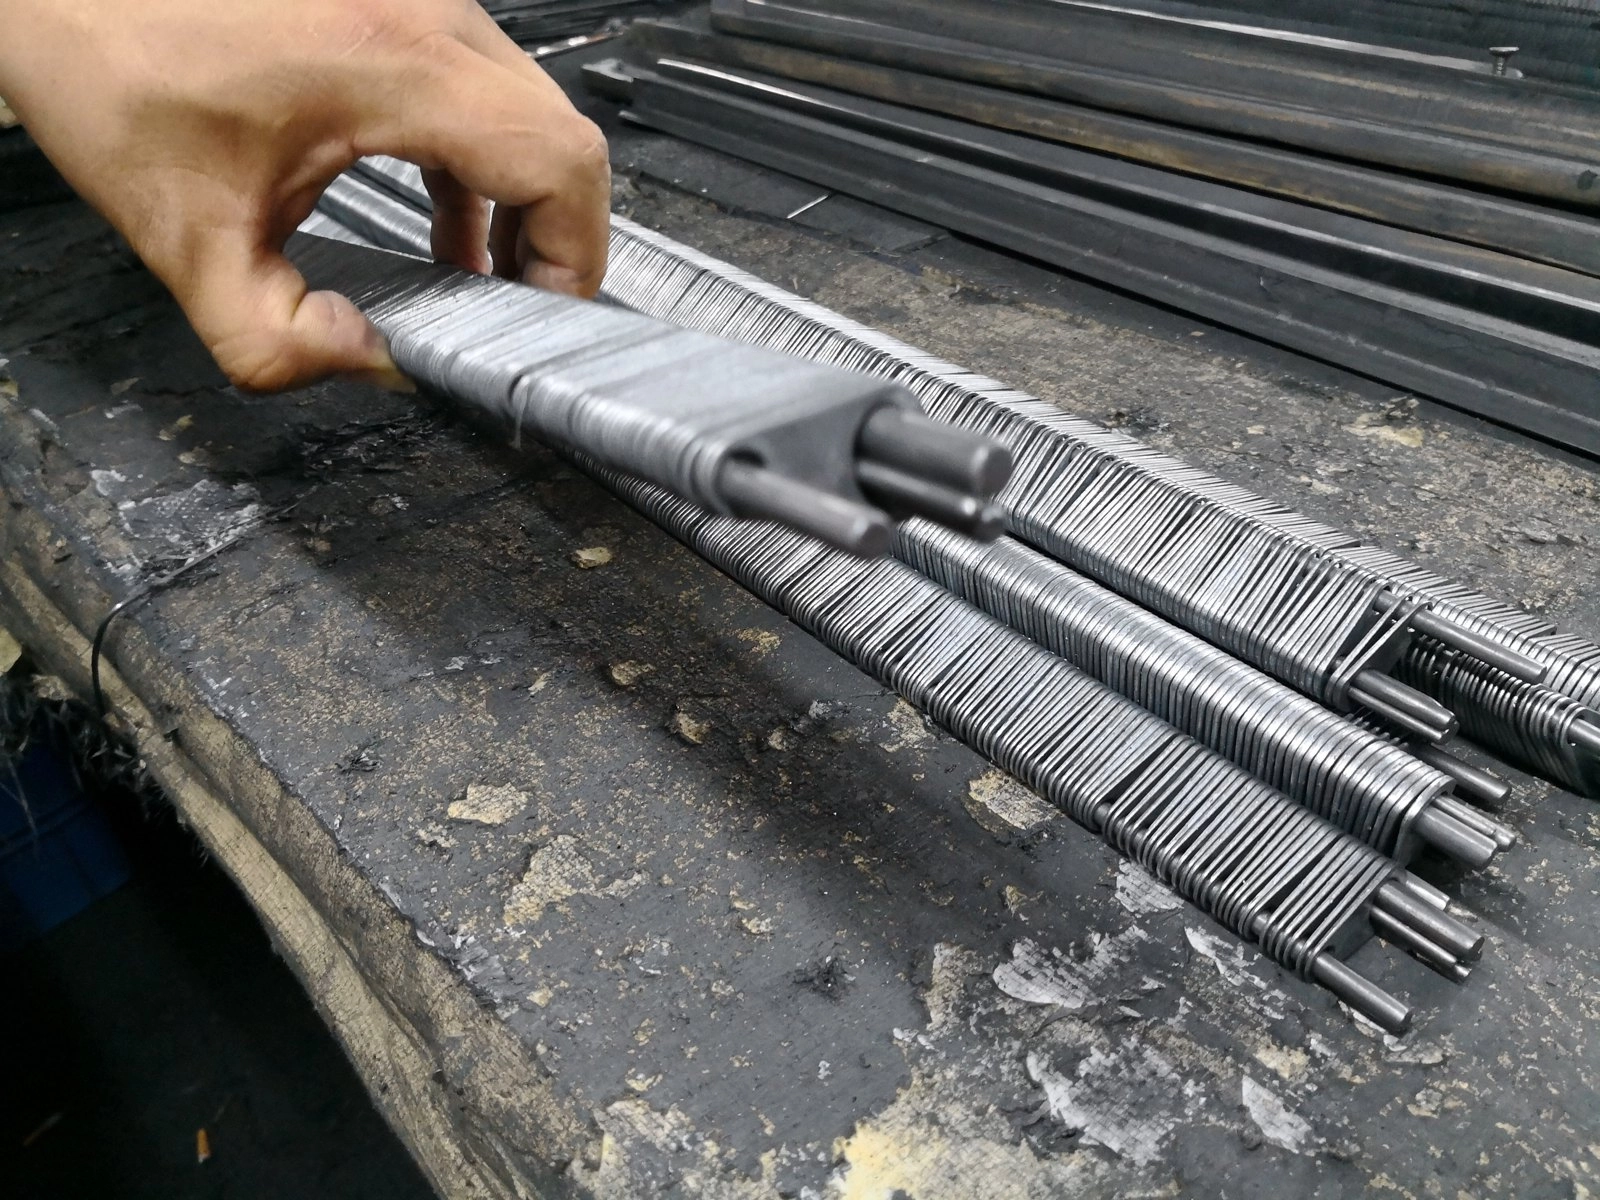
Rack & Fixture Maintenance Manual
Racks are consumable tooling — maintain them like molds. The 6-step routine that cuts rejects 30% and doubles rack life.
The 6-Step Maintenance Routine
What good plating lines do every day, week and month
1Daily Pre-Shift Inspection
Check every rack for broken tips, cracked insulation and loose contacts. One damaged rack contaminates a whole load.
2Periodic Stripping
Copper and nickel build up on racks every cycle. Strip it before it steals current and sheds particles into the bath.
3Insulation Repair
Re-dip damaged plastisol or PVC. Exposed frame metal causes rack marks, shorts and stray current.
4Contact Point Service
File contact tips back to sharp, clean metal. Oxidized tips = resistance = burnt parts.
5Load / Thermal Testing
Run the rack at full current and scan with IR. Any hot spot >10 °C above rack average is a future reject generator.
6Vertical Dry Storage
Hang racks on stands, never stack or lean them. Bent frames and cracked insulation start in the storage corner, not the tank.
Rack Materials Compared
Copper for economy, titanium for life
| Rack Type | Core Material | Best For | Contact | Service Life |
|---|---|---|---|---|
| Copper core | Cu + PVC coat | General, high current | Spring clip / screw | 1–2 yrs |
| Titanium | Ti | Corrosive baths | Spring clip | 5–10 yrs |
| Stainless | SS316 + coat | Acid copper, nickel | Bolt / clamp | 3–5 yrs |
| Aluminum | Anodized Al | Light loads | Spring clip | 1–2 yrs |
| Custom fixture | Mixed | Odd shapes, automation | Engineered | Varies |
What Neglect Actually Costs
Maintenance is cheaper than rejects every time
| Problem | Cost of Neglect | Prevention | You Save |
|---|---|---|---|
| Rack marks | 5–10% reject rate | $50 rack repair | $2000+/mo |
| Burnt parts (bad contact) | Scrap + rework | $20 tip service | $500+/incident |
| Bath contamination | $5000+ bath dump | $200 strip cycle | $4800+/cycle |
| Rack dropped in tank | 2–4 h line stop | $100/mo inspection | $1000+/day |
📌 Rack Maintenance Cheat Sheet
FAQ
When should a rack be scrapped?
In-house repair or send out?
Black spots on parts near contact points?
Custom racks for our part shape?
Get a Free Quote Today
Send us your samples or drawings — our engineers reply within 24 hours with pricing and technical advice.
Contact UsRack inspection checklist
| Item | Check | Frequency |
|---|---|---|
| Contact tips | Clean, spring tension, no build-up | Every cycle |
| Coating | No cracks or exposed copper | Weekly |
| Hooks and frame | No bent arms, no corrosion | Monthly |
| Identification | Part number and rack tag legible | Every rack |
FAQ
How often should racks be stripped?
When coating build-up starts bridging or contact marks appear. Typically every 20-40 cycles depending on bath.
Why do we get recurring rejects on one rack position?
Usually a single contact tip losing tension. Tag the rack, test it on a control part.