
Pretreatment for rack plating
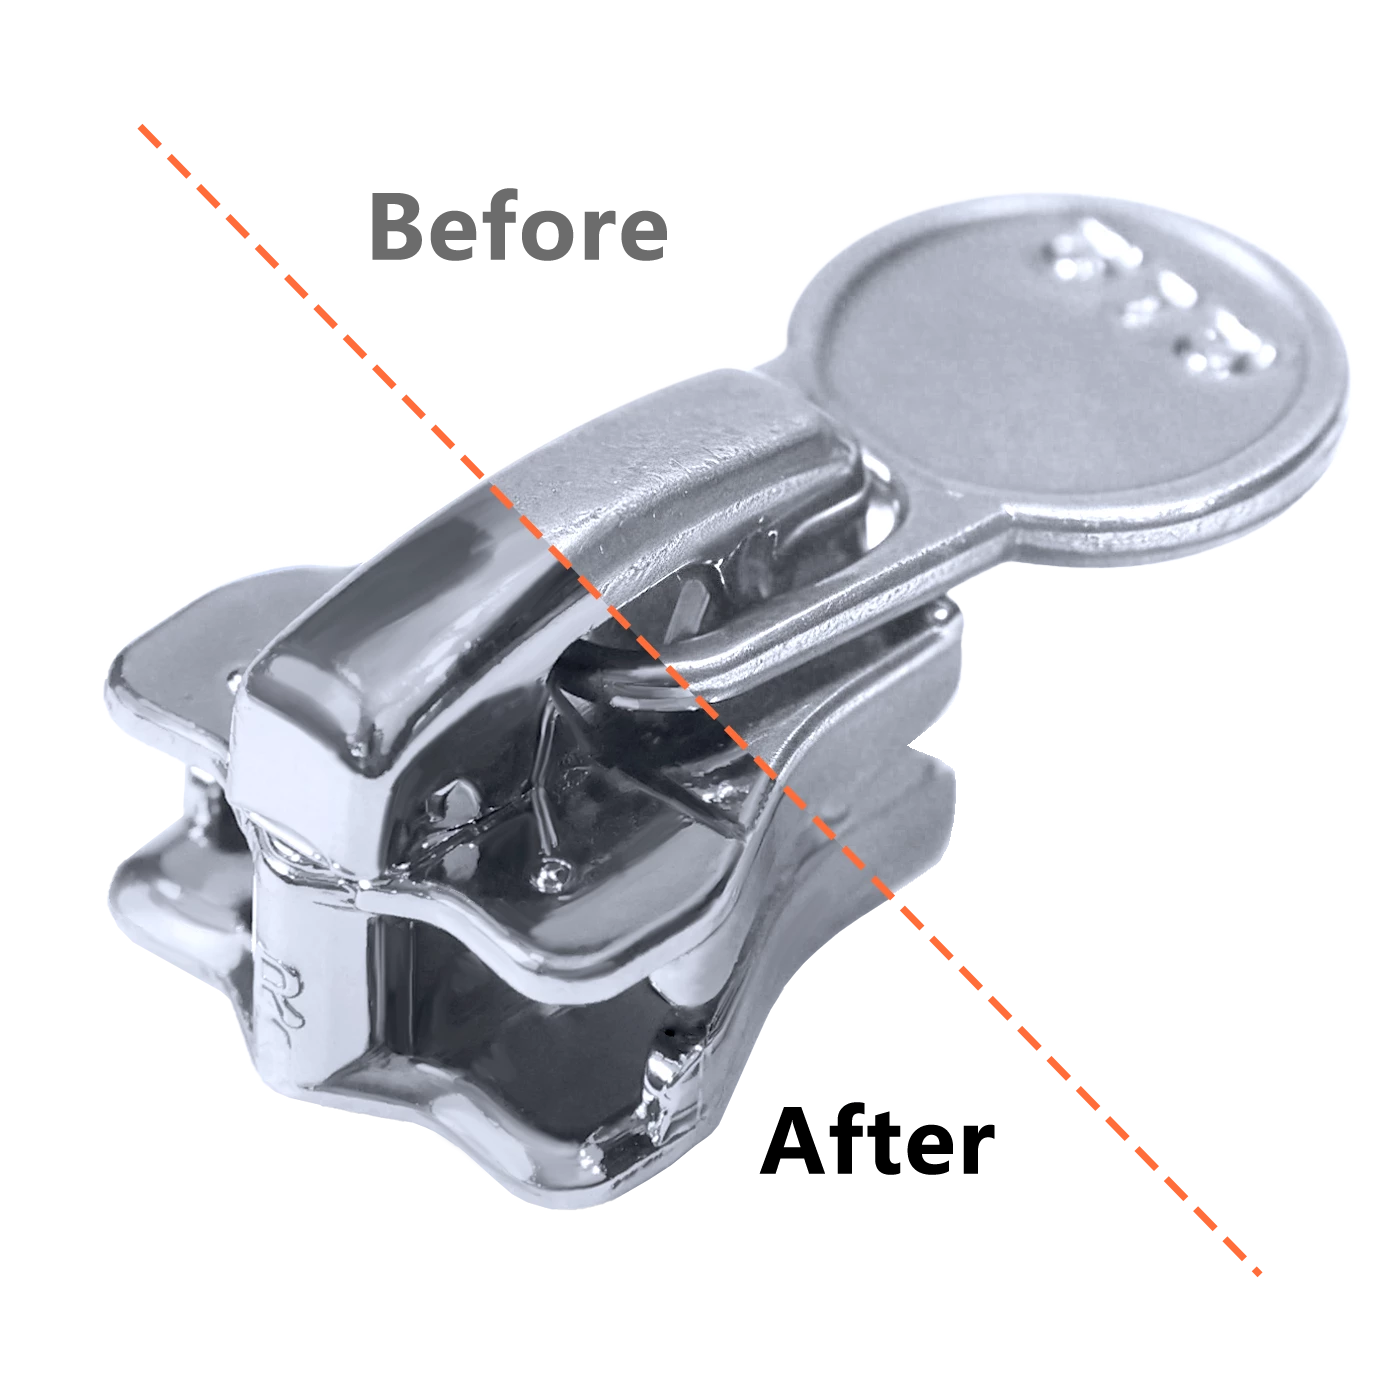
Rack plating pretreatment is the most critical step in the rack plating process (it usually accounts for more than 60% of the total process time, and 60%-80% of plating quality defects arise from improper pretreatment). Its core function is to create a clean, activated and uniform surface condition for subsequent plating, so as to ensure the quality and performance of the plating layer.
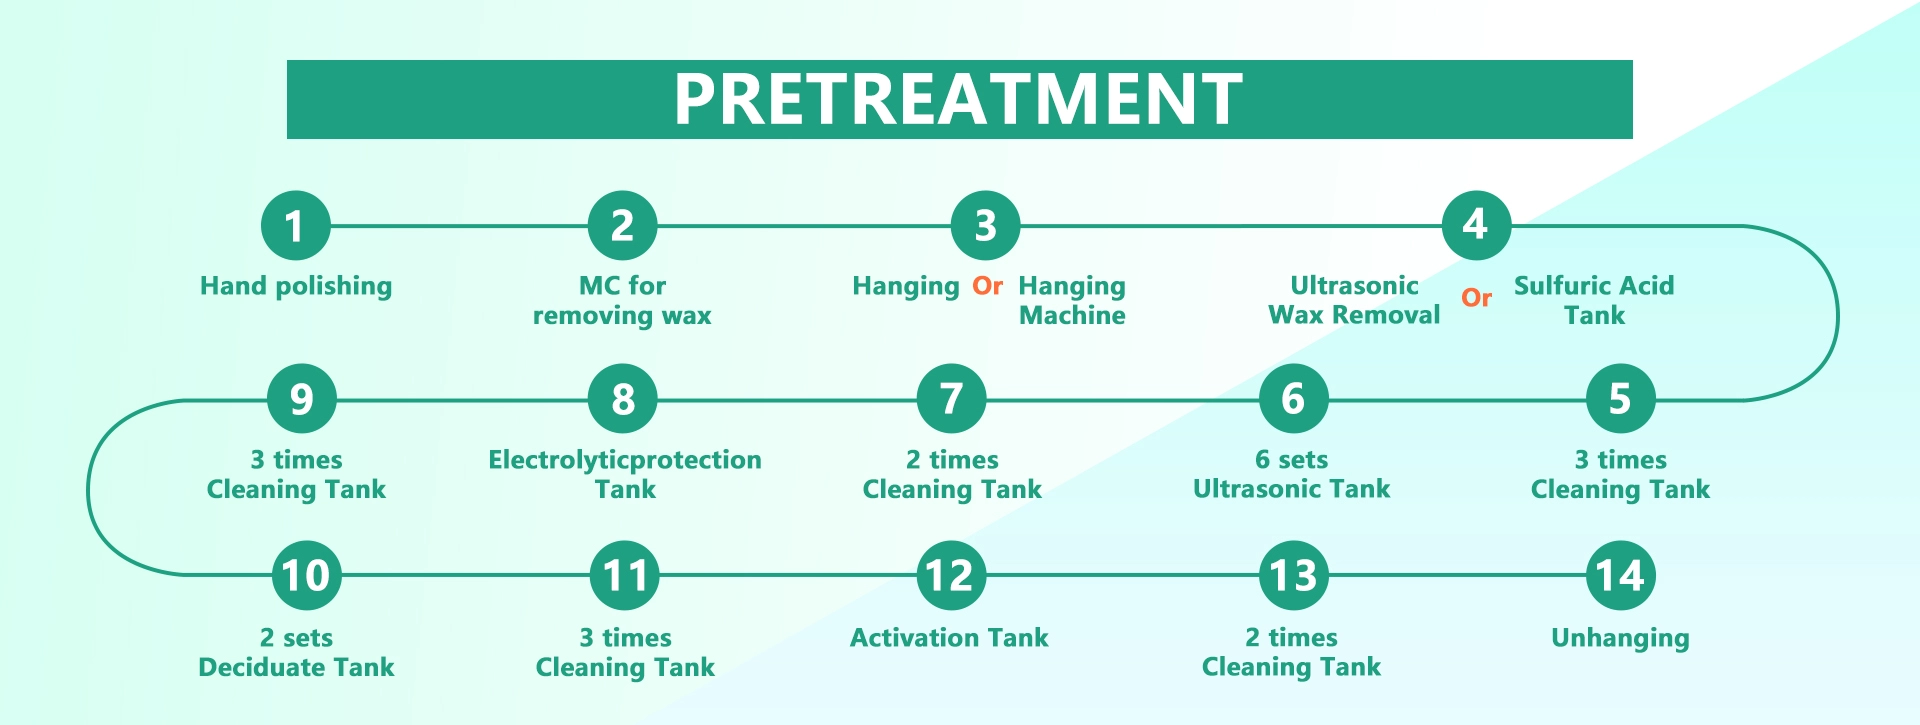
1. Process Flow Chart
2. Process Video
3. Process Details
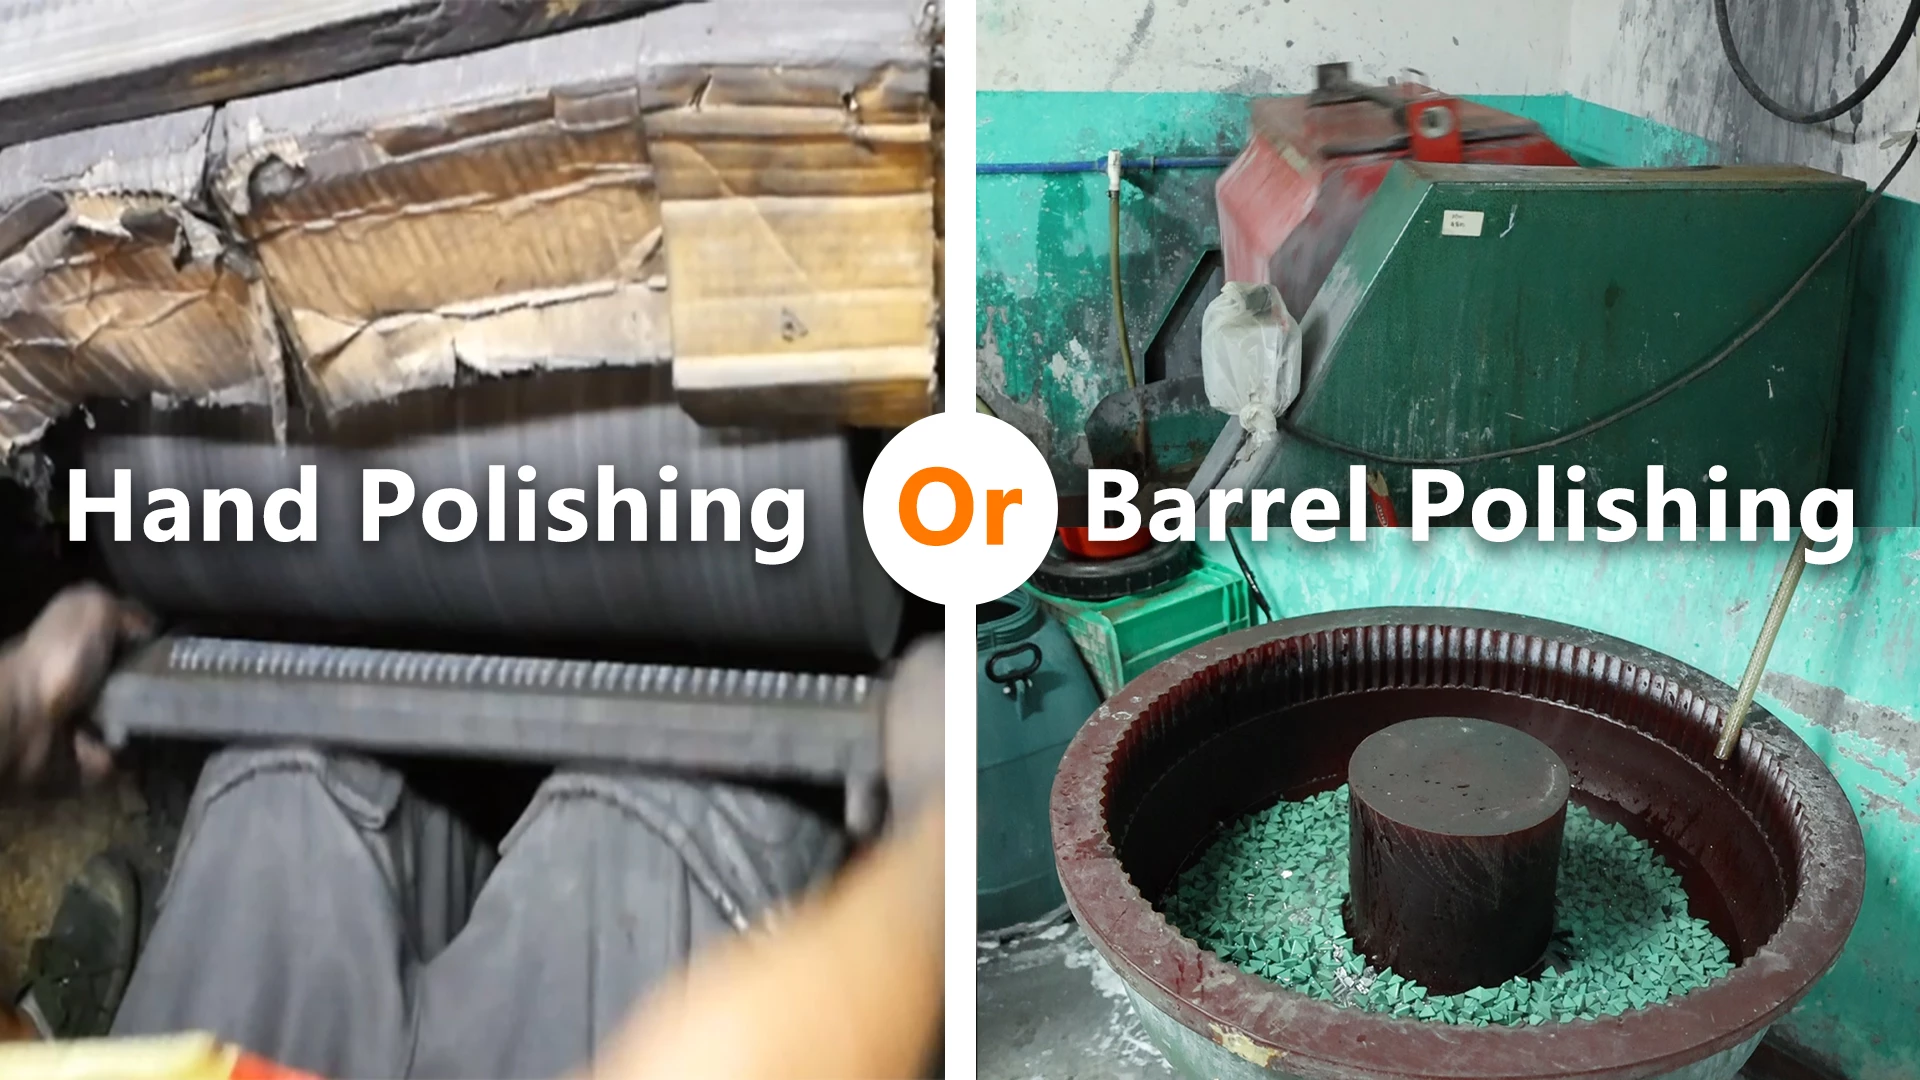
1. Hand Polishing Or Barrel Polishing
Hand polishing is suitable for high-end products, while barrel polishing is recommended for ordinary products. Polish unevenness, burrs, grinding marks, water stains and other defects on the product surface to make the electroplated products more full and bright, achieving a mirror - like finish.
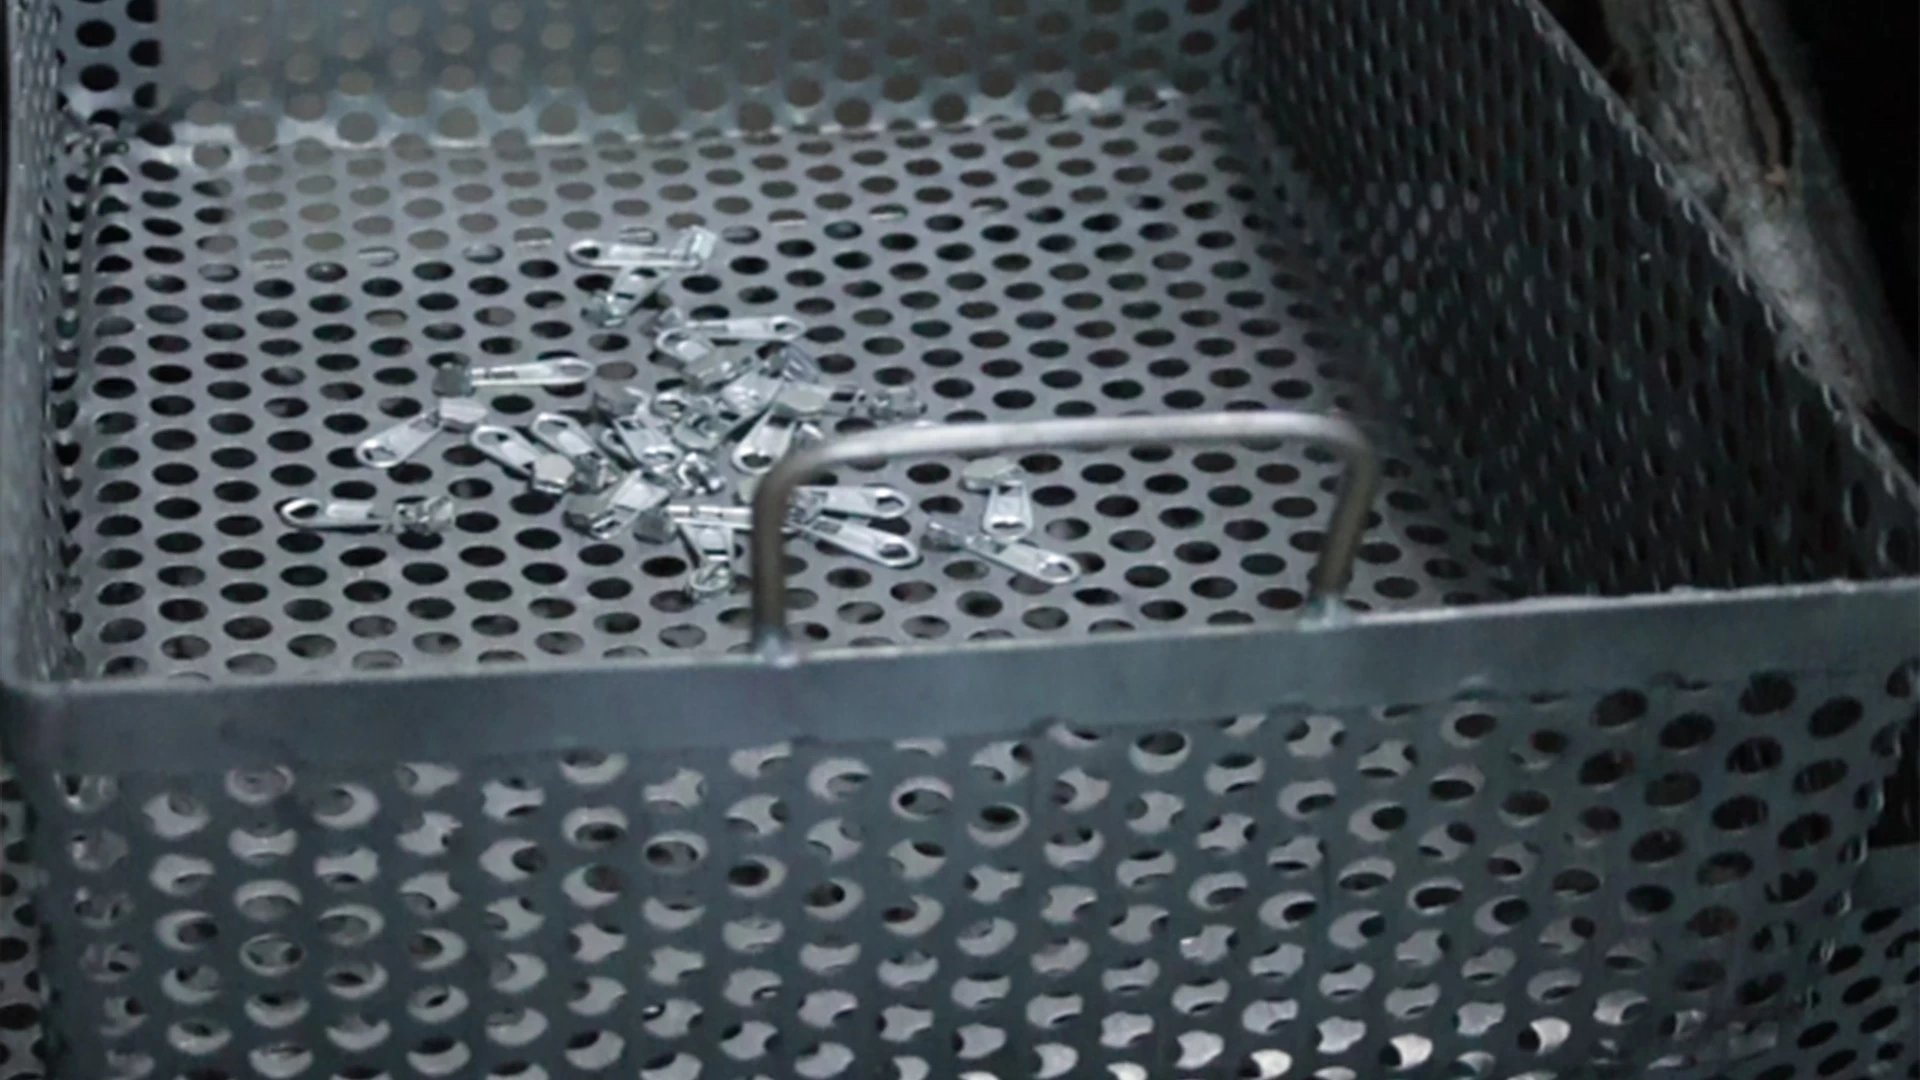
2. MC for removing wax
Remove wax from hand-polished products and dry them thoroughly.
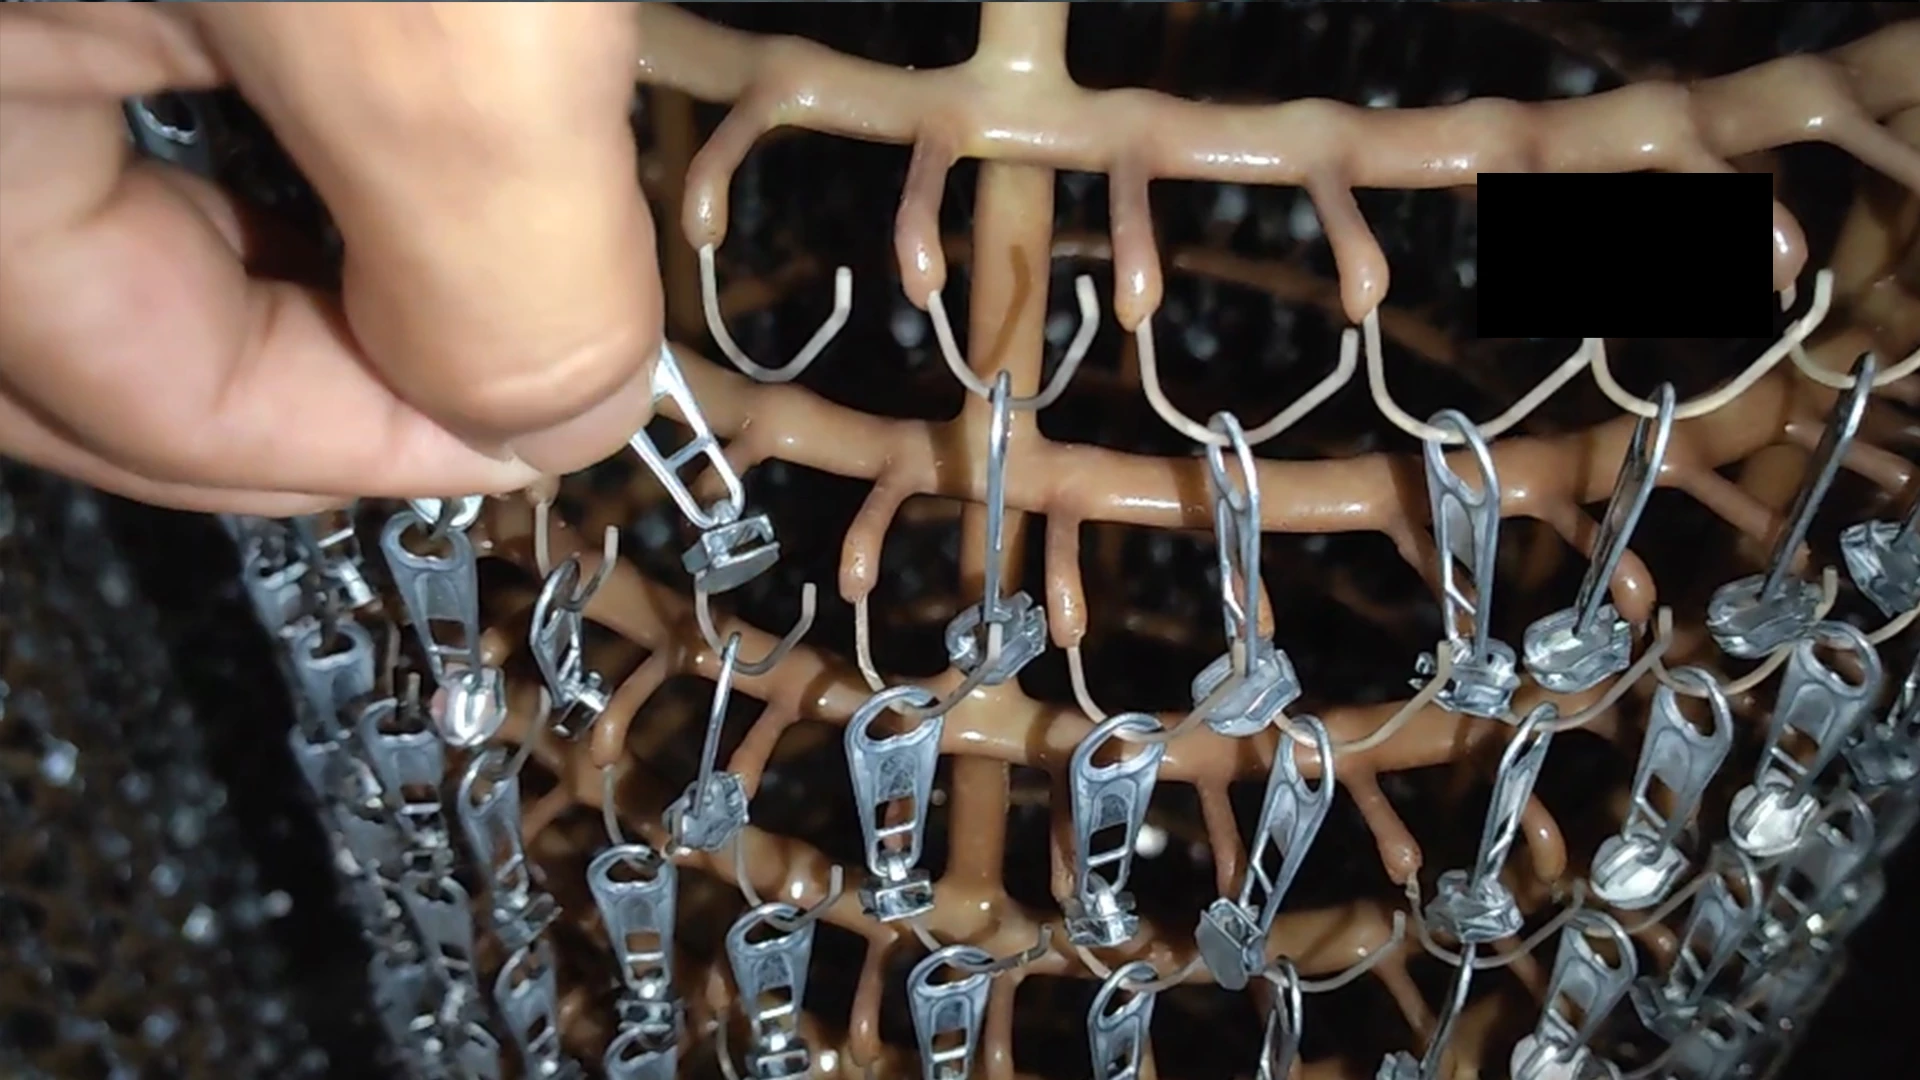
3. Hanging or hanging machine
Hang the hardware parts on special fixtures and avoid collision and scratch of the workpieces.
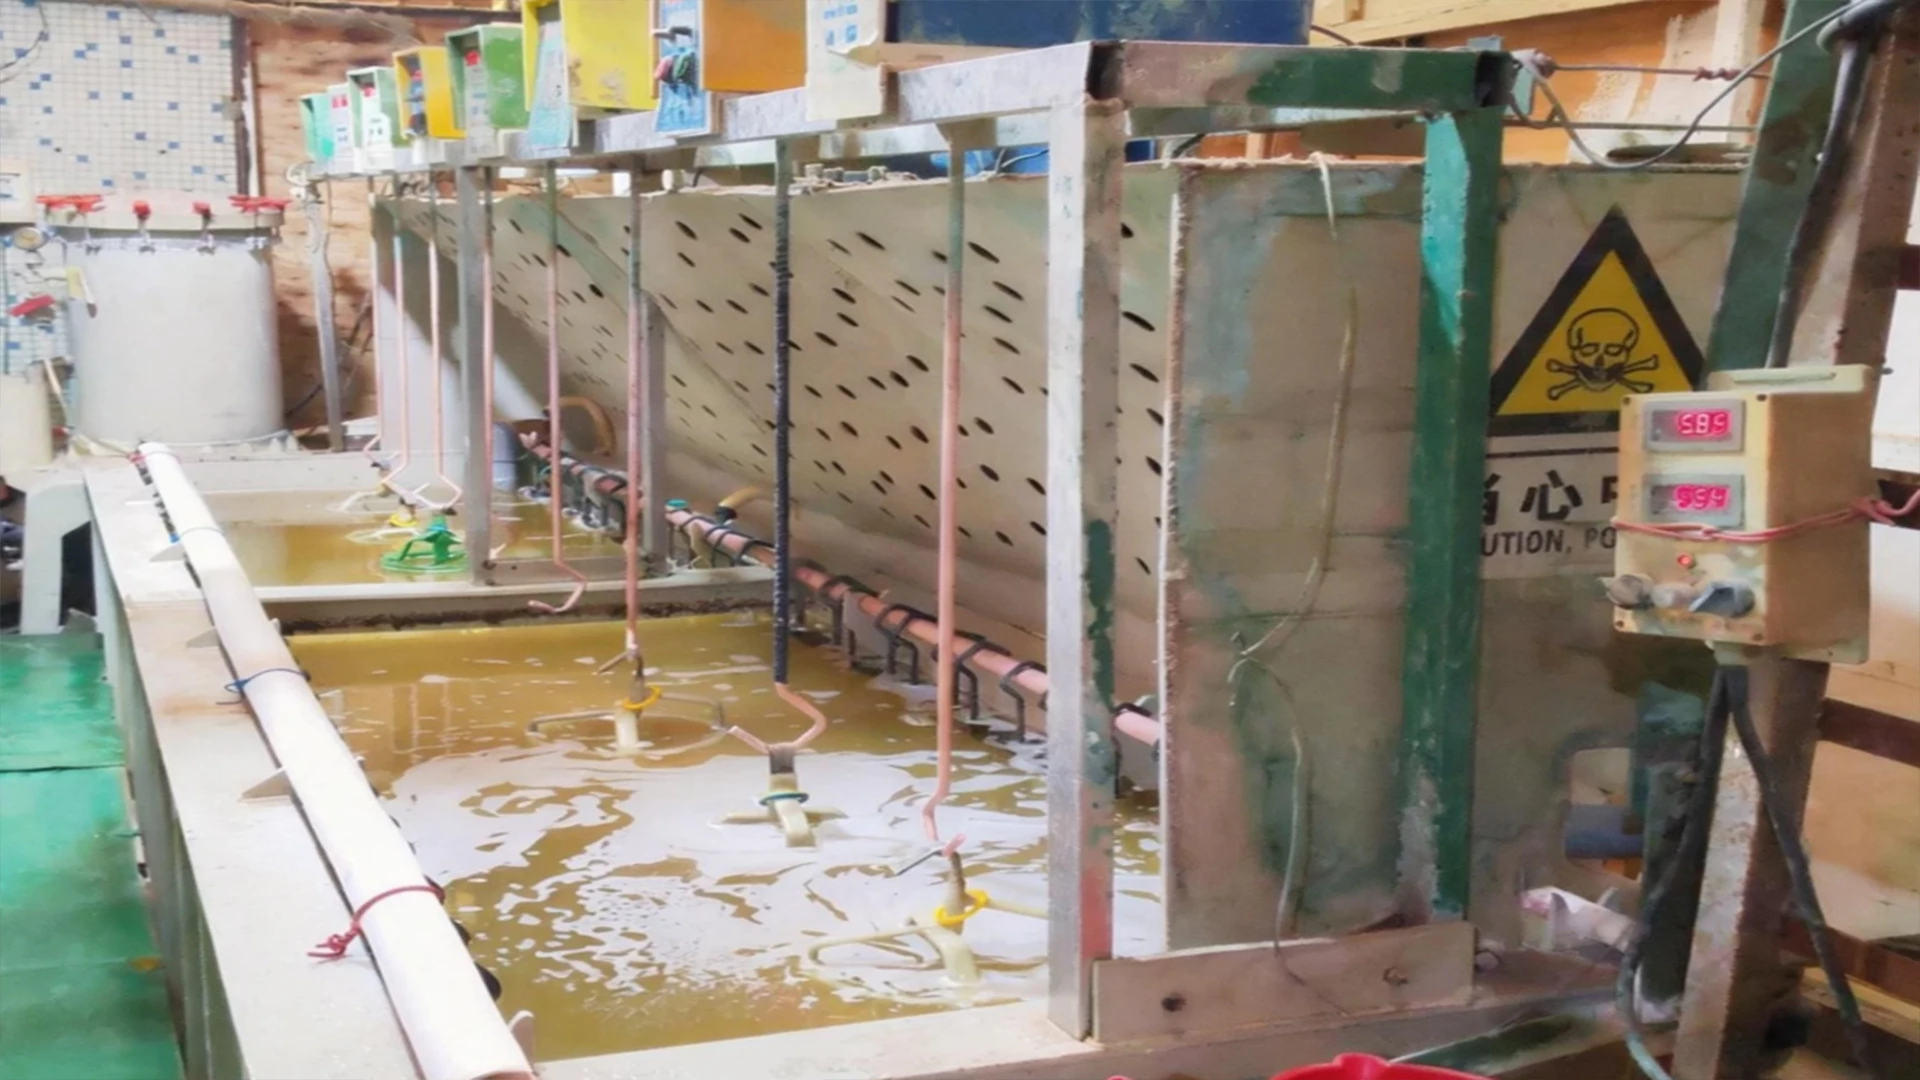
4-1. Sulfuric Acid Tank
Wax Removal / Oil Removal. If the wax is not completely removed, the residual wax or oil will result in poor product quality.
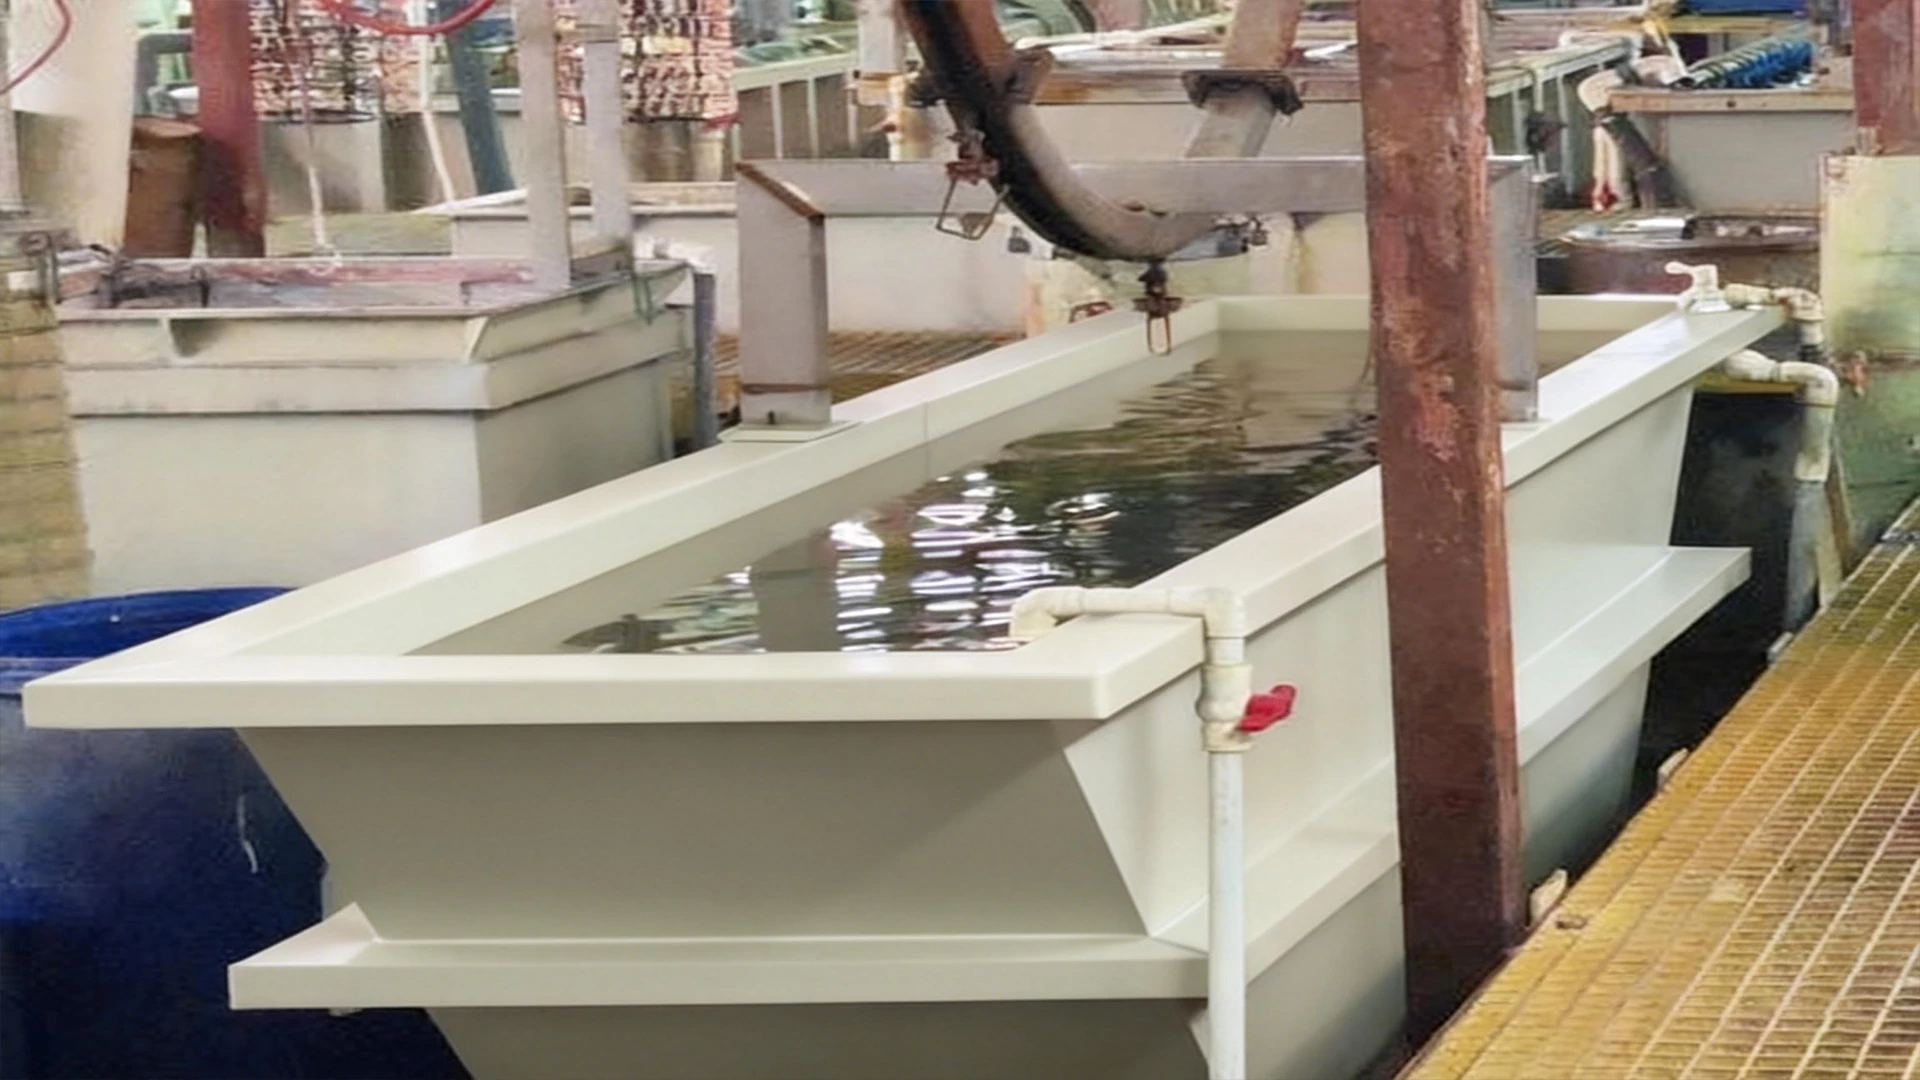
4-1-1. Recycling Tank
Pre-rinsing in recovery tank (30-60 seconds to dissolve concentrated sulfuric acid adhering to the surface) Drain residual liquid
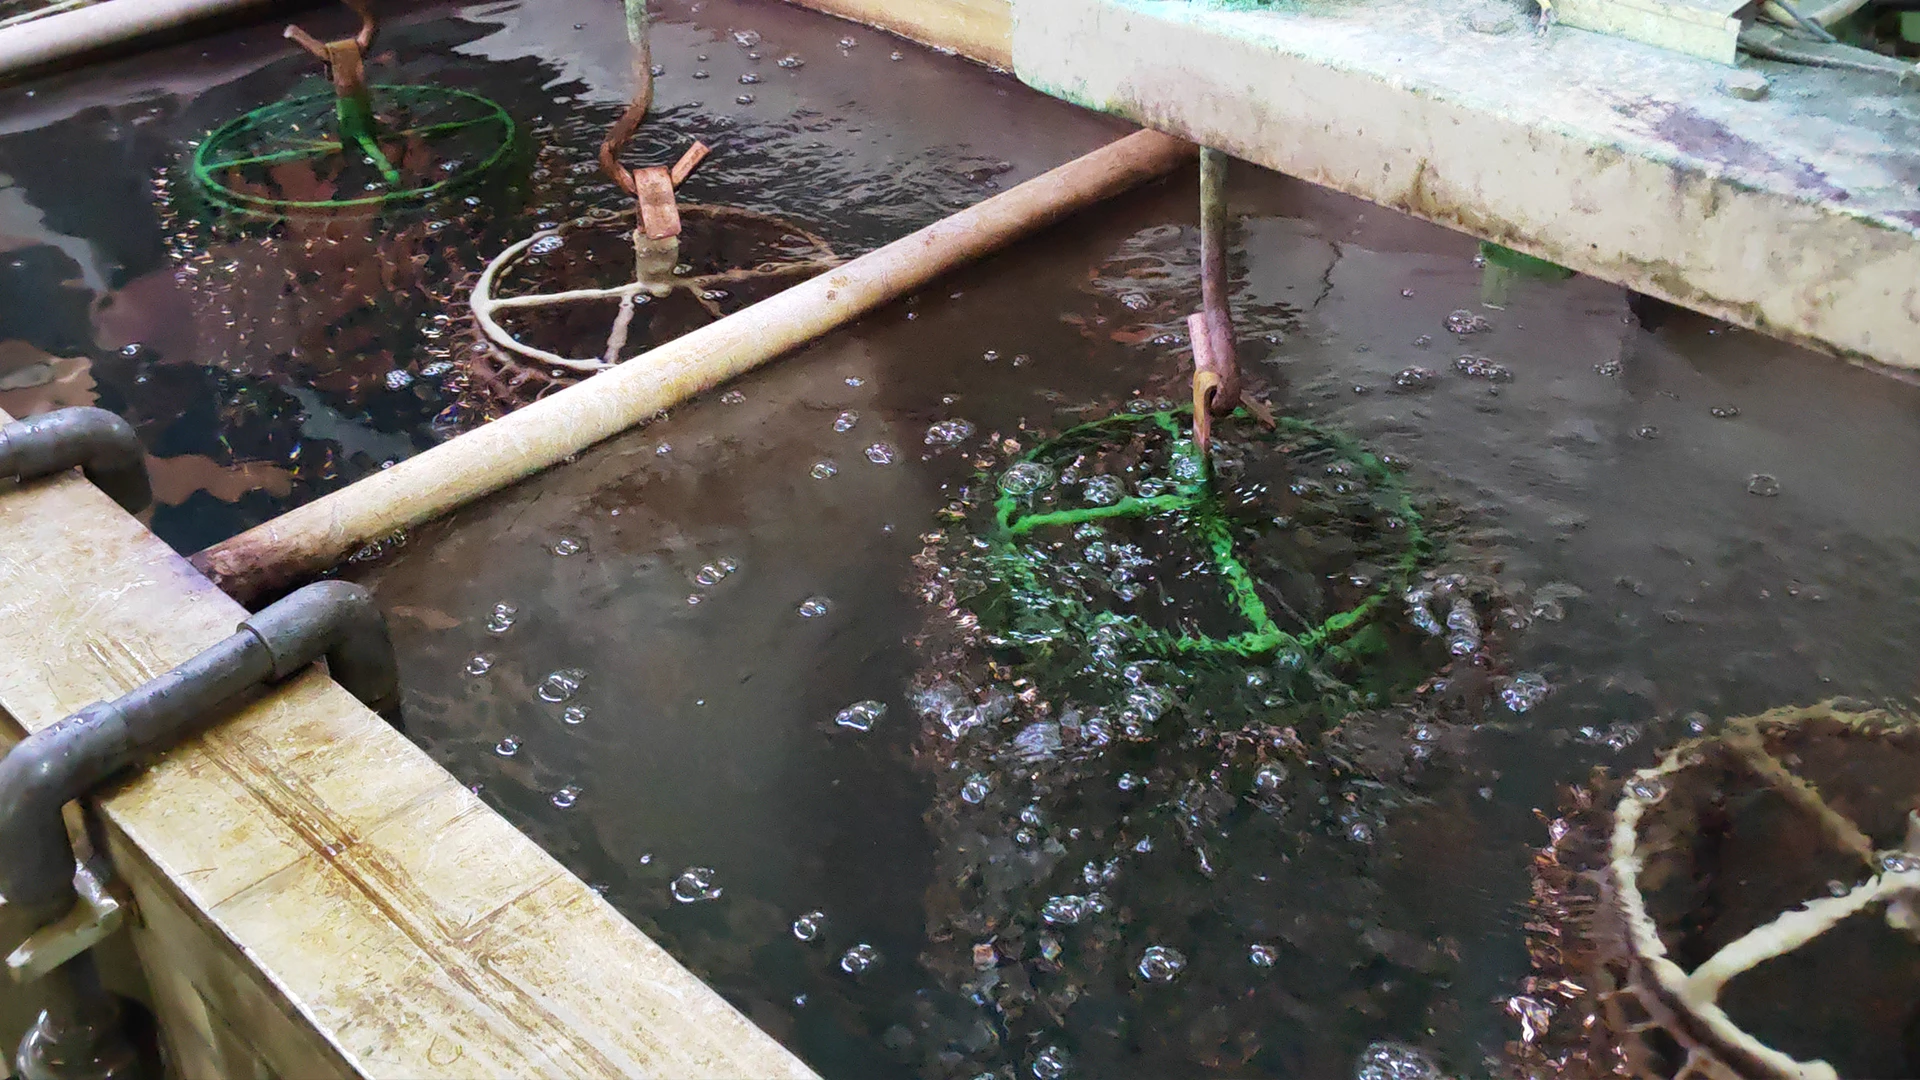
4-2. Ultrasonic Wax Removal (Alternative to the sulfuric acid tank)
Remove wax and oil on the workpiece surface and inside complex structures
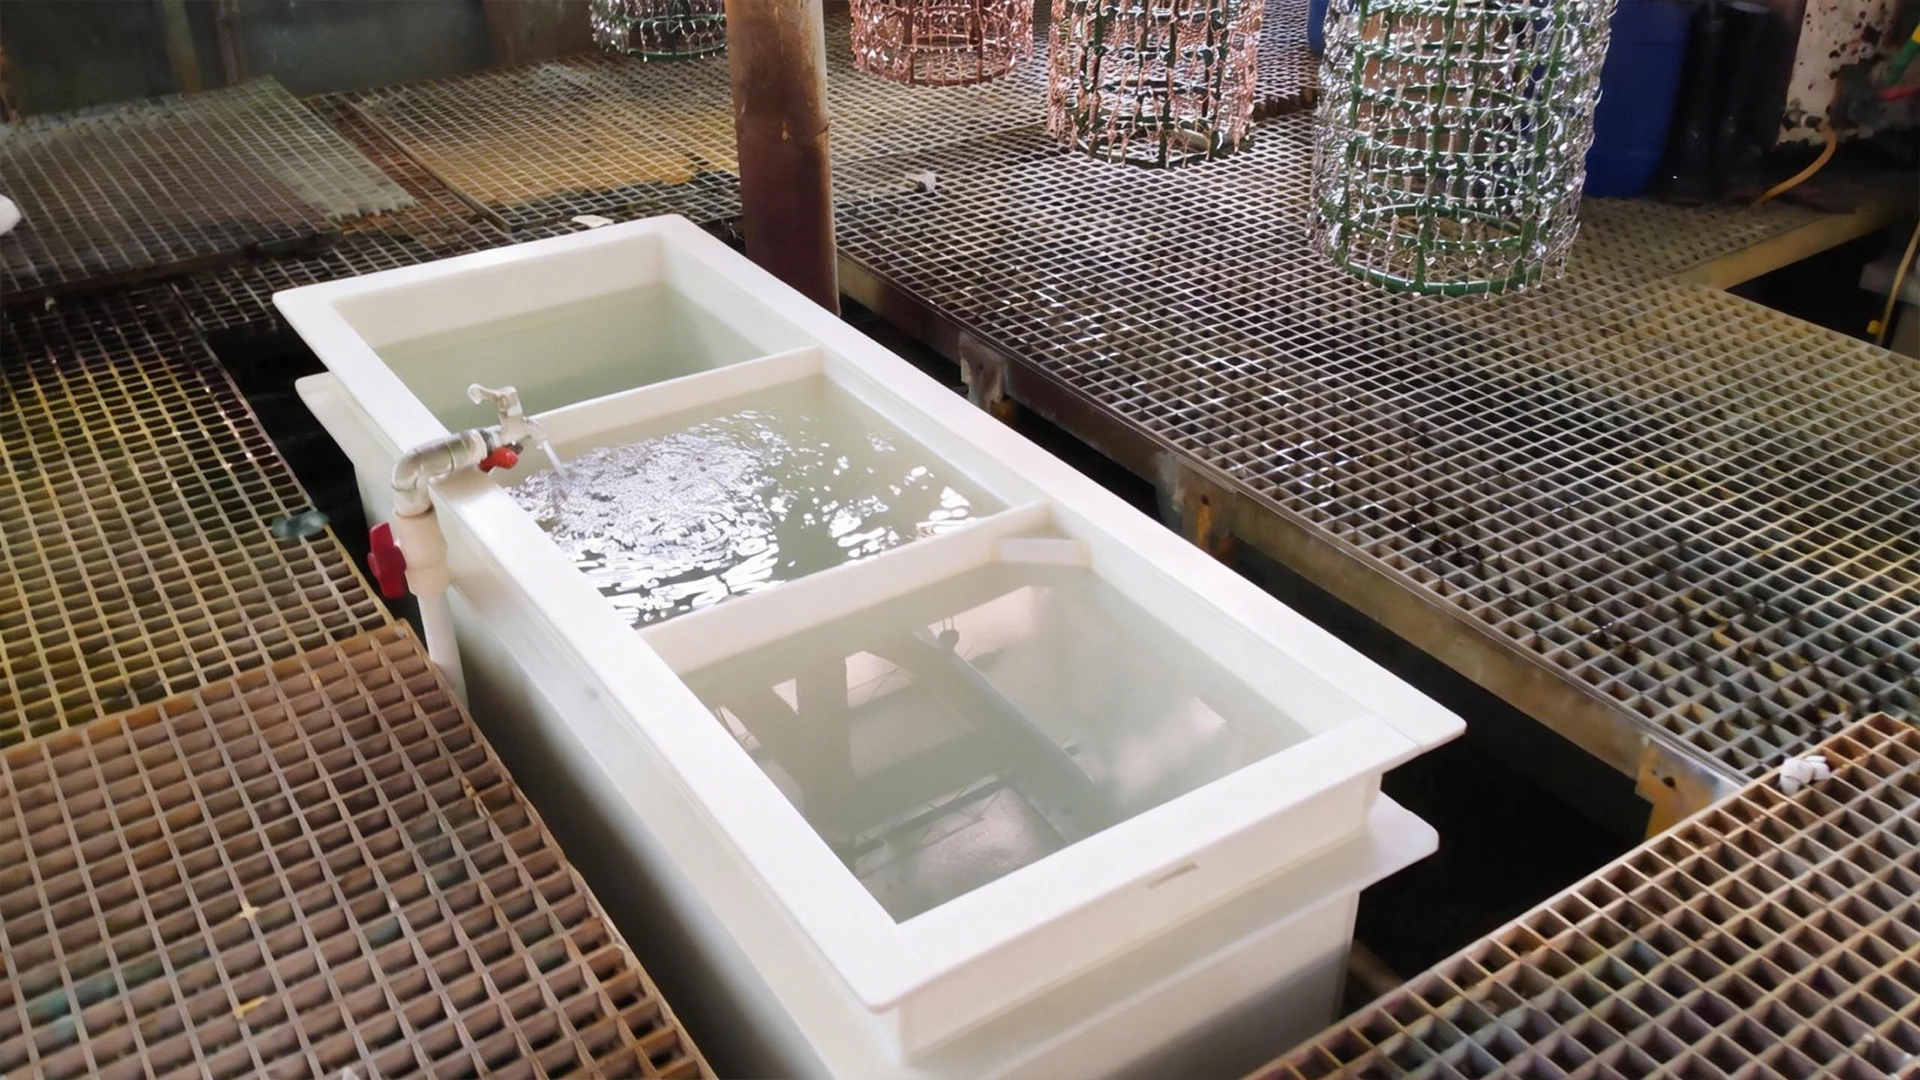
5. Three times Cleaning Tank
Remove residual liquid on the workpiece surface.
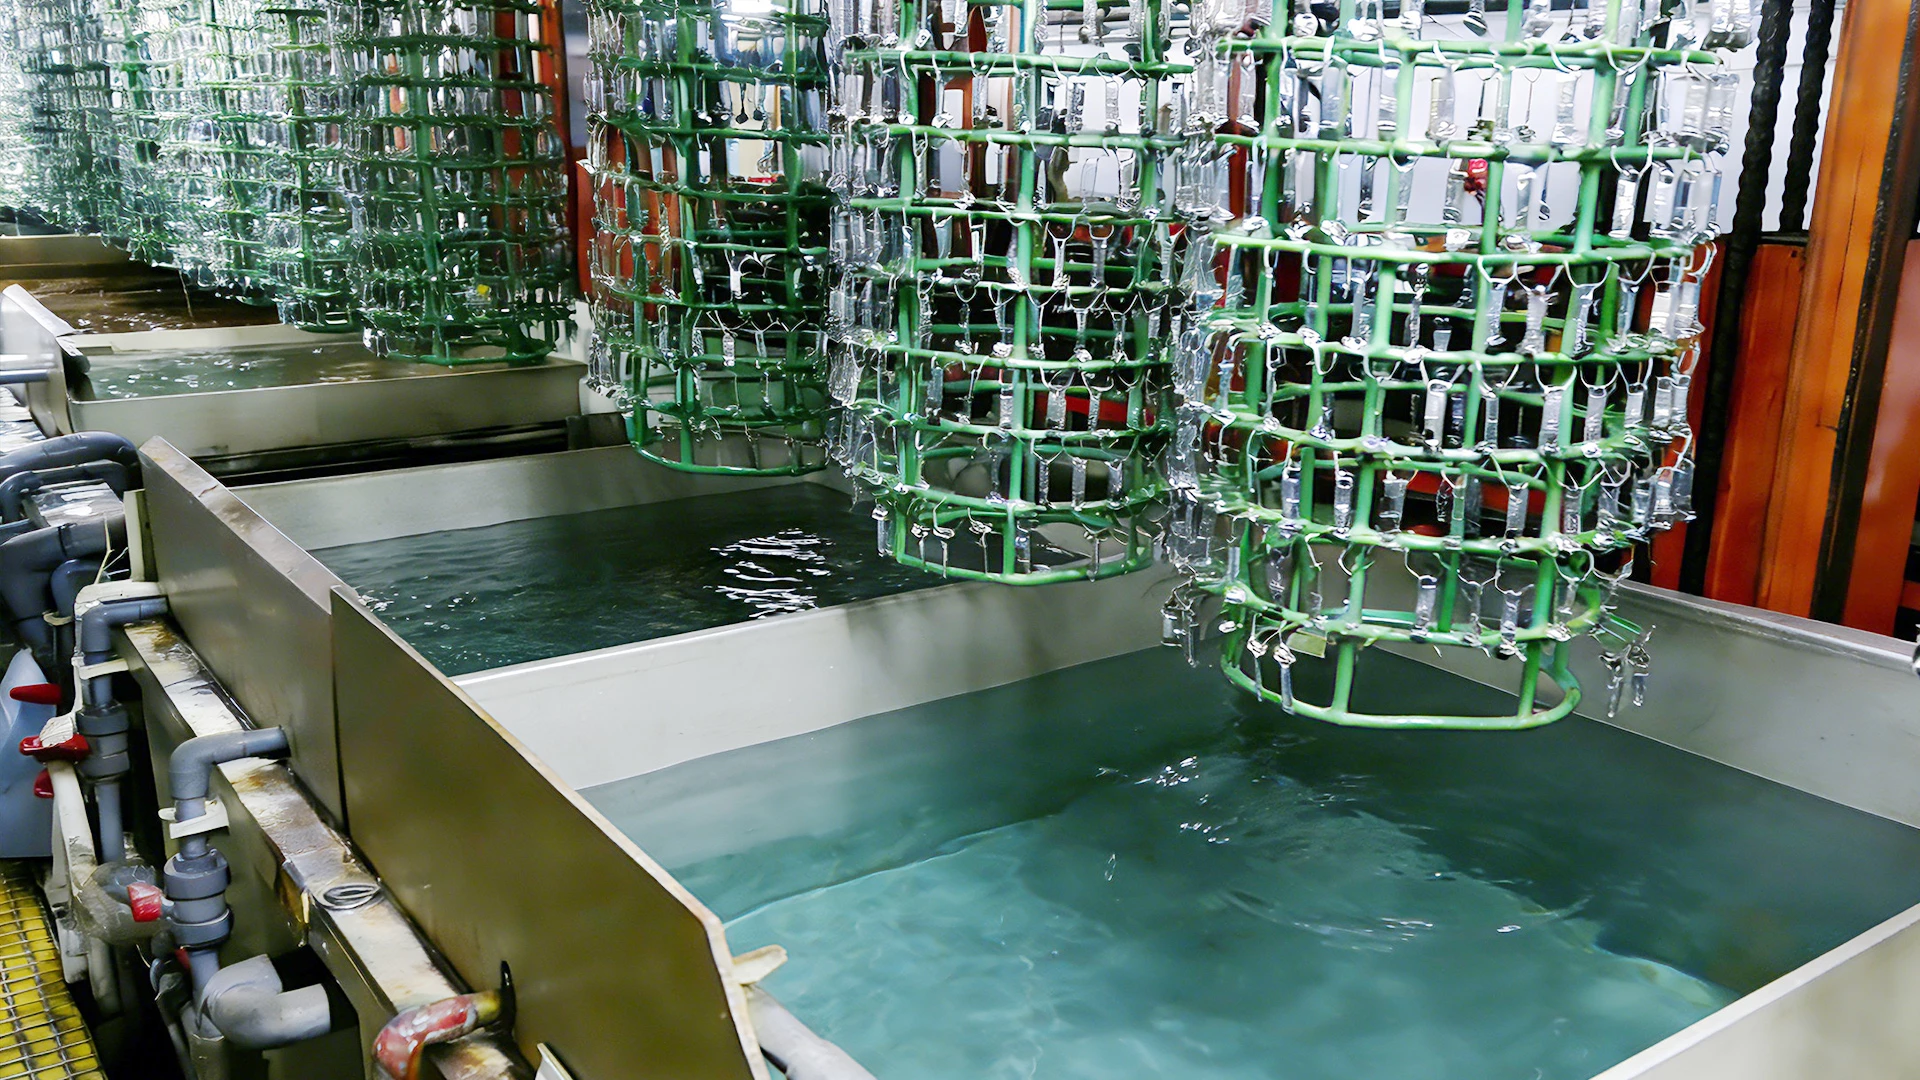
6. Six sets Ultrasonic Tank
Get rid of moisture and electroplating solution better.
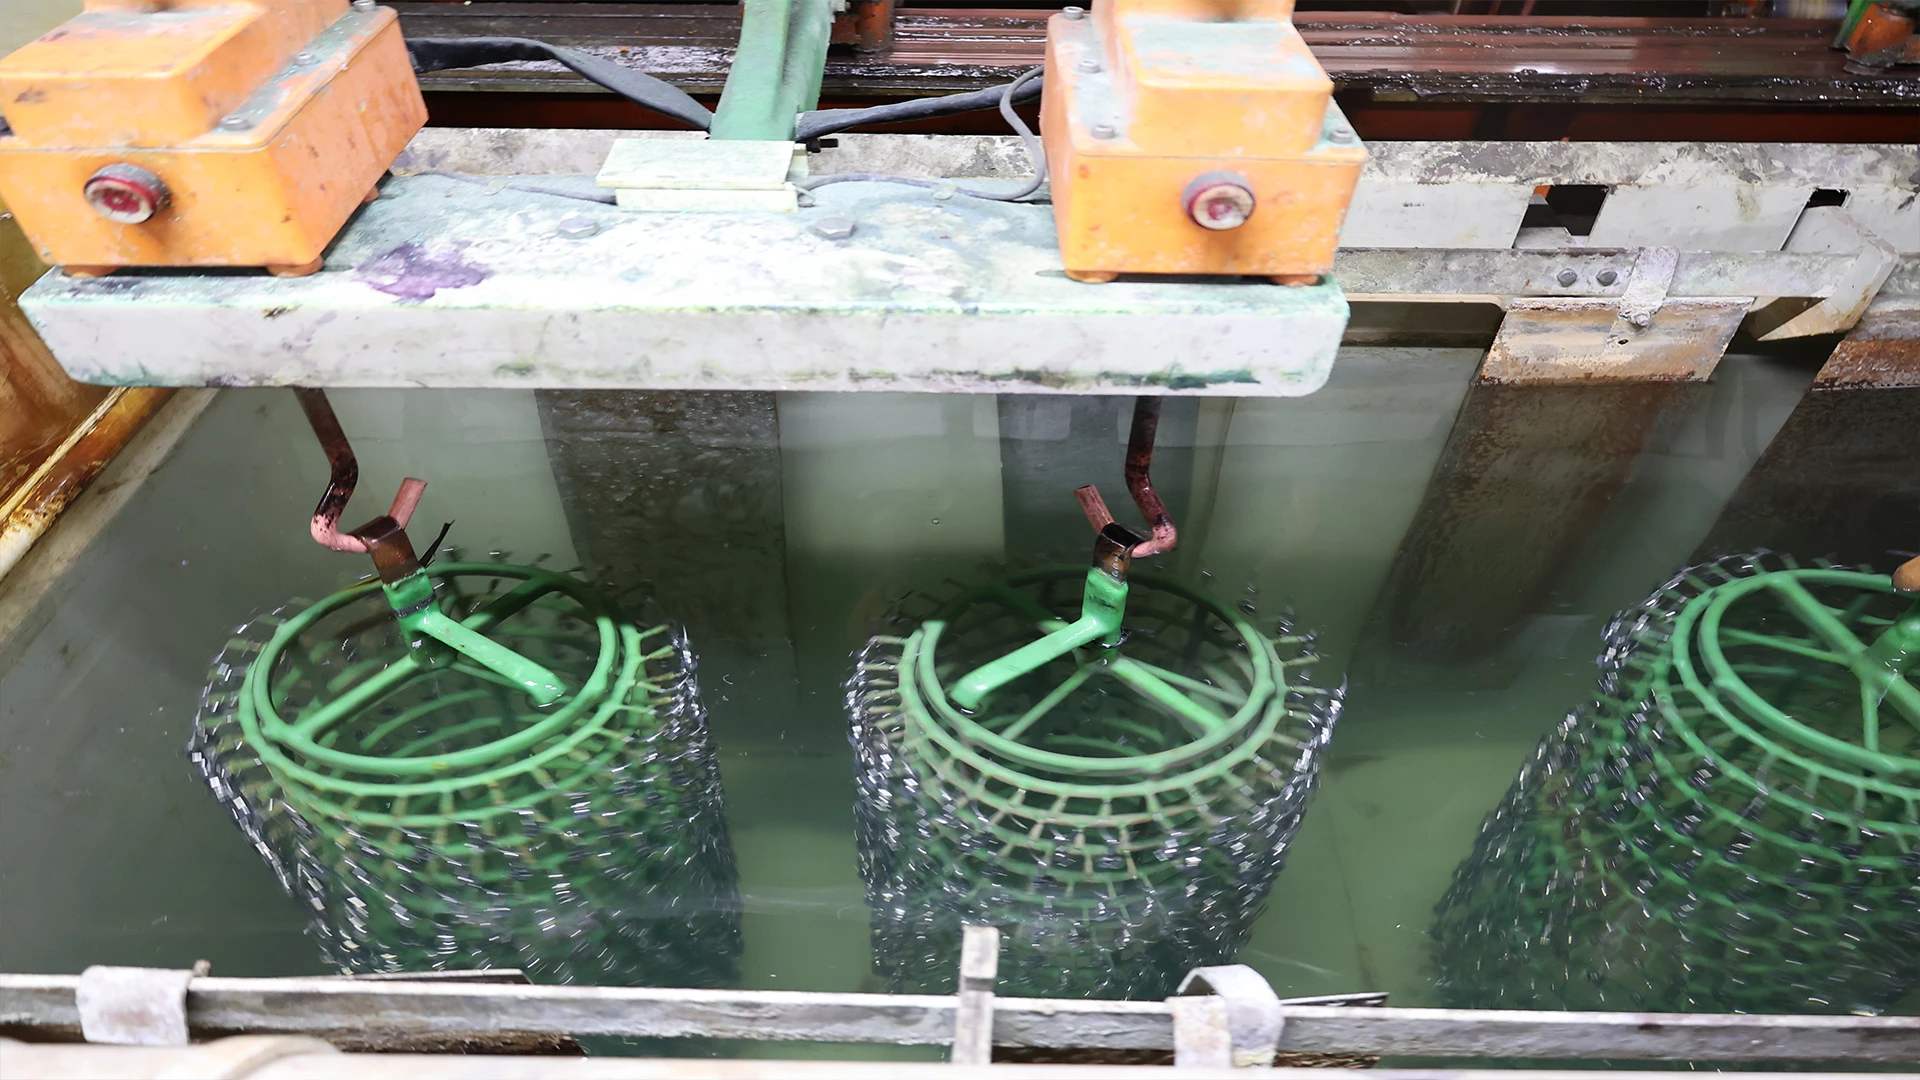
7. Two times Cleaning Tank
Remove residual liquid on the workpiece surface.
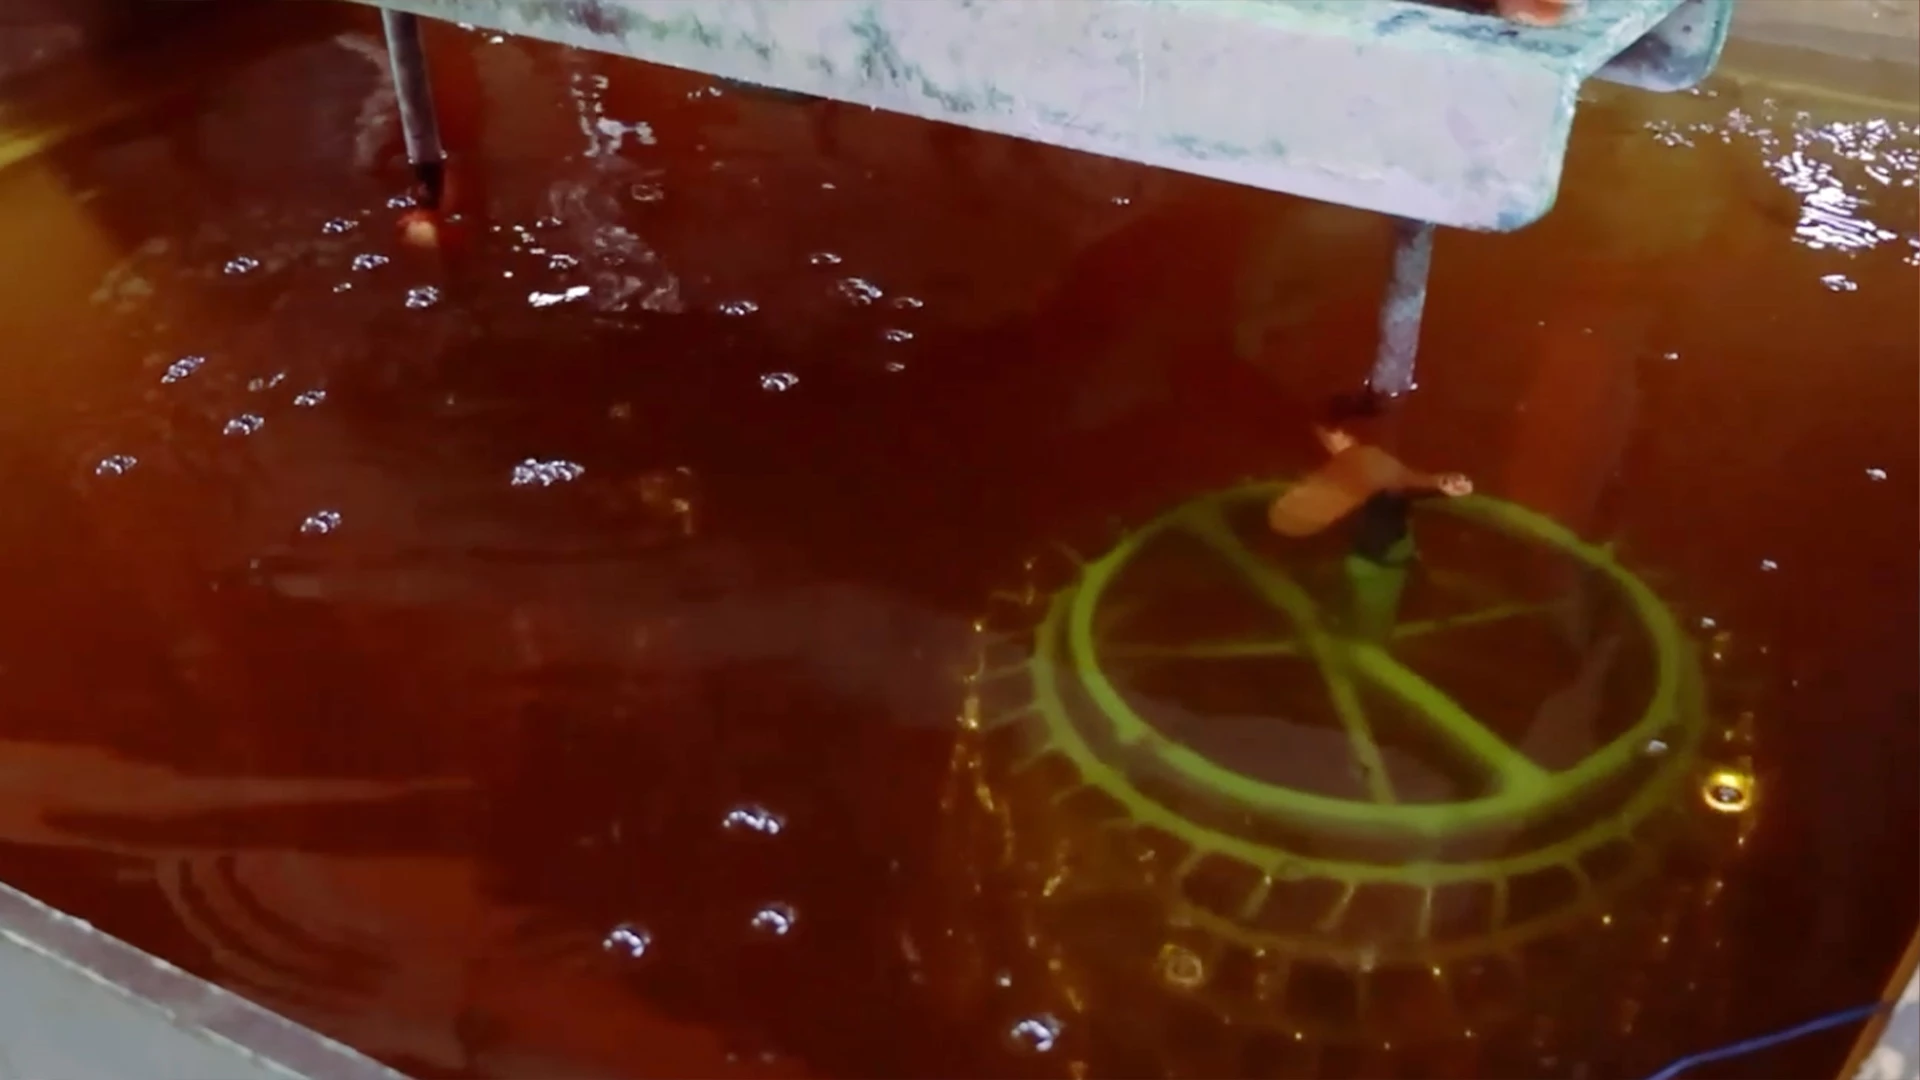
8. Electrolyticprotection Tank
Degrease again to break down impurities, and remove and clean out residues from the holes, gaps or joints of the products.
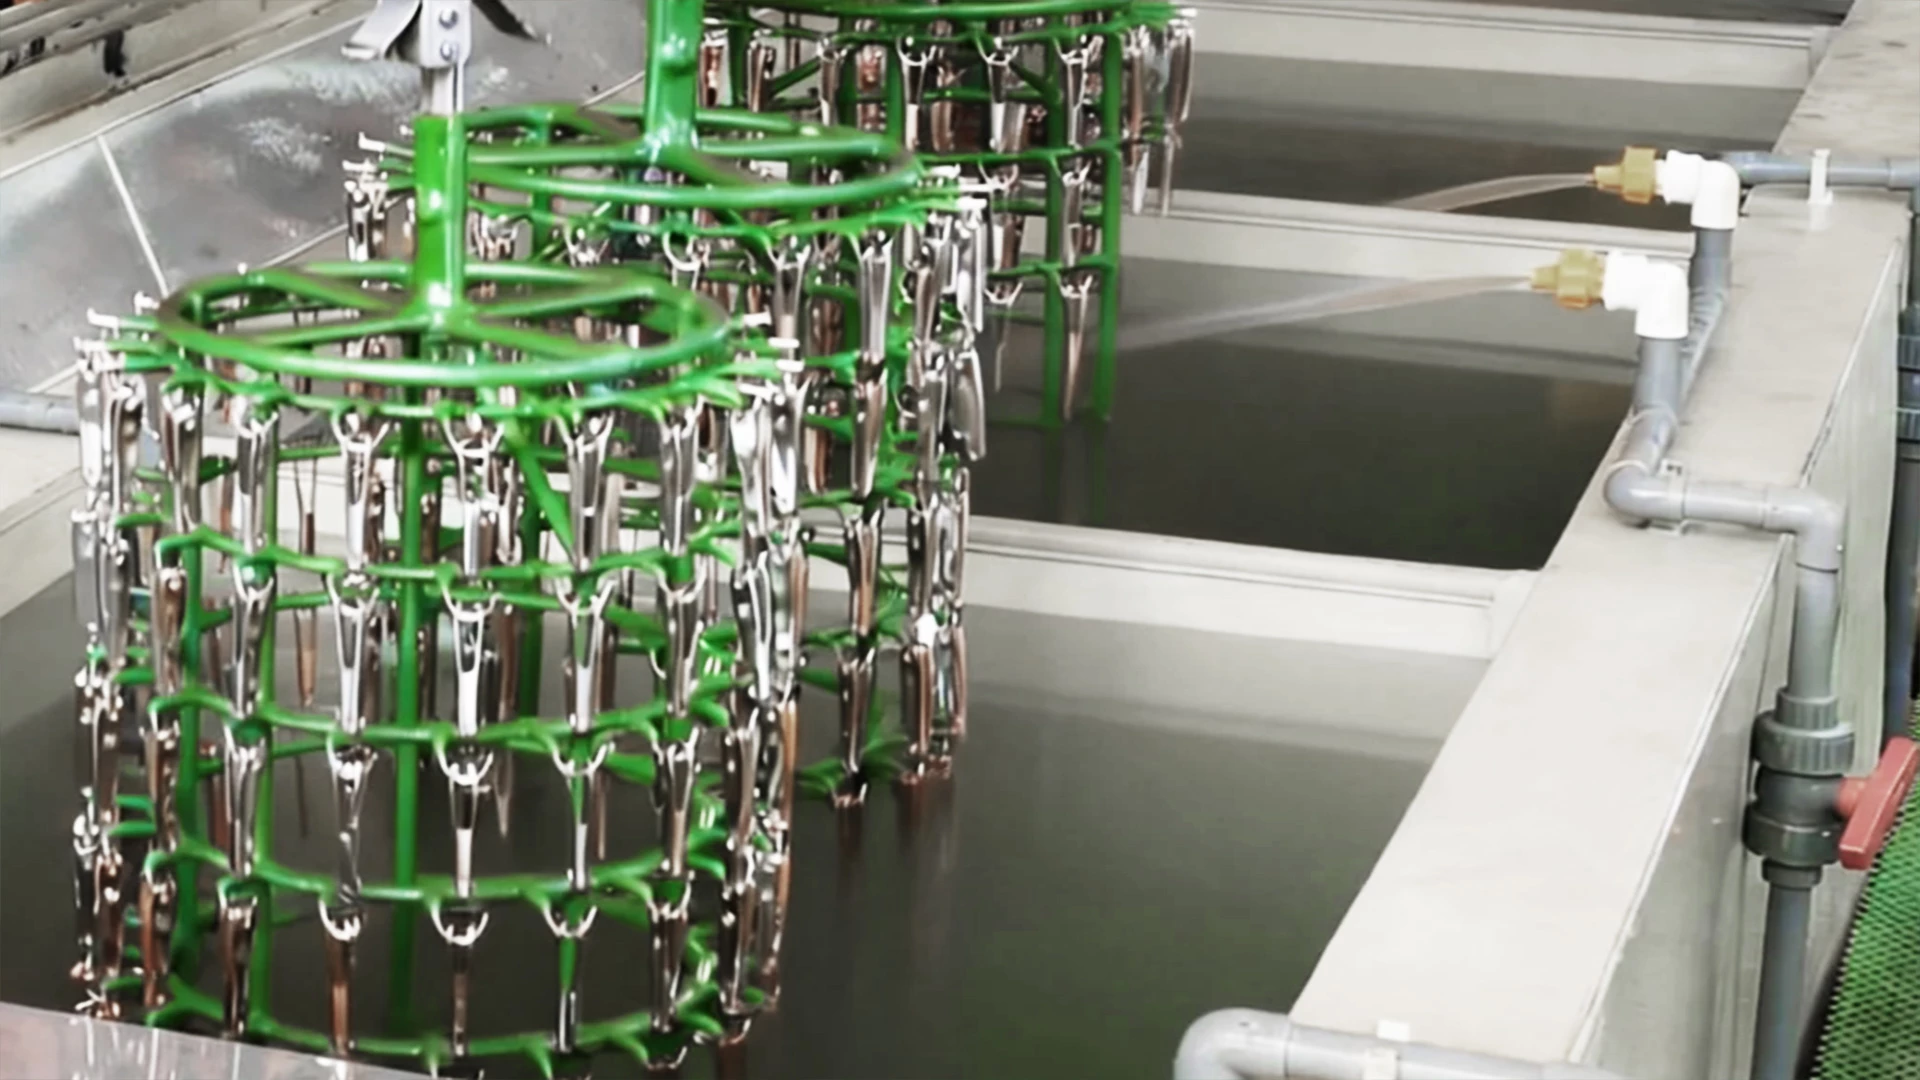
9. Three times Cleaning Tank
Remove residual liquid on the workpiece surface.
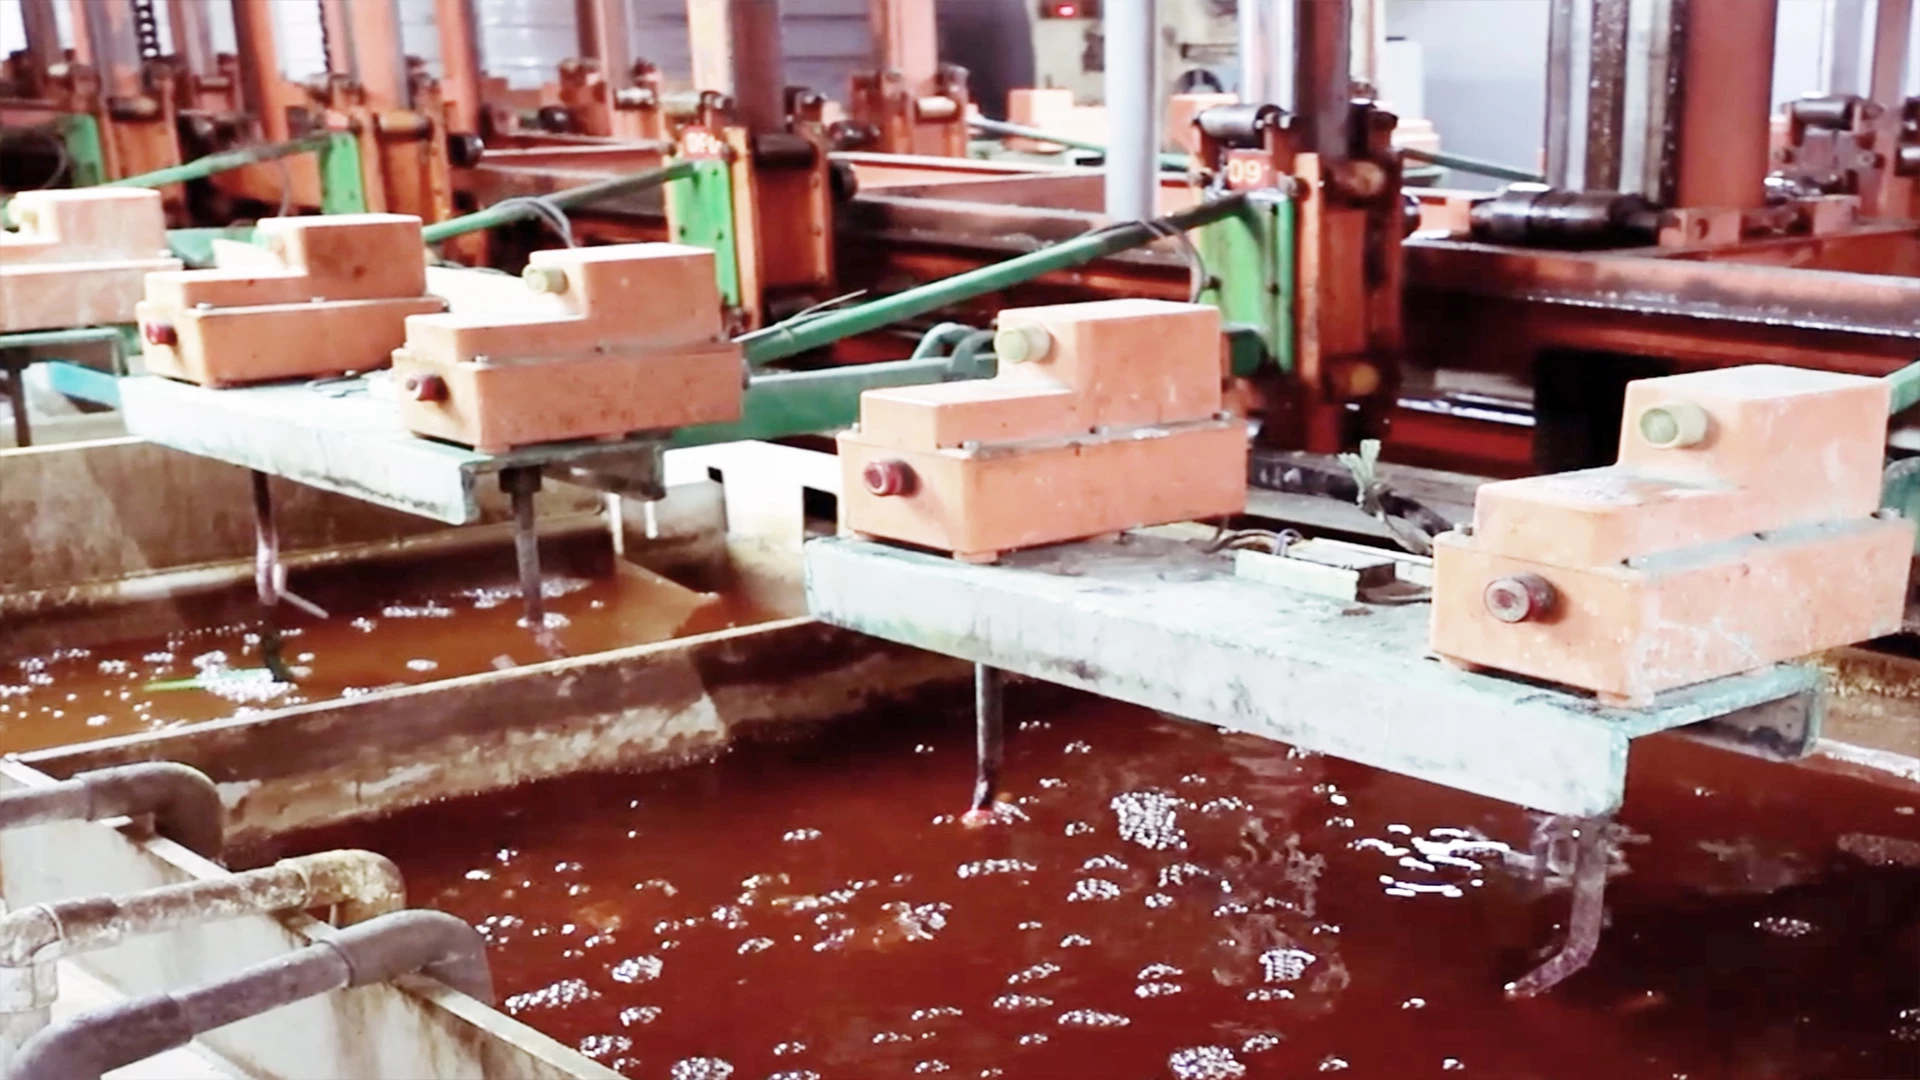
10. Two sets Deciduate Tank
Remove the matte film on the zinc alloy to make the zinc alloy turn white.
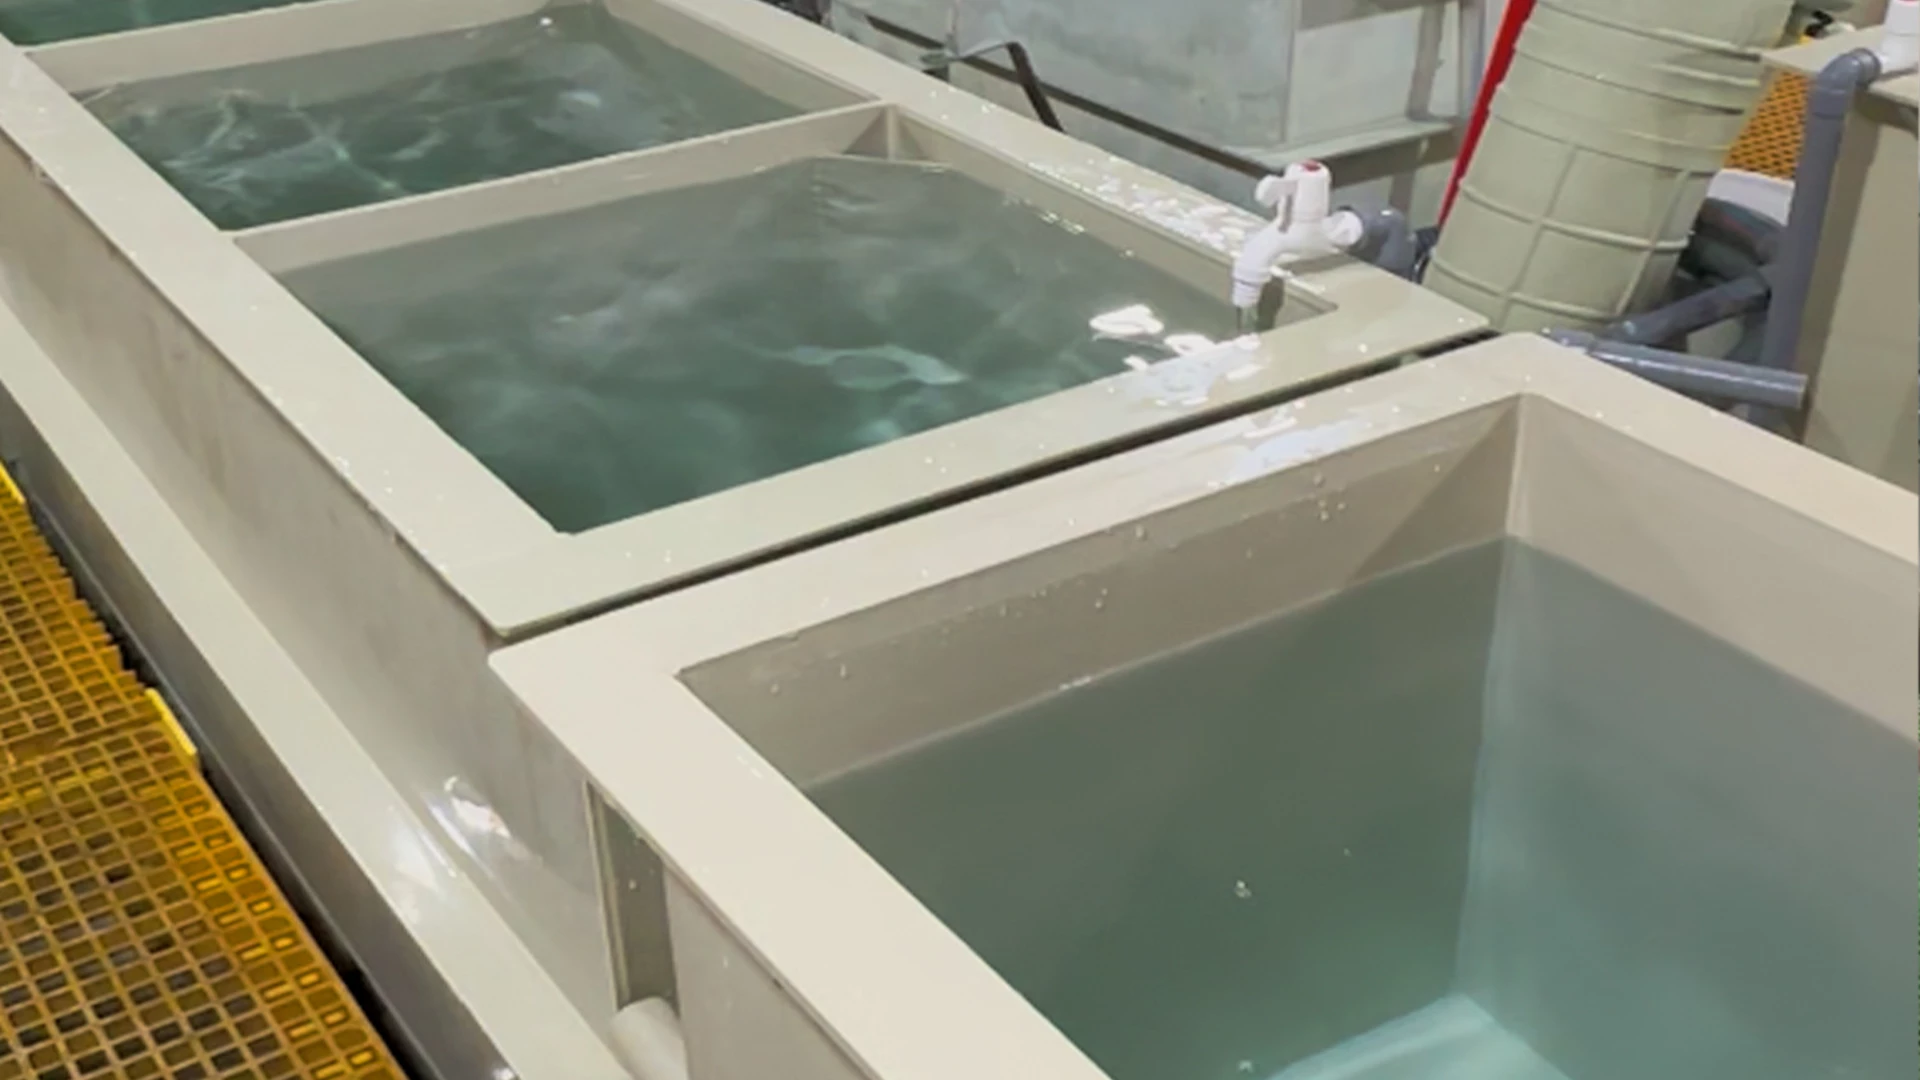
11. Three times Cleaning Tank
Remove residual liquid on the workpiece surface.
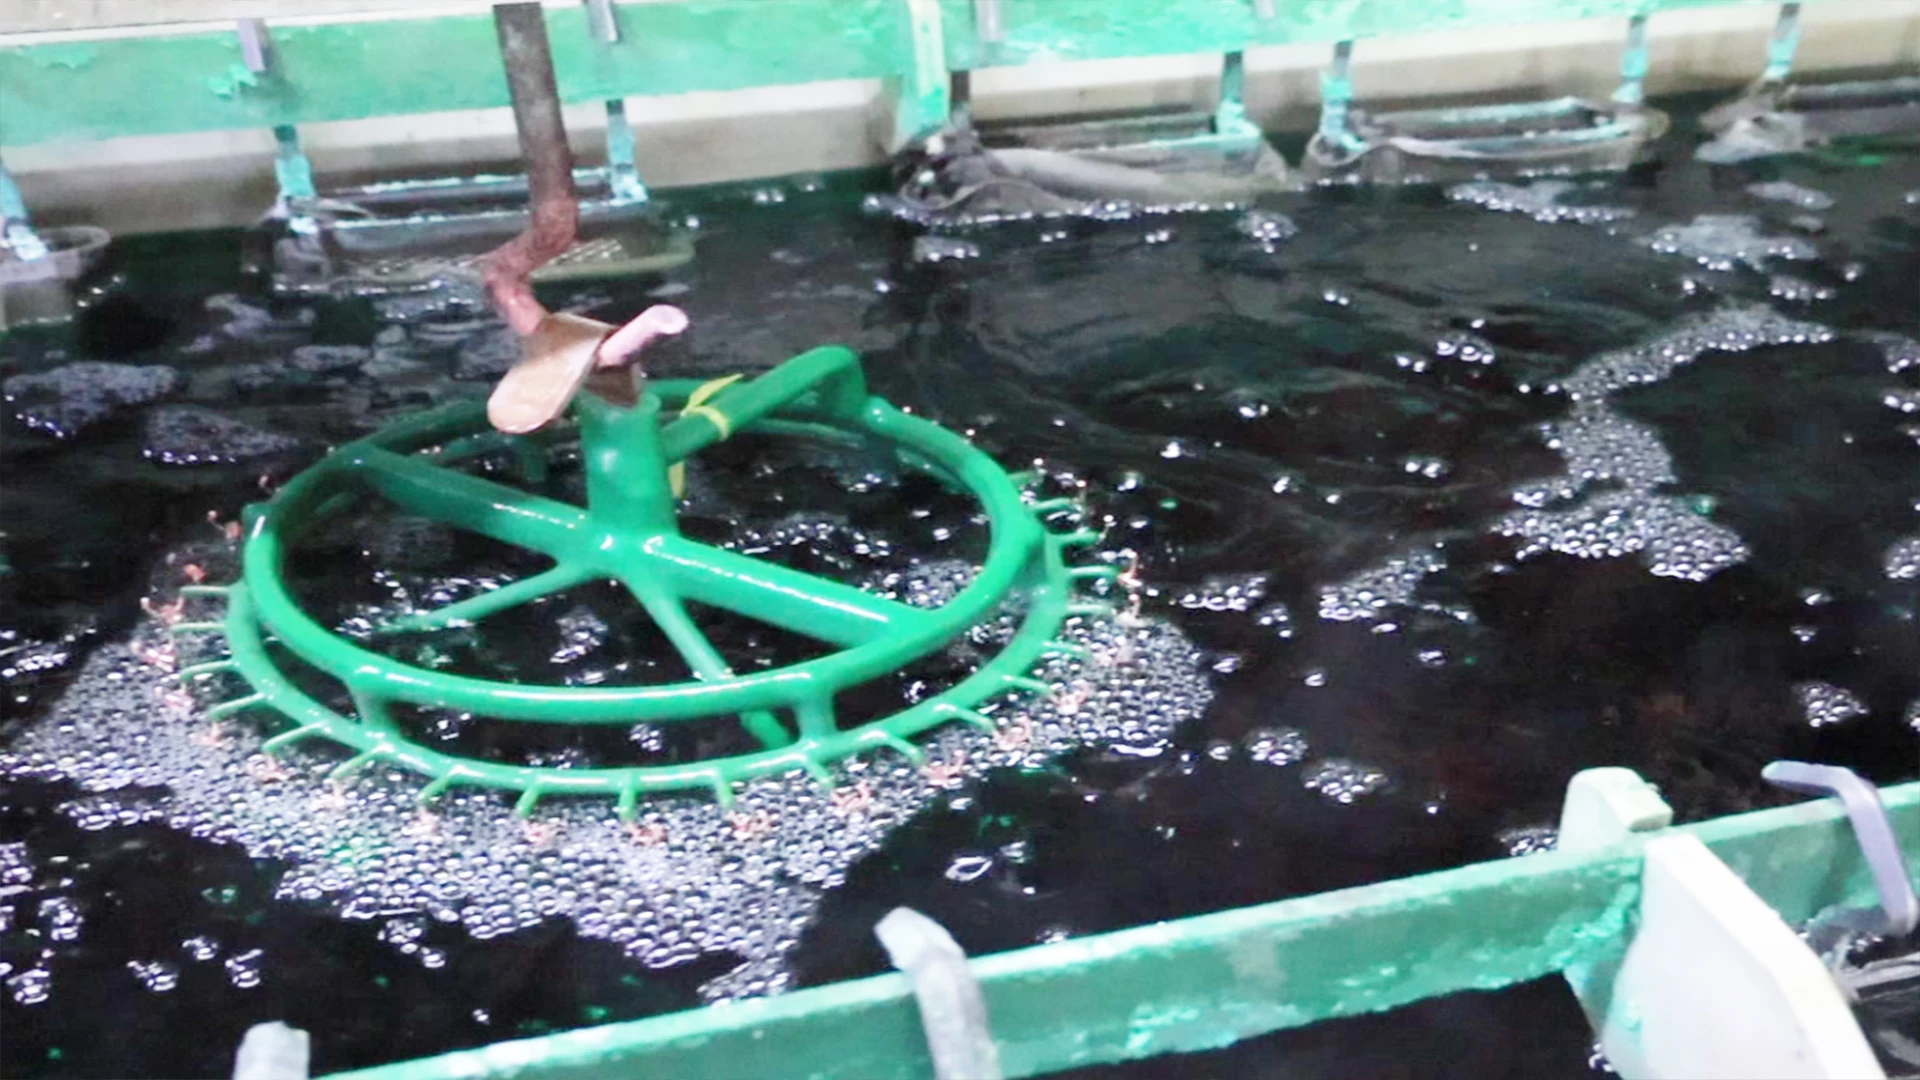
12. Activation Tank
Activation with 15% dilute sulfuric acid (Ratio: 85L water + 15L sulfuric acid = 100L total volume).
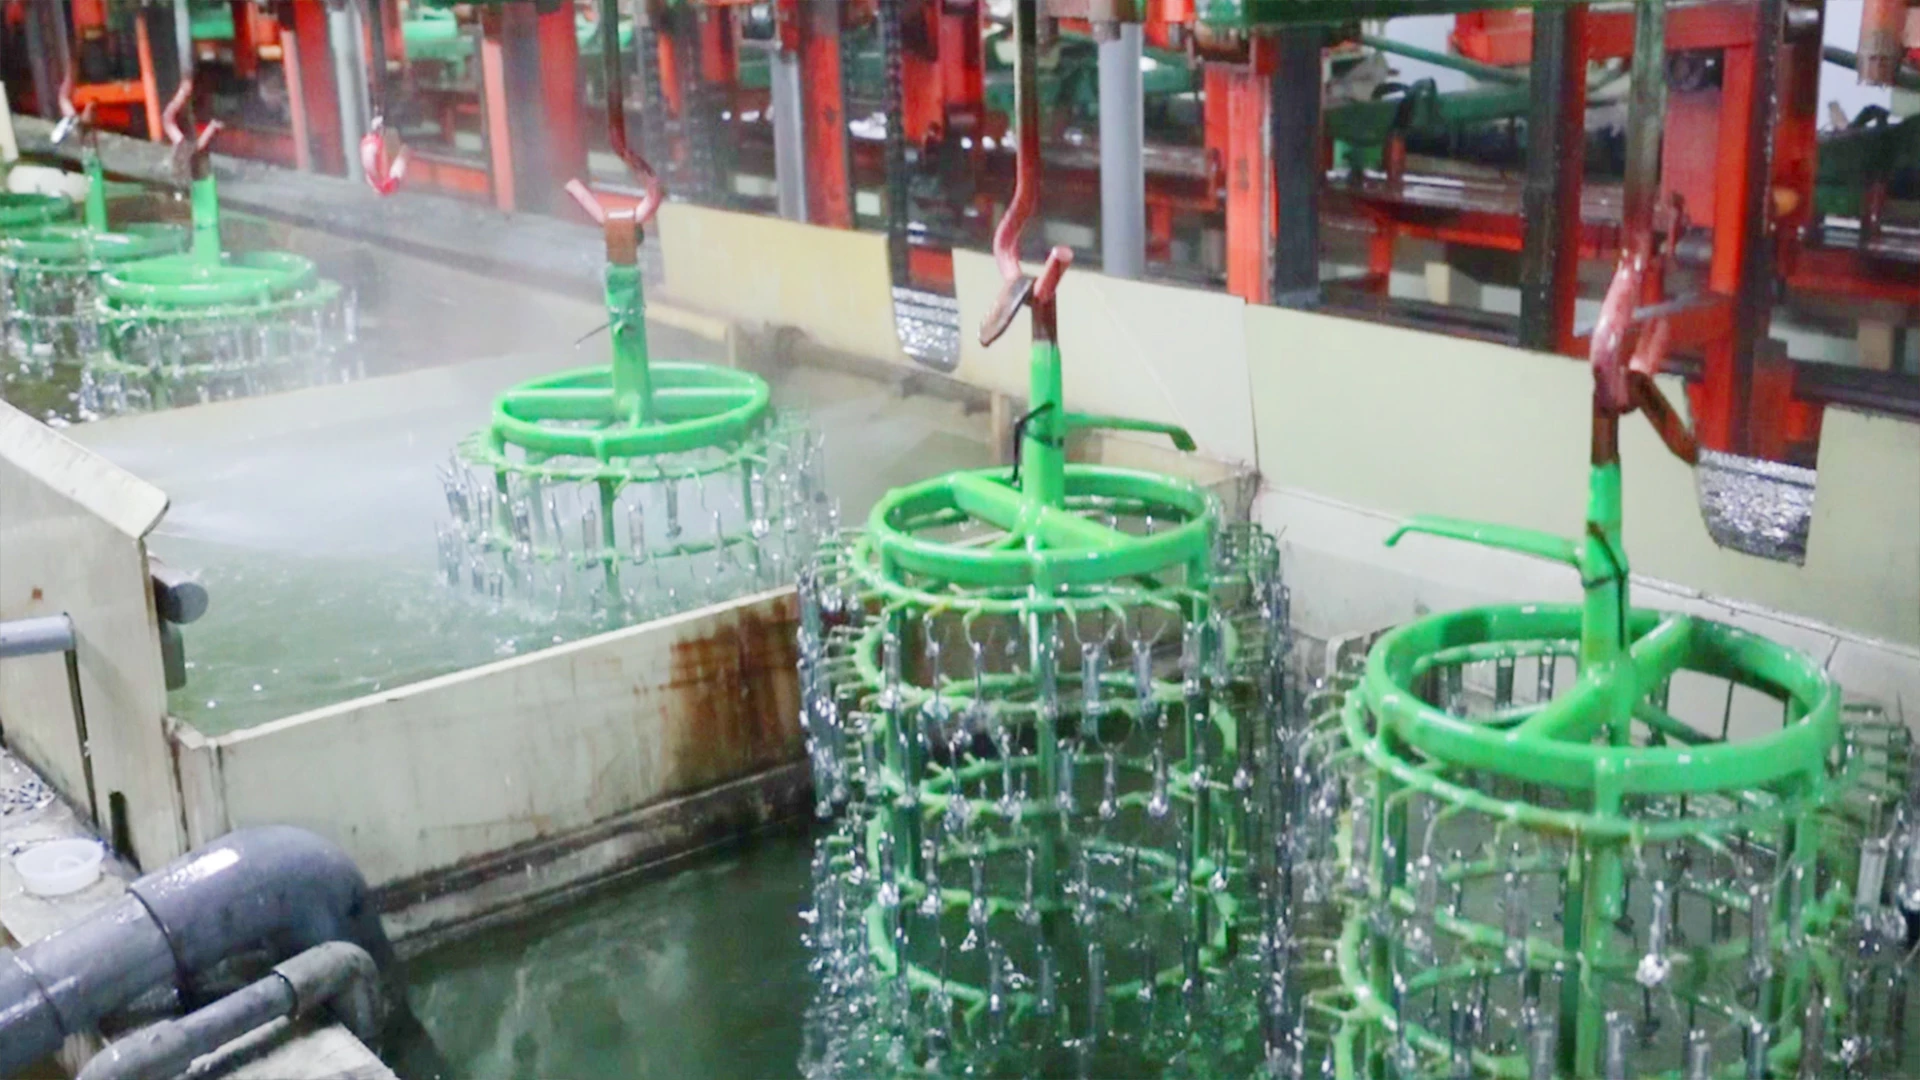
13. 2 times Cleaning Tank
Remove residual liquid on the workpiece surface.
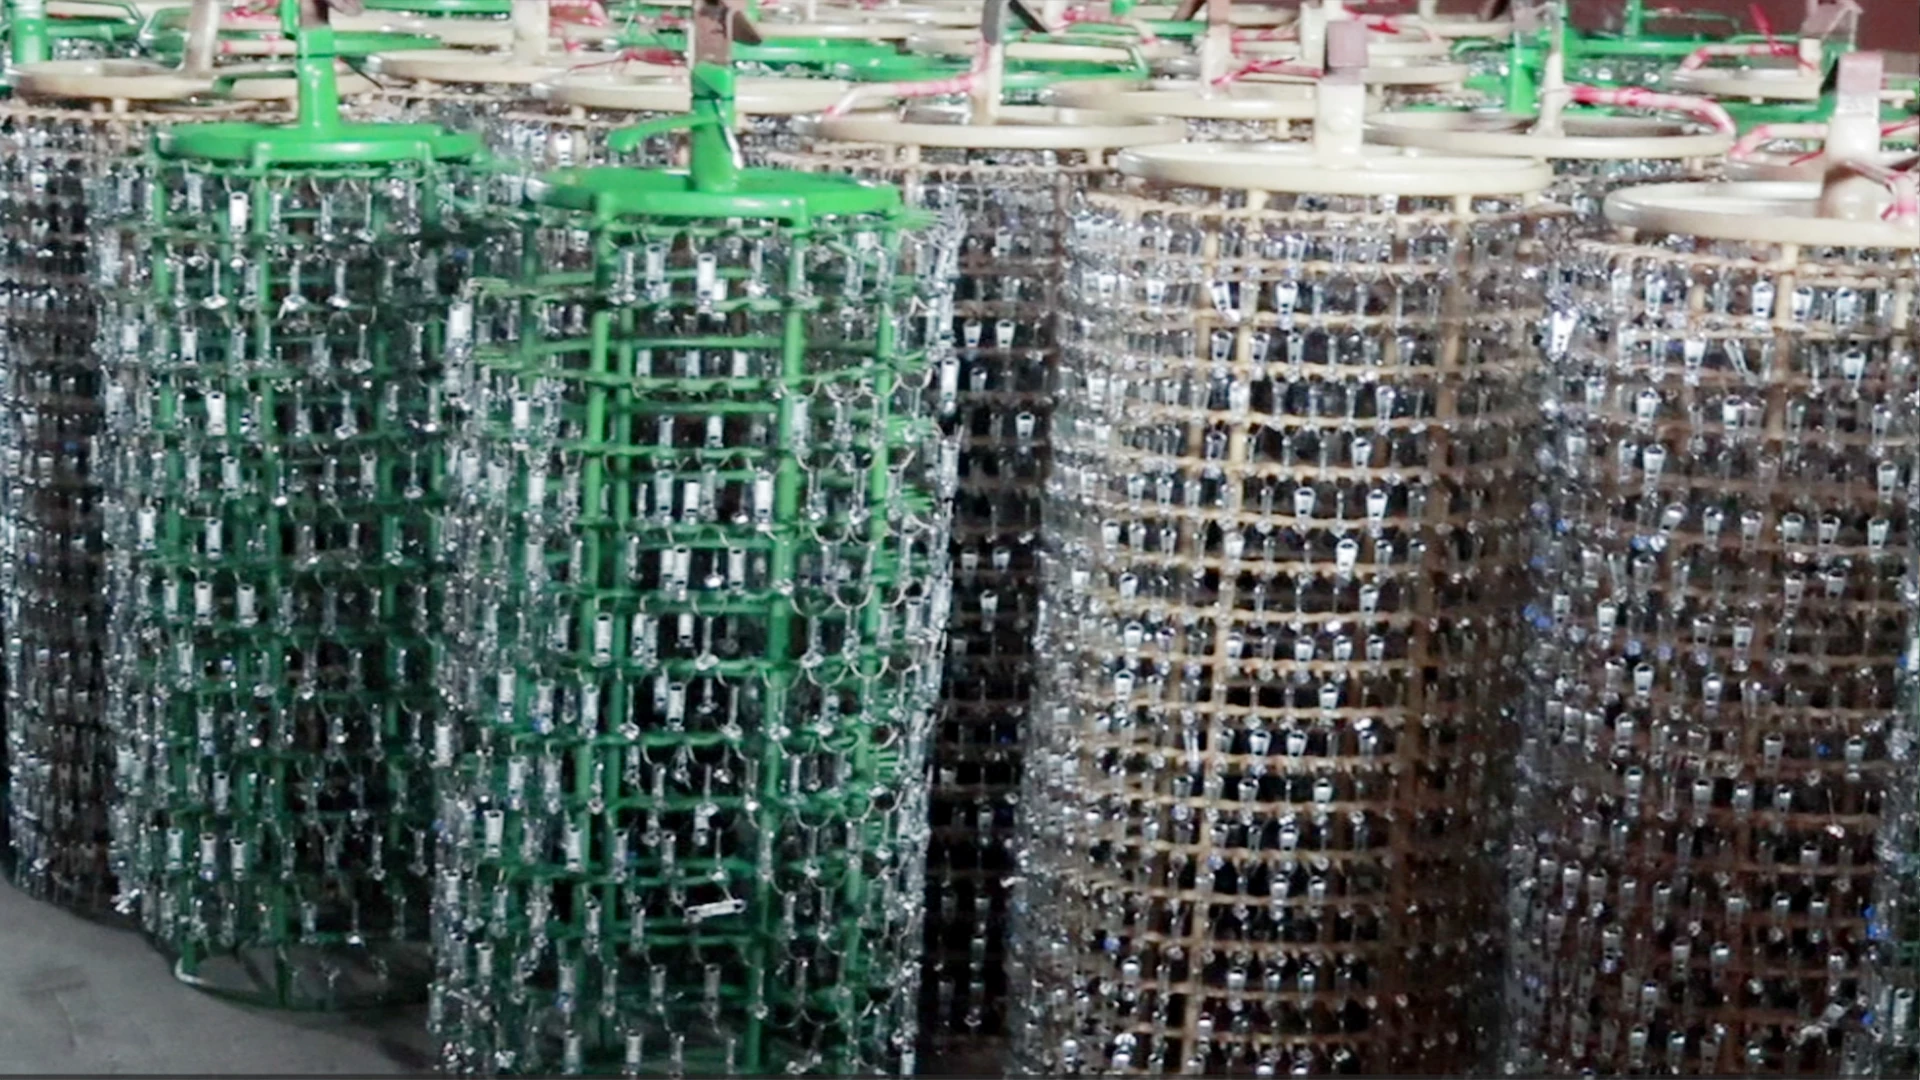
14. Unhanging
Get a Free Quote Today
Send us your samples or drawings — our engineers reply within 24 hours with pricing and technical advice.
Contact UsPretreatment for rack plating — Data Zinc Alloy Finishing Managers Need
The complete pre-treatment department combines polishing, dewaxing, degreasing, acid activation and phosphating so every zinc alloy part enters plating or painting with a chemically clean, activated surface.
Quality Inspection & Control
| Check item | Method | Acceptance standard |
|---|---|---|
| Water-break test | Spray + visual | Continuous film ≥ 30 s on 100% sampled racks |
| Surface roughness | Ra tester | Ra ≤ 0.8 μm before plating; ≤ 0.4 μm bright |
| Activation quality | Copper flash test | Uniform flash, no skip plating |
| Phosphate coating weight | Weigh-difference | 1.5-3.0 g/m² when phosphating applied |
| Cross-contamination | Bath titration logs | All baths within recipe control limits |
| Batch traceability | Work order scan | 100% batch barcode traceable to QC records |
Workshop Layout & Floor Area
| Zone | Area |
|---|---|
| Polishing section | 120 m² |
| Dewaxing & degreasing line | 100 m² |
| Activation & phosphating line | 100 m² |
| Rinse / DI / water treatment | 60 m² |
| QA lab & chemical store | 40 m² |
| Utility & lockers | 30 m² |
| Total department | 450 m² |
Manpower & Shift Plan
| Role | Headcount |
|---|---|
| Operators (all lines) | 10 |
| Chemical technicians | 2 |
| QC inspectors | 2 |
| Supervisor | 1 |
| Maintenance | 1 |
| Total (2 shifts × 10 h) | 16 |
Power & Utility Demand
| Equipment | Demand |
|---|---|
| Polishing equipment | 45 kW |
| Dewax / degrease heating | 38 kW |
| Phosphating heating + pumps | 28 kW |
| Ultrasonic + rinse pumps | 14 kW |
| Air compressor + exhaust | 19 kW |
| Lighting & auxiliary | 6 kW |
| Installed total | 150 kW |
| Typical running load | ≈ 118 kW |
Production Flow Chart
Daily Capacity — 10-Hour Operating Day
| Parameter | Value |
|---|---|
| Line cycle | 40-70 min |
| Simultaneous batches | 6-8 in process |
| Batches per 10 h day | 16-22 |
| Daily output | 1,000,000-2,000,000 pcs |
| Monthly output (26 days) | 26-52 million pcs |
Output Value Estimate
| Parameter | Value |
|---|---|
| Processing fee per piece | USD 0.003-0.008 |
| Daily output value (10 h) | USD 3,000-7,000 |
| Monthly output value | USD 78,000-180,000 |
| Annual output value | USD 940,000-2,160,000 |
Related Products — Complete Pretreatment for rack plating Solution
Machines, chemicals and consumables selected from the real QLQ product range for this process. Every product page is live and ready to quote.
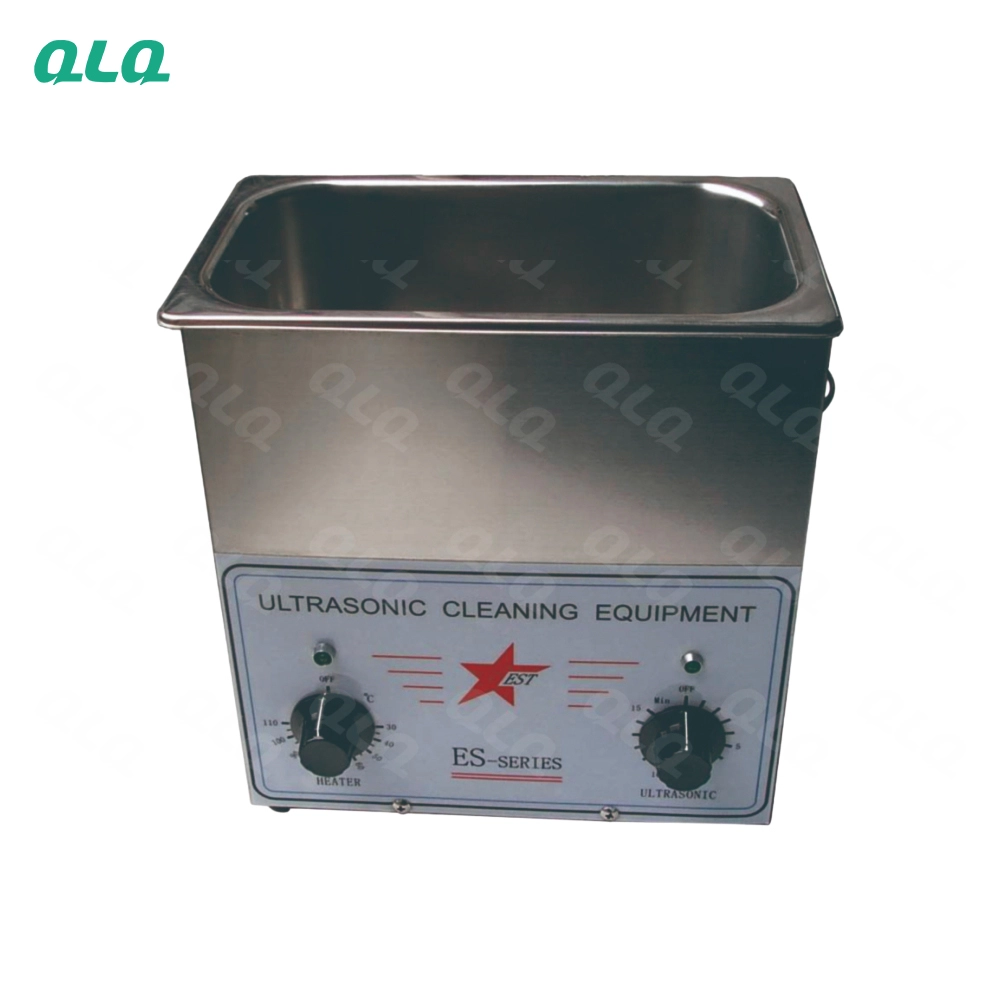
QLQ-UCM Ultrasonic cleaning machine
Machine & Equipment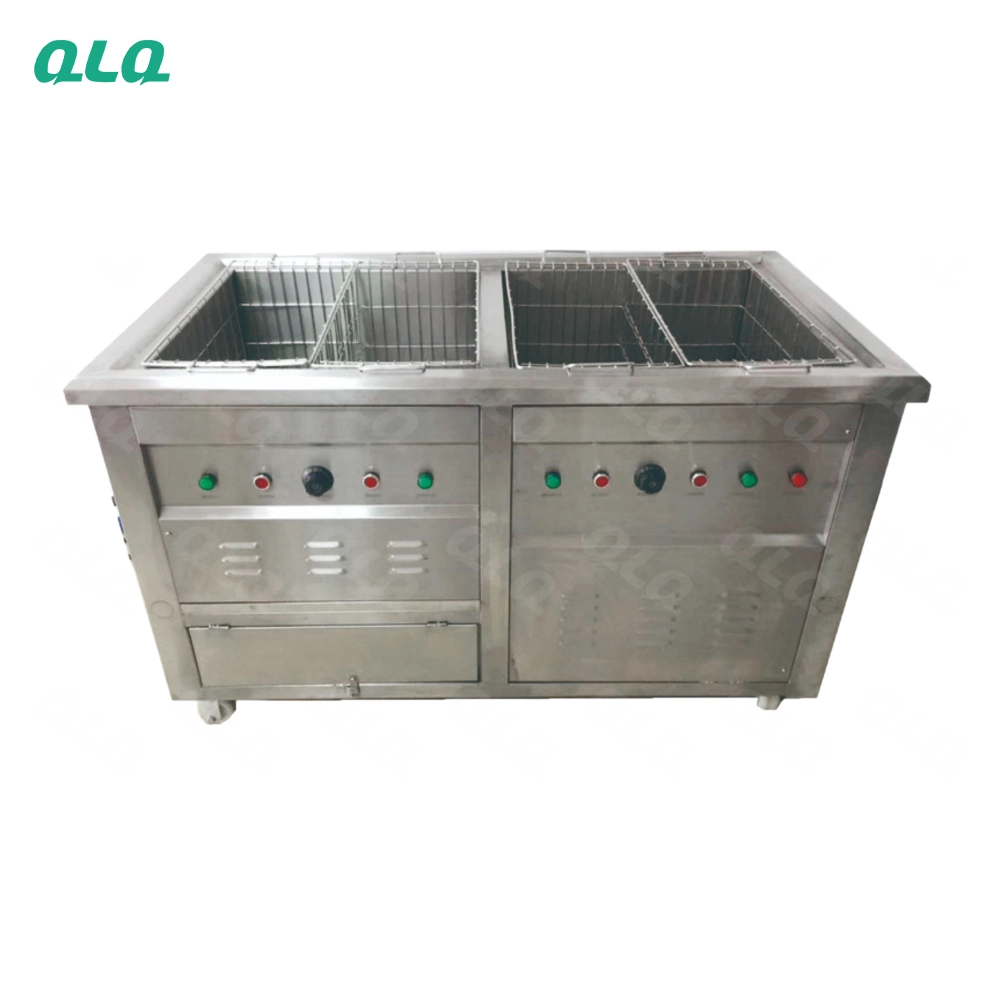
QLQ-TM Trichloroethylene machine(for removing wax)
Machine & Equipment
Automatic washing tank is suitable for rack plating, electrophoresis, and pretreatment.
Machine & Equipment
Oil Cleaning Degreasing Agent
Chemical & Coating
Oil Cleaning/Degreasing Powder
Chemical & Coating
Phosphating Agent
Chemical & Coating
QLQ-CRF Corrosion-resistant Filter
Machine & Equipment
superfilter
Machine & EquipmentRack line pretreatment: sequence and timing
| Stage | Time | Failure mode if short |
|---|---|---|
| Degrease | 3-8 min at 50-60 C | Patchy plate, water break |
| Electroclean | 2-5 min | Residue in blind holes |
| Pickle | 1-5 min | Smut under the deposit |
| Activation | 10-60 s | Passivation during transfer |
| First rinse after plating | Immediate | Stains from dried salts |
FAQ
Why do rack parts fail in recesses but pass on flats?
Solution exchange. Add agitation or an auxiliary anode - chemistry is usually fine.
Should racks be stripped before pretreatment?
Yes, contact tips must be clean. Coating on tips causes the patchy deposit people blame on the bath.