
Professional Zinc Alloy Surface Finishing Solutions
Barrel Plating
Get a Free Quote Today
Send us your samples or drawings — our engineers reply within 24 hours with pricing and technical advice.
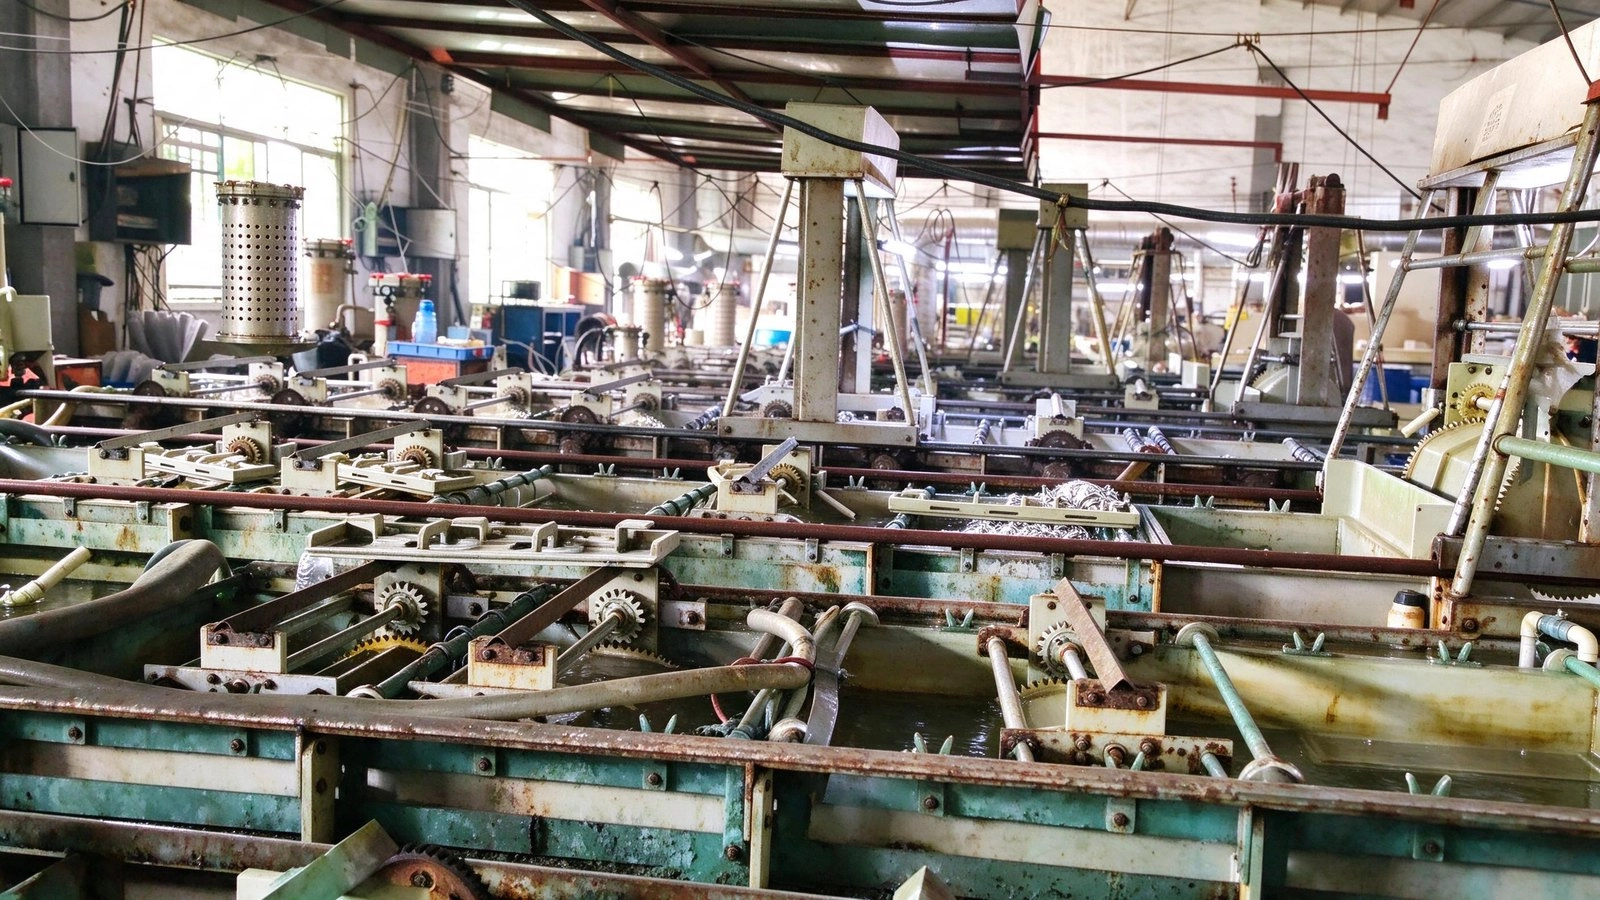
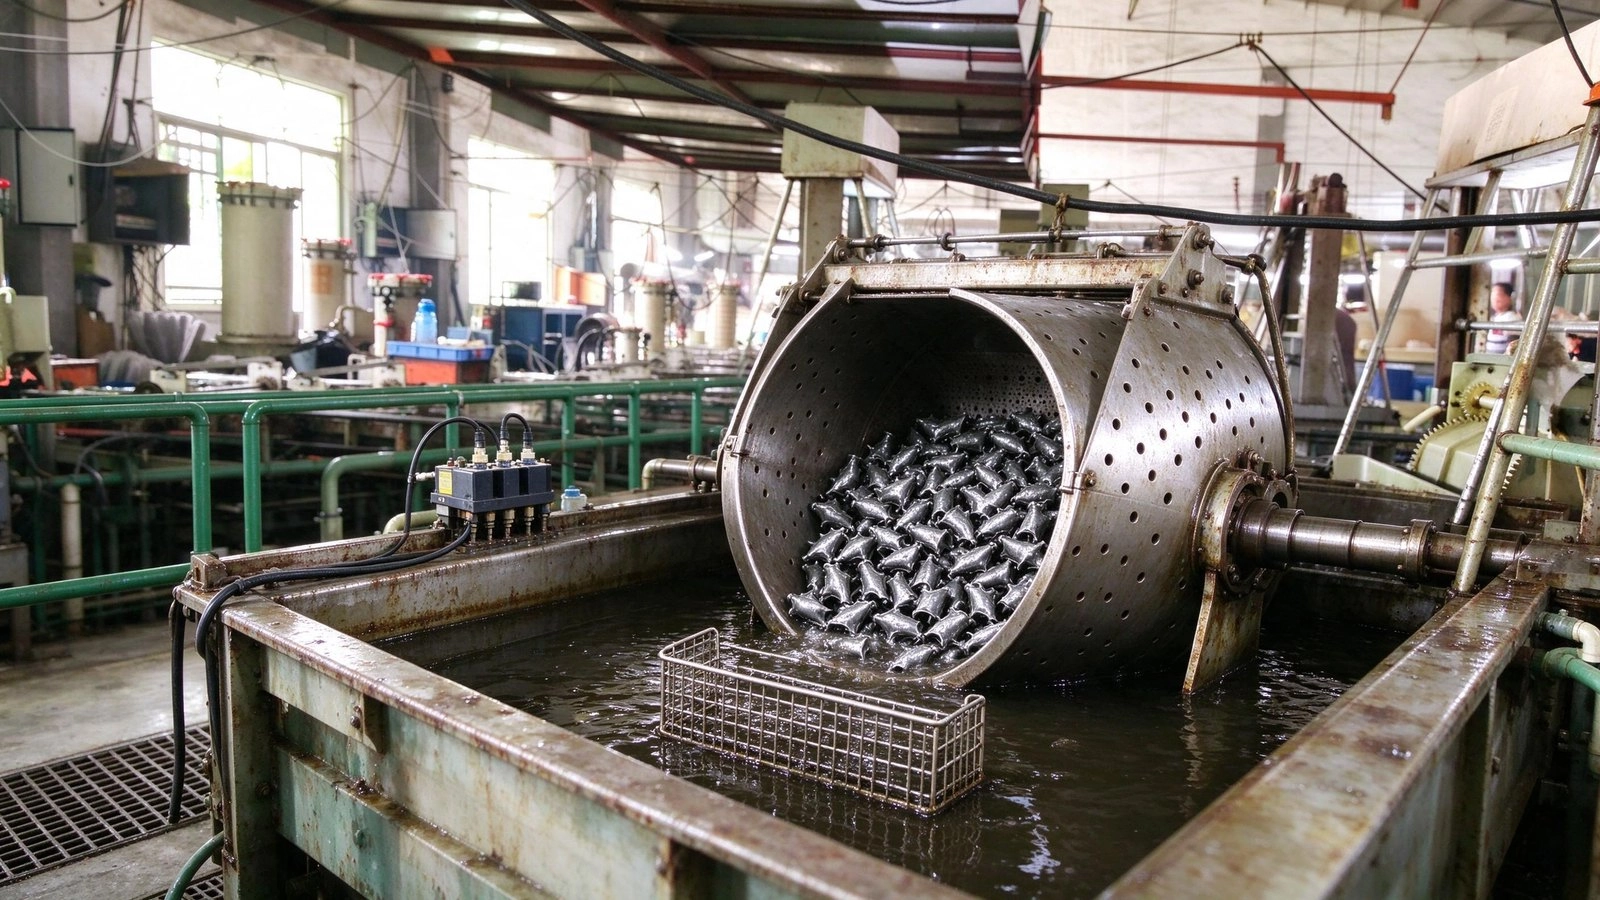
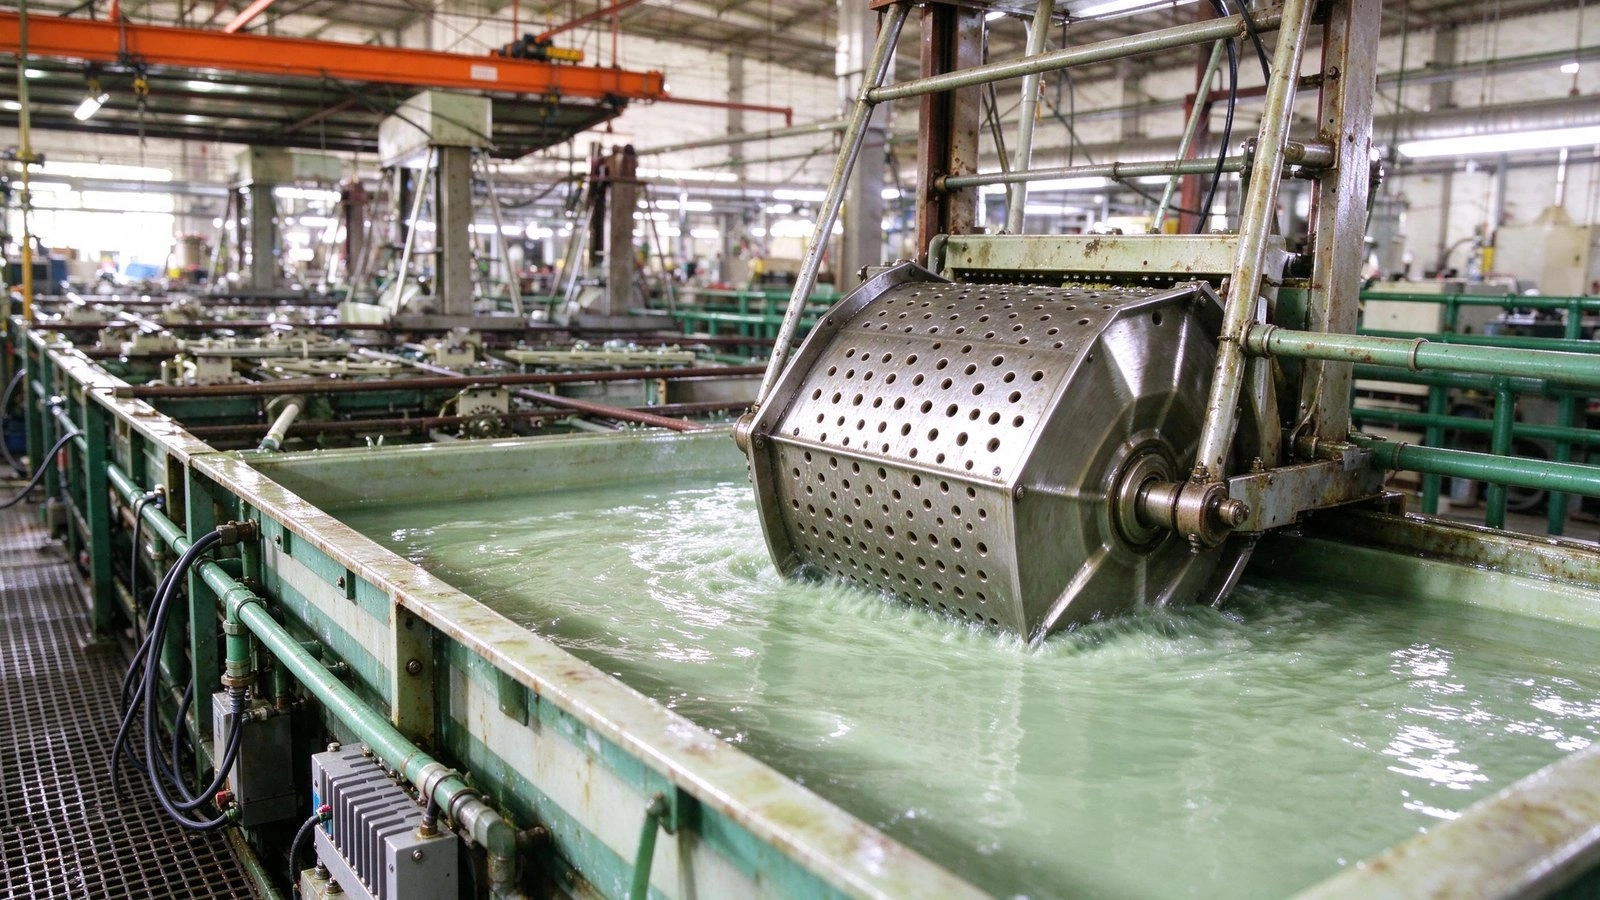
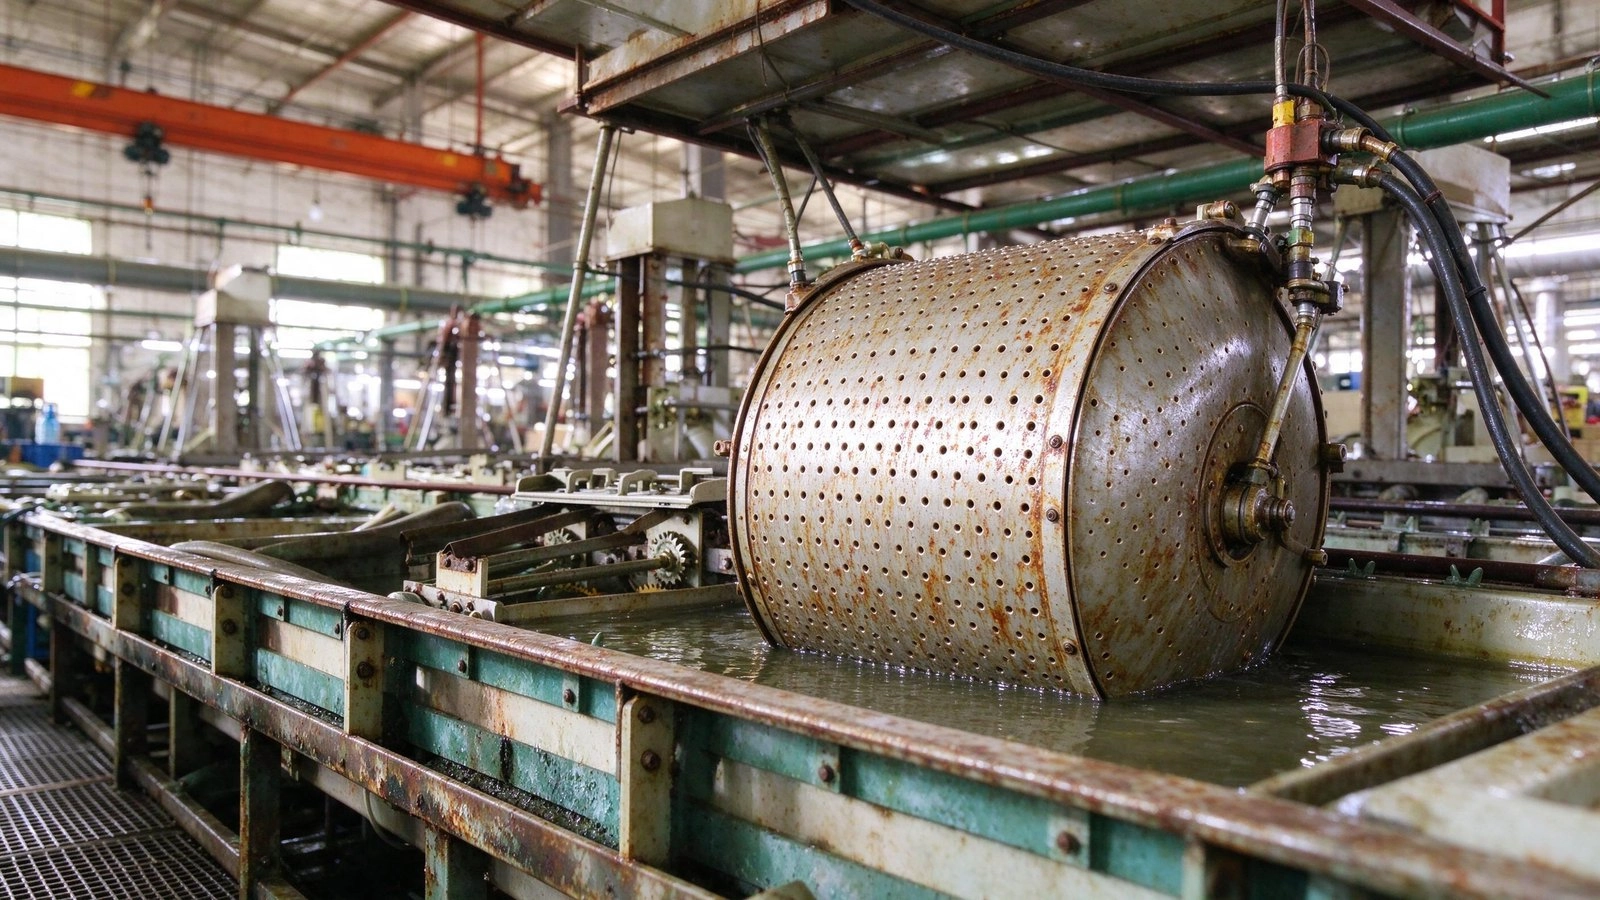
Workshop Planning Data
Barrel Plating — Data Zinc Alloy Finishing Managers Need
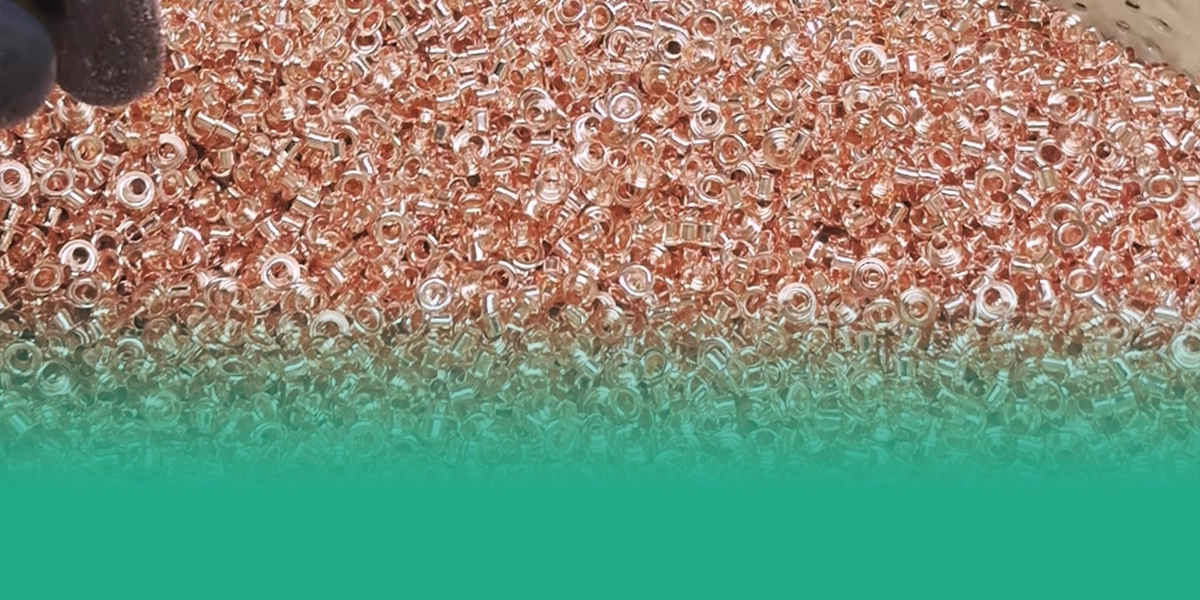
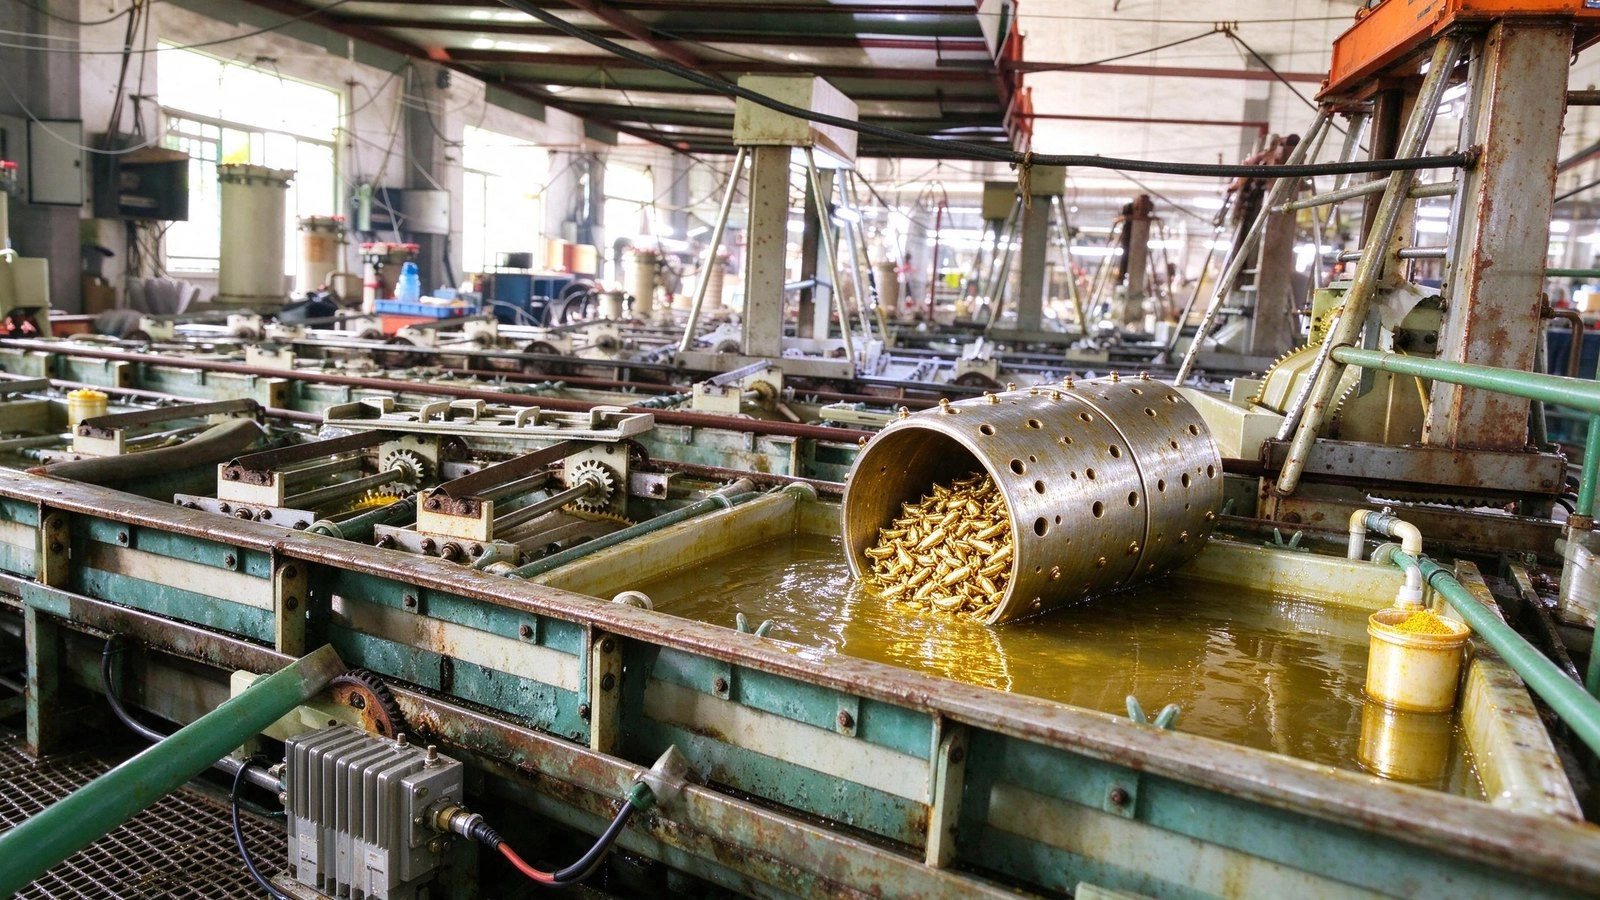
The automatic barrel plating line plates zinc alloy small parts with copper, nickel, tin and color finishes in batches of 50,000+ pieces, delivering uniform thickness and color at the lowest cost per piece.
650 m²Workshop Area
22 peopleTeam Size
260 kWInstalled Power
1.2-2.5M pcs/dayDaily Output (10 h)
Quality Inspection & Control
| Check item | Method | Acceptance standard |
|---|---|---|
| Coating thickness | X-ray fluorescence / coulometric | Per spec: Cu 3-8 μm, Ni 3-10 μm, Sn 3-6 μm |
| Adhesion | Bend / peel / thermal shock | No flaking at 150 °C × 30 min |
| Color match | Colorimeter ΔE / master | ΔE ≤ 1.5 vs approved master |
| Salt spray | NSS chamber | 12-72 h per finish spec |
| Pitting / roughness | 10× inspection | No pitting, nodules or burnt deposits |
| Thickness uniformity | 5 positions / batch | CV ≤ 10% across barrel load |
Workshop Layout & Floor Area
| Zone | Area |
|---|---|
| Automatic barrel line (12-16 tanks) | 260 m² |
| Chemical storage / dosing | 60 m² |
| Rectifier room | 40 m² |
| QA lab + X-ray | 50 m² |
| Dryer / centrifuge / sorting | 80 m² |
| Rinse & waste treatment | 110 m² |
| Utility & lockers | 50 m² |
| Total workshop | 650 m² |
Manpower & Shift Plan
| Role | Headcount |
|---|---|
| Line operators | 10 |
| Chemical technicians | 3 |
| QC inspectors (incl. X-ray) | 3 |
| Wastewater operator | 1 |
| Supervisor | 1 |
| Maintenance / electrician | 2 |
| Logistics & sorting | 2 |
| Total (2 shifts × 10 h) | 22 |
Power & Utility Demand
| Equipment | Demand |
|---|---|
| Rectifiers 12 V × 500-2000 A (4 sets) | 80 kW |
| Tank heating + cooling | 55 kW |
| Barrel drive motors (12-16) | 24 kW |
| Pumps / filters / dosing | 30 kW |
| Exhaust + scrubber | 22 kW |
| Dryer + centrifuge | 20 kW |
| Wastewater treatment | 18 kW |
| Lighting & auxiliary | 11 kW |
| Installed total | 260 kW |
| Typical running load | ≈ 205 kW |
Production Flow Chart
PretreatmentPolish, degrease, activate
Alkaline CopperStrike layer for adhesion
Acid Copper / Nickel / TinBuild thickness + brightness
Color FinishGold, gun, black, antique etc.
Rinse ChainRecovery → counter-flow → DI
Dry & SortCentrifuge, inspect, pack
Daily Capacity — 10-Hour Operating Day
| Parameter | Value |
|---|---|
| Batch cycle | 25-45 min |
| Load per barrel | 40-80 kg |
| Parts per batch | 50,000-100,000 |
| Batches per 10 h day | 14-20 |
| Daily output | 1,200,000-2,500,000 pcs |
| Monthly output (26 days) | 31-65 million pcs |
Output Value Estimate
| Parameter | Value |
|---|---|
| Plating fee per piece | USD 0.005-0.015 |
| Daily output value (10 h) | USD 7,000-18,000 |
| Monthly output value | USD 180,000-470,000 |
| Annual output value | USD 2,160,000-5,600,000 |
Related Products — Complete Barrel Plating Solution
Machines, chemicals and consumables selected from the real QLQ product range for this process. Every product page is live and ready to quote.
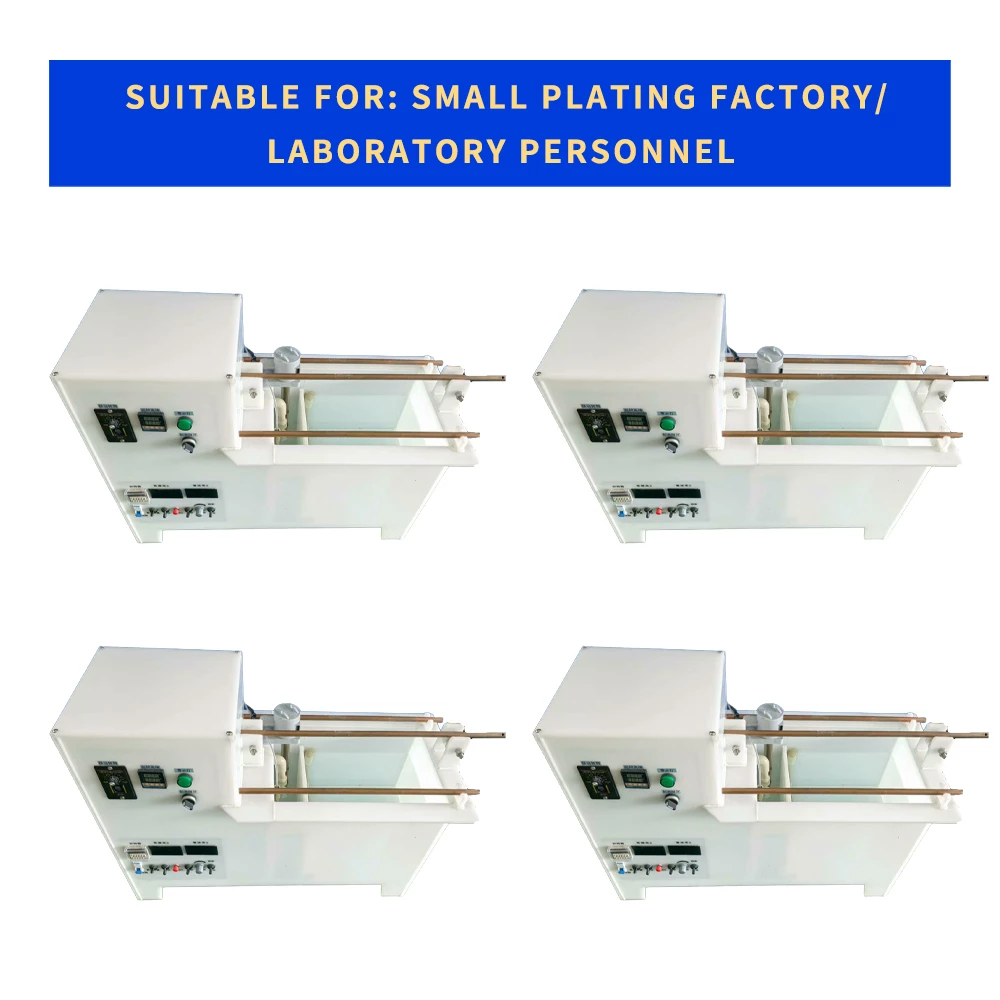
Small Roll plating and hanging plating machine
Machine & Equipment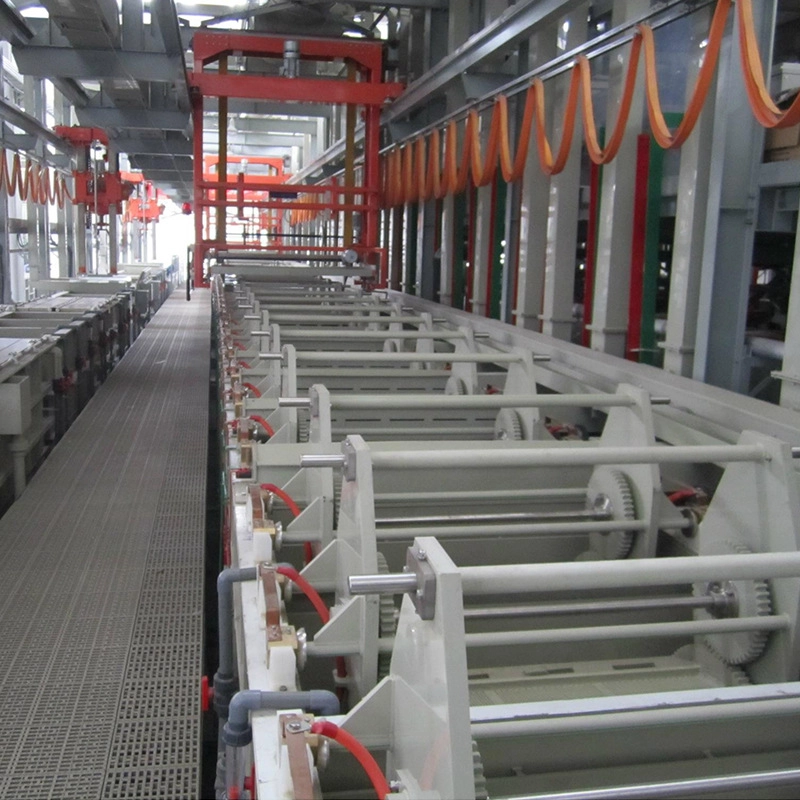
Barrel Plating Machine Nickel Zinc Plating Machine Gold Plated Electroplating Chemical Metal Electroplating Machinery
Machine & Equipment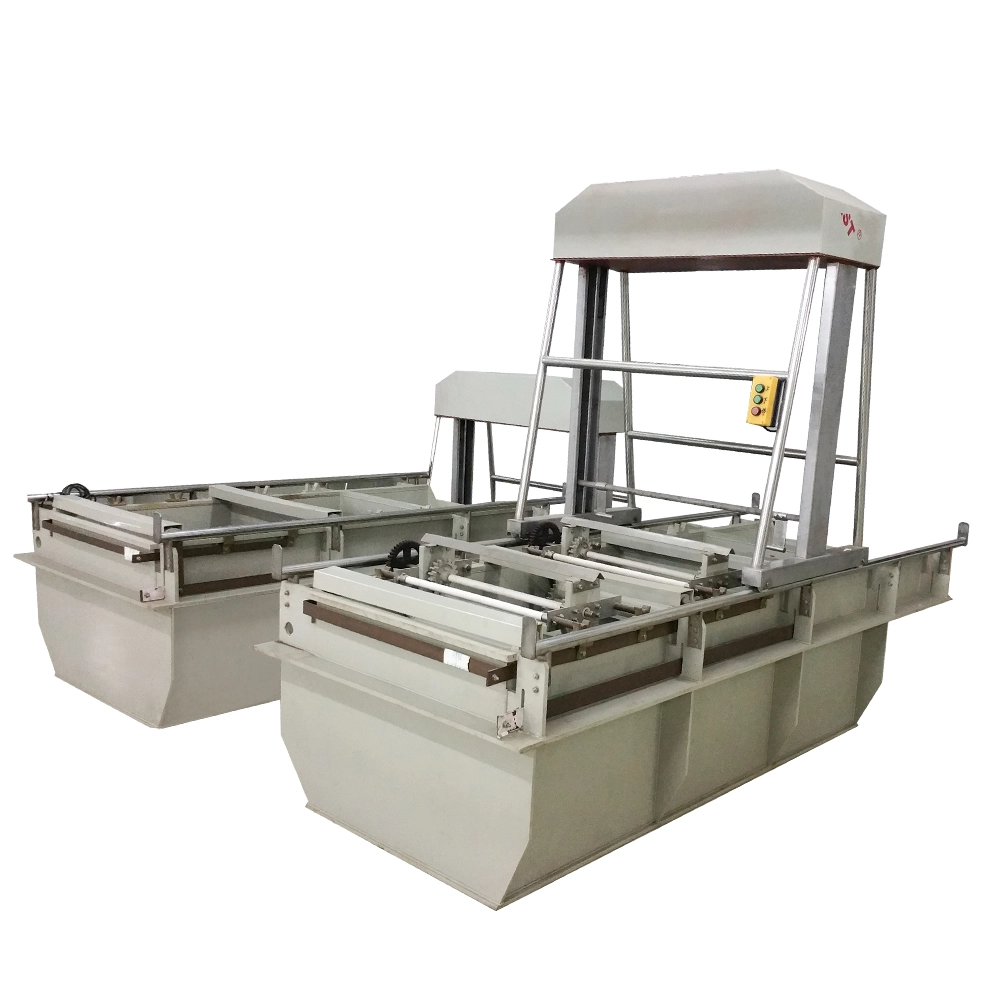
QLQ-BPM barrel plating machine(4 baskets)
Machine & Equipment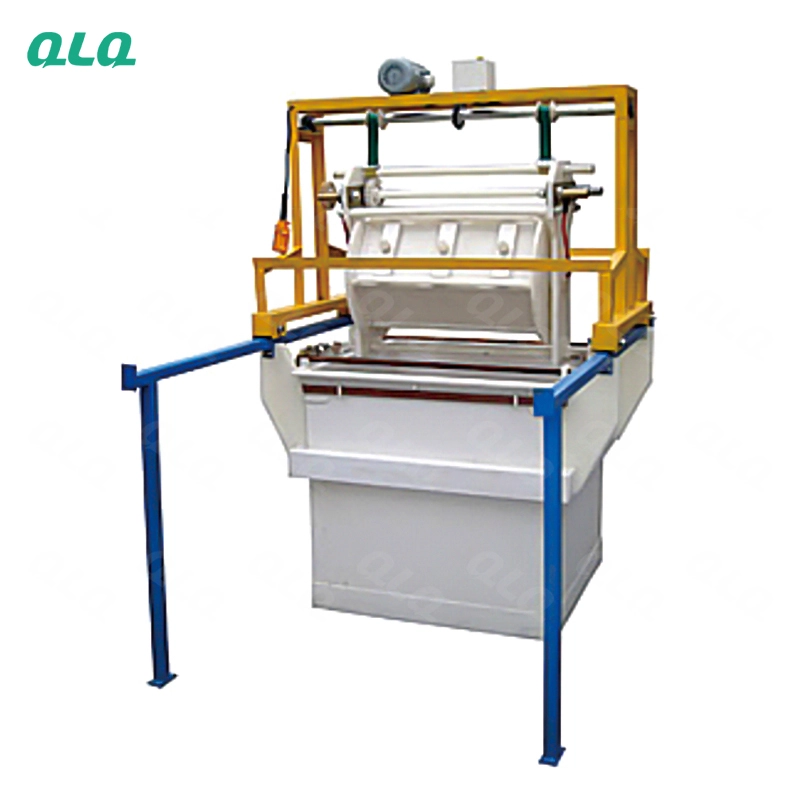
QLQ-BPM Barrel plating machine(single basket)
Machine & Equipment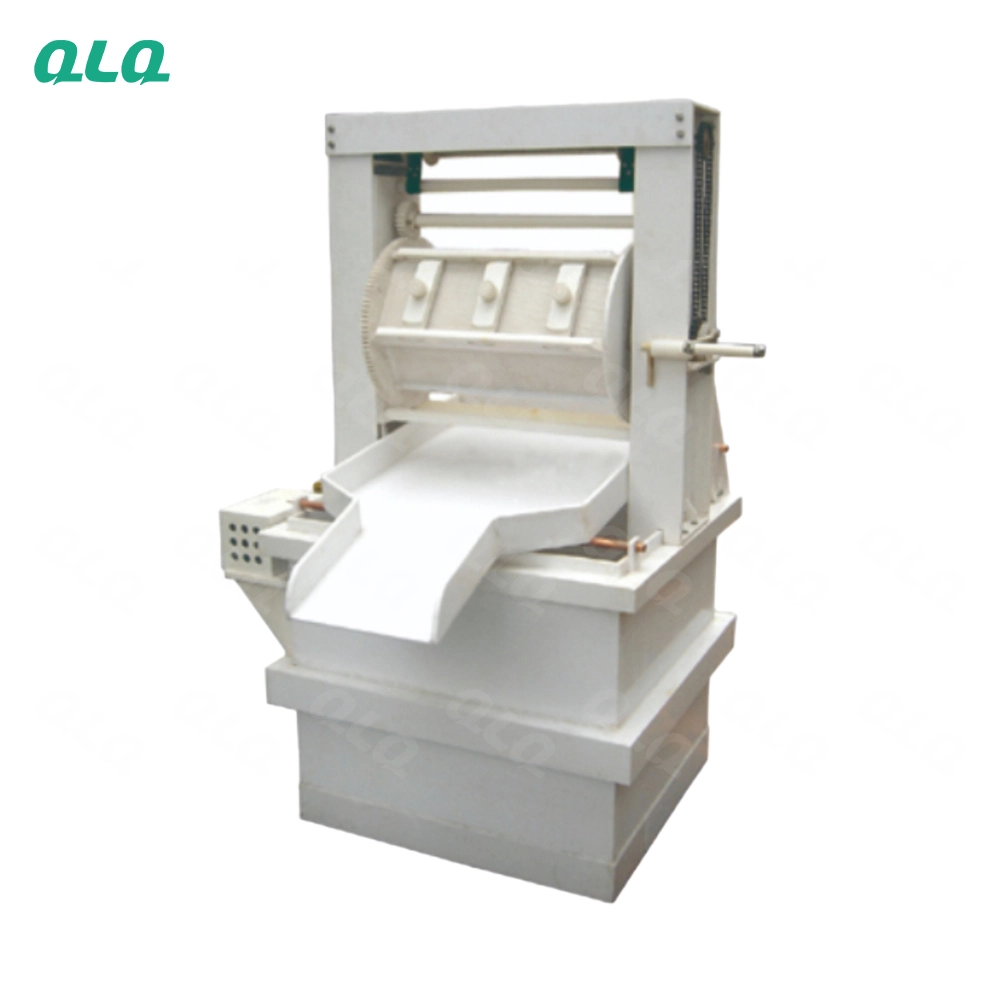
QLQ-BPM Small barrel plating mahcine
Equipment & Spare Part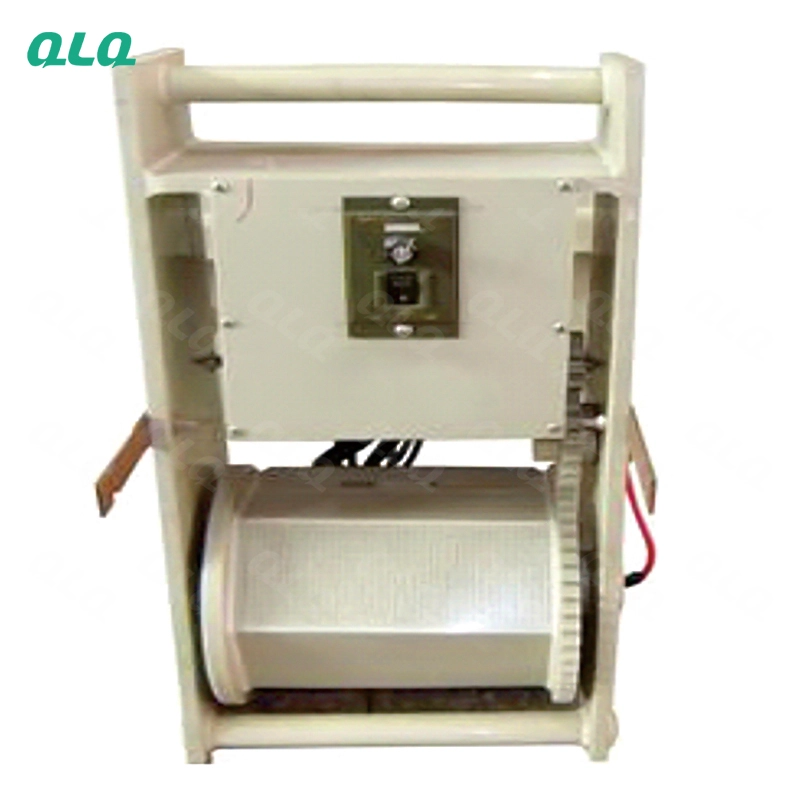
QLQ-BPM Barrel plating test machine
Machine & Equipment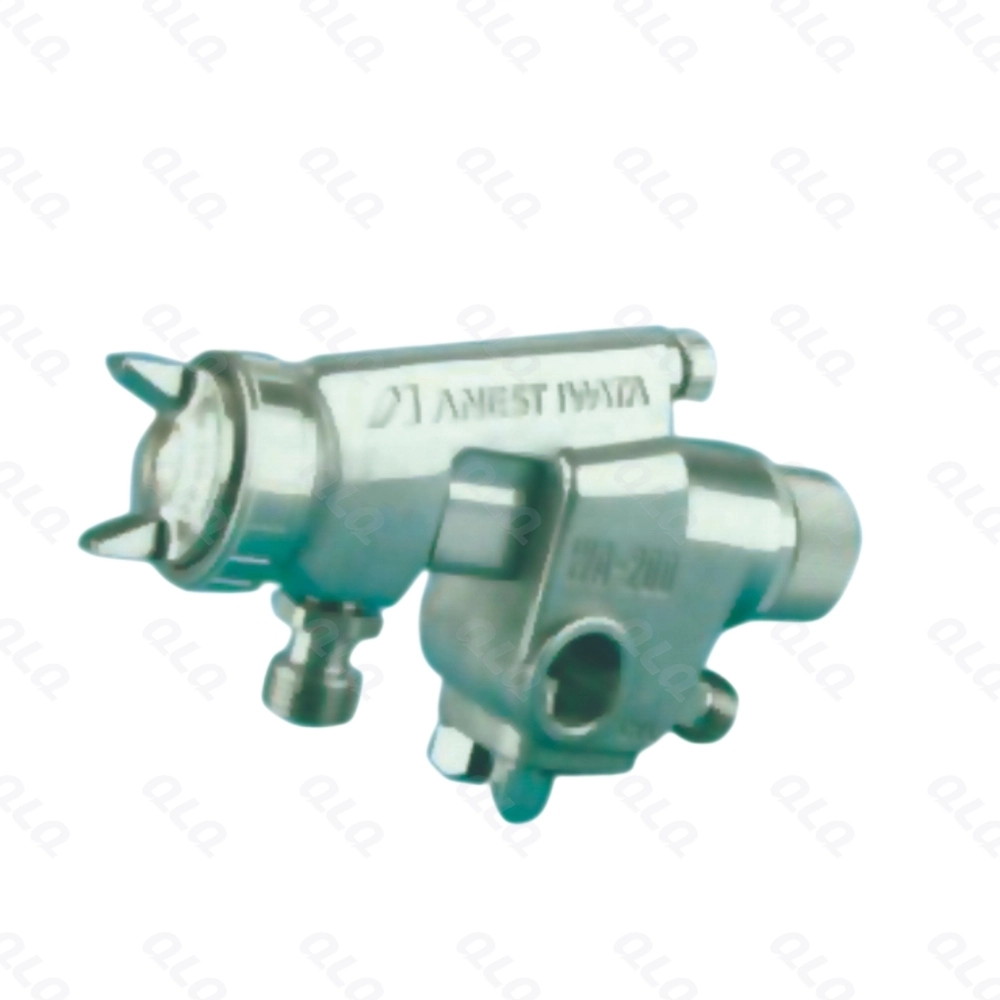
Machine Painting Gun
Machine & Equipment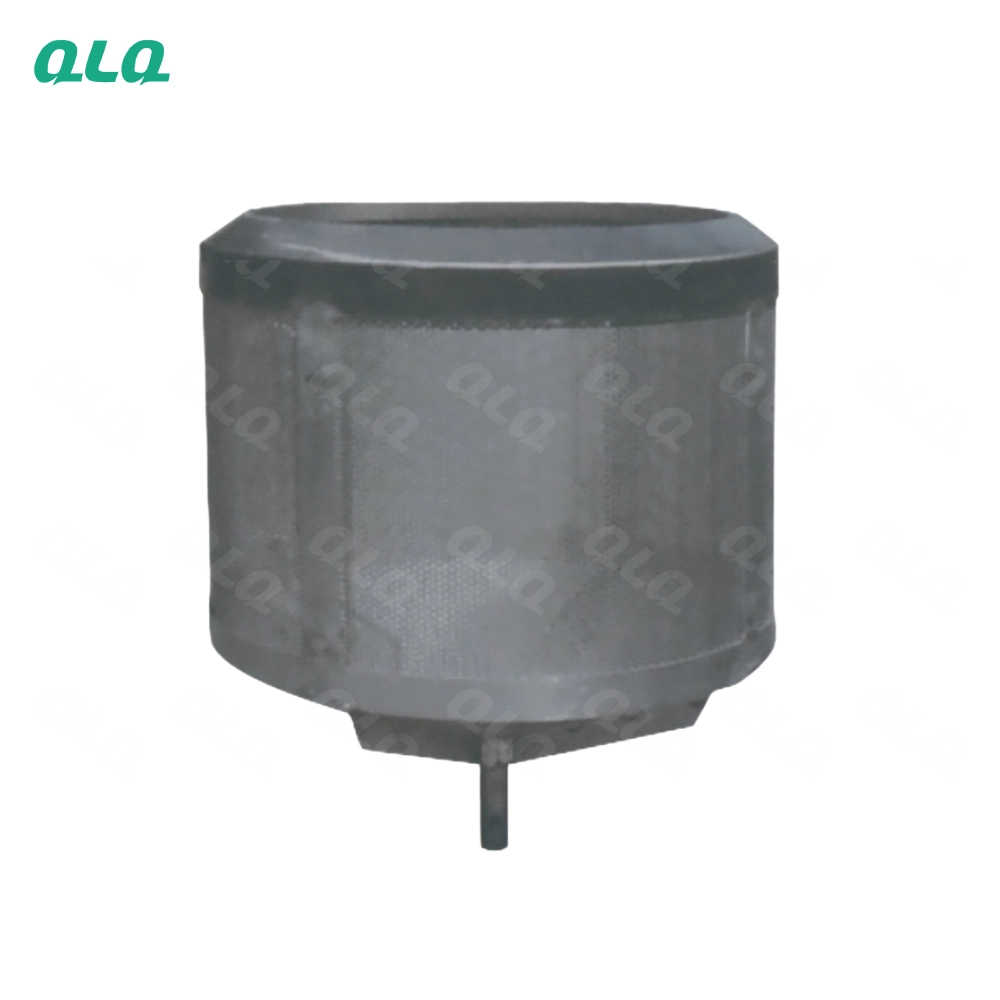
Stainles steel basket of painting machine
Machine & EquipmentView Full Product Range
Barrel parameters that matter most
| Parameter | Effect | Typical adjustment |
|---|---|---|
| Barrel load | Too full = poor contact and uneven plate | Fill 40-60% of barrel volume |
| Rotation speed | Too slow = marks, too fast = bruising | Start slow, raise after 5 minutes |
| Current per barrel | Set by total surface area, not by barrel | Calculate from part count and area |
| Solution flow | Needs to reach the part inside the load | Perforated barrel + pump circulation |
FAQ
Why do parts at the barrel ends plate thicker?
Current path. The contacts sit at the ends, so the load near them sees higher density - rotate and reverse cycle direction.
How do we plate very small parts without losing them?
Fine mesh barrels and a screened rinse. Also count weight in and out - losses are usually handling, not plating.