
Barrel Spray Painting — High-Volume Batch Coating for Small Hardware
Mass-production painting for zipper sliders, buttons and tiny hardware. Tumbling barrel + spray gun, controlled rotational speed and multi-pass thin coats.
The Barrel Painting Process
Tumble, spray, flash, repeat — the production rhythm for high-volume small parts
1Barrel Spray Machine Setup
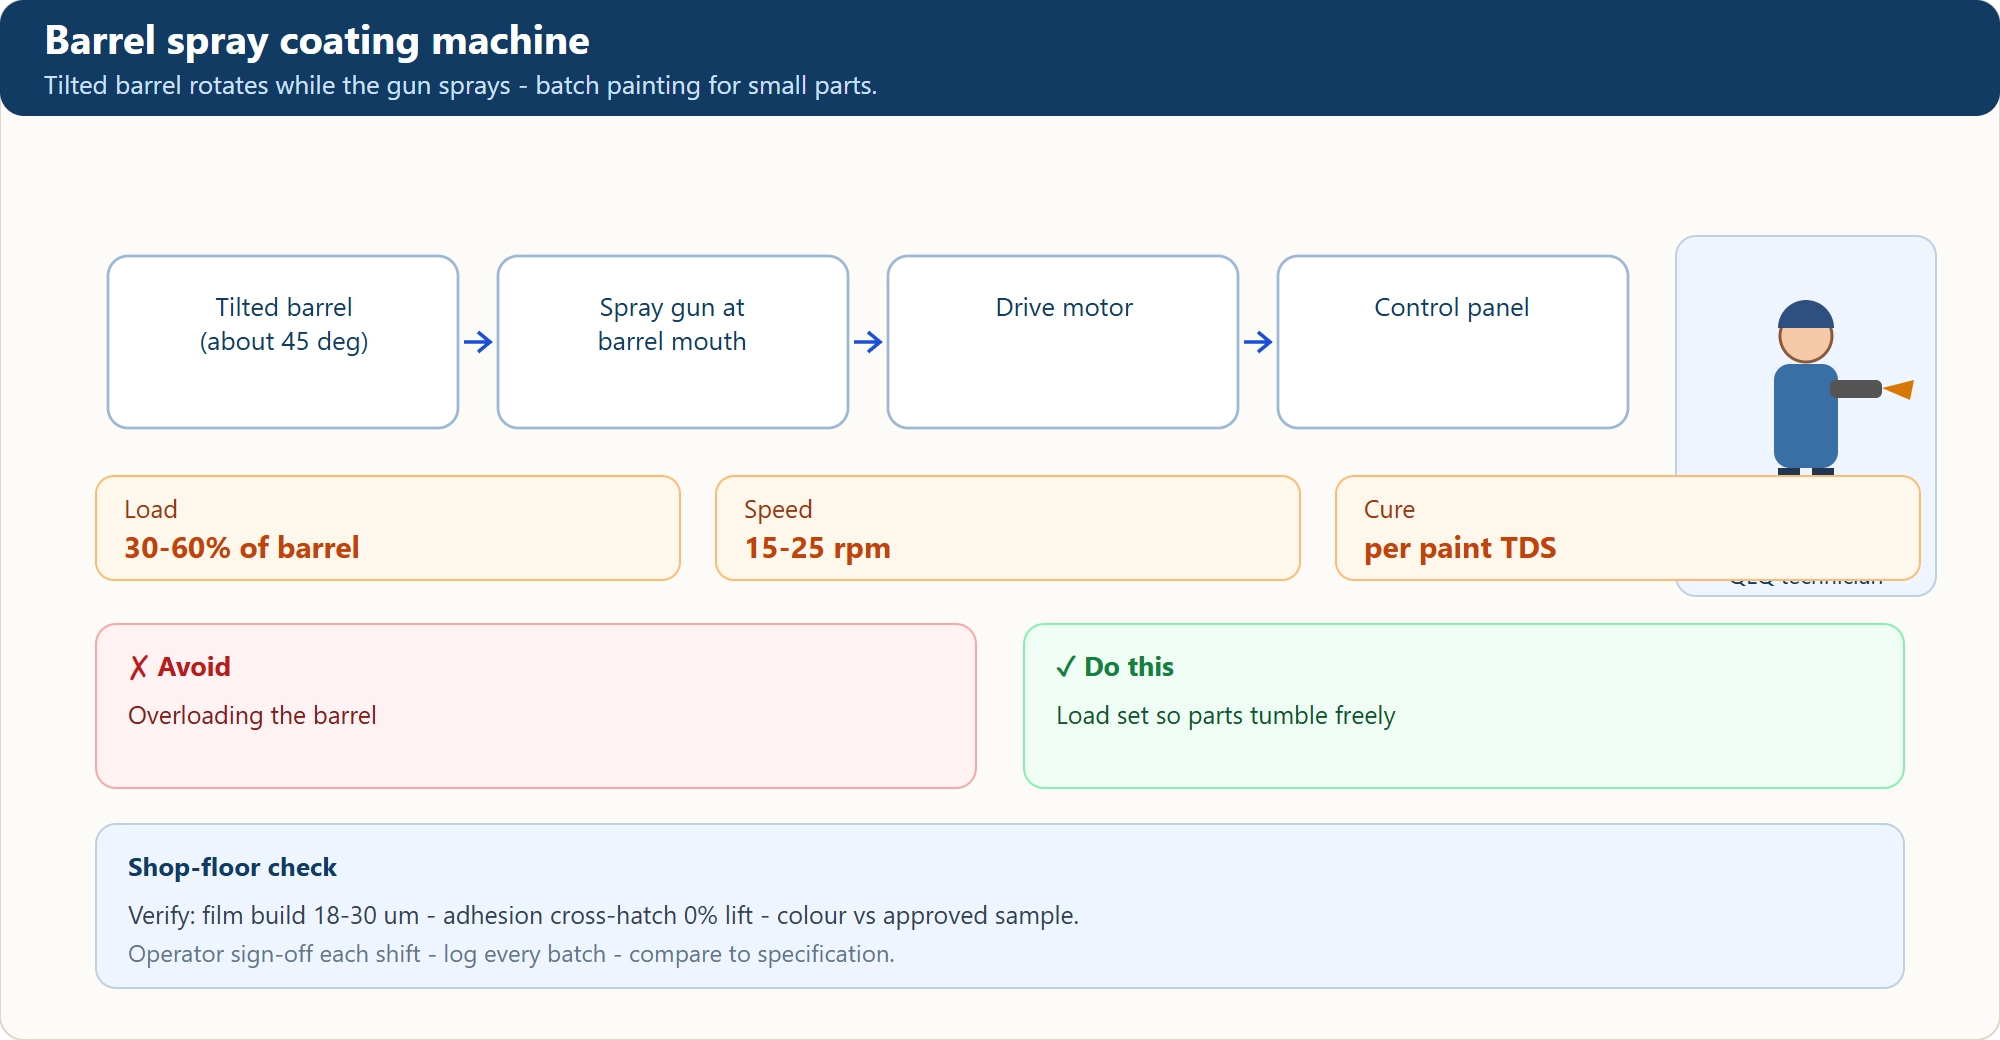
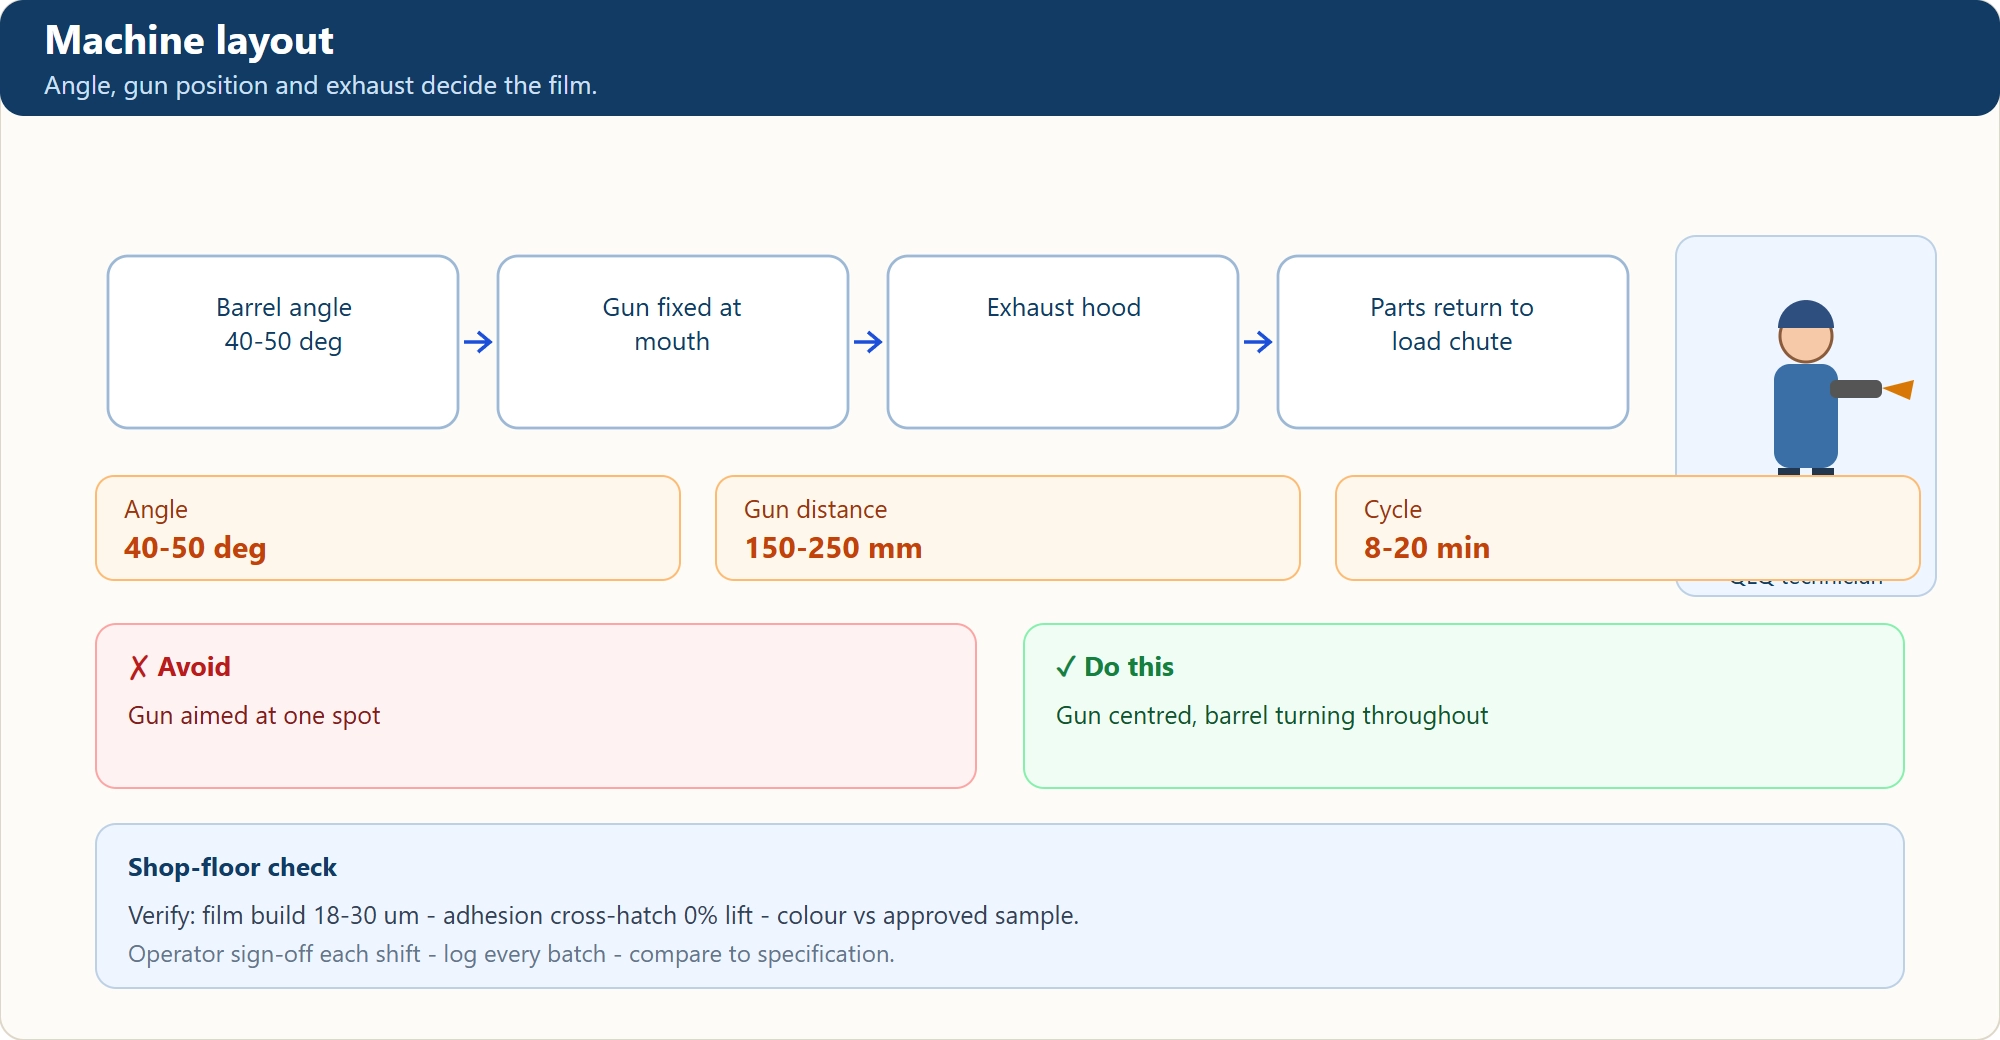
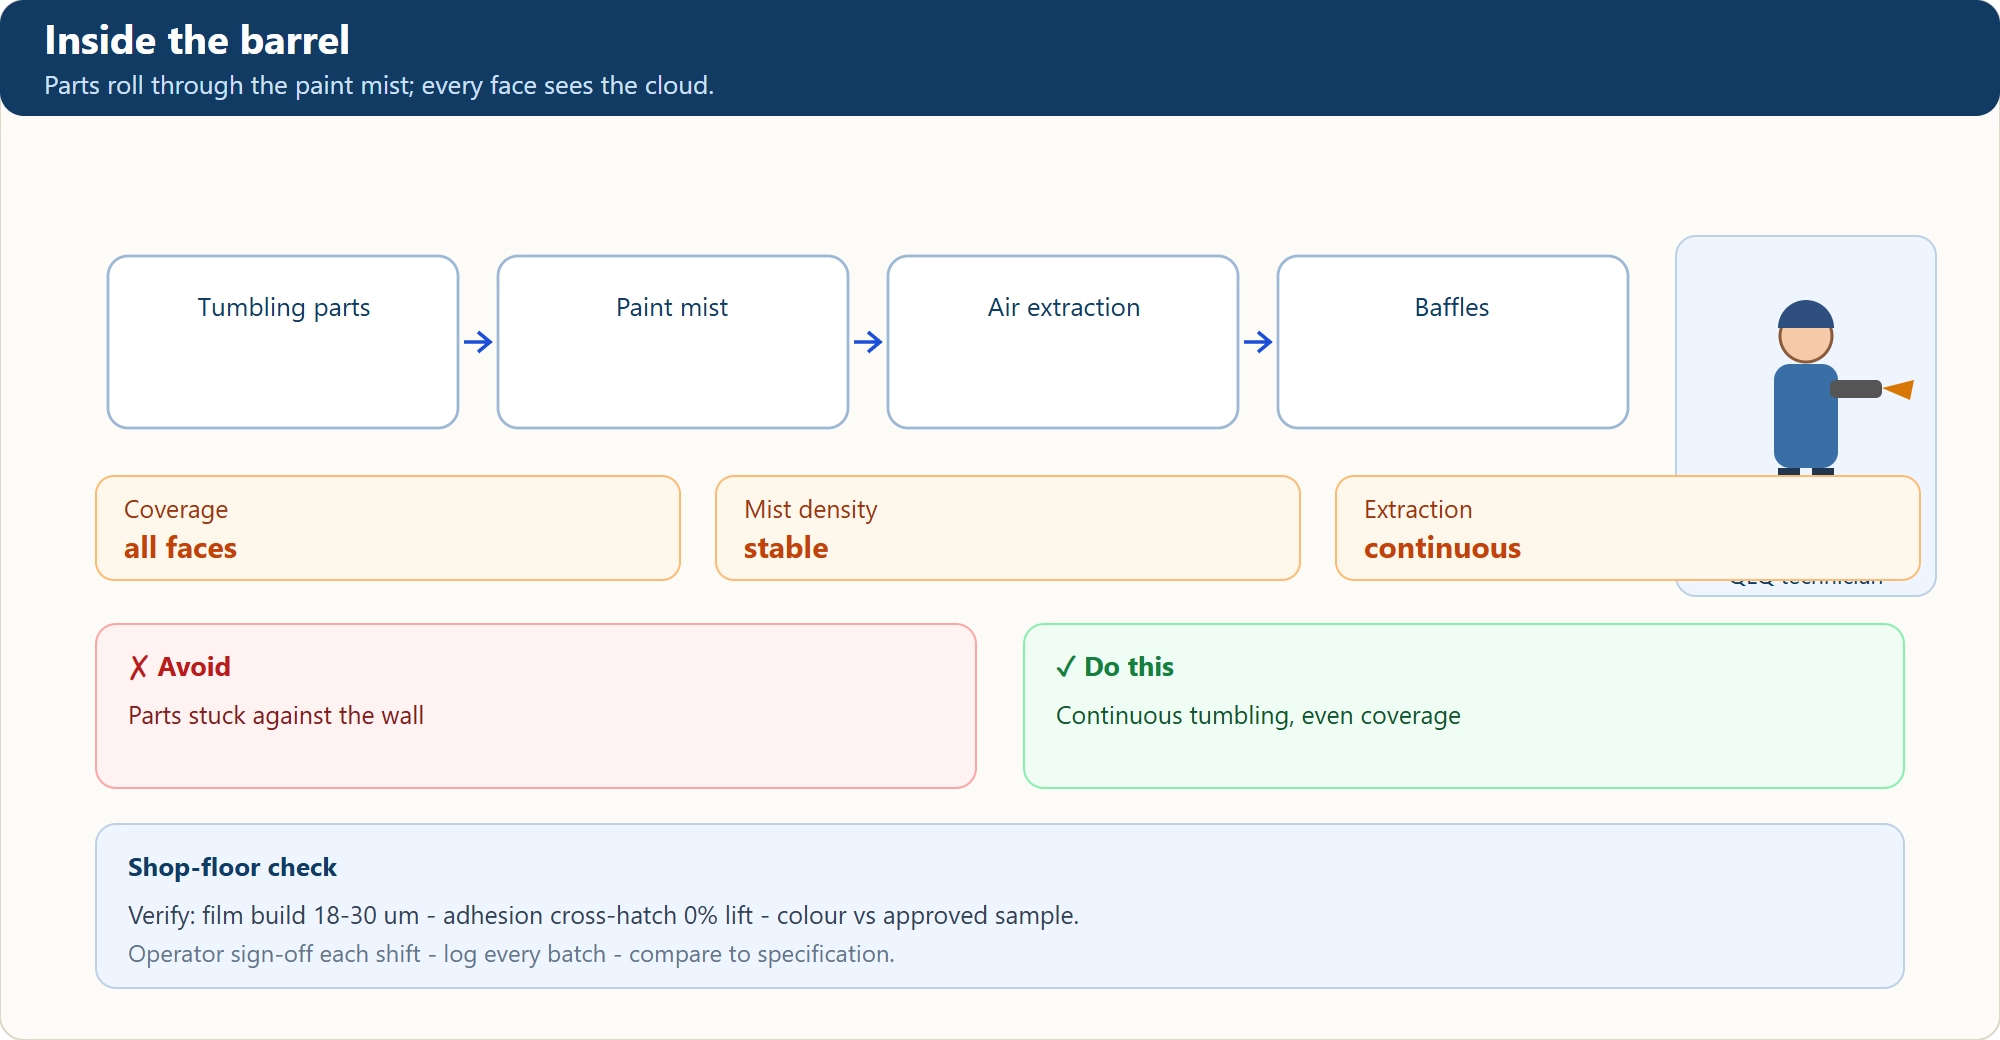
Tilted rotating barrel (30–45°) with a fixed spray gun aimed at the rolling bed of parts. The tumbling action exposes every surface to paint mist. Adjust tilt angle to control dwell time.
2Barrel Speed & Paint Parameters
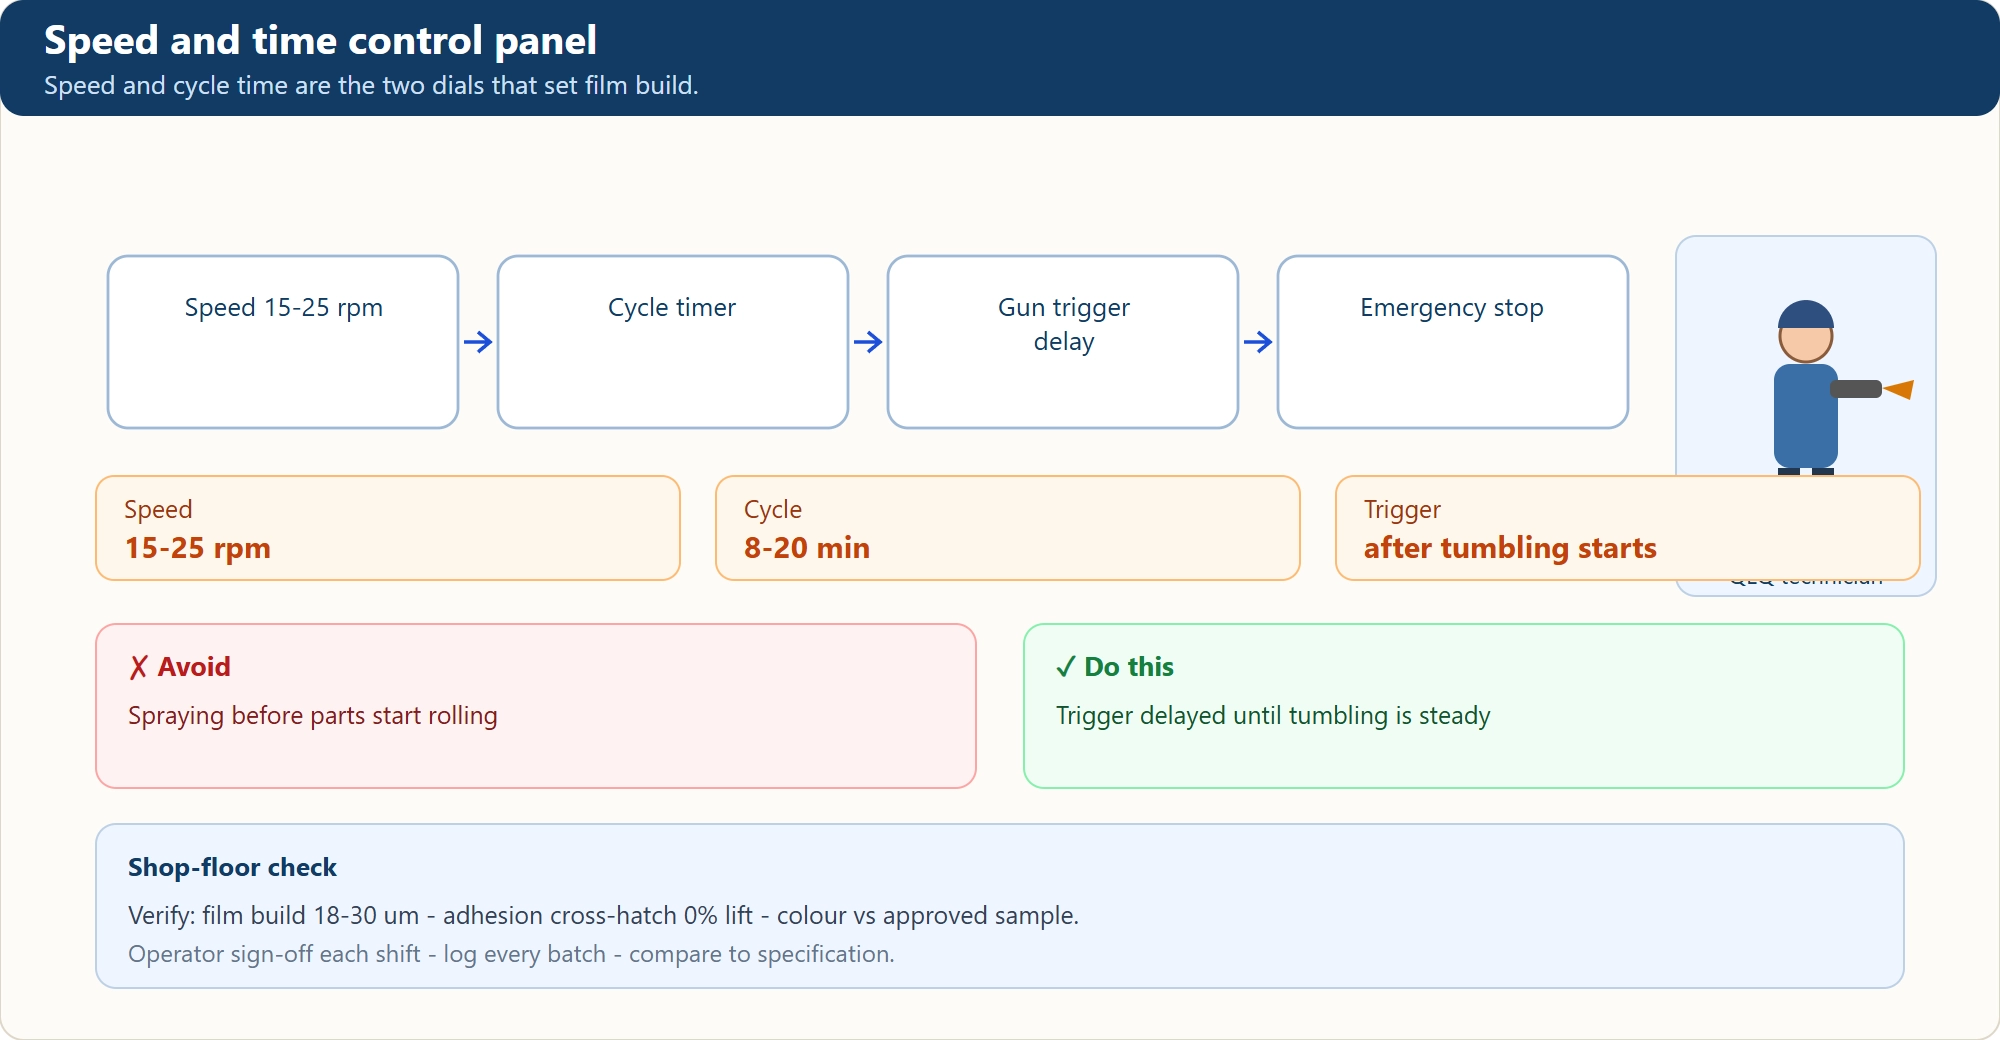
Speed 15–25 rpm — too fast = parts pinned by centrifugal force, no tumbling; too slow = uneven coverage. Atomizing air pressure 0.3–0.5 MPa. Fan width matched to barrel opening.
3Multi-Pass Thin Coating
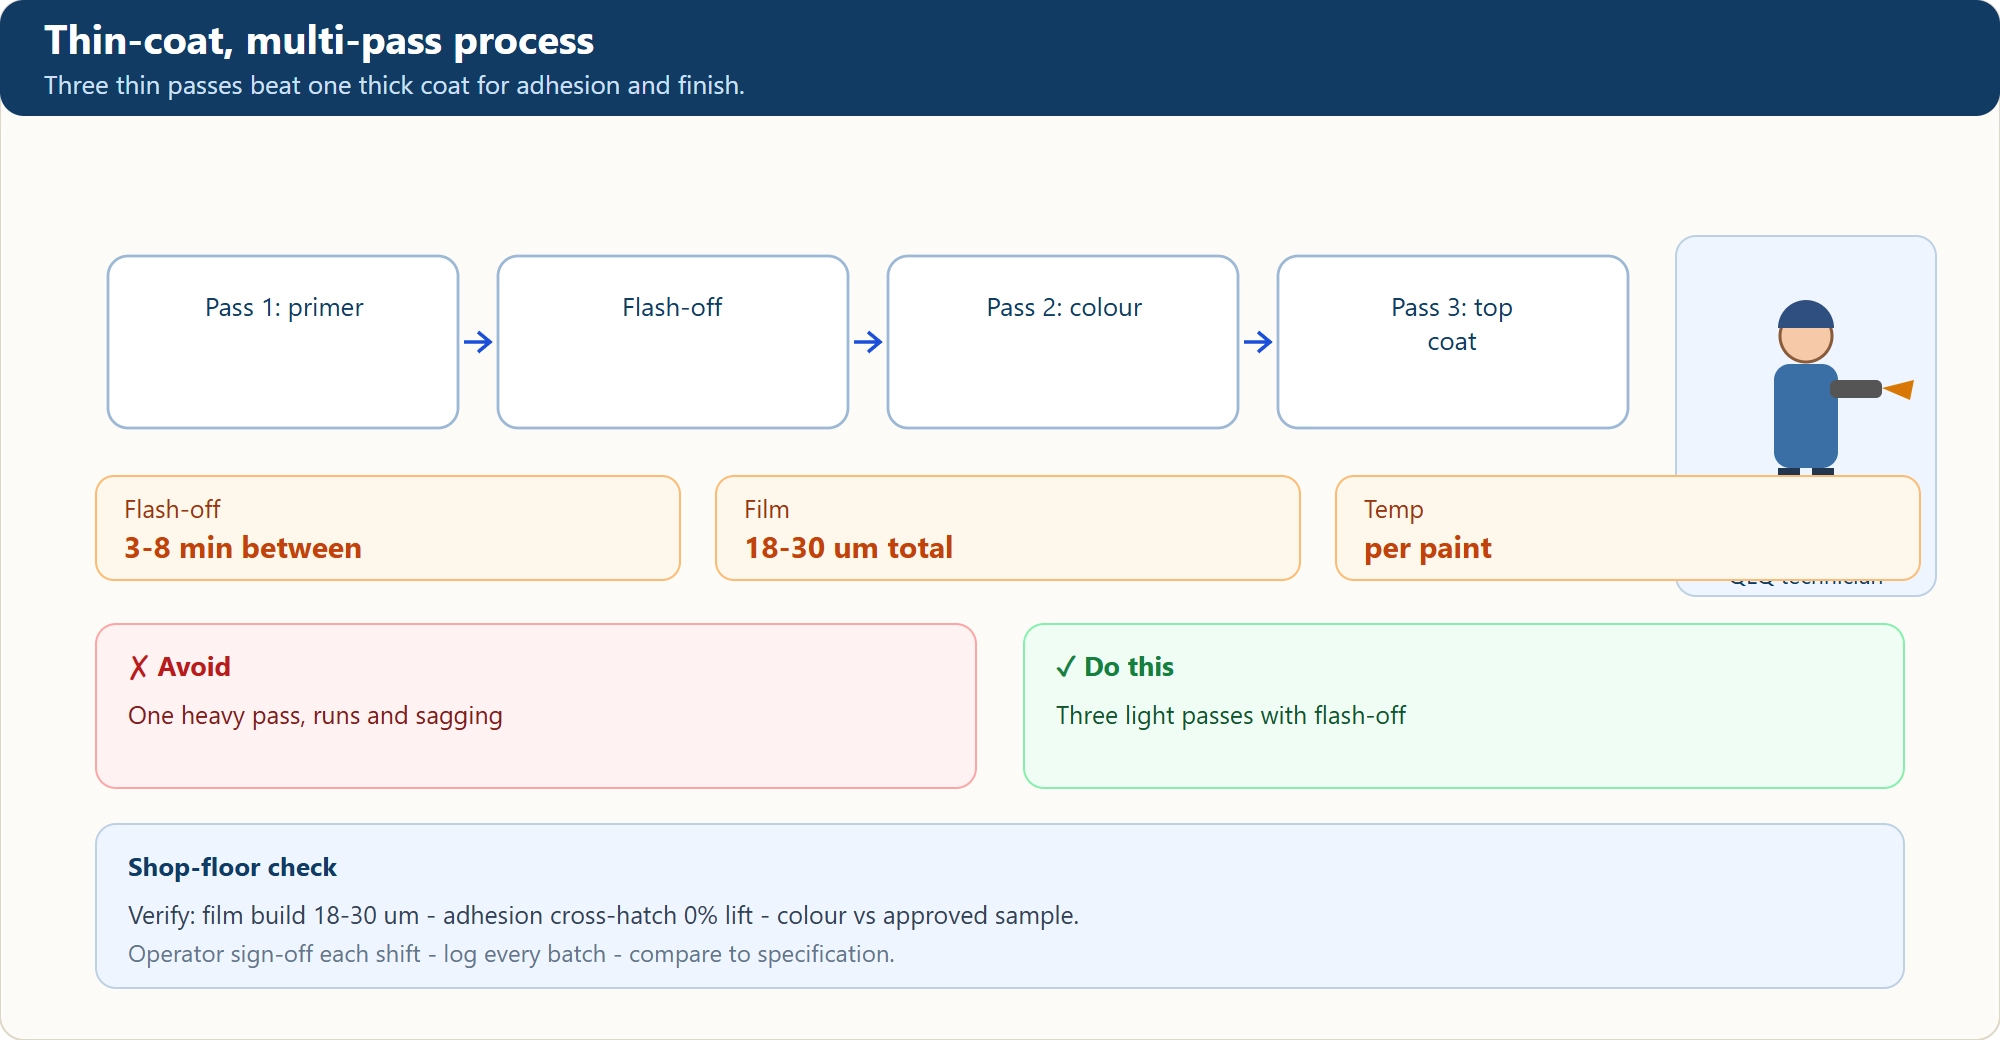
3–5 thin passes with 30–60 s flash-off between coats. Thick single-layer paint runs, sags and traps solvent — thin layers cure evenly and build a smooth finish. Total film build 30–60 μm.
4Unload & Inspection
Dump barrel contents onto a vibratory screen to separate parts. Remove any fused pairs (two parts that stuck together). Visual inspection under D65 light for coverage uniformity.
Barrel vs Hanger Painting — When to Choose Barrel
Volume and part size are the deciding factors
| Factor | Barrel Painting | Hanger Painting |
|---|---|---|
| Part size | Small (< 30 mm) | Small to large |
| Volume per shift | 10,000–100,000 pcs | 500–5,000 pcs |
| Uniformity | Good (tumbling effect) | Excellent |
| Paint waste | Higher (over-spray on barrel wall) | Lower |
| Surface damage risk | Low (parts tumble on each other) | None (suspended) |
| Operator skill needed | Medium | High |
📌 Barrel Painting Cheat Sheet
FAQ
What is the ideal load weight for a 600 mm barrel?
How to fix orange peel texture in barrel painting?
Can barrel painting do metallic or pearl colors?
Why do some parts come out with bare spots?
How to clean the barrel between color changes?
Get a Free Quote Today
Send us your samples or drawings — our engineers reply within 24 hours with pricing and technical advice.
Contact UsBarrel / tumble painting parameters
| Parameter | Typical | Effect |
|---|---|---|
| Load weight | Per drum rating | Overload gives bare patches |
| Rotation speed | Low, steady | Fast rotation bruises soft parts |
| Paint volume | Measured per load | Too much pools in recesses |
| Drying air | Warm, filtered | Cold air gives a dull film |
| Cycle time | Fixed program | Short cycles leave thin edges |
FAQ
Which parts should never be barrel painted?
Thin walls, sharp threads and parts where two faces must stay paint-free. Use rack instead.
How do we fix bare patches?
Reduce load and increase rotation time before adding more paint - volume is rarely the real problem.