Professional Zinc Alloy Surface Finishing Solutions
Sodium Carbonate
Sodium Carbonate
Générer un code QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Sodium Carbonate (Na2CO3) - soda ash - is the finishing line's general-purpose alkali and cleaner builder. It is a white, water-soluble powder (the dense grade flows best in automatic dosing) used in three distinct places: as the buffering alkali in alkaline soak and electrocleaners at 15-50 g/L, as the safe way to raise nickel bath pH when iron must be precipitated out, and as the cheap neutralizing alkali for acid waste before discharge. In QLQ's finishing plants soda ash builds the pre-cleaner and electrocleaner stages of the nickel-chrome hardware lines and corrects pH in the nickel tanks. The market sells light and dense soda ash, and technical grades at 99.2%+ total alkali; for finishing work the specification that matters is low iron and low chloride, because iron stains cleaned work and chloride rides straight into the rinse and plating stages. Carbonate chemistry carries one famous warning for platers: in cyanide zinc, copper and silver baths, carbonate is not an ingredient but a contaminant that builds up from caustic absorbing air - so soda ash must never be added to cyanide process tanks, and its level there is managed by removal, not addition.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
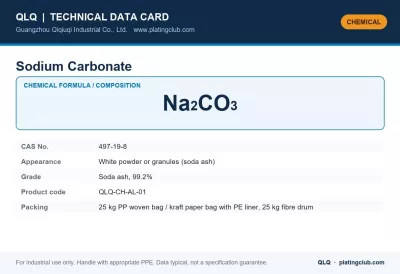
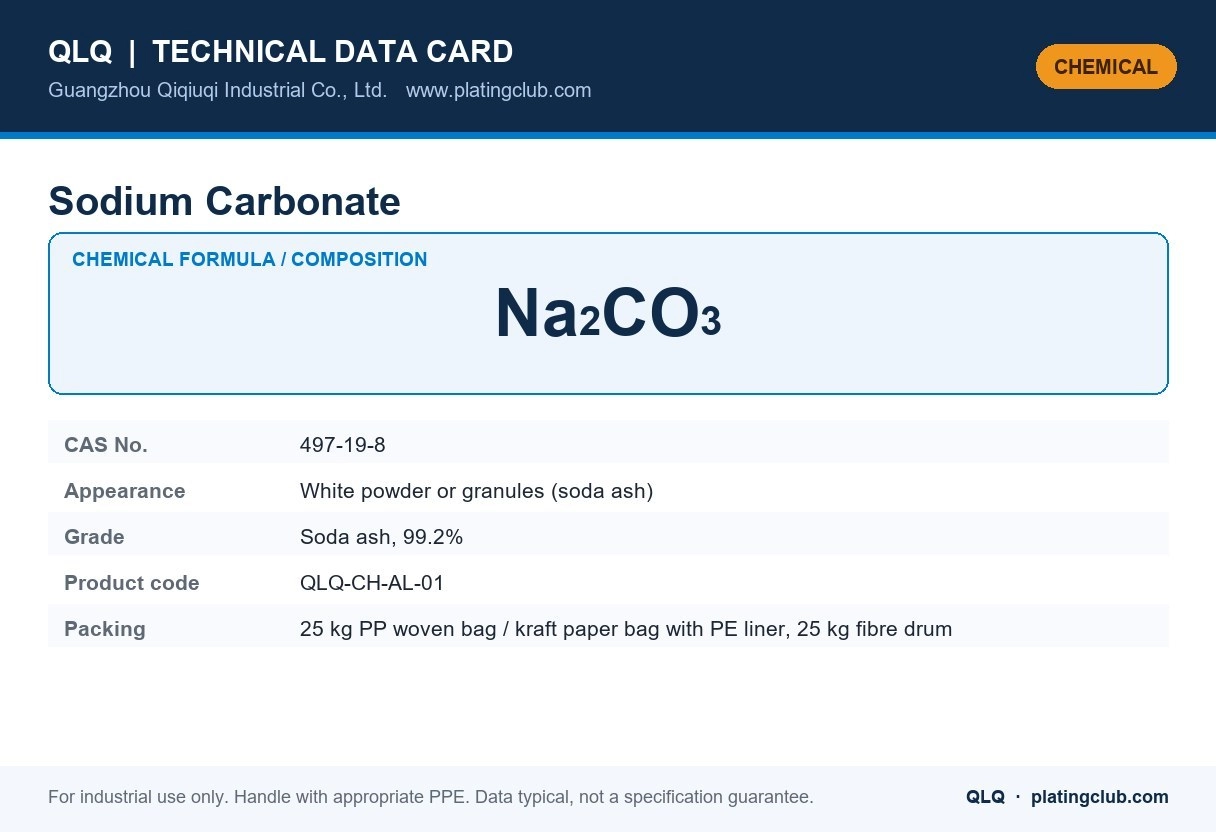
| Chemical name | Sodium Carbonate |
| Chemical formula | Na2CO3 |
| CAS number | 497-19-8 |
| Appearance | White powder or granules (soda ash) |
| Grade / type | Soda ash, 99.2% |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Sodium carbonate (soda ash) is the alkaline builder of soak and electro-cleaners and the neutralising agent used to control the pH of acid drag-out and of spilled acid.
- White powder or granules; the most economical alkaline builder in cleaner formulations.
- Gives the alkaline reserve that keeps the cleaner working as oily soil is dragged in.
- In neutralisation it produces carbon dioxide, so it is added slowly to acid spills.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Alkaline soak cleaner | 20-50 g/L with surfactants and silicates |
| Electro-cleaner | 20-40 g/L |
| Effluent neutralisation | As required to reach pH 8-9 before metal precipitation |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Corrosive (GHS05) — causes severe skin burns and eye damage |
| Personal protective equipment | Face shield + goggles, alkali-resistant gloves, rubber apron; avoid dust generation |
| Spill / first aid | Sweep or vacuum dry powder; dilute and neutralise liquid spills with dilute acid, then collect |
| Storage | Dry sealed store, off the floor, away from acids, aluminium, zinc and organic materials; keep bags closed to avoid caking and carbonation |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Why does the cleaning tank foam over? | Usually too much surfactant, or an overdose of soda ash raising the pH above the range of the surfactant. |
| Can it be used to neutralise acid spills? | Yes, carefully and in small amounts, with the reaction controlled. |
| Item | Typical Value |
|---|---|
| Chemical formula | Na2CO3 (anhydrous soda ash, dense or light) |
| Total alkali (as Na2CO3) | ≥ 99.2% |
| Appearance | White powder or granules, free-flowing |
| Sodium chloride (NaCl) | ≤ 0.5% |
| Iron (Fe) | ≤ 0.004% |
| Water insolubles | ≤ 0.05% |
| Standard packing | 40KG woven bag with PE inner liner |
How It Works in Each Station of the Line
Soda ash earns its place by buffering. In a soak or electrocleaner it holds pH in the alkaline range where oils saponify and soils lift, while its carbonate ion keeps the solution from swinging wildly as parts are dragged through. In the nickel tank it is used not for plating value but for pH correction and iron removal: when iron contamination is suspected, the bath is oxidized with peroxide, heated, and soda ash solution is added to raise pH to about 5.0-5.5 so iron hydroxide precipitates, then the bath is filtered and the pH is dropped back to the working 4.0-4.5 with sulfuric acid. Sodium carbonate is chosen for this job because it raises pH gently and predictably, unlike caustic which overshoots easily. At the effluent station the same alkali neutralizes spent acid dips before flocculation, and its buffering prevents the pH wild swings that redissolve metal hydroxide sludge.
| Station | Typical Na2CO3 level | Working note |
|---|---|---|
| Alkaline soak cleaner (steel / copper alloys) | 15-35 g/L with NaOH and silicate | 60-90°C; 3-10 min immersion |
| Electrocleaner (reverse current) | 25-50 g/L with NaOH | 60-80°C; 2-5 A/dm²; 30-90 s |
| Nickel bath pH up / iron precipitation | Dose 1-3 g/L as 100-200 g/L solution | Raise to pH 5.0-5.5, filter, re-acidify to 4.0-4.5 |
| Acid waste neutralization | Per acid titration | Neutralize to pH 6.5-9 before flocculation |
Dosing discipline: never shovel powder straight into a nickel tank - carbonate fizzes carbon dioxide, and a fast addition locally overshoots pH and dumps nickel hydroxide into the deposit. Always pre-dissolve and add slowly with agitation.
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Appearance | Visual | White, free-flowing; no grey, pink or yellow tint |
| Total alkali | Acid-base titration of a weighed sample | ≥ 99.2% as Na2CO3 |
| Chloride | Silver nitrate test on a 10% solution | Only faint haze; NaCl ≤ 0.5% |
| Iron | COA figure or thiocyanate color test | Fe ≤ 0.004%; iron stains cleaner work and streaks nickel tanks |
| Solution clarity | 50 g in 1 L warm DI water | Clear solution; sediment points to insolubles or hard-water scale in the grade |
How QLQ controls it: soda ash is bought against a written spec with chloride and iron limits, checked visually on arrival and by COA before release, and stored separately from the cleaner salts it is blended with so a mislabeled bag can never dose the wrong station. The cleaner make-up sheets record the lot used, keeping the pre-treatment chemistry traceable.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Work comes out of the cleaner with waterbreak spots | Cleaner exhausted or carbonate level low; pH fell below working range | Titrate total alkali; rebuild to 25-40 g/L carbonate; check temperature |
| White streaks appear on work after nickel | Undissolved cleaner carried over, or hard-water scale from carbonate | Improve rinsing between cleaner and acid; filter cleaner; use softened water for make-up |
| Nickel bath pH shot up during iron treatment | Soda ash added too fast or too strong a solution | Use 100-200 g/L solution, add slowly with air agitation; re-acidify gently with 1:1 sulfuric |
| Cyanide zinc bath efficiency dropping | Carbonate contaminant built up - not from soda ash additions but from caustic absorbing air | Remove carbonate by chilling and settling or proprietary removal; keep tanks covered |
| Effluent pH swings and sludge redissolves | Caustic-only neutralization overshooting past the hydroxide precipitation window | Use carbonate buffered neutralization to pH 6.5-9; hold and mix before settling |
Handling & Safety for the Plating Line
- Health: soda ash dust is alkaline and irritates eyes, nose and skin, especially when damp. Wear goggles, gloves and a dust mask when opening bags and weighing.
- Dissolving: carbonate dissolves with mild heat of solution; use warm water and stir. Pre-dissolve before any tank addition - dry powder dumped into a bath can bridge, sink and dissolve explosively later.
- Storage: soda ash absorbs moisture and CO2 from air, forming lumps and losing assay. Keep bags sealed on pallets in a dry store, and rotate stock.
- Mixing rule: never add soda ash to hot concentrated acid - violent foaming. Neutralization is always acid-into-water or carbonate-solution-into-dilute-acid with mixing.
- Spills: sweep dry and rinse floors with water; the diluted wash is mildly alkaline and safe to treat as normal rinse effluent.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of carbonate cleaning before finishing | Recommended practice |
|---|---|---|
| Iron / steel small hardware | Removes forming oils and shop soils so acid and plating act on bare metal | Soak clean 15-35 g/L carbonate at 70-90°C, rinse, then acid activate |
| Zinc alloy (sliders, buckles) | Mild buffered alkali cleans die-cast zinc without the aggressive attack of straight caustic | Keep pH moderate and time short; rinse well; avoid long dwell in hot strong alkali |
| Copper / brass | Removes tarnish-forming soils before bright acid dips | Short alkaline clean, thorough rinse, then bright dip; carbonate helps prevent filming |
| Stainless steel | Pre-cleaning only; the passive oxide is finished by acid, not alkali | Clean then proceed to acid pickle/activation; stainless tolerates the cleaner well |
FAQ
| Question | Answer |
|---|---|
| Why is carbonate a contaminant in cyanide baths but an ingredient in cleaners? | In cyanide zinc, copper and silver solutions carbonate is a reaction by-product that reduces efficiency and must be removed. In alkaline cleaners it is the deliberate buffering alkali. Never mix the two roles up. |
| Can soda ash replace caustic soda in a cleaner? | Partially. Carbonate buffers and cleans but is weaker than caustic. Cleaners usually run both: caustic for saponification and bite, carbonate for buffering and water softening. |
| How do I raise nickel bath pH without overshooting? | Use dilute carbonate solution (100-200 g/L), add slowly with strong agitation, measure pH continuously, and raise in steps of 0.2-0.3 pH units with time to equilibrate. |
| Does soda ash help remove iron from a nickel bath? | Yes - after oxidizing the iron with peroxide, raising pH to 5.0-5.5 with carbonate precipitates iron hydroxide which is then filtered out. Confirm by analysis before returning to production. |
| Does QLQ supply dense soda ash with support? | Yes. QLQ supplies soda ash with COA covering total alkali, chloride and iron, and engineers help with cleaner formulations and nickel bath iron treatment. |
Cleaning stages underperforming or iron in the nickel tank? QLQ supplies soda ash with COA and engineers who help customers in 10+ countries balance cleaner chemistry and treat nickel baths. Contact us with your process water analysis.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.