Professional Zinc Alloy Surface Finishing Solutions
Sodium Lauryl Sulfate K12
Sodium Lauryl Sulfate K12
Générer un code QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Sodium Lauryl Sulfate (SLS, trade name K12, C12H25OSO3Na) is the classic wetting agent for nickel plating and the standard foaming anionic of electroplating pretreatment. Its job in a nickel tank is specific and easy to verify: hydrogen is evolved at the cathode during plating, and without a wetting agent the gas sticks to the work as bubbles, leaving pinholes and pits in the deposit. K12 lowers the surface tension of the bath so hydrogen releases in fine streams instead of clinging bubbles, and it keeps the nickel surface fully wetted so brightener and leveler action is even. On the cleaning side of the line it is the foaming engine of soak and electrocleaners. Market grades: needle/powder K12 at 90-93% active for bath dosing, and paste at 30-70% active for cleaning blends. The differences that matter in plating are active content (pay on real active, not on bag weight), sulfate salt content, and whether the lot is chloride-free enough for sensitive baths. QLQ supplies the low-salt needle grade with COA so dosing stays predictable.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
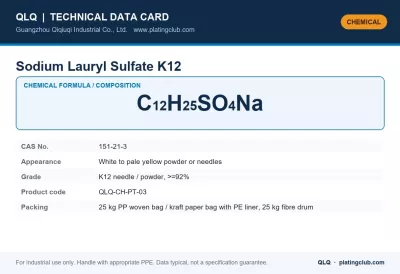
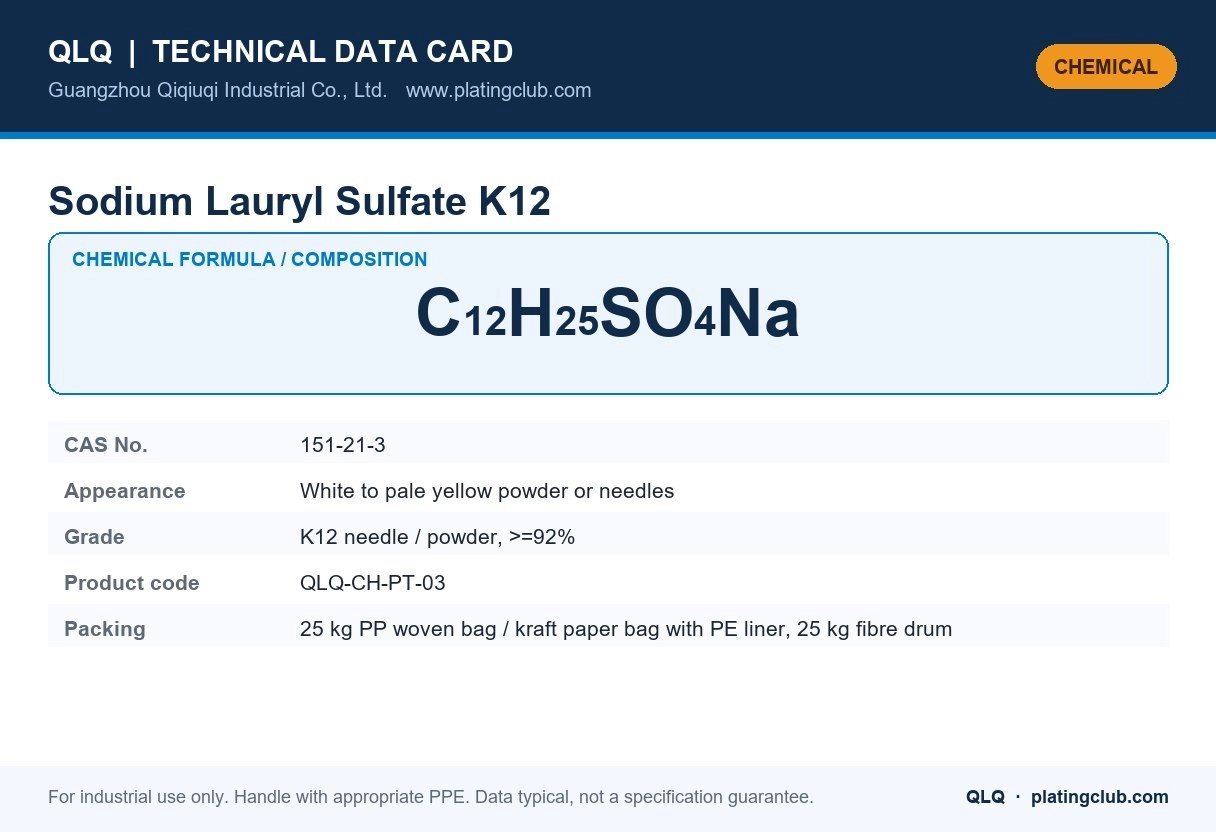
| Chemical name | Sodium Lauryl Sulfate K12 |
| Chemical formula | C12H25SO4Na |
| CAS number | 151-21-3 |
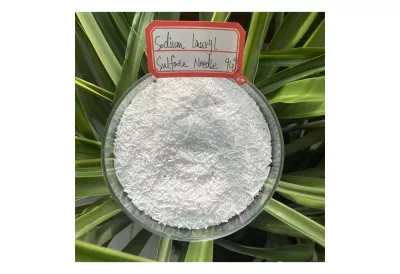
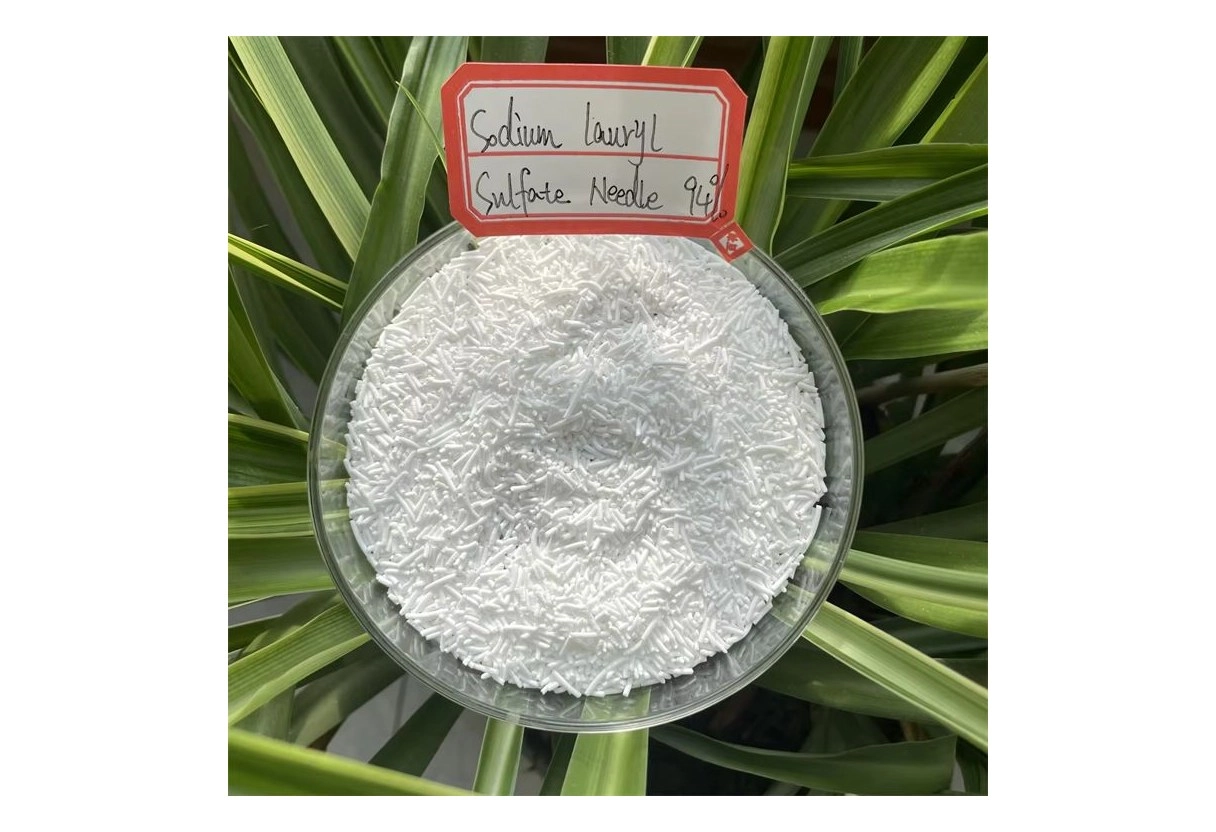
| Appearance | White to pale yellow powder or needles |
| Grade / type | K12 needle / powder, >=92% |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Sodium lauryl sulfate (K12) is the anionic surfactant used as the wetting, emulsifying and foaming agent in cleaners, in pickling inhibitors and in some plating wetting systems.
- White to pale yellow powder or needles; one of the most widely used anionic surfactants in the industry.
- Reduces surface tension so that cleaners reach the bottom of recesses and blind holes.
- Strong foamer - it needs care in spray and in high-agitation equipment.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Cleaner formulation | 1-10 g/L |
| Pickling wetting | 0.1-1 g/L |
| Note | Choose the powder grade for alkaline blends and the needle grade for liquid blends |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Irritant (GHS07) — causes serious eye irritation; mild skin irritation on prolonged contact |
| Personal protective equipment | Safety goggles and nitrile gloves; avoid contact with eyes; use good general ventilation |
| Spill / first aid | Absorb or mop up; surfactant solutions are slippery — rinse the floor with plenty of water |
| Storage | Cool, dry, ventilated store; keep containers closed, protect paste and liquid grades from frost and from moisture pick-up |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Which grade should I use in a powder cleaner? | The powder grade blends better and does not cake as easily as the needle grade. |
| Is it the same as the shampoo surfactant? | Chemically yes, but industrial grade is supplied for cleaning and plating use. |
| Item | Typical Value |
|---|---|
| Chemical identity | Sodium lauryl sulfate, C12H25OSO3Na |
| Appearance | White needle / powder, slight fatty odor |
| Active content | ≥ 92% (needle grade) |
| pH (1% solution) | 7.0-9.5 |
| Sodium sulfate | ≤ 5% |
| Chloride | ≤ 0.1% |
| Foam height (Ross-Miles) | ≥ 150 mm at 0.1% |
| Standard packing | 25KG/BAG, PE-lined |
How It Works in the Bath: K12 Anti-Pitting Dose
Nickel baths run at 45-60°C with air or cathode agitation and always evolve some hydrogen at the cathode. Surface tension of an un-wetted nickel bath is high enough for hydrogen bubbles to sit on the surface and grow; when they finally release they leave a pit that the deposit cannot fill. K12 at the right level stops this:
| K12 in bright nickel | Effect on deposit |
|---|---|
| 0 g/L | Pinholes and pitting on vertical faces; roughness at high CD |
| 0.1-0.3 g/L (normal) | Clean, pit-free deposit; steady foam collar on the tank |
| 0.5-1 g/L | Excess foam; brightness falls at low CD; foam drags out brightener |
| > 1 g/L (over-dosed) | Foam overflow, pitted look returns from trapped bubbles in foam, costly drag-out |
Consumption is mainly drag-out (K12 is not destroyed by electrolysis), so a rack line loses roughly 5-15 g per 1000 dm² plated and additions follow surface-tension measurement or a foam-height check, not guesswork.
Where Else K12 Is Used on the Line
| Application | Concentration | Note |
|---|---|---|
| Bright nickel / semi-bright anti-pitting | 0.1-0.3 g/L | Start low; confirm by panel, not by foam looks |
| Acid zinc / acid copper wetting | 0.05-0.2 g/L | Only where the formulation allows foam |
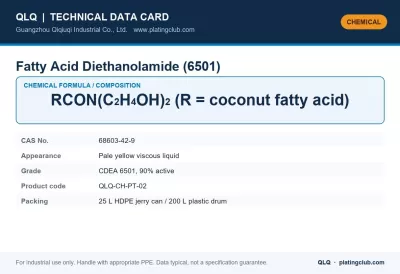
| Alkaline soak cleaner | 0.5-2 g/L | Foaming engine; pair with 6501 for stable foam |
| Electrocleaner (anodic) | 0.2-1 g/L | Watch foam at high current density |
| Barrel finishing / burnishing soap | 0.5-2 g/L | Lubricates media and parts |
Quality Checks Before Use
| Check | Method | Pass |
|---|---|---|
| Appearance | Visual vs retained sample | White needles; no yellowing or caking from moisture |
| Active content | COA (Epton titration) | ≥ 92% |
| Chloride | COA review | ≤ 0.1% (chloride stress-cracks nickel baths) |
| Surface tension | 0.1 g/L in DI water, tensiometer or stalagmometer | Reduces water from ~72 to ≤ 45 mN/m |
| Hull cell panel | Add 0.2 g/L to nickel bath, plate at 3 A | No pinholes at any current density on the panel |
How QLQ controls it: lots are checked for active content, chloride and surface-tension response against a retained reference, and every drum is Hull-cell verified in a working nickel bath before release. Because pitting complaints are nearly always traceable to wetting, the batch number on each bag lets a shop and QLQ agree in minutes whether the K12 lot - or something else - caused the defect.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Pinholes still appear with K12 present | Wetting agent exhausted by drag-out, or organic contamination | Measure surface tension; top up 0.05-0.1 g/L; carbon treat if organics present |
| Foam overflowing the tank | Over-dosed; air agitation too strong | Cut dose, reduce air, skim foam; add low-foam wetter if recurring |
| Bright range narrows after adding K12 | Dose too high for the brightener system | Keep 0.1-0.3 g/L; verify with Hull cell at low CD |
| Deposit rough with white haze | High sodium sulfate salt loading from cheap grade | Verify COA salt level; switch to low-salt needle grade |
| Dusty bags, caked powder | Moisture pickup in storage | Store sealed; dry storage; confirm active before large top-ups |
Handling & Safety
- Health: K12 powder irritates eyes and airways; wear goggles, gloves and a dust mask when weighing. Wash spills off skin promptly.
- Dosing: make a 5-10% stock solution in warm water and add by surface-tension control; never dump powder straight into a hot nickel tank (it can float, foam and locally over-dose).
- Hydrolysis note: K12 is a sulfate ester - in very hot, strongly acidic baths it hydrolyzes slowly. For acid baths above 50°C consider the sulfonate analog (sodium dodecyl sulfonate), which is hydrolysis-stable.
- Foam management: keep an anti-foam spray or a low-foam backup wetter near rack lines; a foam-over during a production run costs brightener and floor time.
- Storage: sealed bags in a dry store; K12 absorbs moisture and the active content of a badly stored bag drifts. Shelf life sealed: 12+ months.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the K12-wetted nickel layer | Practice note |
|---|---|---|
| Iron / steel hardware | Pit-free bright nickel over the copper base keeps rust and moisture from reaching steel through pinholes | K12 0.1-0.2 g/L; confirm pit-free nickel before chrome or lacquer |
| Zinc alloy (sliders, buckles) | Compact, pit-free bright nickel is the barrier that makes the Cu-Ni-Cr stack pass CASS on die-cast | Pinholes here become corrosion tunnels straight to the zinc - keep wetting verified daily |
| Copper / brass | Wetted nickel surface levels and brightens evenly, giving the mirror white finish under chrome | Use the low-chloride grade; chloride from wetter adds to bath chloride control |
| Stainless steel | In nickel strike and subsequent nickel, K12 prevents hydrogen pits that weaken adhesion of the stack | Strike baths: 0.1-0.2 g/L; avoid over-foaming in high-CD strikes |
FAQ
| Question | Answer |
|---|---|
| I still see pinholes even though I added K12. Why? | Measure the real surface tension of your bath, not the bag dosage. If it is above ~45 mN/m, wetter has been lost to drag-out or is being consumed by contamination - top up in verified steps. |
| K12 or sodium dodecyl sulfonate - which for my nickel bath? | K12 is the traditional nickel wetting agent and is fine at 45-60°C. Choose the sulfonate only if your bath runs hot and acidic enough to hydrolyze the ester, or if you need lower foam. |
| Can too much K12 cause dull nickel? | Yes - above ~0.5 g/L the excess foam and surface film suppress low-current-density brightness. Hull cell will show the low-CD haze clearly. |
| Does QLQ supply wetting agent as part of a nickel system? | Yes - QLQ's bright nickel program (QLQ-023/024/025/026) includes a matched wetting and purifier package, and engineers help you balance K12 against them by Hull cell analysis. |
Pinholes ruining your nickel finish? Send QLQ engineering a Hull cell panel and bath data - our chemists help plating shops in 10+ countries trace pitting to wetting, filtration or contamination. Contact us.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.