Professional Zinc Alloy Surface Finishing Solutions
Resist Salt (Anti-Staining Agent)
Resist Salt (Anti-Staining Agent)
Générer un code QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
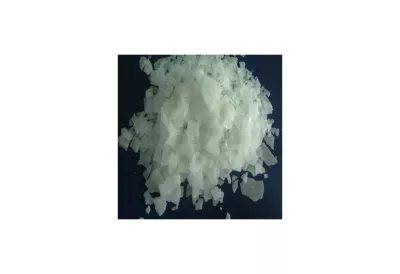
Resist Salt (Sodium m-Nitrobenzenesulfonate, C6H4NO5SNa, CAS 127-68-4) is a yellow crystalline salt with a long service record in metal finishing, where it is sold under names like “anti-staining salt” or “plating resist salt”. Its nitro group makes it a mild, controlled oxidizing agent, and that one property explains its three jobs on a plating line. First, it is an anti-staining (anti-discoloration) auxiliary: added to post-plating dips or rinse stages, it oxidizes the reducing residues and sulfide films that would otherwise brown or yellow bright nickel, copper and silver surfaces during drying, storage and export. Second, it is a bath additive for nickel and copper solutions: at low levels it oxidizes excess reducing impurities, refines crystal growth and helps keep deposits uniform and bright. Third, it is the standard oxidizer component of acid nickel-stripping formulations, where it keeps the dissolving nickel surface active so stripping is fast and even. Market grades differ in active content (≥ 90% standard, ≥ 96% refined) and moisture; quality lots are dry, free-flowing yellow powder that dissolves to a clear yellow solution.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
| Chemical name | Resist Salt (Anti-Staining Agent) |
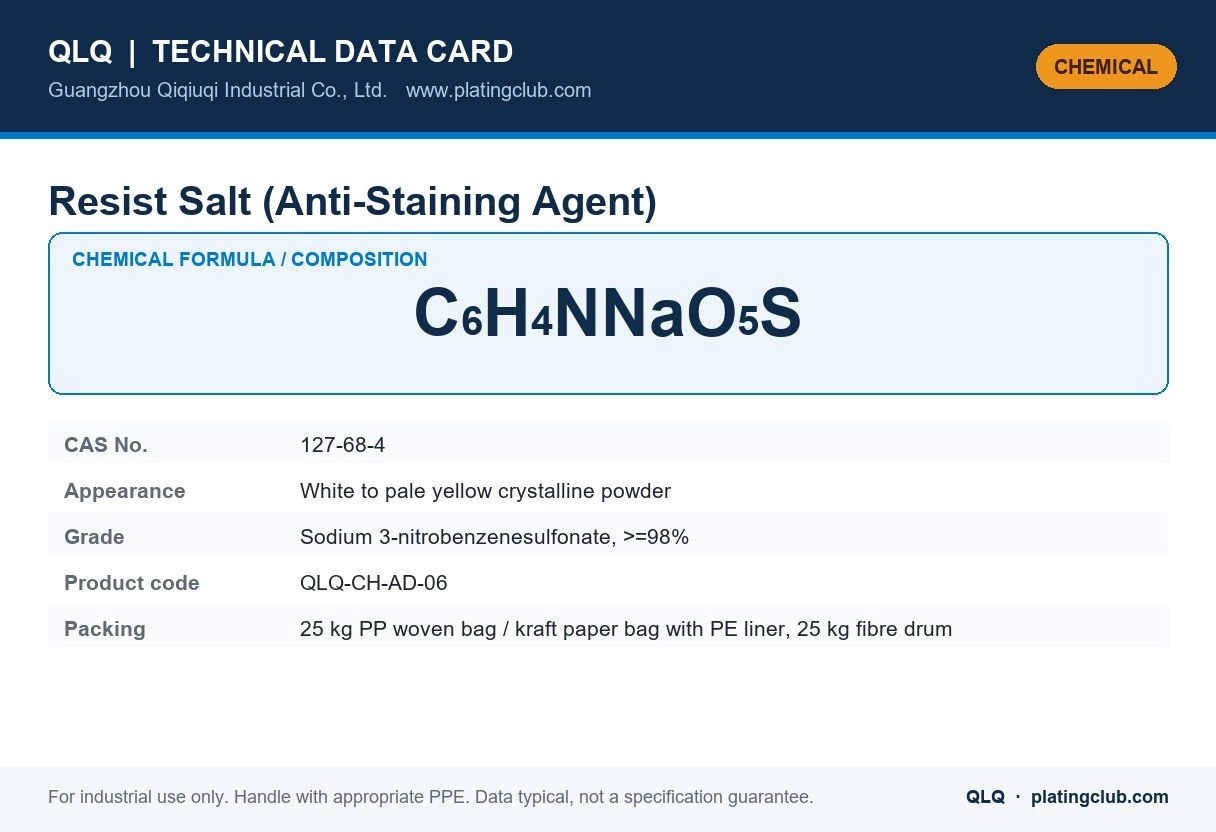
| Chemical formula | C6H4NNaO5S |
| CAS number | 127-68-4 |
| Appearance | White to pale yellow crystalline powder |
| Grade / type | Sodium 3-nitrobenzenesulfonate, >=98% |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Resist salt (sodium 3-nitrobenzenesulfonate) is the anti-pitting and anti-staining additive used in barrel nickel and in zinc baths to stop the pitting that causes rejects on small hardware.
- White to pale yellow crystalline powder; used at 5-20 g/L in barrel nickel baths.
- Also used as a resist salt in anodising and dyeing processes and as a mild oxidiser in some systems.
- Prevents the gas pitting and staining that is the main cause of rejects in barrel nickel plating of sliders.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Barrel nickel | 5-20 g/L depending on the barrel loading |
| Zinc bath | As specified by the formulation |
| Analysis | By titration or colorimetric method |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Not classified as dangerous for transport in most cases; observe good industrial hygiene and dust control |
| Personal protective equipment | Dust mask, goggles and gloves for powder handling; general ventilation |
| Spill / first aid | Sweep up dry; material is a nuisance dust — avoid breathing the dust |
| Storage | Cool, dry, sealed store; keep bags closed, off the floor and away from moisture |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Why do my barrel-plated sliders show grey spotting? | Usually pitting from gas bubbles or from an organic load; check the resist salt level and the bath filtration. |
| Is it the same as the anti-staining agent in anodising? | The chemistry is the same family; the dose and the process differ. |
| Item | Typical Value |
|---|---|
| Chemical identity | Sodium m-nitrobenzenesulfonate, CAS 127-68-4 |
| Appearance | Yellow to light yellow crystalline powder |
| Active content | ≥ 90% (standard), ≥ 96% (refined) |
| pH (1% solution) | 7.0-9.0 |
| Moisture | ≤ 3.0% |
| Solubility | Freely soluble in water - clear yellow solution |
| Ionic type | Anionic; stable in acid and alkali |
| Standard packing | 25KG/BAG, PE-lined |
How It Works: The Three Jobs on a Plating Line
Because the nitro group slowly oxidizes reducing species, resist salt does different work depending on where it is used. Keep the roles separate - a dose that suits a dip is wrong for a plating tank:
| Role | Working range | How it helps |
|---|---|---|
| Anti-staining / anti-discoloration dip after plating | 1-5 g/L, 60-80°C, 30-120 s | Destroys reducing film residues so bright nickel/copper stay white and clear through drying and packing |
| Nickel bath auxiliary additive | 0.5-2 g/L, maintained by analysis | Oxidizes reducing impurities, refines grain, stabilizes white color at low current density |
| Copper bath anti-stain / refining additive | 0.5-2 g/L (trial by Hull cell) | Improves uniformity of deposit in some cyanide and alkaline copper systems |
| Acid nickel-stripping formulations | 40-80 g/L with mineral acid (per recipe sheet) | Oxidizer keeps the nickel surface active; strip is fast and even without pitting the substrate |
Consumption in dips is mostly drag-out; in plating baths it is consumed chemically as the nitro group is reduced, so additions follow analysis, not a calendar. QLQ provides a written recipe sheet with every order so the four roles are not confused on the line.
Why Plated Parts Stain (and How the Dip Stops It)
Freshly plated nickel and copper look bright at the tank, but traces of reducing agents - drag-in from cleaners, decomposed brightener residues, sulfides in the water - keep reacting on the surface after rinsing. Over hours or days they form the faint yellow-brown film shops call staining or tarnish-in-the-bag, which European bag and belt brands reject. The resist-salt dip oxidizes those residues while the part is in the tank, so the surface dries neutral and stays clear:
| Step | Operation | Detail |
|---|---|---|
| 1. Final rinse | Clean water after the last process tank | Keep drag-in low; the dip is not a cleaner |
| 2. Resist-salt dip | 1-5 g/L at 60-80°C, 30-120 s | Use DI or softened water; agitate gently |
| 3. Hot rinse | 60-80°C, 15-30 s | Removes excess salt so no yellow residue dries on |
| 4. Dry and pack | Dry below 80°C | Verify by humidity test: 24 h at 40°C / 90% RH |
Quality Checks Before Use
| Check | Method | Pass |
|---|---|---|
| Appearance | Visual vs retained sample | Dry yellow powder, free-flowing, no dark lumps |
| Active content | COA (nitro-group titration) | ≥ 90% (standard grade) |
| pH (1% solution) | pH meter | 7.0-9.0 |
| Solubility | 10 g in 100 ml warm water | Clear yellow solution, no residue |
| Humidity test | Dip bright nickel panel, rinse, dry, 24 h at 40°C/90% RH | No yellow-brown staining vs untreated control |
How QLQ controls it: every lot is checked for active content, pH and real humidity-test performance on bright nickel panels against a retained reference before release. Because the complaint that matters is “parts stained after export”, QLQ keeps the batch traceable and can reproduce the customer’s dip conditions in its own lab to confirm the lot performed correctly.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Staining returns weeks after dip | Dip exhausted by drag-out, or parts re-wetted before packing | Top up by analysis; dry fully before packing; add desiccant if needed |
| Yellow residue on dried parts | Dip too strong or no hot rinse after it | Cut to 1-3 g/L; add the hot rinse step; confirm with humidity test |
| Nickel low-current range turns hazy | Over-dosed in the plating bath itself | Reduce to 0.5-1 g/L; Hull cell after adjustment; dummy if needed |
| Stripping slows mid-batch | Oxidizer consumed; acid diluted by drag-in | Replenish per recipe; analyze acid and salt; strip in fresh solution |
| Parts etched in strip bath | Acid too strong or wrong substrate for acid strip | Check recipe and substrate; protect copper/brass with correct formulation |
Handling & Safety
- Health: avoid inhaling dust and skin contact; wear a dust mask, gloves and goggles when weighing. Wash hands after handling.
- Nitro chemistry: the dry salt is a mild oxidizer - keep away from strong reducing agents, concentrated acids and ignition sources. Solutions are safe when handled normally.
- Do not guess-mix with cyanide: nitro aromatics and cyanide are combined only in controlled proprietary stripping formulas. Never add resist salt to a working cyanide bath on your own - gas-evolution and safety risks require the written recipe.
- Storage: sealed bags in a dry, cool store; hygroscopic product that cakes when damp. Shelf life sealed: 24 months.
- Waste: spent dips carry metal and nitro-aromatic load - treat as hazardous waste or through the effluent plant's oxidation stage; do not discharge concentrated solution to drain.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role / behavior of resist salt | Practice note |
|---|---|---|
| Iron / steel hardware | Bright nickel over steel stays white through packing - the anti-stain dip prevents in-bag yellowing that looks like rust beginning | Use the dip after the final nickel rinse, before lacquer or dry-off |
| Zinc alloy (sliders, buckles) | Protects the final Cu-Ni-Cr finish from reducing-film staining on edges and in recesses of die-cast parts | Short dip; verify no drag-in of salt to the following lacquer or passivate stage |
| Copper / brass | Copper and copper-alloy work benefits in nickel-stripping rework: controlled formulas strip nickel without eating the copper base | Use the QLQ recipe sheet for copper substrates - never the steel formula |
| Stainless steel | Not needed on bare stainless; relevant only where nickel stripping rework is done on stainless parts | Confirm substrate compatibility of the strip formula before batch rework |
FAQ
| Question | Answer |
|---|---|
| What exactly is “resist salt” in electroplating? | It is sodium m-nitrobenzenesulfonate - a mild oxidizer sold as an anti-staining auxiliary, a nickel/copper bath additive, and the oxidizer component of acid nickel-stripping formulations. The same salt serves three different roles depending on where it is used. |
| My parts stain only after sea shipment. Will the dip fix it? | Usually yes, if staining comes from reducing-film residues. Run the humidity test (24 h at 40°C / 90% RH) on dipped vs untreated panels; if both stay clean the earlier failure was drying or packing, not chemistry. |
| Can I add resist salt directly to my cyanide copper bath? | Only with a controlled, proven formula - nitro aromatics react with cyanide systems and must not be added experimentally. Use it as a bath additive only where the recipe provides for it; otherwise keep it in dips and strippers. |
| Does QLQ supply recipes with the salt? | Yes - each shipment includes a written recipe sheet for anti-stain dips and nickel-stripping use, and QLQ engineers support customers in 10+ countries with humidity-testing advice and rework troubleshooting. |
Bright nickel yellowing in storage or after export? Send QLQ engineering your humidity-test results - we help plating shops in 10+ countries stop in-bag staining at the source. Contact us.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.