
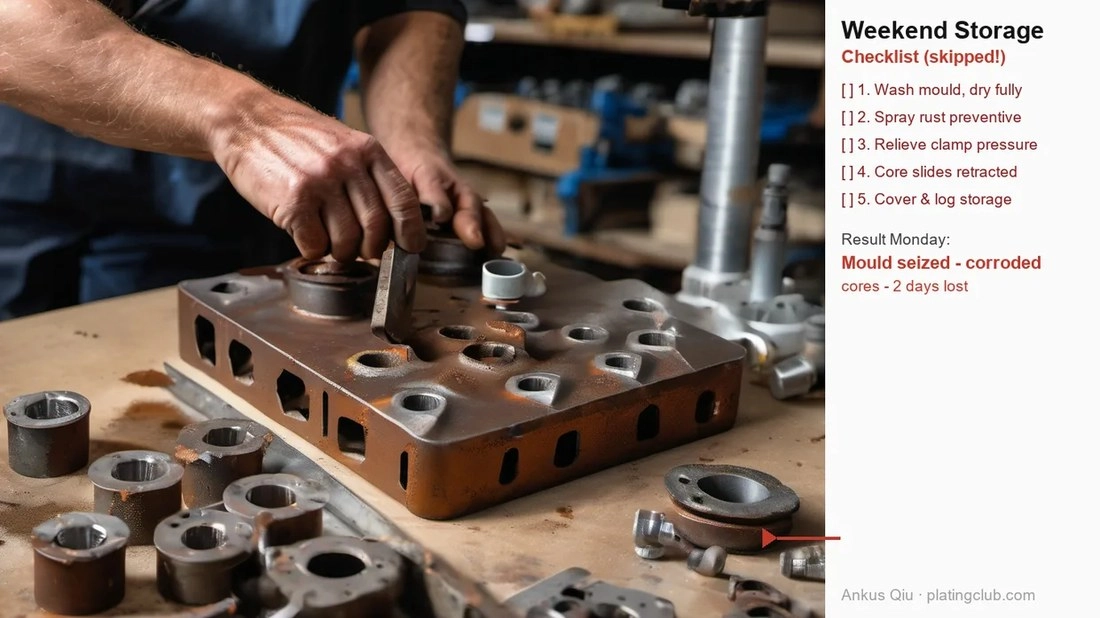
A mould seized on Monday morning and cost four hours of downtime because Friday's shutdown routine was skipped once. Dried lubricant and overnight moisture locked the slides solid.
This junior case guide covers the shutdown and start-up routine that protects moulds across the weekend: cleaning, rust prevention, storage and the pre-run checks.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Shutdown routine skipped | Slides seize by Monday | Run the checklist every Friday |
| 2. Mould left dirty | Residue holds moisture | Clean cavities and slides |
| 3. No rust preventive | Corrosion on polished steel | Spray anti-rust after cleaning |
| 4. Stored open to air | Humidity reaches the steel | Store dry, use VCI |
| 5. No preheat Monday | Thermal shock and sticking | Preheat to 180-220 C first |
| 6. Slides not checked | Seizure found under clamp | Move slides by hand before run |
| 7. Fresh lube forgotten | First shots run dry | Lube slides at every start-up |
| 8. First shots at full speed | Sticking and damage | Run 10 slow shots after start |
| 9. Storage log skipped | Same seizure next week | Sign the shutdown card |
Best Practices
- Run the shutdown checklist after the last shot Friday
- Clean and dry every cavity, slide and core
- Apply rust preventive and store in VCI
- Preheat the mould before clamping Monday
- Check slides by hand and lube before the first shot
- Log shutdown and start-up on the mould card
Implementation Roadmap
| Step | Frequency |
|---|---|
| Clean mould | After last run, every Friday |
| Protect surfaces | Every shutdown |
| Store dry | Every weekend, VCI |
| Preheat | Every Monday start |
| Check slides and lube | Every start-up |
Weekend protection flow
- Clean - Cavities, slides and cores after the last shot. (Residue holds moisture all weekend.)
- Protect - Rust preventive and VCI storage. (Bare polished steel corrodes overnight.)
- Preheat - 180-220 C before clamping Monday. (Cold steel shocks and sticks.)
- Check - Slides by hand, then 10 slow shots. (A seized slide breaks under clamp.)
One skipped shutdown caused four hours of Monday downtime. | Storage humidity below 60% RH keeps corrosion away.
Mould storage and start data
Reference values for weekend mould care on zinc lines.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Shutdown clean | After last shot Friday | Removes residue that holds moisture |
| Rust preventive | Full surface spray | Anti-rust oil, not release agent |
| Storage | Dry room, VCI, below 60% RH | Humidity is the corrosion driver |
| Monday preheat | 180-220 C surface | Prevents shock, sticking and cold shut |
| Slide check | Free by hand | Before clamping, always |
| Lube refresh | Every start-up | Dried lube locks slides |
| Slow first shots | 10 shots at reduced speed | Proves movement before full cycle |
Friday shutdown checklist
| Step | Detail | Sign off |
|---|---|---|
| Clean | Cavities, slides, cores | Date and name |
| Dry | Air blow all surfaces | Date and name |
| Protect | Anti-rust spray | Date and name |
| Store | VCI, dry rack | Date and name |
| Log | Shutdown card | Date and name |
Case 1 - one skipped shutdown cost four hours
Scenario. A mould for zinc alloy sliders seized on Monday; the Friday shutdown routine had been skipped once because the shift ended early. Dried lubricant and shop moisture locked the slides.
Action. The mould was warmed to 190 C, the stuck slides were freed with heat and gentle tapping, and the full shutdown checklist was made mandatory with a signed card.
Result. No seizure in six months, and Monday downtime for mould causes dropped from four hours to zero.
Case 2 - corrosion in a coastal plant
Scenario. A plant 200 meters from the sea found fine corrosion on cavities every Monday, even on moulds that ran fine on Friday.
Action. VCI bags, a toolroom dehumidifier and a rust-preventive spray step were added to the shutdown routine.
Result. Corrosion marks disappeared, and the toolroom humidity reading became part of the weekly check.
Frequently Asked Questions
Why seize on Monday?
Dried lubricant and moisture act over the weekend; a clean, protected mould stays free.
How long does shutdown take?
Five minutes per mould with a checklist; the seizure it prevents cost four hours.
What should I use for protection?
A proper rust preventive or VCI wrap; release agent dries and does not protect.
How dry must storage be?
Keep the toolroom below 60% RH; coastal plants need a dehumidifier.
Why preheat Monday?
A cold mould shocks the steel and causes sticking and cold shuts in the first shots.
How do I check a slide?
Move it by hand after preheat, before clamping; force under clamp breaks it.
Do I need to lube every start?
Yes - lube dries out; refresh slides at every start-up.
What speed for first shots?
Run about 10 shots at reduced speed to prove slide and ejector movement.
Why sign the card?
A signed log makes the routine visible and stops the 'somebody else' excuse.
What Would You Like to Solve?
Tell us your mould type, storage area and Monday failure pattern, and we can build the shutdown and start-up checklist for your toolroom.
FAQ - A Seized Mould on Monday: The Weekend Storage Routine That Was Skipped
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.