Professional Zinc Alloy Surface Finishing Solutions
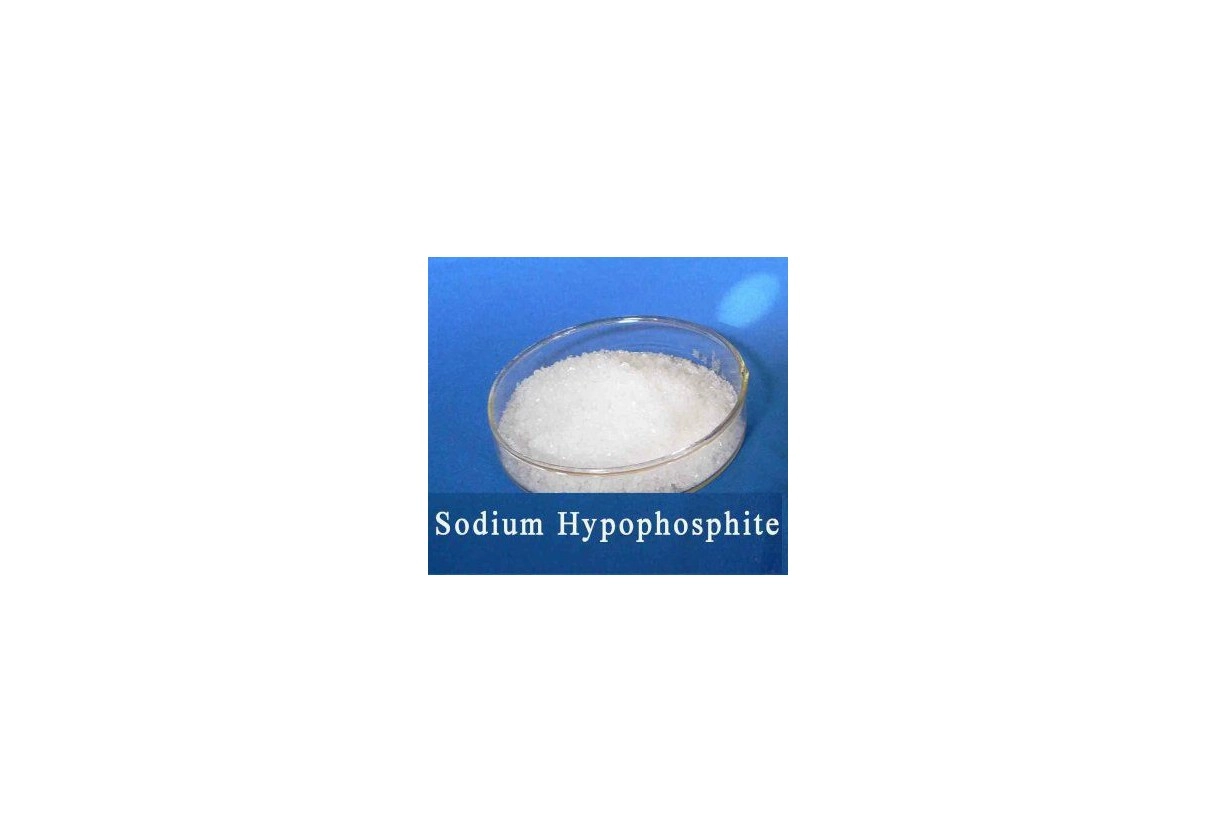
Sodium Hypophosphite
Sodium Hypophosphite
Generar código QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Sodium Hypophosphite Monohydrate (NaH2PO2·H2O) is the reducing agent that makes electroless nickel possible - the chemical that donates the electrons to turn nickel ions into a nickel-phosphorus deposit on any properly activated surface, with no anodes, no rectifier and no current-density limits. It is a white, free-flowing crystalline salt, very soluble in water, and it is the single most quality-critical input in an EN line: the bath's rate, phosphorus content, stability and service life all track the purity and consistency of this one salt. During plating only about one third of the hypophosphite consumed goes into the deposit; the rest generates hydrogen, which is why replenishment by analysis is mandatory. Market grades: EN/plating grade is produced and certified with tightly controlled heavy metals (which act as catalytic poisons or destabilisers), low sulfate and low phosphite; lower grades sold for other reducing chemistry are not held to those limits. In QLQ's plants sodium hypophosphite feeds mid- and high-phosphorus EN for corrosion and wear duty on fasteners, valve parts and electronic hardware.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
| Chemical name | Sodium Hypophosphite |
| Chemical formula | NaH2PO2·H2O |
| CAS number | 10039-56-2 |
| Appearance | White crystalline granules |
| Grade / type | Technical grade, >=99% |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Sodium hypophosphite is the reducing agent of the electroless nickel process - the chemistry that deposits nickel without any electric current, giving a uniform layer on complex shapes.
- White crystalline granules, very soluble; the phosphorus content of the deposit comes from this reducing agent.
- Electroless nickel deposits are uniform in thickness on complex shapes, which is why the process is used on hardware that cannot be racked for electroplating.
- Phosphite, the reaction by-product, builds up in the bath and limits its life; the bath is usually worked to a set number of metal turnovers.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Electroless nickel bath | 20-30 g/L sodium hypophosphite with the nickel salt and complexant |
| Operating conditions | pH 4.5-5.0 at 85-90 C for the acidic process |
| Control | Nickel and hypophosphite by titration; phosphite by titration or by MTO counting |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Not classified as dangerous for transport in most cases; observe good industrial hygiene and dust control |
| Personal protective equipment | Dust mask, goggles and gloves for powder handling; general ventilation |
| Spill / first aid | Sweep up dry; material is a nuisance dust — avoid breathing the dust |
| Storage | Cool, dry, sealed store; keep bags closed, off the floor and away from moisture |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| How do I know when to change the bath? | By the number of metal turnovers and by the phosphite level; most shops dump at 6-10 MTO. |
| Why does the plating stop? | Usually a low hypophosphite level, a pH drift or a stabiliser overdose; check the analysis in that order. |
| Item | Typical Value |
|---|---|
| Chemical formula | NaH2PO2·H2O |
| Assay | ≥ 98.5% (EN grade; premium 99%+) |
| Appearance | White crystals, free-flowing when sealed |
| Solubility (20°C) | ~ 1000 g/L in water |
| pH (5% solution) | 6.0-8.0 |
| Heavy metals (as Pb) | ≤ 0.001% (stabiliser-sensitive) |
| Sulfate / Chloride | ≤ 0.1% / ≤ 0.02% |
| Iron (Fe) | ≤ 0.001% |
| Water insoluble | ≤ 0.01% |
| Standard packing | 25KG woven bag with PE inner liner |
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Appearance | Visual against retained sample | Uniform white crystals; grey/yellow tint or damp clumps = contamination or moisture damage |
| Solubility / clarity | Dissolve 50 g in 100 ml DI water | Clear, colourless solution; no cloud, no residue |
| Assay | COA (iodometric titration) | ≥ 98.5%; reject below 98% - assay drift changes your Ni:HP ratio |
| Heavy metals | Supplier COA + periodic lab check | Pb/Fe within spec - catalytic metals change bath stability at ppm level |
| Plating-rate coupon | Make up or top up an EN bath with the new lot, plate steel coupon at 88°C for 1 h | Rate within 10% of reference (typically 12-20 μm/h); bright, adherent deposit |
How QLQ controls it: hypophosphite is the EN salt where a bad lot costs a whole bath, so every incoming lot is quarantined, assay-verified, and run as a rate coupon in a live bath before release. The batch number is recorded and kept 12 months so any rate or stability complaint can be re-tested against the exact delivery.
How It Works in the Electroless Nickel Bath
On a catalytically active surface (steel, nickel, cobalt, palladium-activated plastic), hypophosphite oxidises and donates electrons to nickel ions, depositing nickel metal while phosphorus co-deposits - the phosphorus content is set by bath chemistry and temperature, and it decides the deposit's character: mid-phosphorus (7-9%) for balanced corrosion and wear, high-phosphorus (10-13%) for maximum corrosion resistance and non-magnetic behaviour. The reaction also produces hydrogen ions, so pH falls continuously and must be held in the working window. Bath composition, temperature and the Ni-to-hypophosphite ratio interact: raise hypophosphite and rate climbs until about 30-35 g/L, then plateaus; let the ratio drift and you trade rate for stability or deposit quality.
| Parameter | Mid-P EN (typical) | High-P EN (typical) |
|---|---|---|
| Nickel sulfate NiSO4·6H2O | 25-35 g/L | 25-35 g/L |
| Sodium Hypophosphite (this product) | 25-30 g/L | 25-35 g/L |
| Complexant (lactate/citrate/glycolate system) | per process supplier | per process supplier |
| pH | 4.6-5.2 | 4.4-5.0 (lower pH favours higher P) |
| Temperature | 85-92°C | 85-92°C |
| Deposition rate | 12-20 μm/h | 10-18 μm/h |
| Phosphorus in deposit | 7-9% | 10-13% |
| Ni:HP molar ratio (maintained) | 0.30-0.45 by analysis | |
| Load ratio | 0.5-2 dm²/L | |
Consumption reference: about 125 g of sodium hypophosphite per 100 g of nickel sulfate consumed, and only a third of it ends up in the deposit - the rest leaves as hydrogen. Daily hypophosphite analysis (iodometric) is the minimum discipline on a working EN line.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Rate drops below target | Hypophosphite low (drag-out, under-replenishment) or nickel low | Analyse both; top up hypophosphite to 25-30 g/L; restore Ni:HP ratio |
| Bath decomposes (violent gas, black powder) | Overheating, stabiliser exhaustion, contamination (catalytic particles), or under-complexed bath | Shut down, cool, treat or dump per supplier; find the trigger before restarting |
| Rough or dull deposit | pH drift, low complexant, particulate in bath | Correct pH to window, verify complexant level, filter continuously at 1-5 μm |
| Skip-plating / no start on parts | Poor activation, over-stabilised bath, or load too high for the tank | Re-check activation and load; verify stabiliser ppm against supplier spec |
| Phosphorus content drifts | pH or temperature moved out of window | Hold pH ±0.1 and temperature ±2°C; re-verify with a deposit analysis |
| Lots behave differently batch to batch | Salt purity/assay spread between suppliers or grades | Buy certified EN grade; keep lot-to-lot assay spread under 0.5% |
Handling & Safety
- Health: sodium hypophosphite is low in acute toxicity, but dust irritates eyes and airways - gloves and a dust mask for weighing and dissolving are sufficient.
- Decomposition hazard: hypophosphites can decompose when heated above about 100°C or in contact with strong oxidizers, releasing toxic phosphine gas (PH3). Never heat the dry salt, never dry it in ovens, and never mix it with oxidizers (nitrate, peroxide, chlorate) in the dry state.
- Dissolving: dissolves readily in water; dissolution is mildly exothermic. Make a 30-40% stock solution and dose by analysis. Add hypophosphite separately from concentrated nickel salt - never pour both dry into the same spot.
- Bath make-up order: dissolve complexant and nickel salt first, heat, then add hypophosphite and stabiliser last. Adding hypophosphite to a hot, partially made bath is the classic way to trigger premature decomposition.
- Storage: keep bags sealed in a dry store. The salt is stable for years when dry but slowly oxidises to phosphite when damp - a damp bag measures low on assay and stresses your replenishment.
- Spills: sweep dry spills; flush residues with plenty of water. Hypophosphite in effluent consumes oxygen (BOD/COD) and can feed algae - keep it inside your discharge consent.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the EN layer from this reducer | Recommended practice |
|---|---|---|
| Iron / steel parts | Uniform Ni-P barrier on threads, bores and complex geometry - corrosion and wear duty where electrolytic nickel cannot reach | Clean, acid activate; plate 10-25 μm; post-treat or heat-treat per application |
| Zinc alloy die-castings | Not a direct substrate for acid EN - zinc dissolves and poisons the bath; EN applies only over a suitable copper/nickel undercoat | Copper plate first, then EN; keep parts out of the acid EN tank until coated |
| Copper / brass | Copper is catalytic for EN - deposits start immediately and give a bright, solder-friendly Ni-P layer used in electronics and hardware | Deoxidise lightly, rinse, plate; short dwell for thin build if brightness is the goal |
| Stainless steel | EN plates on stainless after proper activation and is used for wear, release and corrosion layers on valves and fittings | Activate (cathodic or acid); verify adhesion by bend test before production batches |
FAQ
| Question | Answer |
|---|---|
| Can I add more hypophosphite to plate faster? | Only up to a point. Rate rises with hypophosphite to roughly 30-35 g/L and then plateaus, while bath stability falls as you push higher. Keep the Ni:HP ratio in the 0.30-0.45 window and raise rate by temperature and pH, not by overdosing the reducer. |
| How do I know my salt batch caused a bath failure? | Compare: run the suspect salt as a rate coupon against your reference lot in identical small baths. A difference in rate, haze or stability at the same dose points to the salt - which is exactly why every QLQ lot is coupon-tested before it ships. |
| Why does my bath need daily hypophosphite analysis? | Only a third of the hypophosphite you add actually plates; the rest is consumed by hydrogen generation, and drag-out removes it too. Without daily iodometric analysis the ratio drifts silently, and rate or stability fails a week later with no obvious cause. |
| Does QLQ supply EN chemicals and support? | Yes - sodium hypophosphite with COA for every lot, plus process support from QLQ engineers for customers in 10+ countries: make-up schedules, analysis routines and remote defect diagnosis from photos. |
Electroless nickel misbehaving? Send QLQ your analysis values (nickel, hypophosphite, pH) and a panel photo - engineers check the ratio and stability balance and return a written recovery plan. Contact us.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.