Professional Zinc Alloy Surface Finishing Solutions
Sodium Chloride
Sodium Chloride
Generar código QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Sodium Chloride (NaCl) is the finishing shop's low-cost chloride-ion source. Its main plating job is in Watts-type nickel and nickel-iron baths, where dissolved chloride keeps nickel anodes dissolving at near 100% efficiency and raises solution conductivity. Because nickel chloride (NiCl2·6H2O) costs several times more than sodium chloride per kilogram, many shops run a blended chloride system: part nickel chloride for its nickel value, part sodium chloride for its chloride value. Beyond plating, refined salt makes the 50 g/L sodium chloride solution used for neutral salt spray testing (ASTM B117) and the brine that regenerates deionizer resin beds feeding rinse lines. In QLQ's finishing plants, salt is used in the nickel-chrome hardware lines and in the in-house salt spray cabinet that audits plated zipper sliders and buckles. Not every salt is equal for this work: vacuum-refined salt (white, ≥ 99.3%, low calcium and magnesium, no additives) is the plating-grade choice, while crude sea salt or solar salt carries calcium, magnesium, sulfate and organic residues, and common table salt may contain anti-caking agents or iodide - both of which contaminate a nickel bath.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
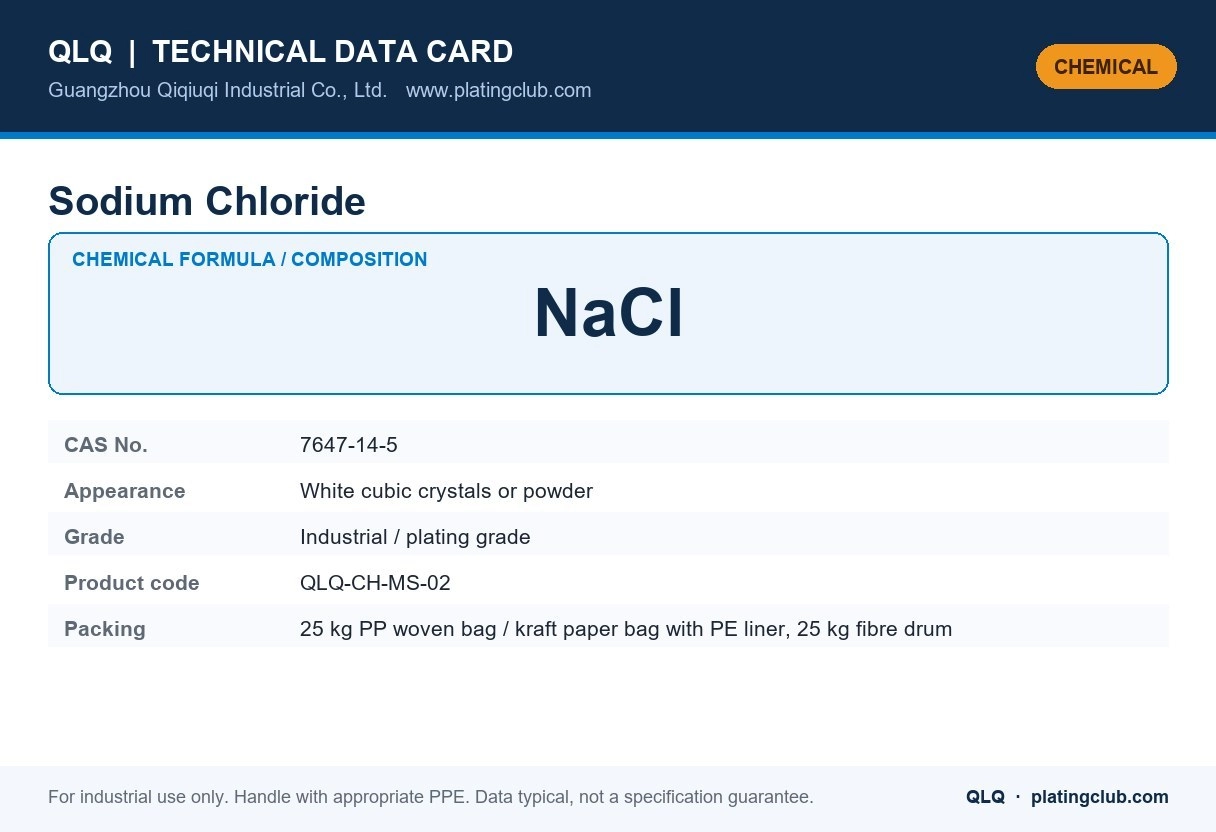
| Chemical name | Sodium Chloride |
| Chemical formula | NaCl |
| CAS number | 7647-14-5 |
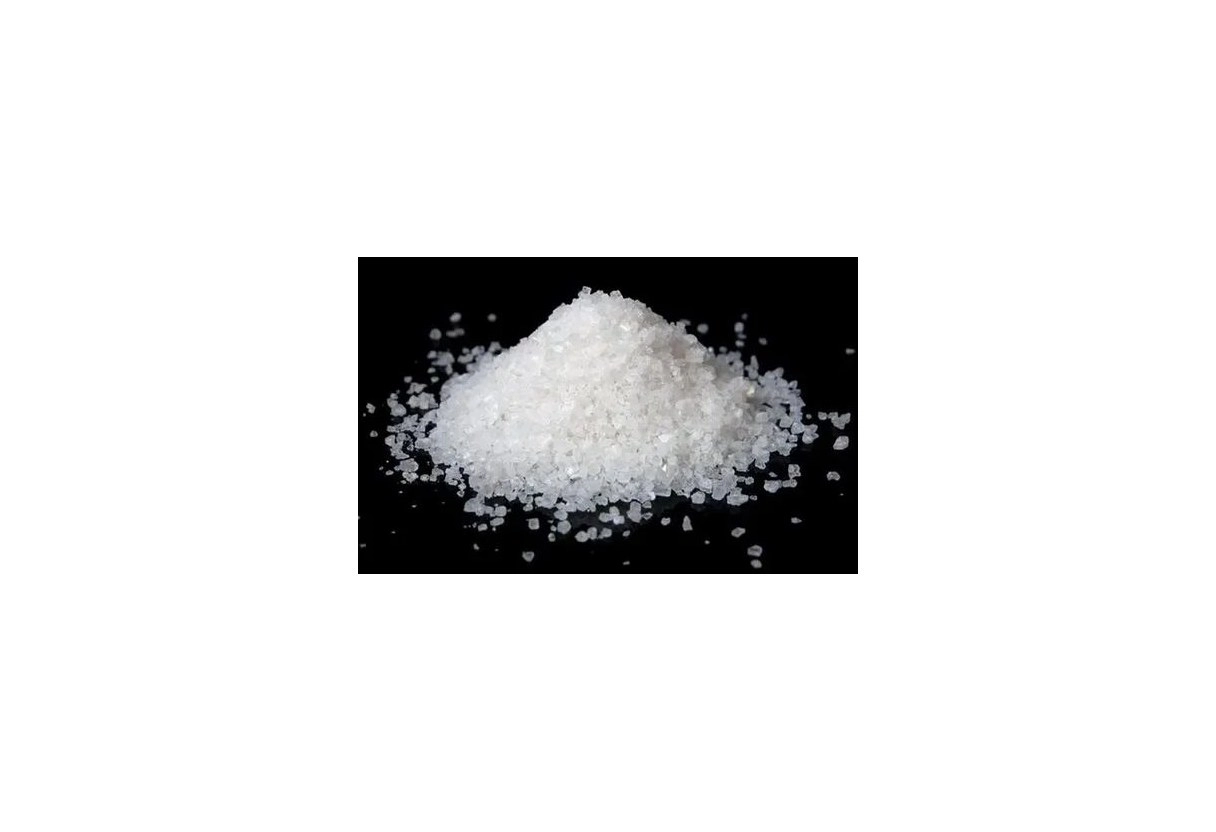
| Appearance | White cubic crystals or powder |
| Grade / type | Industrial / plating grade |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Sodium chloride is the low-cost chloride source used in zinc and nickel plating baths, in pickling accelerators, and as the brine base of many cleaning and rinsing operations.
- White cubic crystals, very soluble; the chloride ion activates the anode and helps it dissolve uniformly.
- In acid zinc baths it is added together with ammonium or potassium chloride to reach the required conductivity.
- Chloride levels must be controlled in nickel baths because too much chloride causes pitting.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Zinc chloride bath | 20-30 g/L in the ammonium chloride / zinc chloride electrolyte |
| Nickel bath (Watts type) | 20-30 g/L as an alternative to nickel chloride |
| Rinse and salt additions | As required by the bath analysis |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Not classified as dangerous for transport in most cases; observe good industrial hygiene and dust control |
| Personal protective equipment | Dust mask, goggles and gloves for powder handling; general ventilation |
| Spill / first aid | Sweep up dry; material is a nuisance dust — avoid breathing the dust |
| Storage | Cool, dry, sealed store; keep bags closed, off the floor and away from moisture |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Which chloride should I use in my zinc bath? | Sodium, potassium or ammonium chloride all work; the choice is normally made on cost and on the potassium tolerance of the bath. |
| Do you supply food grade? | Yes, food and technical grades are available; state the certificate you need when ordering. |
| Item | Typical Value |
|---|---|
| Chemical formula | NaCl |
| NaCl content | ≥ 99.3% (vacuum refined), ≥ 98.5% (industrial) |
| Appearance | White free-flowing crystals, no added anti-caking agents |
| Calcium + magnesium | ≤ 0.05% (refined grade) |
| Water insolubles | ≤ 0.05% |
| Iodide / anti-caking additives | None (specified zero for plating use) |
| Standard packing | 25KG woven bag with PE liner |
Why Chloride Matters in a Nickel Bath (and How Much NaCl Fits)
In a Watts nickel bath the anode is the source of nickel metal, but a sulfate-only solution passivates nickel anodes and the bath starves. Chloride ions break that passivation film, and the practical rule is simple: keep total chloride (as Cl-) between roughly 12 and 20 g/L for dependable anode dissolution, and never below about 5-8 g/L or anodes film over at normal current density. Nickel chloride supplies chloride and nickel at the same time; sodium chloride supplies only chloride and sodium. On a chloride basis, 10 g/L NaCl carries about the same Cl- as 20 g/L NiCl2·6H2O, which is why a common cost-saving blend replaces roughly a third of the nickel chloride with salt. Sodium is tolerated by nickel baths in moderate amounts, but it carries no plating value, so the blended bath is controlled on total chloride by titration and on nickel metal by analysis, not by habit.
| Component | Standard Watts bath | NaCl-blended option |
|---|---|---|
| Nickel sulfate (NiSO4·6H2O) | 250-300 g/L | 250-300 g/L |
| Nickel chloride (NiCl2·6H2O) | 40-50 g/L | 20-25 g/L |
| Sodium chloride (NaCl) | - | 10-15 g/L |
| Boric acid | 40-45 g/L | 40-45 g/L |
| Total chloride (as Cl-) | ≈ 12-15 g/L | ≈ 12-15 g/L |
| pH / temperature | 4.0-4.8 / 45-58°C | same working range |
Two housekeeping notes for blended operation: sulfate and hardness impurities in crude salt build calcium sulfate scale on anodes and tank walls, and sodium that is never plated out accumulates - so keep drag-out under control and let routine carbon treatment and partial dumps manage the sodium load rather than topping the bath with salt alone forever.
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Appearance & flow | Visual; shake a handful | White, free-flowing crystals; no lumps, no colored specks |
| Assay | Silver nitrate titration (Mohr) of a weighed sample | ≥ 99.3% NaCl for the refined grade |
| Additive / iodide check | Dissolve 10 g in 100 mL water; check COA | Clear solution; COA states no iodide, no anti-caking agent |
| Hardness (Ca + Mg) | EDTA titration or COA figure | ≤ 0.05%; avoids scale and haze in nickel and cleaner tanks |
| Hull cell in live nickel | Add planned NaCl amount to a 267 mL cell | Bright range unchanged; no haze, no anode filming at 2-4 A/dm² |
How QLQ controls it: salt is bought against a written specification that bans iodide and anti-caking additives, and every delivery is checked for appearance and clarity before the bags go into the nickel-line store. A Hull cell panel run on each new lot confirms the salt is electrically clean before it is used for production, and the lot number is logged against the tank record for traceability.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Nickel anodes filmed, tank voltage climbing | Chloride drifted below ~5-8 g/L or anode bags too tight | Titrate chloride; bring to 12-15 g/L with NaCl or nickel chloride; check anode bag fit and anode area |
| Dull, hazy nickel after switching salt bags | Crude or table salt brought in iodide, organics or anti-caking agents | Stop using that salt; carbon-treat the bath; re-spec vacuum-refined, additive-free salt |
| White scale on anodes and heat exchanger | Calcium/magnesium from unrefined salt, precipitated as sulfate or hydroxide scale | Flush scale mechanically or with inhibited acid; switch to low-hardness refined salt |
| Salt spray results suddenly optimistic or erratic | Wrong salt, wrong conductivity, or pH drift in the cabinet solution | Use 50 ± 5 g/L pure NaCl in DI water, pH 6.5-7.2 at 35°C per ASTM B117; check daily |
| Nickel deposit harder or more stressed over months | Sodium accumulating from heavy salt replacement without control | Analyze sodium occasionally; balance chloride source between NiCl2 and NaCl; improve rinsing |
Handling & Safety for the Plating Line
- Health: sodium chloride is a mild irritant only. Dust from handling bags can irritate eyes and airways - wear a dust mask and goggles when emptying bags in enclosed areas.
- Solution preparation: salt dissolves quickly in warm water with stirring; a 50 g/L salt spray solution is made up in DI water, not tap water, so calcium and magnesium do not distort the test.
- Corrosion: salt brine is aggressively corrosive to carbon steel racks, bus bars and concrete floors. Rinse spills promptly and keep the salt storage area dry and off the floor.
- Storage: keep bags sealed on pallets. Salt absorbs moisture and cakes, and a caked bag breaks open - not a safety hazard, but it makes weighing inaccurate.
- Contamination discipline: keep the plating salt physically separate from table salt and crude salt stores. Color-coded bags and a clear label prevent the classic mix-up that ruins a nickel bath.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the chloride from this salt in the line | Recommended practice |
|---|---|---|
| Iron / steel small hardware | Keeps the nickel anode active so the barrier nickel under chrome deposits steadily | Run blended chloride at 12-15 g/L Cl-; nickel 6-10 μm for indoor decorative parts |
| Zinc alloy (sliders, buckles) | Nickel layer quality over die cast depends on a stable anode; chloride stability avoids shutdowns and re-plates | Maintain copper underlayer practice; keep chloride constant to avoid current surges that burn zinc parts |
| Copper / brass | Stable bright-nickel deposition on brass parts for the nickel-silver look | Activate briefly, plate 3-6 μm nickel, rinse; salt plays no direct role on the copper itself |
| Stainless steel | Chloride content of the strike nickel (Woods type) governs the adhesion bridge to stainless | Woods nickel already carries its own chloride; do not substitute NaCl in strikes without re-qualifying adhesion |
FAQ
| Question | Answer |
|---|---|
| Can I replace all nickel chloride with sodium chloride? | Not sensibly. Nickel chloride also supplies 25% of the bath's nickel metal; replacing it entirely with salt forces the sulfate salt to carry the whole metal load and lets sodium build up. A partial blend is the usual practice. |
| Why is my nickel bath rough after using a cheap salt? | Impurities are the usual suspects - organics or anti-caking agents haze the deposit and calcium precipitates as scale. Switch to vacuum-refined, additive-free salt and carbon-treat. |
| Is common table salt acceptable in an emergency? | Only if it is plain iodized-free, additive-free salt, and then only for temporary make-up. Anti-caking agents and iodide are nickel-bath contaminants; verify the label before use. |
| How do I measure chloride in my nickel bath? | Titrate a bath sample against silver nitrate with chromate indicator (Mohr method); 1 mL of 0.1 N AgNO3 equals 3.545 g/L Cl- per mL used on a 10 mL sample. |
| Does QLQ supply refined sodium chloride with support? | Yes. QLQ supplies vacuum-refined salt with COA and helps customers set chloride control, blend economics and salt spray cabinet practice for plated hardware. |
Cutting nickel-line cost without cutting quality? QLQ engineers help customers blend chloride sources, set titration schedules and audit salt spray cabinets across 10+ countries. Contact us with your bath analysis.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.