
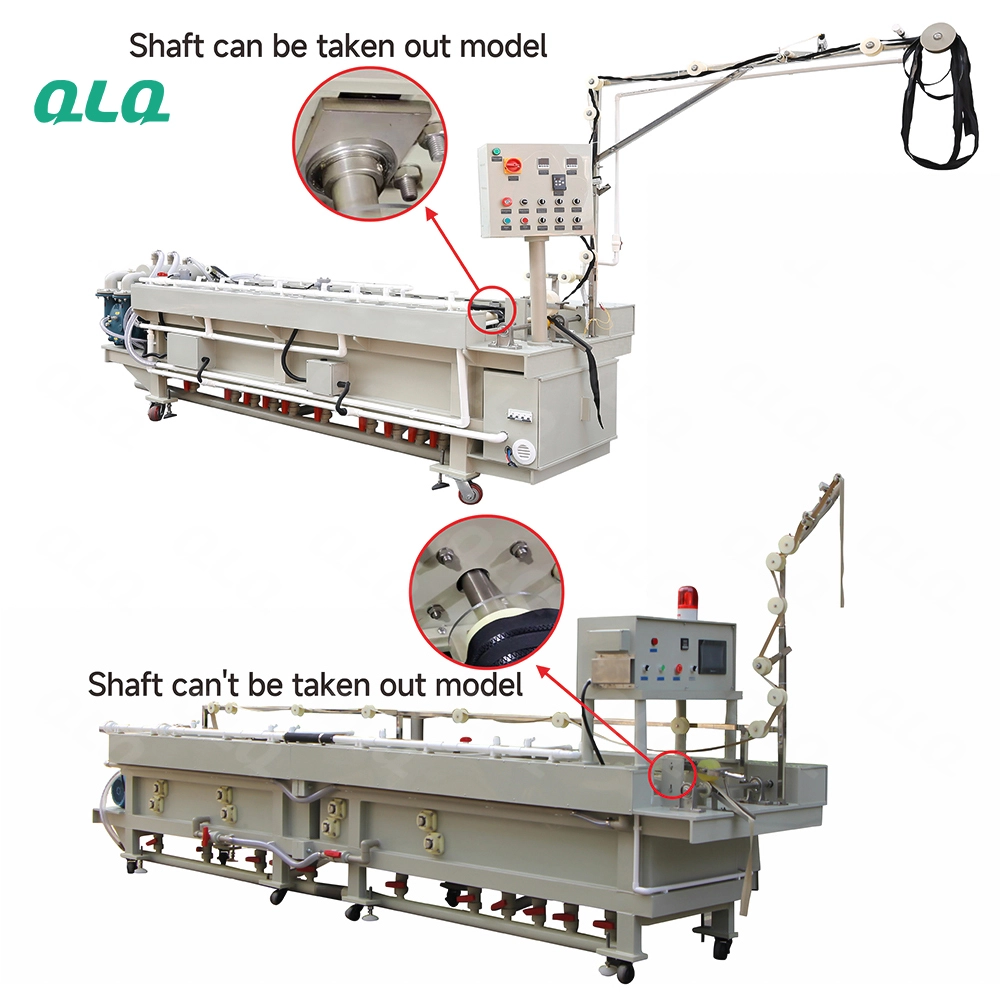
A rack line's capacity is set by the racking station: how fast parts can be loaded determines how full the line runs. Planning the station is planning the line.
This management guide covers racking throughput math, line balance, labour planning and the buffers that keep the rack line full.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Line capacity counted from tanks | Racking is the real limit | Time the racking station |
| 2. Racking time untimed | Labour plan wrong | Time per part per rack |
| 3. Rackers idle | Line starves | Balance labour to the line |
| 4. No buffer racks | One delay stops the line | Stage loaded racks |
| 5. Part change-over ignored | Throughput drops | Plan change-over slots |
| 6. One skilled loader | Absence stops racking | Cross-train |
| 7. Rack mix unplanned | Wrong racks at the station | Plan rack mix per order |
| 8. No OEE | Losses invisible | Track racking OEE |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Time the racking station, not just the tanks
- Plan labour to keep rackers ahead of the line
- Stage buffer racks at the line
- Plan change-over slots for part switches
- Cross-train rackers
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Racking capacity flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Throughput = rackers x racks/hour per person.
- Buffers absorb part delays.
- Do not rush racking - contact quality falls.
- Change-over time is real capacity.
Working Data & Formula Notes
Racking capacity data
Reference math for rack line planning.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Throughput | Rackers x racks/hour | Racking sets the line rate |
| Bottleneck | Racking or plating | Balance the slower one |
| Buffer | 2-4 loaded racks | Absorbs delays |
| OEE | Availability x performance | Losses become visible |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Racking time table
| Part | Parts per rack | Time per rack | Racks/hour/person |
| Sliders | Logged | Logged | Logged |
| Frames | Logged | Logged | Logged |
| Caps | Logged | Logged | Logged |
Implementation Cases
Case 1 - a tank line waiting on the rackers
Situation. A line with plenty of tank capacity ran at 60%; timing showed racking produced only 12 racks/hour while plating could take 18.
Approach. Racking was rebalanced with a second loader and staged buffers; part-specific time cards were posted.
Outcome. Line output rose to 90% of tank capacity; the racking station became the planning unit.
Case 2 - change-over that killed the afternoon
Situation. Every part switch cost 45 minutes of empty line because racks and tools were not pre-staged.
Approach. Change-over slots were planned with pre-staged racks and a standard switch sequence; time dropped to 20 minutes.
Outcome. The saved time added two racks per switch day; the slot is now in the schedule.
Frequently Asked Questions
Why is racking the real limit?
The line can only run as fast as parts are loaded; tank capacity beyond that is idle.
How do I time racking?
Measure parts per rack and time per rack per person, averaged across part types.
What is line balance?
Matching racking output to plating capacity so neither starves nor queues.
Why stage buffers?
Loaded racks waiting at the line absorb small delays without stopping production.
How do I plan change-overs?
Schedule slots with pre-staged racks and a standard switch sequence.
Why cross-train rackers?
One skilled loader is a risk; backups keep the station running.
What is racking OEE?
Availability x performance of the racking station; it shows where loading time is lost.
How many rackers do I need?
Divide the required racks/hour by the per-person rate, plus buffer labour.
How often review the plan?
Monthly, plus after part mix or rack design changes.
What Would You Like to Solve?
Tell us your racking times, part mix and tank capacity. We can build the throughput math, labour plan and buffer schedule for your rack line.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Rack Line Capacity and Racking Station Planning: Throughput Math and L
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.