
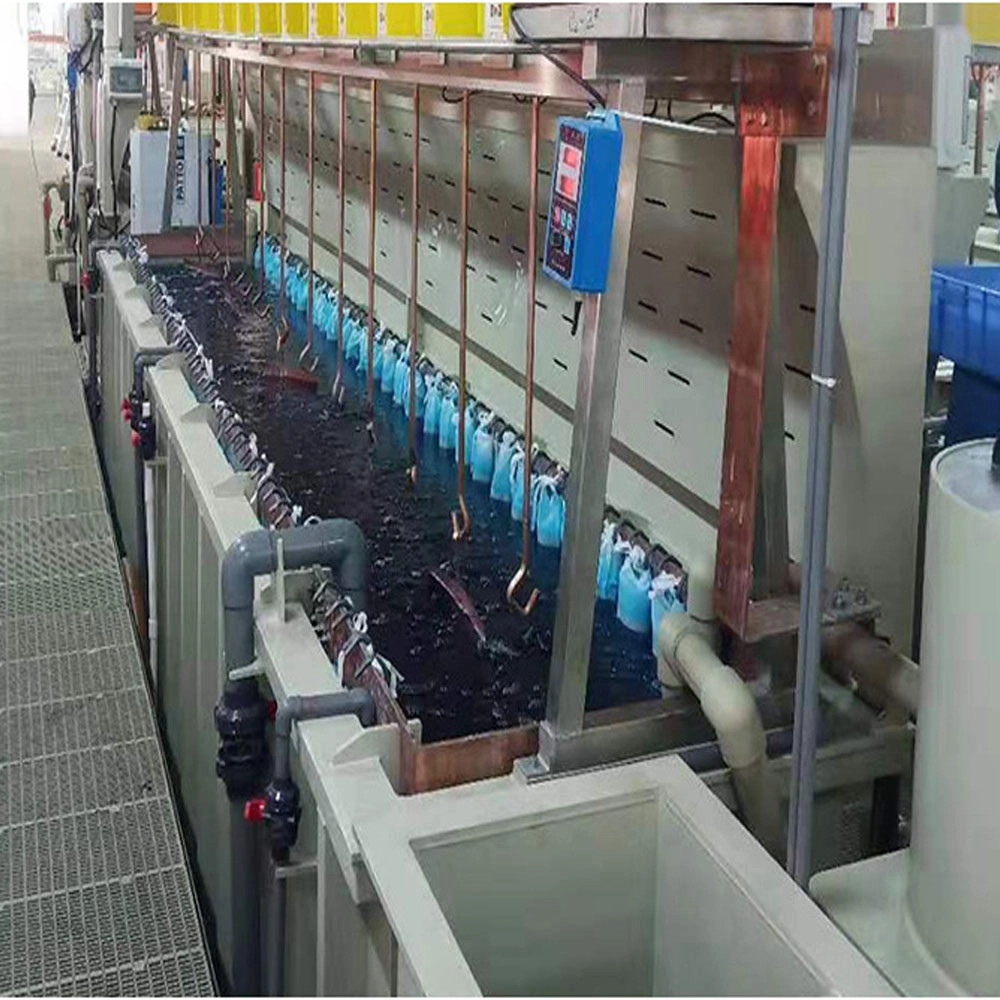
Rack tips are the smallest part of the line and the most ignored. A dirty tip or a worn spring marks parts and starves the deposit at the same time.
This junior guide is the contact and tip care routine: cleaning, spring replacement, tip dressing and the preventive schedule that keeps contacts honest.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Tips never cleaned | Contact marks and thin spots | Clean per schedule |
| 2. Worn springs used | Parts move or drop | Replace daily if worn |
| 3. Tip plating build-up | Insulating layer | Strip or dress per schedule |
| 4. Contact mark ignored | Batch repeats the fault | Stop, fix, log |
| 5. All tips cleaned the same | Different racks, different needs | Schedule per rack type |
| 6. Rack repair skipped | Faults compound | Repair at the log point |
| 7. No tip log | Patterns invisible | Per-rack-type log |
| 8. Cleaning chemical wrong | Tip damage | Use the specified cleaner |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Clean tips per shift or per rack-count rule
- Check springs daily and replace worn ones
- Dress or strip tips on schedule
- Stop immediately on any contact mark
- Keep a per-rack-type care log
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Tip care flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Contact marks are the alarm for tip care.
- A test rack proves a repaired rack.
- Use only the specified tip cleaner.
- Strip chemicals need PPE and extraction.
Working Data & Formula Notes
Tip care data
Reference schedule for rack contact care.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Tip clean | Per shift or 3 racks | Dirty tips mark parts |
| Spring check | Daily | Worn springs drop parts |
| Tip dress | Per rack-type schedule | Build-up insulates |
| Test rack | After repair | Proves the fix |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Contact care schedule
| Rack type | Clean | Springs | Dress |
| Standard | Per 3 racks | Daily | Weekly |
| High-current | Per shift | Daily | Weekly |
| Fine tips | Per shift | Daily | Per usage |
Implementation Cases
Case 1 - a contact mark that followed one rack type
Situation. Contact marks appeared only on parts from rack type B; the tip log showed type B tips were not being cleaned on the night shift.
Approach. The cleaning schedule was tied to rack count for all shifts, and a stop-and-log rule was added for contact marks.
Outcome. Contact marks stopped; the log proved the pattern and the fix.
Case 2 - build-up that acted as an insulator
Situation. A rack slowly plated thinner each week until parts failed; tips had heavy deposit build-up that blocked current.
Approach. Tips were stripped and dressed, and a weekly dress point was added to the rack-type schedule.
Outcome. Deposit returned to target; the weekly dress became a fixed task.
Frequently Asked Questions
Why do tips matter so much?
The tip is the electrical contact for the part; a bad tip starves or marks the deposit.
How often clean tips?
Per shift or per three racks depending on current and part type.
What causes contact marks?
Dirty, worn or loose tips that concentrate current at the touch point.
Why replace springs daily?
Worn springs let parts move and mark; daily checking is cheap.
What is tip dressing?
Cleaning and reshaping the tip face so it contacts the part cleanly.
Why strip build-up?
Plated build-up insulates the tip and slowly starves the deposit.
What do I do on a contact mark?
Stop, find the rack, fix the tip and log it before running more parts.
Why per-rack-type schedules?
Racks carry different currents and part types; one schedule misses the differences.
What is a test rack?
A small load run after repair to prove the rack contacts correctly again.
What Would You Like to Solve?
Tell us your rack types, currents and contact-mark pattern. We can build the tip-care schedule and the per-rack log for your line.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Rack Contact and Tip Care: The Junior Routine That Prevents Contact Ma
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.