
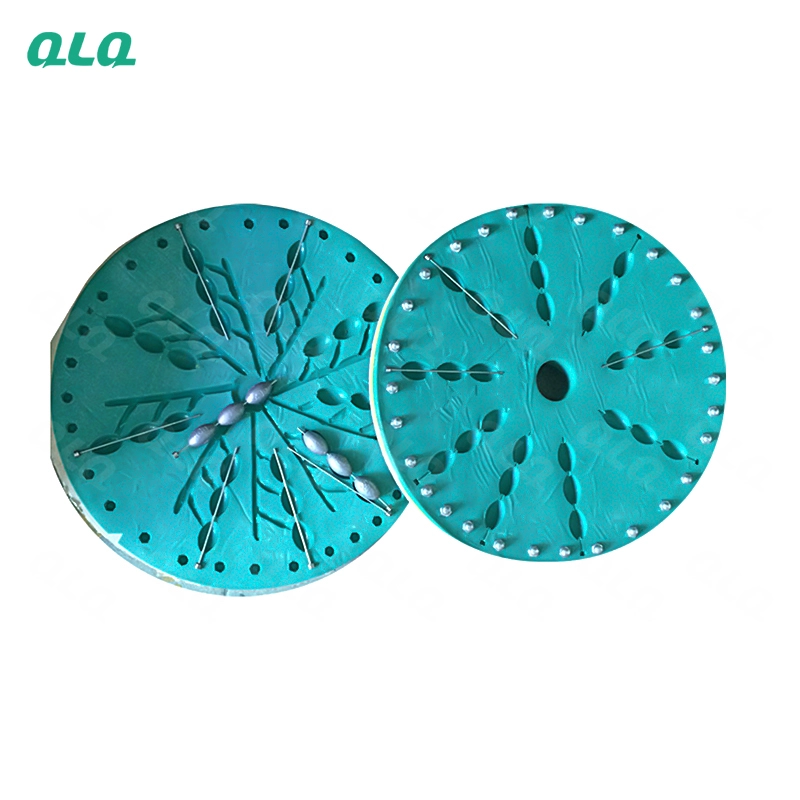
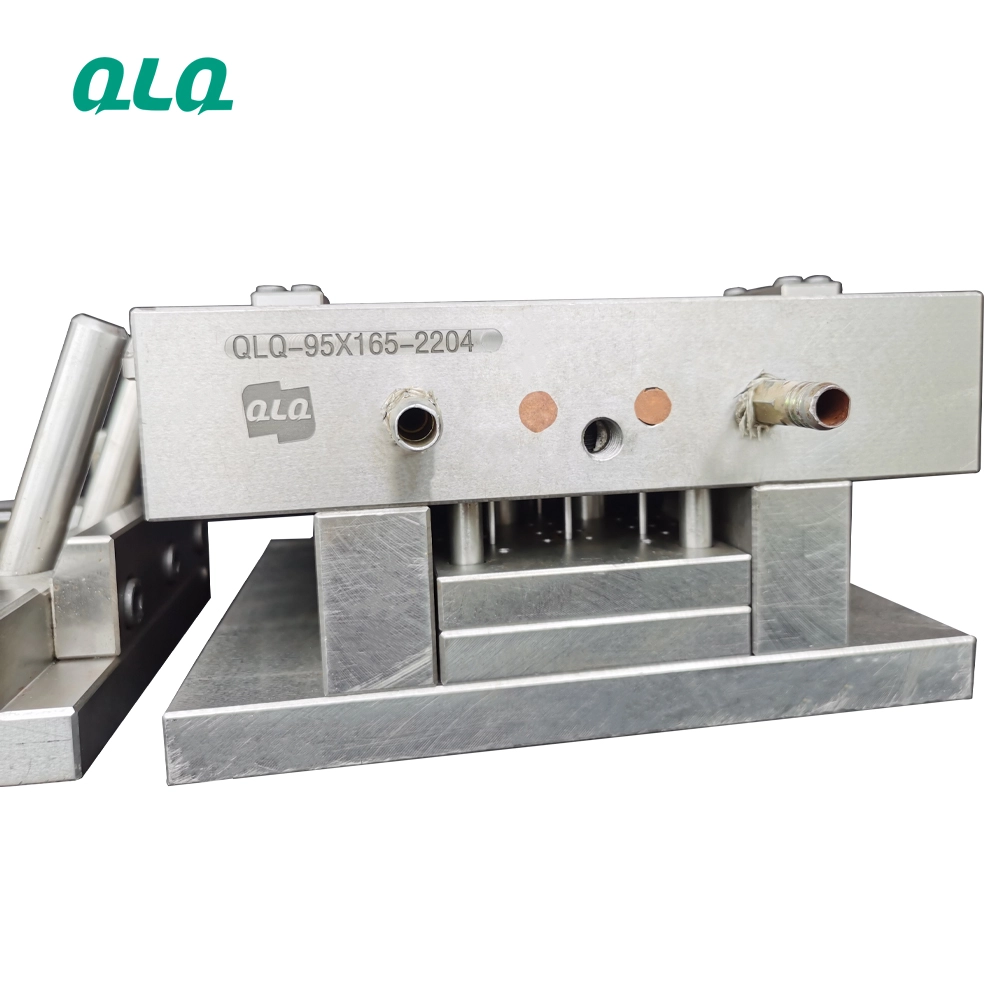
A mould is the most expensive tool on the line, and it fails on a shot-count schedule if it is tracked. The senior skill is deciding repair versus refurbish before the tool prints a bad batch.
This guide covers shot thresholds, refurbish decisions and the toolroom gate that protects the asset.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No shot count | Wear surprises | Log shots per mould |
| 2. Refurbish too late | Tool past saving | Act at the threshold |
| 3. Welding without heat control | Soft spots | Qualified toolroom |
| 4. Hardness never checked | Erosion hidden | Spot check |
| 5. Repairs ungated | Bad moulds run | First-article gate |
| 6. One expert owns the tool | Absence stops | Cross-train |
| 7. No spare strategy | Stops stretch | Plan by risk |
| 8. History lost | Same fix repeats | Mould card |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Track shots per mould
- Refurbish at the threshold
- Qualified toolroom only
- Gate every repair
- Keep the mould card
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Mould life flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Shot count turns maintenance into a plan.
- The mould card is the tool memory.
- Toolroom work needs qualified staff.
- Heavy moulds need safe handling.
Working Data & Formula Notes
Working data - mould thresholds
Reference values for zinc die-casting moulds.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Gate thickness | 0.8-1.2 mm | Below the window = refurbish. |
| Cavity hardness | HRC 46-52 | Soft spots erode fast. |
| Shot threshold | Per mould history | Maintenance trigger. |
| Cooling flow | All channels | Scale blocks heat removal. |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Decision table
| Gate erosion | Refurbish gate | Measure and re-machine |
| Soft cavity | Re-nitride or replace | Hardness first |
| Cracked insert | Replace | Qualified toolroom |
| Baked release | Clean and re-polish | Per schedule |
Implementation Cases
Case 1 - a shot threshold that saved the tool
Situation. A gate was caught at the shot threshold before flow marks appeared.
Approach. Planned refurbishment ran in maintenance time.
Outcome. No bad batch, and the tool was saved early.
Case 2 - a weld that failed twice
Situation. The same cavity was welded twice and failed fast.
Approach. Hardness showed soft spots from uncontrolled heat; the insert was re-nitrided.
Outcome. The repair lasted, and hardness became a repair gate.
Frequently Asked Questions
Why track shots?
Shot count is the maintenance trigger; without it wear surprises.
When should I refurbish?
At the threshold - gate below 0.8 mm, hardness loss or cooling failure.
Why qualified toolroom?
Uncontrolled heat creates soft spots that erode fast.
What is the repair gate?
First articles after every repair before production.
Why plan spares?
High-risk moulds with spares keep stops to minutes.
How do I keep history?
The mould card: shots, measurements, repairs, thresholds.
Why check hardness?
Soft spots print into parts and erode quickly.
How do I avoid single-expert risk?
Document methods and cross-train the toolroom.
What Would You Like to Solve?
Track the shots, measure at the threshold, decide with evidence and gate every repair. Mould life is managed, not hoped for.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Die-Casting Mould Life Management: Shot Thresholds, Refurbish Decision
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.