
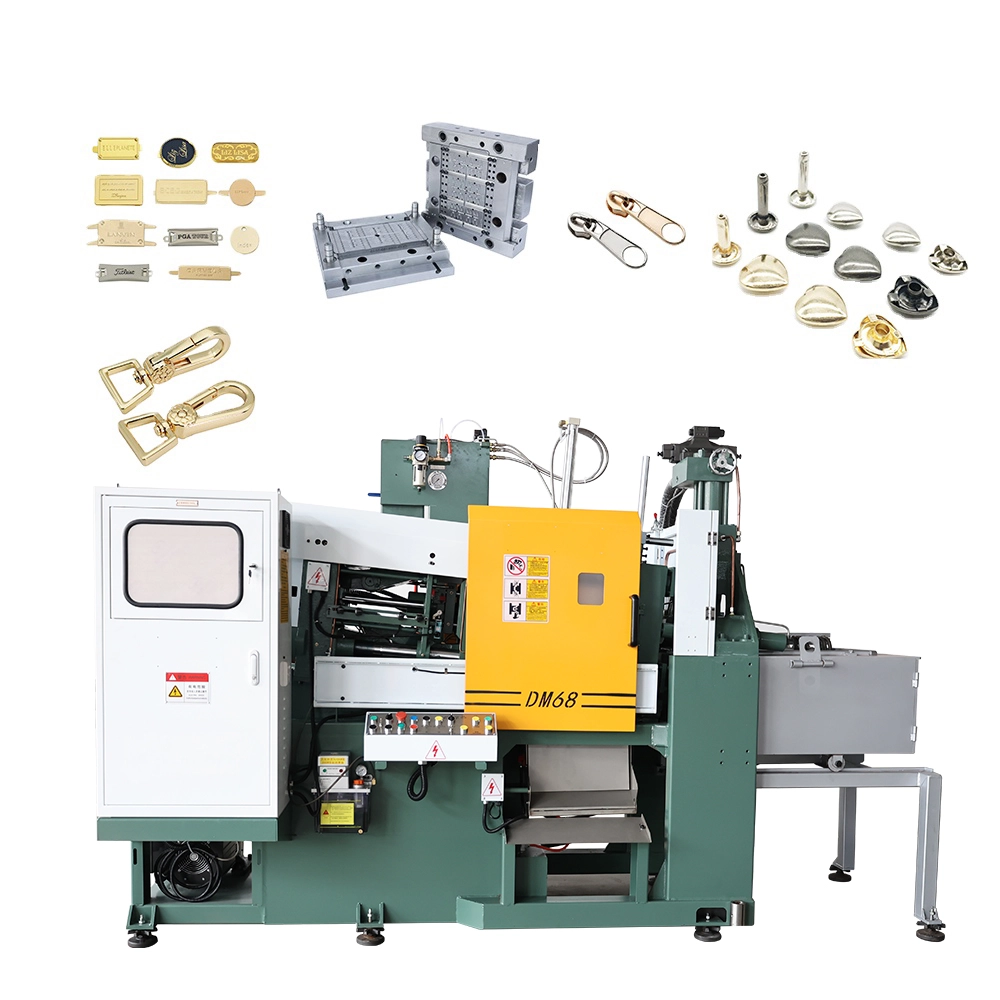
Cold shuts and flow marks both live in the fill, but they are different fingerprints: cold shuts follow a cold mould, flow marks follow a worn gate or blocked vent. Read the location and fix the cause.
This guide is the intermediate method for locating and fixing cold shuts and flow marks.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Raising pressure for cold shuts | Flash without fill | Heat the mould and melt |
| 2. Polishing flow marks away | The cause remains | Measure the gate |
| 3. Vents assumed clear | Gas lines appear | Clean and check depth |
| 4. Gate measured once | Wear returns | Measure at maintenance |
| 5. Cold melt at shot | Shuts appear | Probe the melt at shot |
| 6. No location map | Cause unclear | Map defect location |
| 7. Two variables changed | Cause hidden | One change, one batch |
| 8. No first-article gate | Faults run | Gate after each fix |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Heat the mould before tuning the shot
- Measure the gate at maintenance
- Clean vents per run
- Map defect locations
- One change, one batch
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Cold shut / flow mark flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Cold shuts follow cold metal; flow marks follow worn geometry.
- A location map turns a mystery into a check.
- Hot mould work needs proper tools.
- Vent cleaning needs care not to deepen past spec.
Working Data & Formula Notes
Working data - fill defect controls
Reference windows for cold shuts and flow marks.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Mould temp | 180-220 C | Cold shuts below the window. |
| Melt at shot | 420-450 C | Cold melt = incomplete fill. |
| Gate thickness | 0.8-1.2 mm | Erosion = flow marks. |
| Vent depth | Per design | Blocked = gas lines. |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Location to cause
| Cold shut at thin edges | Mould cold | Raise mould temp |
| Cold shut at the end of fill | Melt cold or shot slow | Check melt and fill phase |
| Flow marks on one face | Gate wear | Measure and refurbish |
| Gas lines near vents | Vents blocked | Clean vents |
Implementation Cases
Case 1 - cold shuts that ignored pressure
Situation. A buckle line raised pressure to clear cold shuts and gained flash instead.
Approach. The mould was below 170 C; it was stabilised at 200 C and pressure returned to normal.
Outcome. Cold shuts cleared without flash.
Case 2 - flow marks that followed gate wear
Situation. Flow marks appeared on one face after a high shot count.
Approach. Gate measurement showed erosion; the gate was refurbished.
Outcome. Flow marks stopped, and gate measurement joined maintenance.
Frequently Asked Questions
Why do cold shuts ignore pressure?
Pressure cannot fill metal that has already frozen. Heat the mould and melt first.
What causes flow marks?
Gate erosion or blocked vents change the fill pattern. Measure and clean.
How do I read the location?
Cold shuts at thin edges point at mould temperature; at fill end point at melt/shot; flow marks on one face point at the gate.
Why measure the gate?
Erosion changes fill velocity and prints flow marks.
How often clean vents?
Per run or per shot-count schedule; blocked vents trap gas.
Should I change mould and shot together?
No - one variable, one batch.
What is the proof?
First articles after the single change.
When do I call the toolroom?
When gate erosion or mould temperature control needs repair.
What Would You Like to Solve?
Read the location, heat or clean first, measure the gate and prove with one change. Cold shuts and flow marks both surrender to the right fix.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Cold Shuts and Flow Marks on Zinc Die-Castings: Mould Temperature, Gat
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.