
Two painters shared one cold paint booth and produced two different finishes: one ran at 55-60 units of 60° gloss, the other at 75-80, and rework sat at 9 percent. The paint and the booth were identical; the working standards were not.
This case study shows the governance that closed the gap: one written standard per product, a first-piece gate every shift, instrument checks on gloss, color and film, and a 15-minute daily booth audit. Rework fell to 2 percent within a month.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No written standard | Each painter's habit becomes the spec | Publish one standard per product with photos |
| 2. Viscosity not logged | Same paint, different results | Log Ford cup 4 per batch |
| 3. No first-piece gate | A bad start runs all shift | Approve the first piece every shift |
| 4. Gloss judged by eye | Visual judgment drifts | Measure with a 60° gloss meter |
| 5. Color checked under one light | Metamerism starts disputes | Use a standard light box |
| 6. Training by word of mouth | Each version of the method spreads | Documented training with practical tests |
| 7. Guns not maintained | Atomization differs between painters | Check nozzles per shift |
| 8. Rejects not attributed | Painter variance stays invisible | Log the painter per batch |
| 9. Audit skipped when busy | Standards decay quietly | Run the 15-minute audit daily |
Best Practices
- Write one standard per product with photos
- Log viscosity, film and painter per batch
- Approve the first piece each shift
- Measure gloss and color with instruments
- Train painters against the written standard
- Audit the booth daily for 15 minutes
Implementation Roadmap
| Step | Frequency |
|---|---|
| Publish the product standard | Per product |
| Approve the first piece | Per shift |
| Instrument checks | Per batch |
| Booth audit | Daily |
| Review painter variance | Weekly |
Unified finish governance flow
- Standard - One written spec per product. (Verbal standards multiply.)
- Gate - First piece each shift. (A bad start runs all shift.)
- Measure - Gloss, color, film thickness. (Eyes drift; instruments hold.)
- Audit - 15 minutes every day. (Skipped audits decay standards.)
Painter variance is a management problem with a measurement answer. | The first piece of the shift decides the whole shift.
Finish quality governance data
Reference values for cold paint line quality gates.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Gloss tolerance | 60° gloss ±5 units | Wider spread means setup drift |
| Color tolerance | ΔE below 1.5 | Above 1.5 fails the standard panel |
| Film thickness | Per product 25-40 µm | Thickness bands per product spec |
| Viscosity | Ford 4 per product window | Same paint needs same viscosity |
| Rework target | Below 3% | Above 5% needs a cause review |
| First-piece gate | Per shift and product change | Catches setup drift early |
| Audit frequency | 15 min daily | Weekly audits decay faster |
Finish quality gates
| Gate | Instrument | Tolerance |
|---|---|---|
| Gloss | 60° gloss meter | ±5 units |
| Color | Spectrophotometer | ΔE below 1.5 |
| Film | Film thickness gauge | Per product band |
| Viscosity | Ford cup 4 | Per product window |
Painter variance board
| Field | Content | Owner |
|---|---|---|
| Batch | Product, painter, shift | Operator |
| Gloss | Measured value | Inspector |
| Color | ΔE vs standard | Inspector |
| Rework | Cause-classified | Supervisor |
Case 1 - two painters, two finishes on one booth in Vietnam
Scenario. Two painters shared a cold paint booth in Vietnam and produced gloss readings of 55-60 and 75-80 on the same product; rework ran at 9 percent and each painter blamed the other's technique.
Action. The plant wrote one standard per product with photos, added a first-piece approval every shift, and started measuring gloss, color and film on every batch with instruments.
Result. Rework fell to 2 percent within a month, and the gloss spread closed to within 5 units of the product standard.
Case 2 - color drift across rotating shifts in Indonesia
Scenario. A cold paint line in Indonesia ran three rotating shifts on the same products, and color drifted between shifts so far that customers rejected mixed-lot deliveries.
Action. Each shift approved a first piece against the standard panel under a light box, viscosity and film were logged per batch, and a 15-minute booth audit ran daily with instrument checks.
Result. Color difference stayed below ΔE 1.5 across shifts within three weeks, and mixed-lot complaints stopped.
Frequently Asked Questions
Why do two painters produce different finishes?
Without a written standard, each painter's habit becomes the specification.
How do I unify quality?
One standard per product, first-piece gates and instrument checks on every batch.
What gloss tolerance?
60° gloss within ±5 units of the product standard.
What color tolerance?
ΔE below 1.5 against the approved standard panel.
Why measure instead of look?
Eyes adapt to drift; instruments hold the line stable.
What goes in the daily audit?
Booth condition, viscosity log, first-piece sign-off and gun nozzles.
How to train new painters?
Against the written standard with a practical test, not word of mouth.
How to attribute rejects?
Log the painter, batch and product on every reject.
What rework target?
Below 3 percent with the gates in place.
How to keep standards from decaying?
The daily 15-minute audit and the weekly variance review.
What Would You Like to Solve?
Describe the painter count, product mix and measured finish differences; a technical review can set the gates and audit routine.
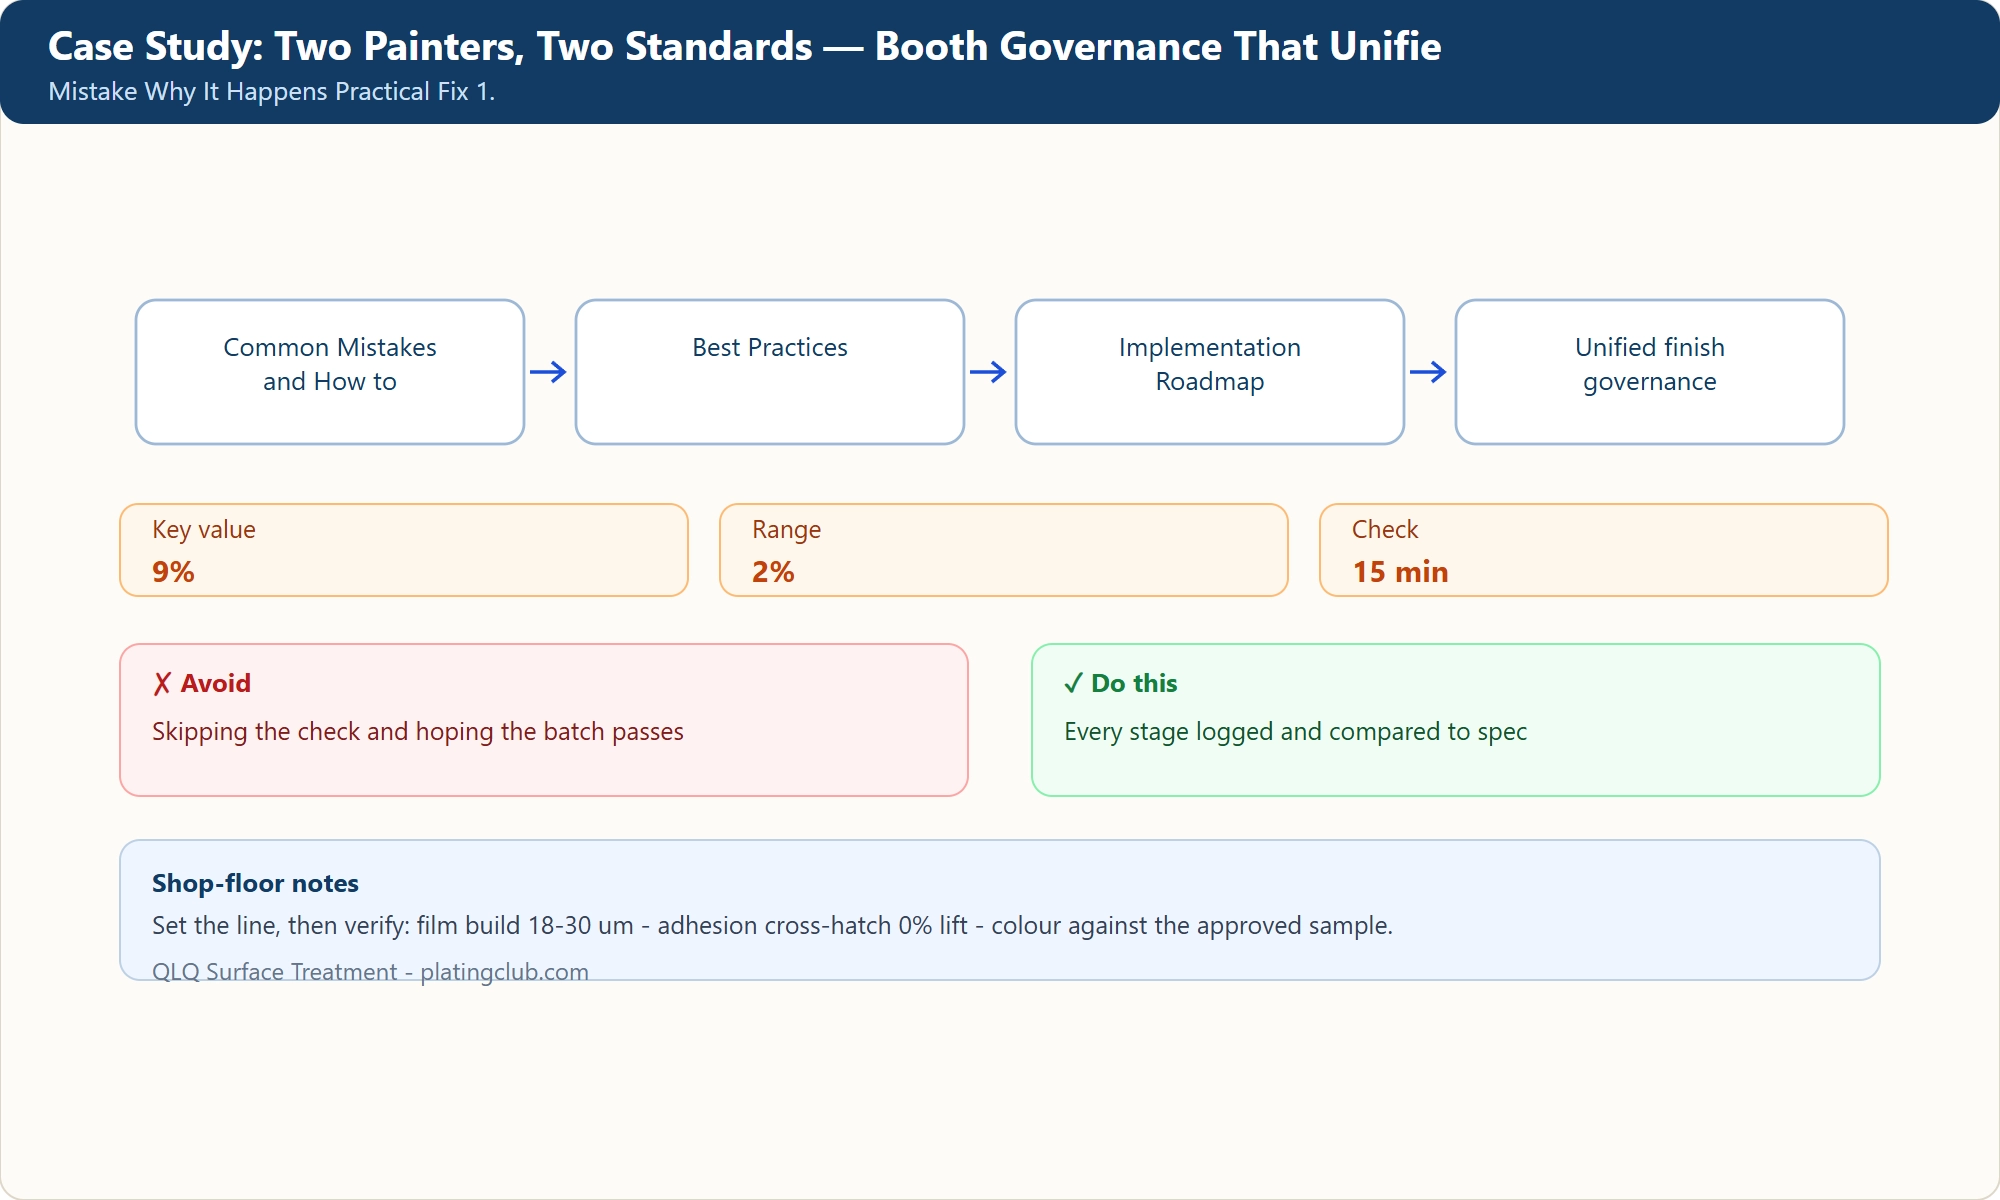
Quick reference - what to check and why
| Stage | What it means on the line |
|---|---|
| Common Mistakes and How to Avoid Them | Mistake Why It Happens Practical Fix 1. |
| Best Practices | Write one standard per product with photos Log viscosity, film and painter per batch Approve the first piece each shift Measure gloss and color with instruments Train painters against the wr |
| Implementation Roadmap | Step Frequency Publish the product standard Per product Approve the first piece Per shift Instrument checks Per batch Booth audit Daily Review painter variance Weekly |
| Unified finish governance flow | Standard - One written spec per product. |
| Finish quality governance data | Reference values for cold paint line quality gates. |
| Finish quality gates | Gate Instrument Tolerance Gloss 60° gloss meter ±5 units Color Spectrophotometer ΔE below 1.5 Film Film thickness gauge Per product band Viscosity Ford cup 4 Per product window |
FAQ - Case Study: Two Painters, Two Standards — Booth Governance That Unifie
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.