
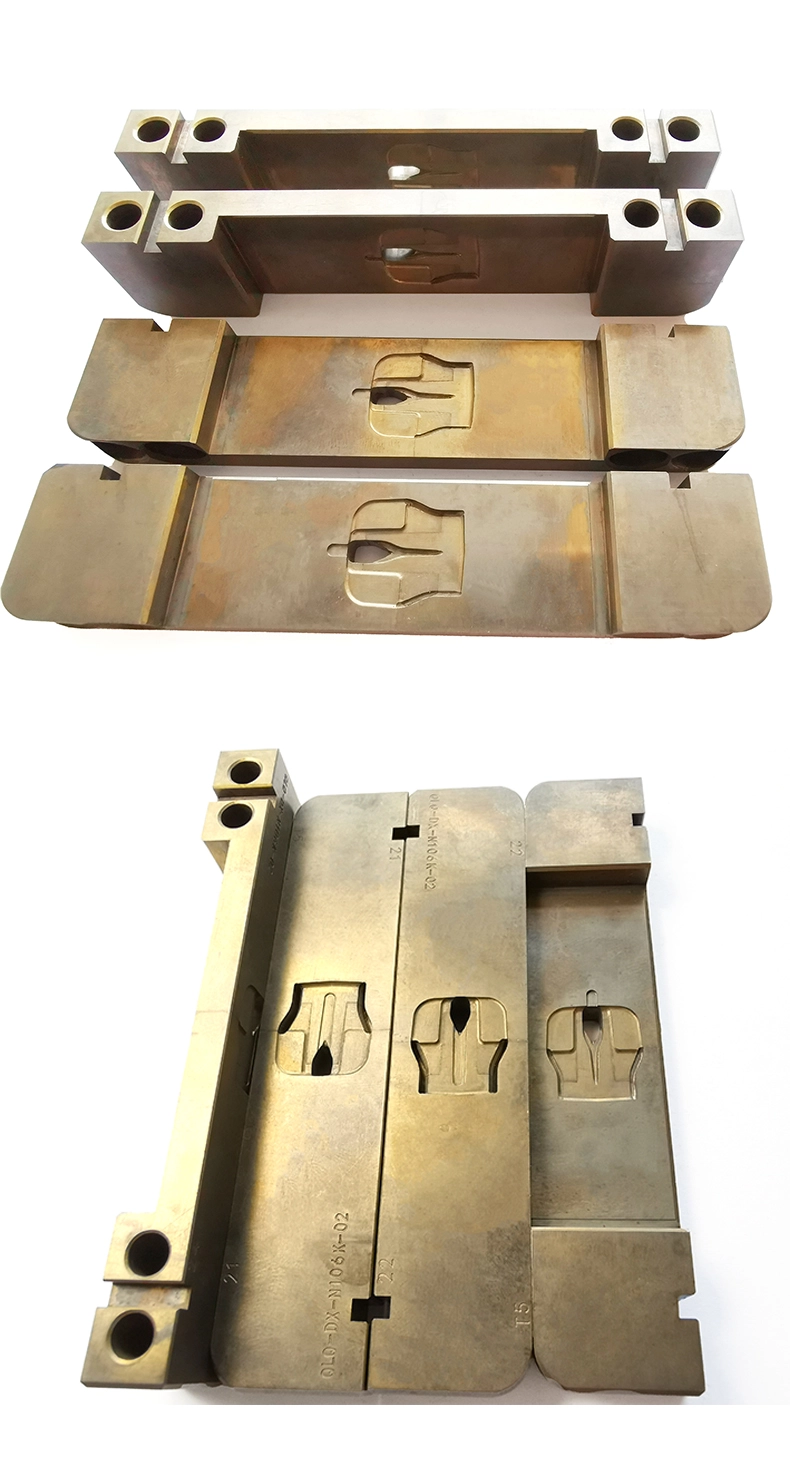
Forty racks sat in the rebuild queue for four weeks while the line ran short of racks every afternoon, and daily downtime from rack failures kept climbing. The rebuild time averaged two to three days per rack with no inspection gate to catch faults early.
The backlog was cleared in three weeks by a shift-level inspection gate, a standardized spare kit and an eight-hour rebuild target. This case study covers the gates, the standards and the rack log that cut rack-related downtime by 60 percent.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No inspection gate | Faults found on line, cost a batch | Check tips, springs, spacing per shift |
| 2. Spares not standardized | Five spring types, three tip designs | Standardize to two types, one profile |
| 3. Rebuild by feel | Two to three days per rack | Set an 8-hour target and parts kit |
| 4. No rack cycle log | Replacement planned by guess | Log cycles per rack type |
| 5. Racks run to failure | Batch lost before repair | Pull racks at gate, not on failure |
| 6. Backlog invisible | Queue grows without notice | Review backlog weekly |
| 7. Inventory mismatched | Overstock ties cash, gaps stop line | Hold 1.3-1.5× peak daily need |
| 8. Rebuild quality unchecked | Same fault returns | Test-load every rebuilt rack |
| 9. No spare ownership | Kits empty at the wrong moment | Assign one owner per station |
Best Practices
- Run a shift-level inspection gate before loading
- Standardize spares to two spring types and one tip profile
- Set an eight-hour rebuild target with a pre-packed kit
- Log cycles per rack and pull racks at the gate
- Test-load every rebuilt rack before release
- Review the backlog and downtime weekly
Implementation Roadmap
| Step | Frequency |
|---|---|
| Inspect racks at the gate | Per shift |
| Log rack cycles | Per rack, per day |
| Rebuild with standard kit | Per rack, 8-hour target |
| Test-load rebuilt racks | Per rebuild |
| Review backlog and downtime | Weekly |
Rack availability flow
- Gate - Shift-level inspection before loading. (Faults found on line cost a batch.)
- Standardize - Two spring types, one tip profile. (Five types double the stock and the confusion.)
- Rebuild - Eight-hour target with a packed kit. (By-feel rebuilds take days.)
- Release - Test-load every rebuilt rack. (Unverified rebuilds repeat the fault.)
Racks are production tooling; treat them like machines with cycle counts. | An inspection gate catches faults for minutes instead of batches.
Rack management data
Reference values for rack inventory and rebuild planning.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Rack inventory | 1.3-1.5× peak daily need | Overstock ties cash, gaps stop line |
| Inspection gate | Per shift before loading | Faults caught for minutes, not batches |
| Rebuild time | 8 hours per rack target | 2-3 days builds backlog |
| Spare standardization | 2 spring types, 1 tip profile | Fewer types, lower stock |
| Cycle log | Per rack, per day | No count, no plan |
| Test load | Every rebuilt rack | Proves the repair |
| Downtime target | Below 2% of run time | Racks are a process input |
Inspection gate card
| Check | Frequency | Pull condition |
|---|---|---|
| Tip condition | Per shift | Wear groove or ridge |
| Spring tension | Per shift | Loose or crushed |
| Spacing | Per shift | Bent or touching |
| Coating | Weekly | Flaking or worn |
Rebuild standard kit
| Item | Standard | Quantity |
|---|---|---|
| Spring type A | Small parts | Per rack |
| Spring type B | Heavy parts | Per rack |
| Tip profile | Single standard | Per rack |
| Insulation | Frame coating | Per rack |
Case 1 - a 40-rack backlog cleared in three weeks
Scenario. A rack line carried a 40-rack rebuild backlog four weeks deep while daily rack failures caused afternoon downtime, and rebuilds averaged two to three days each because every rack was treated as unique.
Action. A shift inspection gate was introduced to pull racks before failure, spares were standardized to two spring types and one tip profile, rebuilds got an eight-hour target with a packed kit, and every rebuilt rack was test-loaded.
Result. The backlog cleared in three weeks, rack-related downtime fell 60 percent, and rack life extended 30 percent as faults were caught early instead of run to failure.
Case 2 - rack inventory cut 40 percent in Thailand
Scenario. A plant in Thailand held racks for every part variant and still ran short at peaks, because spare parts were not interchangeable across rack types.
Action. Rack types were consolidated, spares standardized, and inventory set at 1.4 times peak daily need with a weekly review.
Result. Rack inventory dropped 40 percent, peak shortages ended, and the weekly review became the standing agenda item.
Frequently Asked Questions
Why do racks fail on the line?
No inspection gate means faults are found at the worst moment, during loading or plating.
What should the gate check?
Tips, springs, spacing and coating condition, every shift, before racks are loaded.
How long should a rebuild take?
Eight hours per rack with a pre-packed standard kit; two to three days means no system.
Why standardize spares?
Fewer spring and tip types mean lower stock, faster rebuilds and fewer loading errors.
How much rack inventory do I need?
About 1.3-1.5 times peak daily need; more ties up cash, less stops the line.
Why log cycles per rack?
Cycle counts turn replacement from a guess into a schedule and extend rack life.
Should rebuilt racks be test-loaded?
Always - a test load proves the repair before the rack returns to production.
How do I measure the fix?
Track backlog depth, rack downtime share and rebuild time weekly.
What is a healthy downtime share?
Below 2 percent of run time from racks; above that the gate or the spares need work.
What Would You Like to Solve?
Tell us your rack count, part variants and rebuild workload, and we can help design the inspection gate and spare standards for your line.
FAQ - Case Study: Rack Rebuild Backlog Cleared — Inspection Gates and Spare
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.