
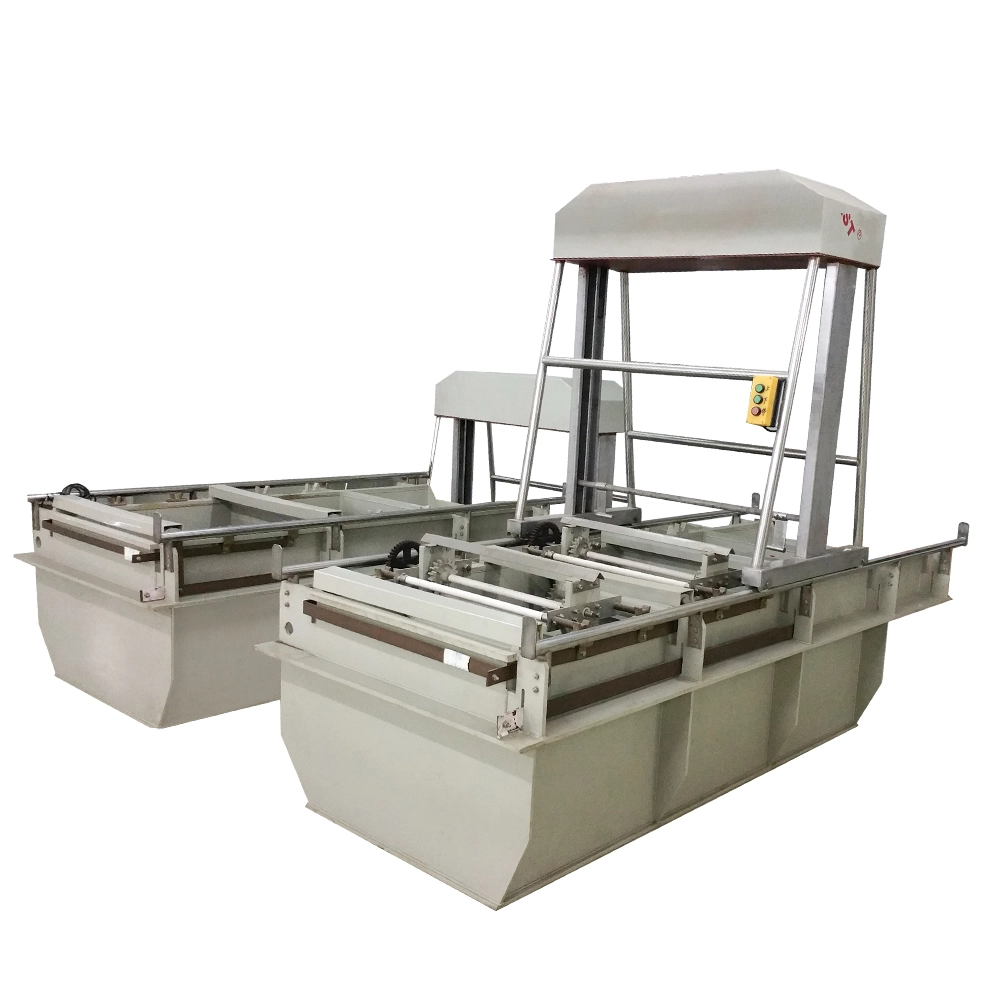
A barrel department is run on ampere-hours: the meter, the dosing, the Hull cell and the yield that follows. Managers who govern the bath by Ah data and build a trained team keep the barrel line stable through load changes and shift changes.
This guide is for barrel plating managers: bath governance, yield KPIs, training and the shift gates that keep the line predictable.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Barrel speed fixed | Tumbling marks | Set per product |
| 2. Hangers unmaintained | Current loss | Clean per schedule |
| 3. No surface-area record | Current drifts | Log per load |
| 4. Anode bags overdue | Sludge roughens | Inspect weekly |
| 5. Unload splashing | Stains and damage | Handle carefully |
| 6. No first-article gate | Errors repeat | Gate every load |
| 7. Managing by memory | Drift unseen | Run KPI and trend reviews |
| 8. Single-expert dependency | Absence stops the line | Cross-train and document |
| 9. Gates not enforced | Faults escape | Audit the gates |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Maintain hangers
- Log surface area per load
- Inspect anode bags weekly
- Gate every load
- Run KPI reviews
- Build a cross-trained team
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Barrel management flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Ah history is the department memory.
- Cross-trained baths survive holidays.
- Safety gates apply to managers too.
- Never push a failed Hull cell to output.
Working Data & Formula Notes
Working data - barrel management KPIs
Reference KPIs for a barrel plating department.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Yield | First-pass per batch | The honest department number. |
| Ah per batch | Per product family | Basis for dosing and cost. |
| Rework rate | Per thousand parts | Tracks skill and drift. |
| Consumables cost | Per thousand parts | Anodes, bags, brightener. |
| Training coverage | Percent on ladder | Capability insurance. |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Management review
| Yield and Ah | Weekly | Per product family |
| Hull cell gate compliance | Weekly | Shift starts |
| Rework by shift | Weekly | Shared data |
| Seasonal trend | Quarterly | Water and temperature |
| Training progress | Monthly | Ladder completion |
Implementation Cases
Case 1 - yield that followed Ah governance
Situation. A barrel line had unstable yield and constant brightener overuse.
Approach. The manager moved the line to Ah-based dosing with a Hull cell gate per shift.
Outcome. Yield stabilised and chemical cost dropped.
Case 2 - cross-training through a holiday
Situation. The only bath expert went on leave and quality drifted.
Approach. Documented bath cards and two trained intermediates held the windows.
Outcome. The line stayed stable, and the dependency was gone.
Frequently Asked Questions
How do I manage a barrel department?
Govern by Ah data: dosing, yield and cost follow the meter. Gate shifts with a Hull cell and first articles.
Why is Ah governance central?
Barrel work is load-driven. Calendar dosing cannot follow the load; Ah dosing can.
How do I gate a shift?
Hull cell at shift start and first-article inspection. Both shifts read the same numbers.
Should output beat yield?
No - track yield with output. Speed without yield is just rework.
How do I stop single-expert risk?
Document the baths and cross-train. If one person owns the chemistry, the line is one absence from drift.
What KPIs should I run?
Yield, Ah per batch, rework per thousand and consumables cost per thousand.
Why review seasonally?
Water and temperature drift with seasons. The quarterly review catches the drift before it becomes rejects.
How do I keep the gates real?
Audit them. A gate nobody audits becomes decoration.
What Would You Like to Solve?
Govern by the meter, gate the shifts, measure yield with output and build the ladder. The barrel department that runs on Ah data runs predictably.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Managing the Barrel Plating Department: Ampere-Hour Governance, Yield
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.