
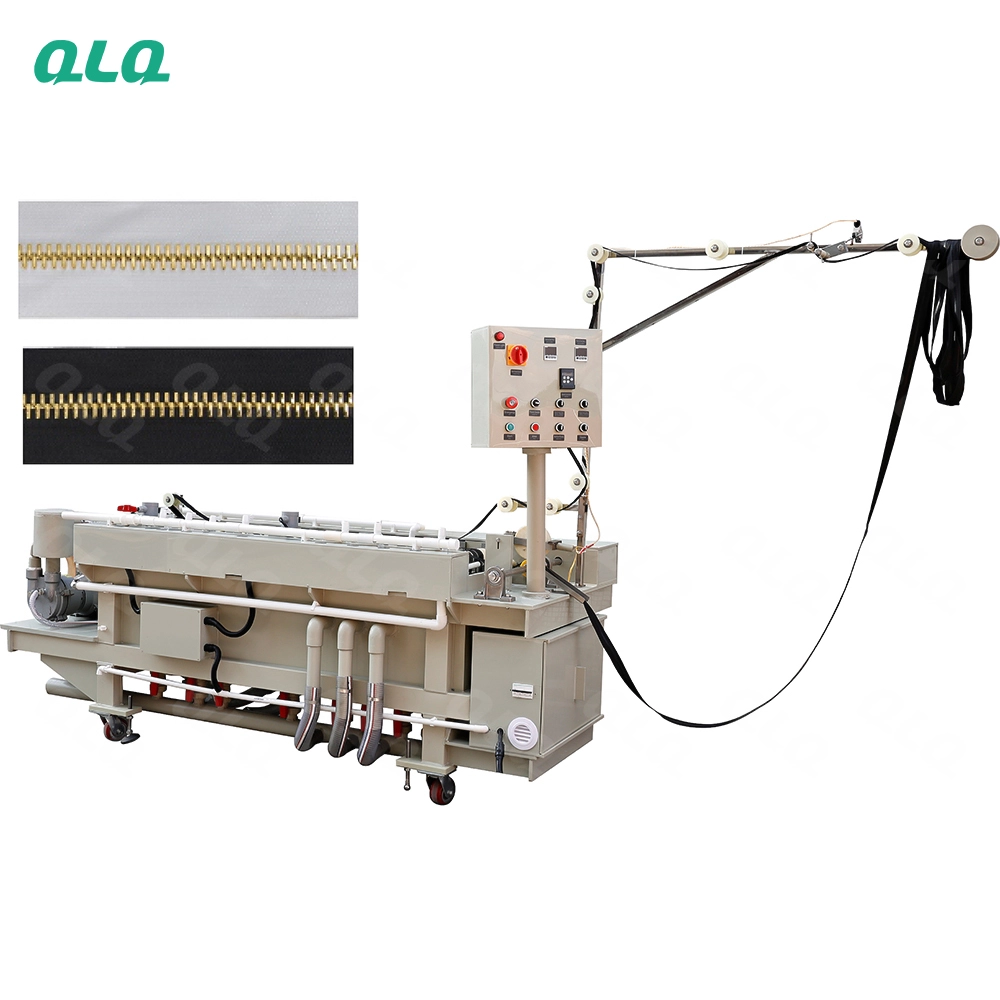
An anodizing department is managed on bath governance: trends, film gates and seal verification. Managers who run this keep film and colour stable.
This guide is for anodizing managers.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Agitation weak | Hot spots and milky film | Verify per shift |
| 2. Dye temperature drift | Shade shifts | Hold dye temperature |
| 3. Rack contact corrosion | Uneven film | Clean contacts |
| 4. Seal bath exhausted | Bleed returns | Titrate or replace |
| 5. No film map | Defects unlocated | Map the rack |
| 6. No retention sample | Disputes | Keep samples |
| 7. Managing by memory | Drift unseen | Run KPI and trend reviews |
| 8. Single-expert dependency | Absence stops the line | Cross-train and document |
| 9. Gates not enforced | Faults escape | Audit the gates |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Verify agitation
- Hold dye temperature
- Clean rack contacts
- Map film across the rack
- Run KPI reviews
- Build a cross-trained team
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Anodizing management flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Film is the anodize number.
- Seal gates prevent late failures.
- Acid safety applies to managers.
- Never pass a failed film gate.
Working Data & Formula Notes
Working data - anodizing KPIs
Reference KPIs for an anodizing department.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Yield | First-pass per batch | The department number. |
| Rework | Per thousand parts | Tracks drift and skill. |
| Chemical cost | Per thousand parts | Bath and dye waste. |
| Film compliance | Percent batches | Governance health. |
| Training coverage | Percent on ladder | Capability insurance. |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Management review
| Yield and rework | Weekly | By batch |
| Film compliance | Weekly | Per batch |
| Bath trends | Weekly | Acid and temperature |
| Seal gates | Weekly | Per batch |
| Training progress | Monthly | Ladder |
Implementation Cases
Case 1 - trends that ended a slow decline
Situation. Film quality declined for weeks.
Approach. Bath trends and film gates were enforced.
Outcome. Film stabilised.
Case 2 - cross-trained bath control
Situation. Only one technician set the bath.
Approach. Cards and two backups.
Outcome. The bath held through leave.
Frequently Asked Questions
How do I manage anodizing?
Trend the bath, gate film and seal, and measure yield with output.
Why bath trends?
Drift shows before rejects.
What are the gates?
Film, shade and seal.
How do I stop single-expert risk?
Cross-train.
What KPIs should I run?
Yield, rework, chemical cost and film compliance.
Why seal gates?
Late failures follow poor sealing.
Why profile the environment?
Seasons change the bath.
How do I keep gates real?
Audit them.
What Would You Like to Solve?
Trend the bath, gate the film and build the ladder. The anodize department that runs on data runs predictably.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.
FAQ - Managing Anodizing: Bath Governance, Film Yield and the Team Behind th
Straight answers from the shop floor. Ask us on WhatsApp if your case is different.