Professional Zinc Alloy Surface Finishing Solutions
Potassium Pyrophosphate
Potassium Pyrophosphate
Generează cod QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
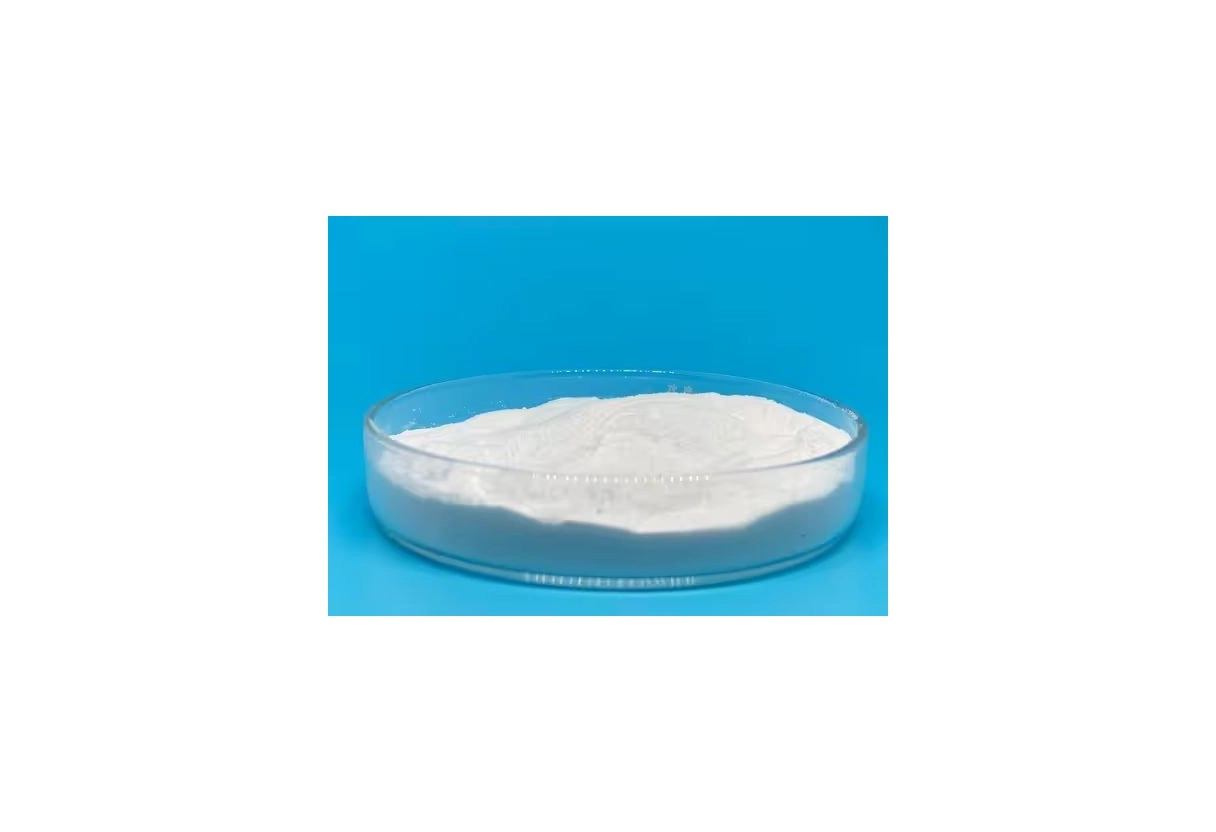
Potassium Pyrophosphate (K4P2O7, usually supplied as the trihydrate K4P2O7·3H2O) is the inorganic complexant that makes pyrophosphate copper plating work - the best-established cyanide-free alkaline copper system. It is a white, free-flowing hygroscopic powder or granular salt, freely soluble in water, and a 1% solution sits at pH 10.2-10.7. Its job in the bath is to hold copper ions in solution as stable pyrophosphate complexes at pH 8.0-8.8, where free cyanide chemistry is not needed and zinc die-castings are not attacked. In decorative lines for zipper sliders, belt buckles and small hardware on zinc alloy, pyrophosphate copper is the classic cyanide-free undercoat before bright nickel and chrome. Market grades differ mainly by end use: detergent / food-industry grades sold as cleaner builders, and plating-grade (technical) salt with tighter metal limits (Fe, heavy metals), lower chloride and a guaranteed pyrophosphate assay. Buying detergent-grade material to save money is false economy - its higher iron and orthophosphate load shortens bath life and dulls deposits.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
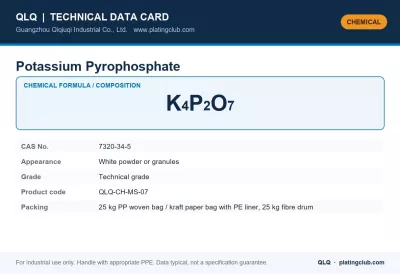
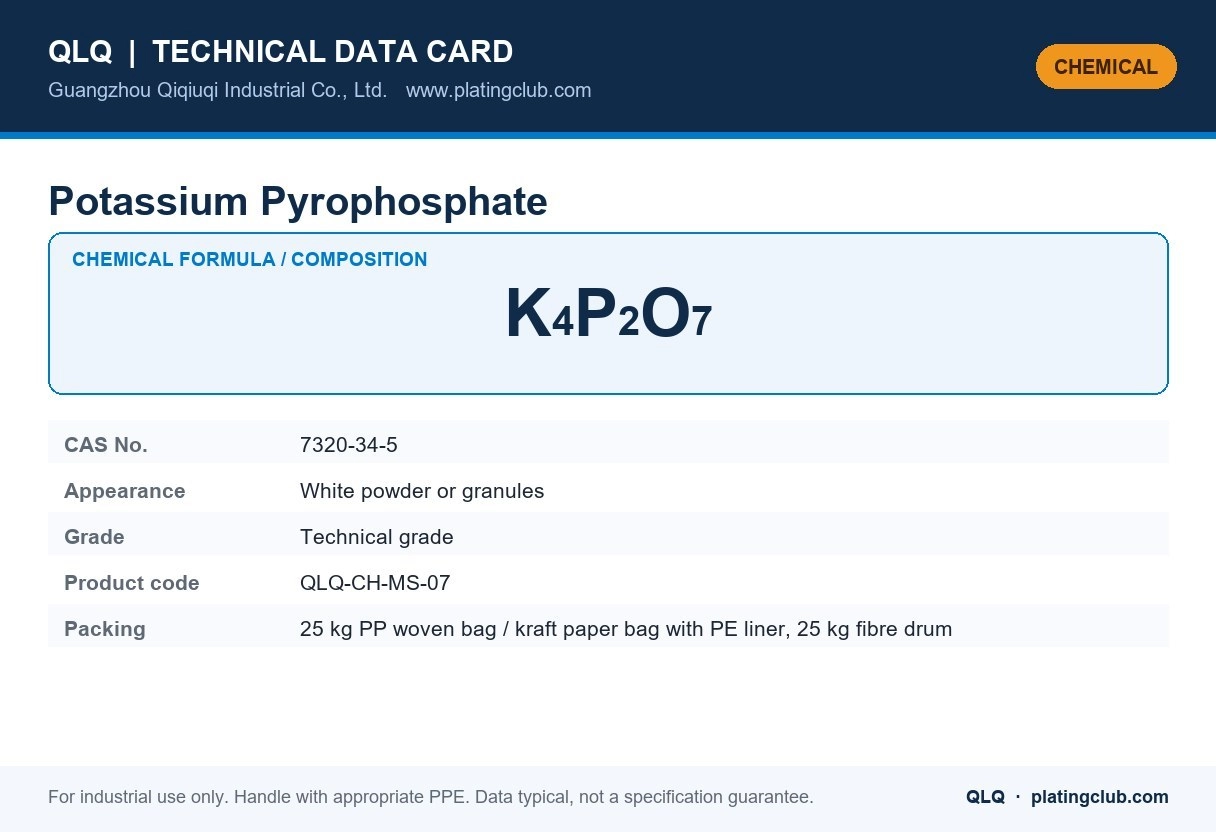
| Chemical name | Potassium Pyrophosphate |
| Chemical formula | K4P2O7 |
| CAS number | 7320-34-5 |
| Appearance | White powder or granules |
| Grade / type | Technical grade |
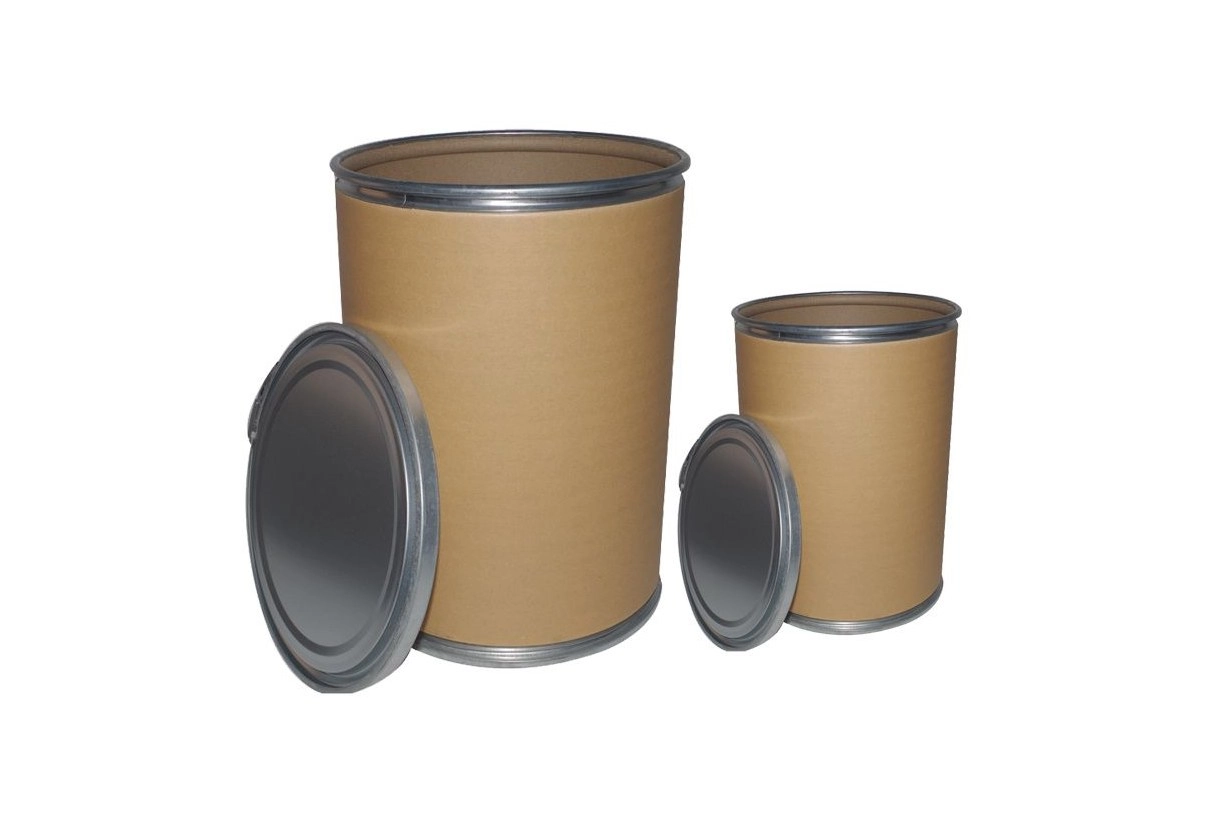
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Potassium pyrophosphate is the complexant that dissolves copper pyrophosphate and buffers the alkaline copper bath, and it is also used in the pyrophosphate tin and tin-copper baths.
- White powder with strong complexing power for copper, tin and iron; the P ratio (pyrophosphate to metal) is the key control parameter.
- It keeps the pH of the bath stable around 8.5-9.2 without a separate buffer.
- Iron accumulation is removed by precipitation and filtration during maintenance.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Copper pyrophosphate bath | 200-300 g/L, P ratio maintained at 7.0-7.5 |
| Tin pyrophosphate bath | 150-250 g/L |
| Analysis | Pyrophosphate by titration with standard copper solution |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Not classified as dangerous for transport in most cases; observe good industrial hygiene and dust control |
| Personal protective equipment | Dust mask, goggles and gloves for powder handling; general ventilation |
| Spill / first aid | Sweep up dry; material is a nuisance dust — avoid breathing the dust |
| Storage | Cool, dry, sealed store; keep bags closed, off the floor and away from moisture |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| How is the P ratio corrected? | Add copper pyrophosphate to lower the ratio or potassium pyrophosphate to raise it, then confirm by analysis. |
| Does it hydrolyse? | Slowly at high temperature, which is why the bath is normally run at 50-60 C and not higher. |
| Item | Typical Value |
|---|---|
| Chemical formula | K4P2O7 (anhydrous) / K4P2O7·3H2O |
| Assay | ≥ 96% (anhydrous basis, plating grade) |
| P2O5 content | ≈ 42-43% (anhydrous basis) |
| Appearance | White crystals/granules, free-flowing when sealed |
| Iron (Fe) | ≤ 0.002% |
| Chloride | ≤ 0.01% |
| Heavy metals (as Pb) | ≤ 0.001% |
| Water insoluble | ≤ 0.05% |
| pH (1% solution) | 10.2-10.7 |
| Standard packing | 25KG woven bag with PE inner liner |
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Color & form | Visual against retained sample | Uniform white; yellow or brown tint means iron contamination; lumps mean moisture ingress |
| Solubility / clarity | Dissolve 50 g in 100 ml DI water at 40°C | Clear solution in 5 min; no residue or surface film |
| Assay | COA (pyrophosphate titration) on every lot | ≥ 96%; reject lots below 95.5% |
| Orthophosphate in salt | Ammonium molybdate yellow test on a 5% solution | No heavy yellow precipitate at room temperature |
| Hull cell trial | 267 ml cell, add 10% new salt to your live copper bath, 2 A, 5 min | Bright range and limiting current unchanged; no edge burning or haze |
How QLQ controls it: every incoming lot is quarantined until the COA is matched against a retained reference and a Hull cell panel is run in a live pyrophosphate bath. Only lots that pass both checks are released, and the batch number is recorded so a defect can be traced back within one day. That discipline is why QLQ's cyanide-free copper lines hold their ratio and brightness for years without full dumps.
How It Works in the Bath (Pyrophosphate Copper)
Pyrophosphate (P2O74-) wraps each copper ion in a complex - roughly Cu(P2O7)26- - so copper stays dissolved at pH 8-9 without cyanide or strong chelating organics. The P2O7:Cu weight ratio is the master control: too low and copper hydrolyses out or plates rough at low current density; too high and current efficiency falls and the deposit loses brightness. Free ammonia and nitrate are deliberate additions that help the anode dissolve and widen the bright current-density window. The bath is run warm, filtered continuously, and replenished by analysis, not by habit.
| Component | Rack / General Purpose | Barrel Work (small parts) |
|---|---|---|
| Copper metal (from copper pyrophosphate Cu2P2O7) | 22-30 g/L | 15-22 g/L |
| Potassium Pyrophosphate (this product) | 250-380 g/L | 250-320 g/L |
| P2O7 : Cu ratio (maintained) | 7.0-8.0 : 1 | 7.5-8.5 : 1 |
| Free ammonia (as NH3) | 1-3 g/L | 1-2 g/L |
| Potassium nitrate (optional accelerator) | 10-15 g/L | 5-10 g/L |
| pH (KOH or pyrophosphoric acid) | 8.2-8.8 | 8.4-8.8 |
| Temperature | 50-60°C | 50-55°C |
| Cathode current density | 1-5 A/dm² | 0.5-2 A/dm² |
| Agitation | Solution movement / cathode movement | Barrel rotation |
These are workshop-proven ranges for zipper and hardware work. Orthophosphate builds up slowly from hydrolysis and drag-in; when it passes roughly 100 g/L the bath needs dilution or partial replacement because brightness and limiting current fall. Keep anodes in bags, filter at 5 μm, and dummy-plate at low current density after long idle periods.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Rough, gritty deposit at normal current | Ratio below ~6.5:1, copper hydrolysing, or insolubles from low-grade salt | Analyse Cu and P2O7; add potassium pyrophosphate to ratio 7.5:1; check salt insolubles |
| Burning / powdery edges at high current density | P2O7:Cu ratio too high (> 9) or copper metal too low | Raise copper with copper pyrophosphate; keep ratio below 8.5 |
| Anodes filmed green and bath copper falls | Anode passivation: low free ammonia, low temperature, ratio too high | Add ammonia to 1-3 g/L, run at 55°C, scrub anodes, raise anode area |
| Dull, streaky, slow deposit | Organic build-up or brightener/additive imbalance | Carbon filter 2-5 g/L, Hull cell re-balance, dummy plate |
| Haze or precipitate floating in bath | Orthophosphate accumulation, or zinc/iron dragged in from substrate | Analyse; dilute or partial bath replacement; improve rinses before the tank |
| Blistering on zinc die-cast parts | Alkaline attack: pH above 9 or chloride drag-in from earlier acid dips | Hold pH at 8.2-8.8, tighten rinsing, never add caustic to the strike zone |
Handling & Safety for the Plating Line
- Health: pyrophosphate dust is alkaline and irritating to eyes, skin and airways. Wear goggles, gloves and a dust mask when opening bags or dissolving; wash splashes immediately with water.
- Dissolving: add salt slowly to cold or lukewarm water with good stirring. The solution is alkaline - never add concentrated acid directly to it, and never add water to a pile of salt (caking, slow dissolution).
- Storage: potassium pyrophosphate is hygroscopic. Keep bags sealed on pallets in a dry store; caked salt must be broken and fully dissolved - it is still usable but check assay if caking was severe.
- Spills: sweep dry spills; rinse residues with plenty of water into the effluent system - the bath itself is cyanide-free, which is the point, but copper-bearing rinse water still needs treatment to ≤ 1-2 mg/L before discharge.
- Incompatibility: keep this salt and its solutions away from acid lines and from cyanide baths - accidental mixing wastes both chemistries and creates handling hazards.
- Bath hygiene: copper anodes must be OFHC in bags; dropped zinc or steel parts left in the bath dissolve and contaminate. Filter continuously and dummy at 0.3-0.5 A/dm² after shutdowns.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the pyrophosphate copper layer | Recommended practice |
|---|---|---|
| Iron / steel hardware | Alkaline non-cyanide copper undercoat that seals the surface before nickel-chrome; better levelling than an acid copper on rough steel | Alkaline clean + acid dip, copper 3-8 μm, then nickel; avoid long dwell at high pH |
| Zinc alloy (sliders, buckles) | The reason this bath exists: copper deposits on zinc without the etching of acid baths and without cyanide waste | Strike 1-3 μm at low current first, then build to 5-8 μm; hold pH below 8.8 to protect the zinc surface |
| Copper / brass | Used to re-plate stripped parts or to build thick ductile copper before further finishing without acid attack on fragile sections | Activate in 3-5% sulfuric, then copper; parts keep dimensional accuracy because there is no chemical etching |
| Stainless steel | Provides an alkaline first layer after nickel strike when a full cyanide-free sequence is specified | Nickel strike first (Woods type), rinse, then pyrophosphate copper; never plate copper directly on passive stainless |
FAQ
| Question | Answer |
|---|---|
| Why is the P2O7:Cu ratio more important than the salt concentration? | It fixes how much copper stays complexed and how fast it plates. Below ~6.5:1 copper drops out or plates rough; above ~9:1 efficiency falls and edges burn. Analyse both values, not just the salt. |
| Can pyrophosphate copper replace my cyanide copper strike completely? | For decorative zinc-alloy and steel work, yes - many lines run 100% cyanide-free. Start with a low-current strike step and verify adhesion by bend and heat tests before switching production. |
| How do I know if a bad batch of salt caused my problem? | Run a Hull cell on 90% live bath + 10% new make-up with the suspect salt, against a reference panel. Any shift in brightness, haze or limiting current points to the salt. |
| Does QLQ support cyanide-free copper conversion projects? | Yes. Shipments include a COA for every lot, and QLQ engineers help with the strike schedule, ratio analysis training and defect diagnosis from photos for customers in 10+ countries. |
Copper bath drifting? Send QLQ your analysis sheet and Hull cell photos - engineers diagnose pyrophosphate ratio, ammonia and contamination problems remotely and return a written correction plan. Contact us.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.