Professional Zinc Alloy Surface Finishing Solutions
Activated Carbon
Activated Carbon
QR 코드 생성
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Activated Carbon is the plating shop's standard bath-purification media for removing organic contamination - decomposed brighteners, drag-in oils, breakdown products and wetting-agent residues - from nickel, copper, zinc and tin solutions. Its internal surface area (typically 800-1200 m²/g) adsorbs organic molecules by the million, and one well-run carbon treatment can restore a hazy, pitted bath that new brightener additions cannot fix. Plating shops buy two physical forms for two different jobs: powdered carbon (200-325 mesh) for batch treatments - dumped into the tank at 2-5 g/L, agitated, settled and filtered out - and granular carbon (e.g. 4-8 or 8-30 mesh) for continuous side-stream polishing columns that keep organics low around the clock. The quality attributes that matter are iodine value (adsorption capacity), ash content, and - above all - acid-washed, low-metal grades: a non-acid-washed carbon can leach iron, zinc and calcium straight back into the very bath you are cleaning. Market grades for plating are coal- or coconut-based; coconut shell gives harder granules for columns, coal-based powder is the economical batch-treatment workhorse.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
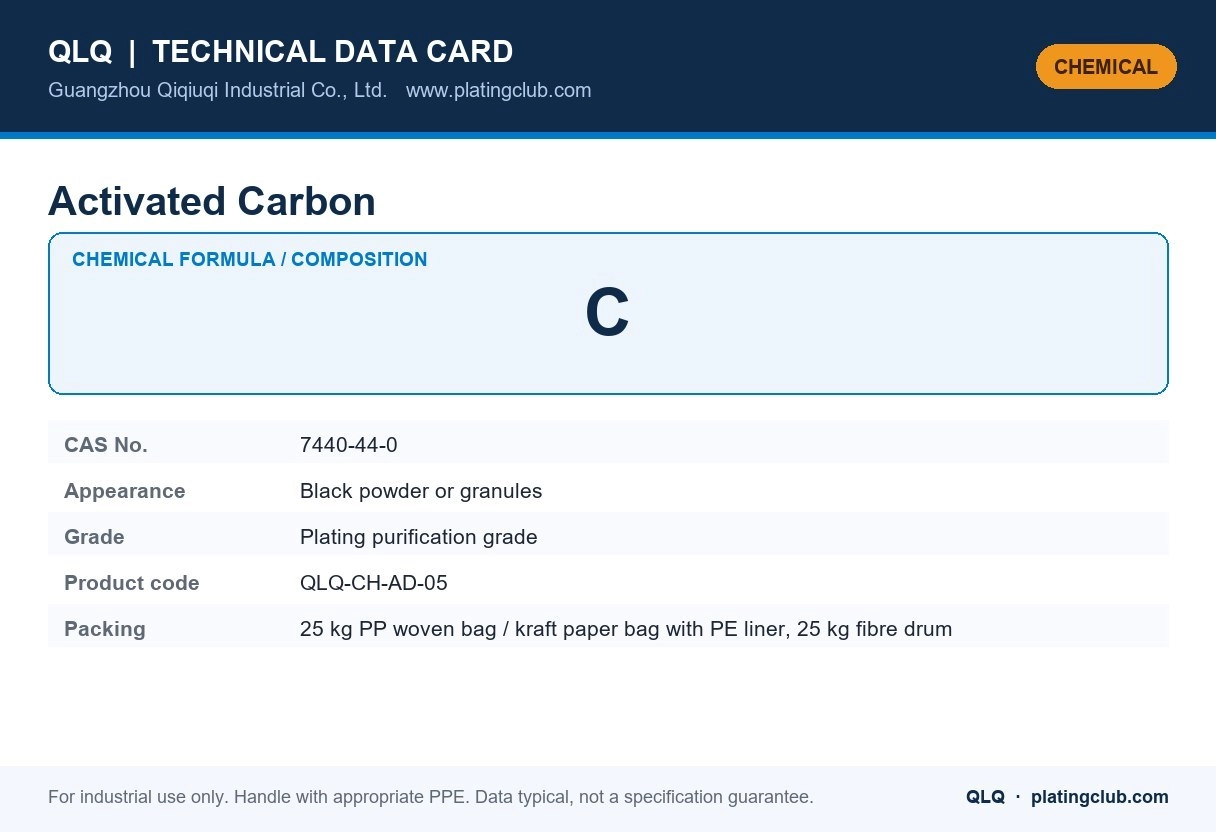
| Chemical name | Activated Carbon |
| Chemical formula | C |
| CAS number | 7440-44-0 |
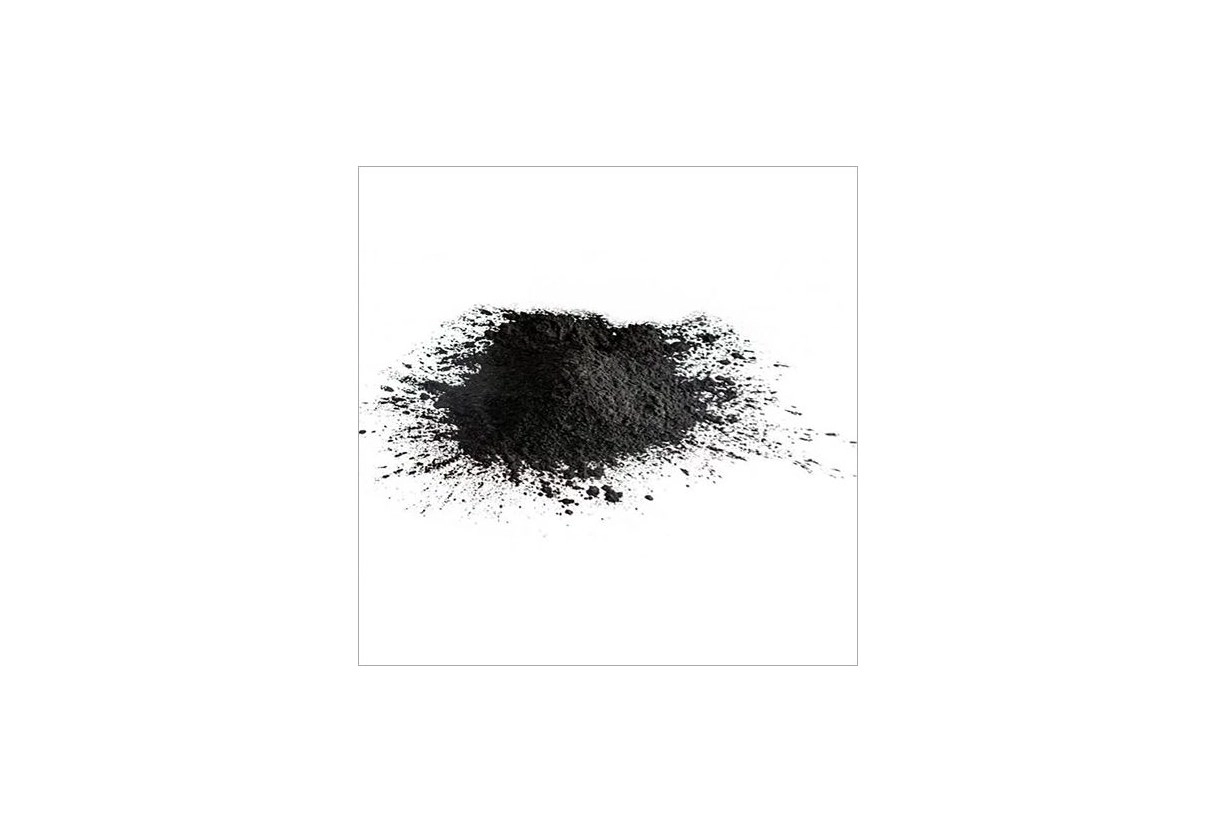
| Appearance | Black powder or granules |
| Grade / type | Plating purification grade |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Activated carbon is the purifying agent used to strip organic contamination and brightener breakdown products from plating baths so that the deposit returns to its correct brightness and ductility.
- Black powder or granules with a very high internal surface area; dosed at 1-5 g/L for batch purification.
- Removes organic brightener residues, oil and the breakdown products that cause dark, brittle or patchy deposits.
- Must be filtered out completely after treatment, otherwise the carbon itself becomes a contamination source.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Batch purification | 1-5 g/L, agitate for 1-2 hours, then filter with a fine filter aid |
| Continuous purification | A cartridge of granular carbon in the filter loop |
| Note | Never leave carbon in the tank overnight - it also removes the useful brighteners |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Not classified as dangerous for transport in most cases; observe good industrial hygiene and dust control |
| Personal protective equipment | Dust mask, goggles and gloves for powder handling; general ventilation |
| Spill / first aid | Sweep up dry; material is a nuisance dust — avoid breathing the dust |
| Storage | Cool, dry, sealed store; keep bags closed, off the floor and away from moisture |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| After carbon treatment the deposit lost brightness - why? | The carbon removed the brightener as well as the contamination; re-add the brightener system and check with a Hull cell. |
| Powder or granular carbon? | Powder for batch purification, granular for continuous cartridge use. |
| Item | Typical Value |
|---|---|
| Form | Powder (200-325 mesh) and granular (4-8 / 8-30 mesh) |
| Base material | Coal (powder), coconut shell (granular) |
| Iodine value | 900-1200 mg/g (declared per lot) |
| Surface area | ≥ 900 m²/g |
| Ash | ≤ 8% (acid-washed grades lower) |
| Moisture | ≤ 5% |
| Water-soluble iron | ≤ 0.05% (acid-washed) |
| Standard packing | 15KG/CARTON, sealed bags inside |
Process Note: When a Bath Needs Carbon
Carbon removes organics indiscriminately - including the brighteners you paid for - so it should never be the first move. These signs on the Hull cell and on parts point to organic contamination:
| Sign on parts / panel | What is building up | Action before carbon |
|---|---|---|
| Haze in the low-current range that brightener top-up will not clear | Brightener breakdown products | Confirm by adding brightener to a fresh panel - no change means organics |
| Pinholes and pitting returning despite wetting agent in range | Oils, wetter residues, decomposed colloids | Check surface tension and filtration first |
| Dull, cloudy nickel that chromium rejects | Mixed organic load + metal contamination | Carbon treat, then low-CD dummy for metals |
| Cloudy solution, bath smells | Heavy soil drag-in or bacterial growth (warm lines) | Carbon treat with extra rinse of work before the tank |
If adding fresh additive to a Hull cell restores the bright range, the bath is merely under-dosed - carbon would waste the new brightener. If the fresh-additive panel stays hazy, carbon is the correct next step.
How to Run a Batch Carbon Treatment
| Step | Operation | Detail |
|---|---|---|
| 1. Heat the bath | Raise to 50-60°C | Adsorption is faster and more complete warm |
| 2. Add carbon | Slurry 2-5 g/L powder in warm DI water | Make a slurry first - never dump dry powder (dust and clumping) |
| 3. Agitate | Circulate or air-stir 1-2 hours | Keep agitation gentle; longer for badly fouled baths |
| 4. Settle and filter | Settle 1-2 h, filter through 1-5 μm | Change filter cartridges as they blind; do not let carbon sit overnight |
| 5. Rebuild additives | Hull cell, then add brightener/wetter to target | Carbon strips organics - expect to re-dose from zero, not top-up |
| 6. Dummy and verify | Low-CD dummy 30-60 min, plate test panels | Clear haze gone, brightness and pit-free finish restored |
For continuous protection, a side-stream column of granular carbon (5-10% of bath volume per hour through the column) keeps nickel and acid copper lines organically clean between batch treatments.
Quality Checks Before Use
| Check | Method | Pass |
|---|---|---|
| Iodine value | COA (standard iodine adsorption test) | ≥ 900 mg/g for plating grades |
| Acid leach test | 10 g in 100 ml warm 5% H2SO4, 1 h, test metals | Fe/Zn/Ca low - no meaningful pickup (acid-washed grade) |
| Decolorizing test | Shake 0.5 g with 50 ml colored (tea/organic-dyed) water | Visible decolorizing in 10 min |
| Panel confirm | Treat a hazy Hull cell panel's bath sample | Haze clears, bright range returns after additive rebuild |
| Ash / moisture | COA review | Moisture ≤ 5%; high ash carbon carries salts into the bath |
How QLQ controls it: each activated-carbon lot is checked for iodine value, moisture and - critically - acid-leachable metals against a retained sample before release. QLQ ships only acid-washed grades for plating because a cheap non-washed lot can add more metal contamination than it removes; the COA records the leach result per lot.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Treatment does not clear the haze | Dose too low, bath too cold, or contact too short | Re-treat with 4-5 g/L at 55-60°C for 2 h |
| Bath metal content rises after carbon | Non-acid-washed carbon leaching Fe/Zn | Stop the lot; dummy the bath; switch to acid-washed grade |
| Filters blind in minutes | Carbon not settled, or powder too fine for the filter | Settle longer; use a pre-coat filter or 5 μm cartridges first |
| Brightness poor after "successful" treatment | Additives not rebuilt after carbon stripped them | Hull cell and re-dose brightener/wetter to target levels |
| Granules fine out of the column | Wrong mesh or high flow rate eroding the bed | Use 8-30 mesh and hold flow below ~10 bed volumes/hour |
| Bath re-fouls within days | Source of organic load never fixed | Find the drag-in source (cleaner carry-over, bad rinsing) and treat the cause |
Handling & Safety
- Dust: carbon dust is a nuisance and a mild irritant; wear a dust mask and gloves when weighing and slurrying. Carbon dust in air can be an explosion hazard near ignition sources.
- Never mix with strong oxidizers: powdered carbon in hot chromic acid or concentrated nitric acid mixtures can react violently (heat of oxidation). Never carbon-treat hexavalent chromium baths with powder.
- Spills: wet carbon makes slippery floors; sweep dry material and dispose of treated carbon as hazardous waste (it holds adsorbed metals and organics).
- Storage: sealed cartons in a dry store. Carbon adsorbs moisture and odors from the air; a damp, opened carton loses capacity and weighs wrong.
- Disposal: spent carbon from metal baths is metal-bearing waste - send for regeneration or licensed disposal, never to the general waste skip if it carried nickel or copper.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Effect of a clean (carbon-treated) bath on the part | Practice note |
|---|---|---|
| Iron / steel hardware | Pit-free, haze-free nickel that chromium accepts - no organic inclusions that start corrosion at the steel | Carbon treat the nickel when chrome rejection appears; verify before re-plating batches |
| Zinc alloy (sliders, buckles) | Organic-free copper/nickel layers plate dense and uniform - the difference between CASS pass and micro-pitting failure | Clean the copper base bath with carbon; die-cast work drags in the most organics |
| Copper / brass | Bright, level copper and nickel without low-CD haze on decorative panels | Side-stream carbon column suits acid copper; batch treat nickel quarterly |
| Stainless steel | Adherent nickel stack without organic films weakening the strike bond | Carbon treat strike and nickel baths together when adhesion issues recur |
FAQ
| Question | Answer |
|---|---|
| How often should I carbon treat my nickel bath? | Only when evidence demands it - haze that fresh brightener cannot clear, recurring pitting, or chromium rejection. Preventive quarterly treatments are common on busy decorative lines, but every treatment costs additives, so let the Hull cell decide. |
| Powdered or granular carbon - which do I need? | Powder for batch clean-ups (fast, thorough, removed by filtration), granular for continuous side-stream polishing. Most shops need a small stock of each. |
| Carbon stripped my brightener - is the bath ruined? | No - this is normal. After carbon treatment always rebuild the additive package from a Hull cell reading; the bath itself is healthier for having lost the breakdown products. |
| Can QLQ advise on carbon treatment procedure for our line? | Yes - QLQ supplies acid-washed plating carbon and written treatment procedures for nickel, copper and zinc baths, and engineers support customers remotely during their first treatment run. |
Bath haze that brightener cannot fix? QLQ engineering helps plating shops in 10+ countries run carbon treatments and rebalance additives by Hull cell. Contact us with your panel photos.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.