
Plating
Plating groups every process in this section. The overview below shows all options side by side - click any card to open the full process page with working parameters, step-by-step procedure and QC checks.
How to choose
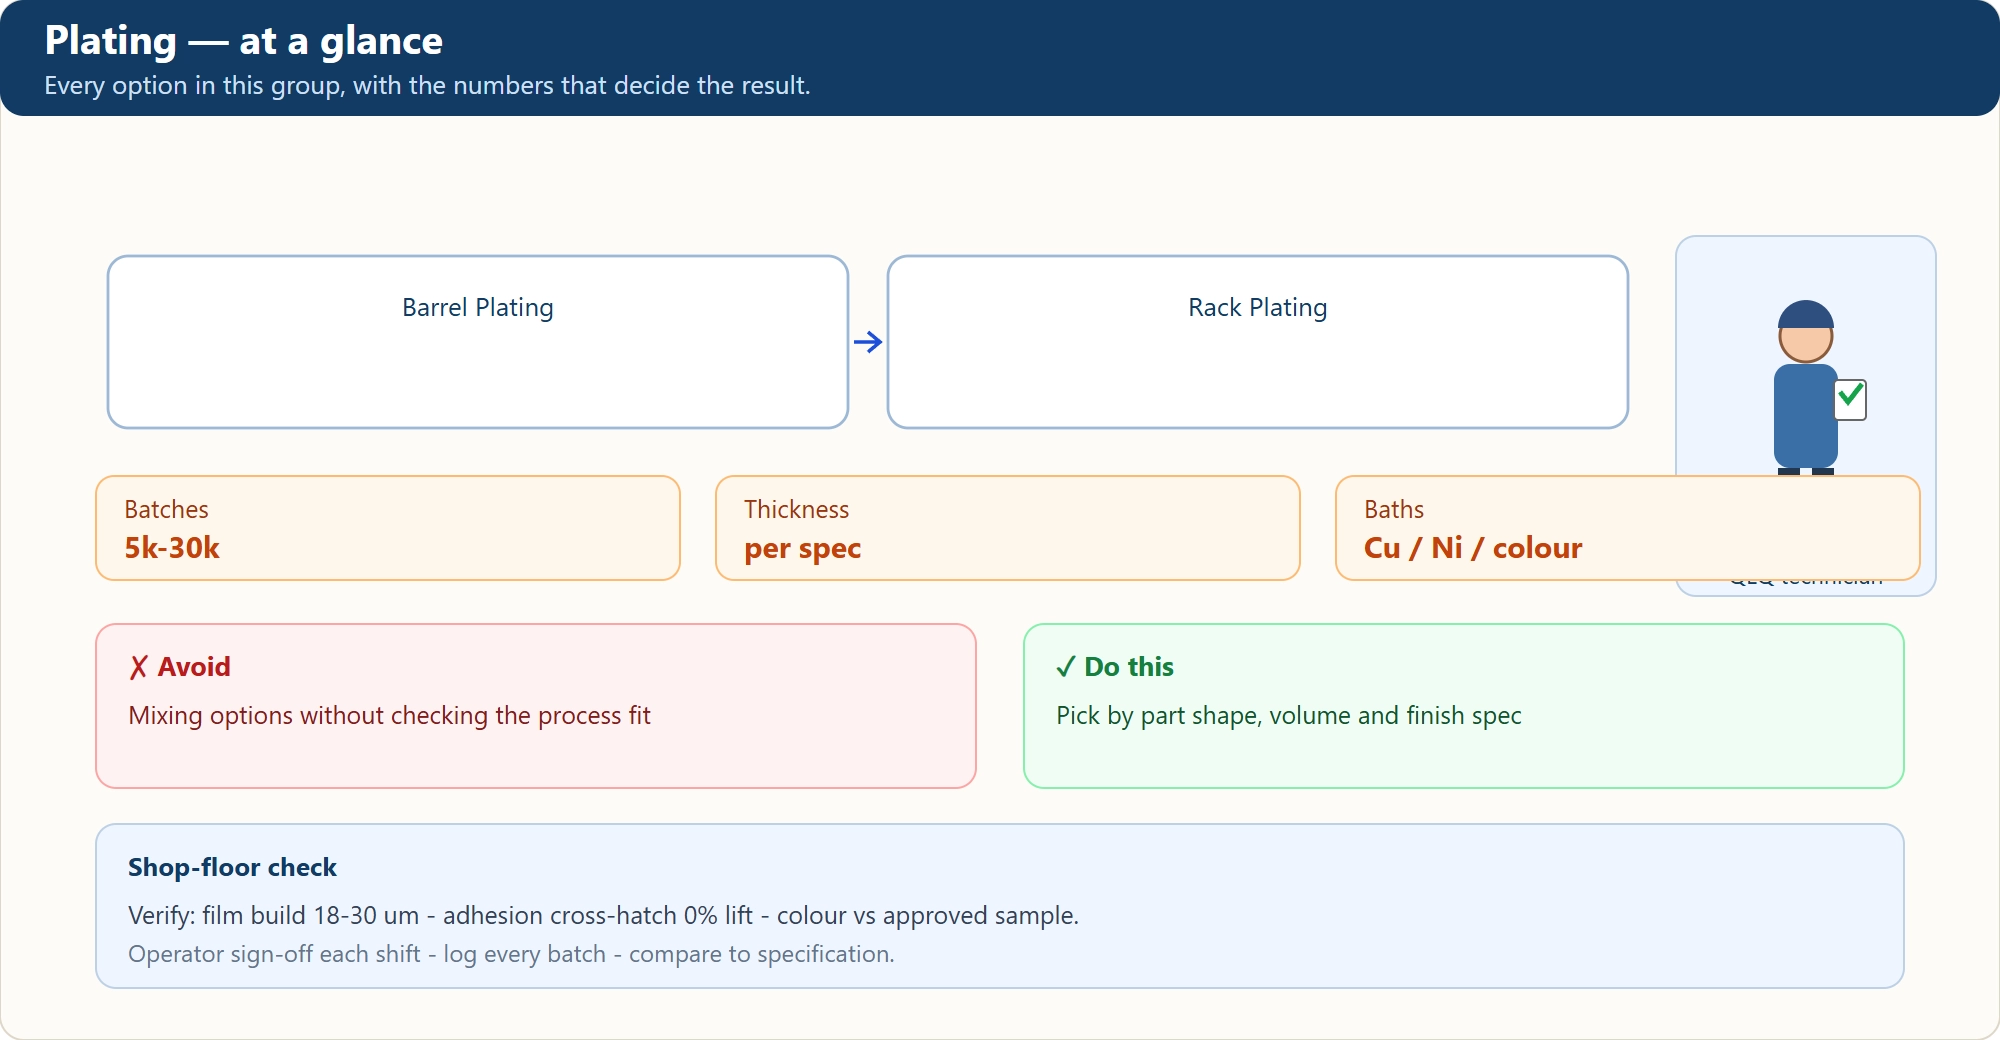
Part shape, batch size and the finish specification decide the route. Every page in this group lists working parameters and the checks that must pass before shipping. Ask QLQ engineering if your case sits between two options.
Rack vs barrel: pick the line by part geometry
| Factor | Rack plating | Barrel plating |
|---|---|---|
| Part size | Large, flat or easily marked | Small, robust, high volume |
| Contact marks | On the rack tips only | None, but tumbling can bruise soft parts |
| Thickness spread | Wide between edge and centre | Even, but longer cycle |
| Typical use | Visible decorative faces | Fasteners, sliders, small stampings |
Many plants run both. The decision is per part number, not per factory.
Defect → cause → fix
| Symptom | Cause | Fix |
|---|---|---|
| Burning at edges | Current density too high at contact points | Reduce current, add shields, improve rack contact |
| Patchy deposit | Poor contact or passivated surface | Clean rack contacts, activate before plating |
| Dull in recesses | Low agitation / low current density | Increase solution movement, use auxiliary anode |
| Pitting | Air or oil in the bath | Filter, carbon treat, check agitation |
FAQ
Can one rack run several part numbers?
Yes, if the current density window is similar. Mixing a large flat panel with small fasteners on the same rack usually gives burnt edges and thin centres.
How do we cut rework?
Log every reject with the rack position. Most repeat defects trace to one contact point or one blind hole, not to the bath.