Professional Zinc Alloy Surface Finishing Solutions
Cobalt Chloride
Cobalt Chloride
Luo QR-koodi
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
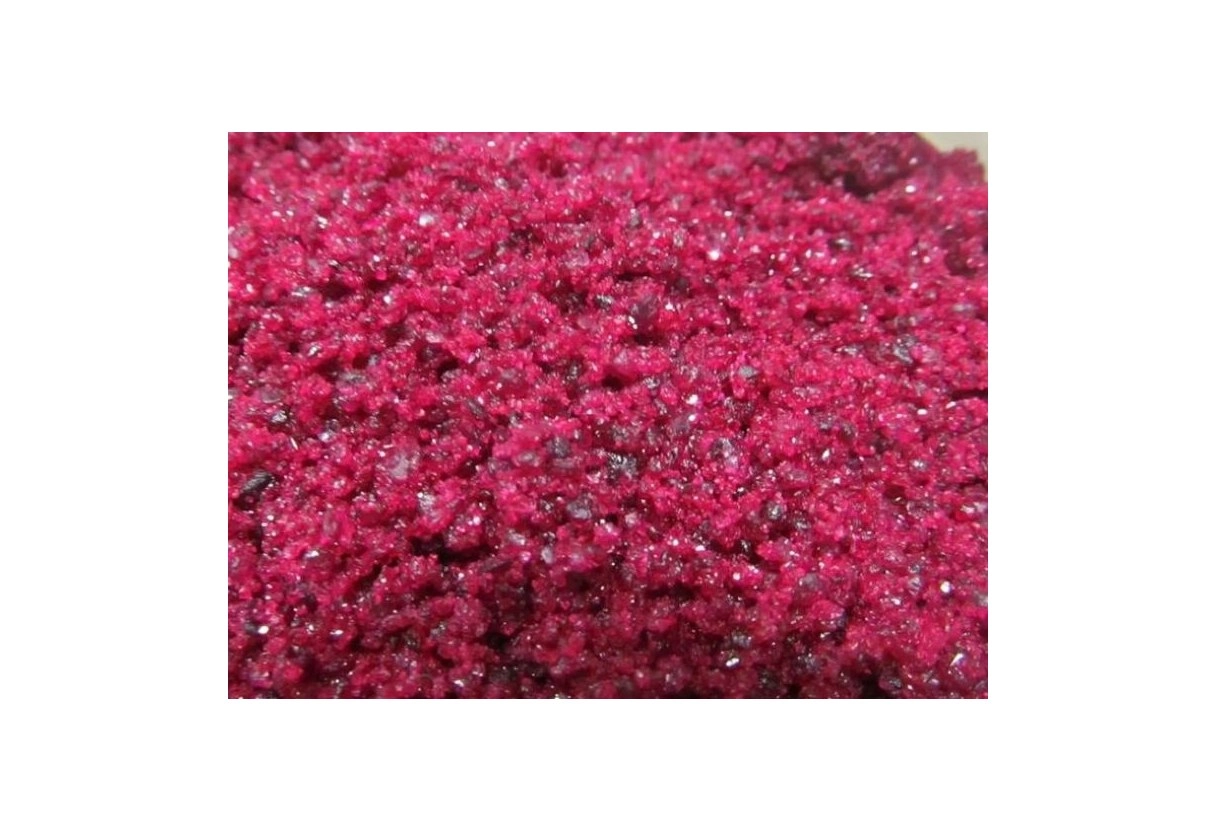
Cobalt Chloride Hexahydrate (CoCl2·6H2O) is the standard soluble source of cobalt(II) ions for the plating line - the salt behind zinc-cobalt alloy deposits (the workhorse corrosion finish for fasteners and small hardware) and nickel-cobalt alloy deposits used where extra hardness, wear resistance or a particular white tone is specified. It forms deep red-violet crystals that dissolve rapidly to a pink solution and carry approximately 24% cobalt metal. In QLQ's finishing plants cobalt chloride is dosed into zinc-alloy corrosion lines for automotive-style fasteners and into decorative Ni-Co work for belt and bag hardware. Market grades differ in metal limits and consistency: plating grade holds nickel, copper and iron tightly (impurities change deposit colour and magnetic behaviour), while catalyst / pigment grades sold for other industries are not controlled to plating requirements. Cobalt salts are significantly more expensive than nickel or zinc salts, so quality should be judged by analysis, not by price per bag.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
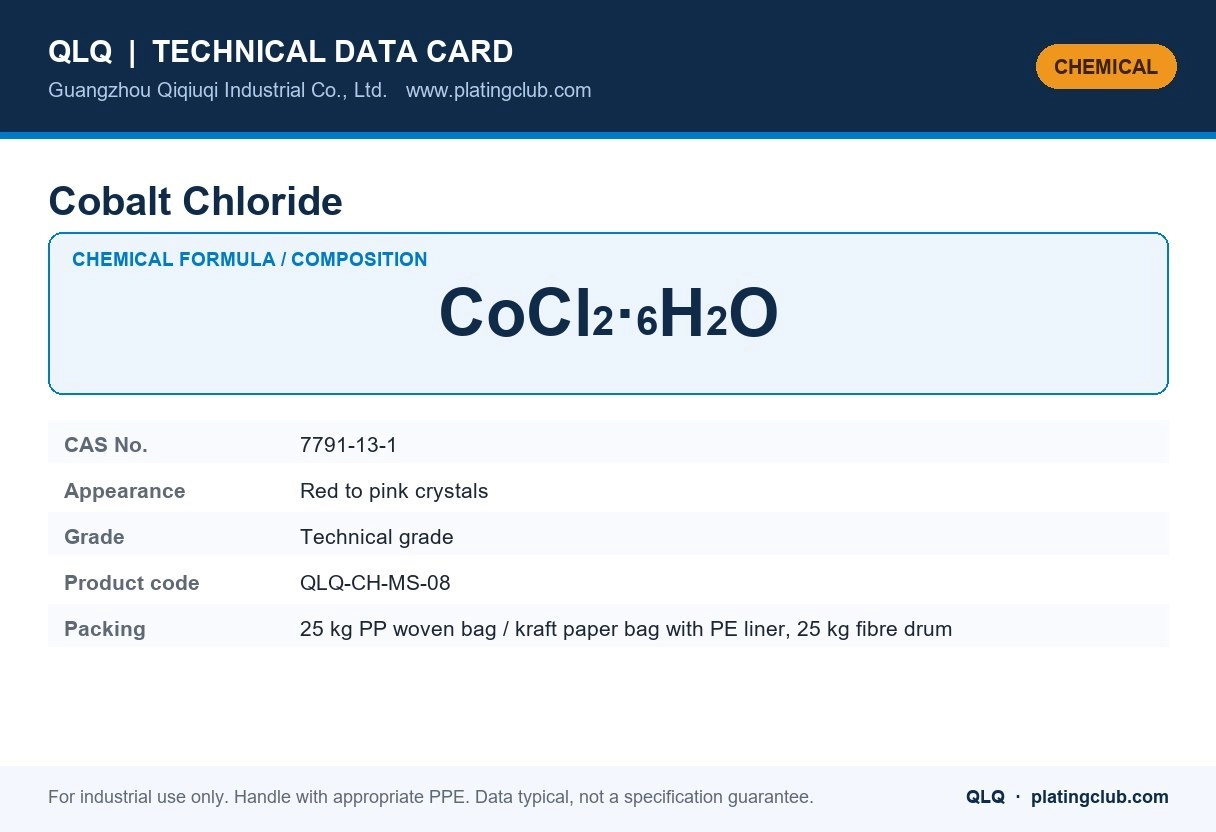
| Chemical name | Cobalt Chloride |
| Chemical formula | CoCl2·6H2O |
| CAS number | 7791-13-1 |
| Appearance | Red to pink crystals |
| Grade / type | Technical grade |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Cobalt chloride is used as a cobalt source and as a brightening additive in nickel and cobalt-nickel deposits, and as the starting material for cobalt colouring solutions.
- Red to pink crystals that lose water of crystallisation and turn blue when heated - the classic test for the hydrated form.
- Added at low concentration to nickel baths to increase hardness and brightness, and to the black nickel formulation.
- Cobalt compounds are hazardous to aquatic life and to health; keep the COA and MSDS with the batch record.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Nickel bath brightening | 1-5 g/L depending on the additive system |
| Cobalt-nickel alloy bath | 10-40 g/L CoCl2.6H2O |
| Black nickel bath | As specified by the formulation |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Harmful / toxic (GHS06/08 depending on the metal) + skin sensitiser |
| Personal protective equipment | Nitrile gloves, goggles, dust mask, coverall; no eating or smoking in the work area |
| Spill / first aid | Sweep up dry, place in a labelled drum, rinse the area; do not discharge metal-bearing solution to drains |
| Storage | Dry, ventilated store, keep bags closed; segregate from acids, oxidisers and food; keep a COA and an MSDS with each batch |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Why does the powder look blue in the drum? | Partly dehydrated material turns blue; it returns to red-pink on dissolution and is not a quality fault. |
| What is the cobalt content? | About 24.7% Co in the hexahydrate; the exact value is printed on each COA. |
| Item | Typical Value |
|---|---|
| Chemical formula | CoCl2·6H2O |
| Cobalt content | ≥ 24.0% |
| Assay | ≥ 98.0% (plating grade) |
| Appearance | Red-violet crystals, pink aqueous solution |
| Nickel (Ni) | ≤ 0.1% (lower for Ni-Co colour work) |
| Cu / Fe (each) | ≤ 0.005% |
| Sulfate | ≤ 0.05% |
| Water insoluble | ≤ 0.01% |
| Standard packing | 25KG drum with PE inner liner (hygroscopic salt) |
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Colour & form | Visual | Deep red-violet crystals; dull brown-red or wet sticky mass = moisture damage or impurity |
| Solubility / clarity | Dissolve 20 g in 100 ml DI water | Clear pink solution in 2 min; no residue, no turbidity |
| Assay / cobalt metal | COA (EDTA titration of Co) | ≥ 24% Co; keep lot-to-lot spread within ±0.3% or re-dose by analysis |
| Nickel impurity | Supplier COA + periodic lab check | Ni ≤ 0.1%; for Ni-Co decorative work prefer ≤ 0.05% - Ni shifts deposit tone |
| Hull cell check | Dose your own Zn-Co or Ni-Co bath with 10% new salt, plate panel | Alloy composition and bright range unchanged; compare against reference panel |
How QLQ controls it: cobalt chemistry is expensive and dose-sensitive, so every lot is quarantined, assay-verified against the COA, and Hull-cell tested in a live alloy bath before release. The batch record is kept for 12 months so any composition drift can be traced to the exact salt lot used on the day.
How It Works in the Alloy Baths
Cobalt co-deposits with zinc or nickel in anomalous fashion - a small amount of cobalt ion in the bath produces a disproportionately high cobalt content in the deposit, and the relationship changes with current density. That is why bath cobalt is maintained by analysis (titration or AA) and by Hull cell panels, never by guesswork. In zinc-cobalt the cobalt refines the zinc deposit and raises its corrosion resistance after passivation; in nickel-cobalt it hardens the layer and changes its colour and magnetic response. Deposits are controlled to a cobalt percentage, and the salt is only the vehicle that delivers it.
| Parameter | Alkaline zincate Zn-Co (barrel) | Acid chloride Zn-Co | Ni-Co decorative/hard |
|---|---|---|---|
| Zinc (as ZnO / ZnCl2) | 6-10 g/L metal (ZnO make-up) | 25-35 g/L metal (ZnCl2) | - |
| Cobalt metal from CoCl2·6H2O | 0.04-0.10 g/L | 3-8 g/L | 5-25 g/L CoCl2·6H2O added to Watts nickel |
| Caustic / chloride carrier | NaOH 110-140 g/L | KCl or NH4Cl 180-230 g/L | NiCl2 + H3BO3 per nickel bath |
| Boric acid | - | 20-30 g/L | 40-45 g/L |
| pH | > 13 (natural) | 4.8-5.5 | 3.8-4.5 |
| Temperature | 20-30°C | 25-35°C | 45-55°C |
| Cathode current density | 0.5-2.5 A/dm² | 1-4 A/dm² | 1-5 A/dm² |
| Typical Co in deposit | 0.4-0.8% | 0.4-1.0% | 5-30% depending on application |
Brightener and complexant systems for these alloys are proprietary and specific to each supplier - the cobalt chloride dose must be matched to the chosen system. These columns are working windows, not a licence to blend a commercial bath without the additive package.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Corrosion test fails (white rust early) | Deposit cobalt below target - bath cobalt drifted low through drag-out | Titrate Co; top up cobalt chloride; re-check Hull cell |
| Deposit darker / banded at low current density | Cobalt content rising in low-CD areas (anomalous co-deposition) | Re-balance bath Co and brightener; check agitation and rack geometry |
| Brittle or stressed Ni-Co deposit | Cobalt too high for the application, or organic build-up | Dilute/partial replace; carbon treat; re-dose cobalt by analysis |
| Bath turns cloudy | pH out of range (Zn-Co acid type), or iron/copper contamination from parts | Correct pH, dummy plate, filter; check dropped parts in tank |
| Salt batch causes tone shift | Nickel or iron impurity above spec in the cobalt salt | Return to certified plating grade; verify impurity limits on COA before use |
Handling & Safety for the Plating Line
- Health: cobalt chloride is a skin and respiratory sensitiser and is classified as a suspected carcinogen (inhalation) and a reproductive hazard in some jurisdictions. Handle with nitrile or PVC gloves, goggles and a dust mask; never inhale powder, and control mist over heated alloy baths with ventilation.
- Dissolving: crystals dissolve readily in water at room temperature with stirring; make a 20-30% stock solution and dose by volume from analysis results.
- Storage: cobalt chloride is deliquescent - keep drums sealed in a dry store. A wet, caked drum has picked up moisture; weigh and analyse carefully before use.
- Spills: collect dry spills; never wash cobalt into drains. Effluent cobalt is regulated (typically 0.1-1 mg/L limits) and does not settle well at simple hydroxide pH - precipitate with sulfide or use the dedicated alloy waste stream.
- Bath contamination: the classic enemies are iron (dissolved parts), copper and organics from brightener over-feed. Filter continuously and dummy-plate after downtime.
- Cross-contamination: keep cobalt dosing tools and stock tanks separate from plain zinc and nickel lines - a few mg/L of cobalt changes a plain zinc deposit's colour and corrosion behaviour.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the cobalt-bearing layer | Recommended practice |
|---|---|---|
| Iron / steel fasteners | Zn-Co alloy with trivalent or hexavalent passivation gives automotive-grade corrosion protection with less deposit than plain zinc | Barrel plate 6-12 μm, passivate, seal; control Co in deposit by periodic strip-and-titrate |
| Zinc alloy (sliders, buckles) | Ni-Co top layers give a whiter, harder decorative finish than plain nickel on small hardware | Copper undercoat first; Ni-Co 5-10 μm; verify wear if parts slide against each other |
| Copper / brass | Ni-Co over brass achieves engineering hardness for working surfaces while keeping a bright white tone | Activate, plate 5-15 μm Ni-Co, check stress if parts are formed after plating |
| Stainless steel | Cobalt-alloy or Ni-Co layers are specified for wear and magnetic applications on precision stainless components | Activate properly (cathodic etch or nickel strike); control cobalt content against the magnetic spec |
FAQ
| Question | Answer |
|---|---|
| Why is my deposit cobalt higher at low current density? | Cobalt co-deposits anomalously with zinc and nickel - its deposition is favoured where current is low. Wide CD ranges widen the cobalt spread, so control geometry, agitation and average CD before suspecting the salt. |
| Can I use cobalt sulfate instead of the chloride? | Yes, both are common cobalt sources. Chloride helps anode dissolution and conductivity in chloride baths; sulfate suits sulfate-based systems. Match the anion to the rest of the bath, and convert the dose on cobalt metal, not on salt weight. |
| How often should cobalt be analysed? | Daily on busy alloy lines, or per shift if drag-out is heavy. Cobalt consumption is small but drag-out is constant; weekly titration on barrel work is the minimum that keeps alloy % inside spec. |
| Does QLQ support Zn-Co conversion projects? | Yes. Every cobalt chloride shipment carries a COA, and QLQ engineers help customers in 10+ countries set up alloy analysis, Hull cell routines and remote defect diagnosis. |
Alloy composition drifting? Send QLQ your titration values and Hull cell panels - engineers check cobalt, carrier salt and impurity balance and return a written correction plan. Contact us.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.