

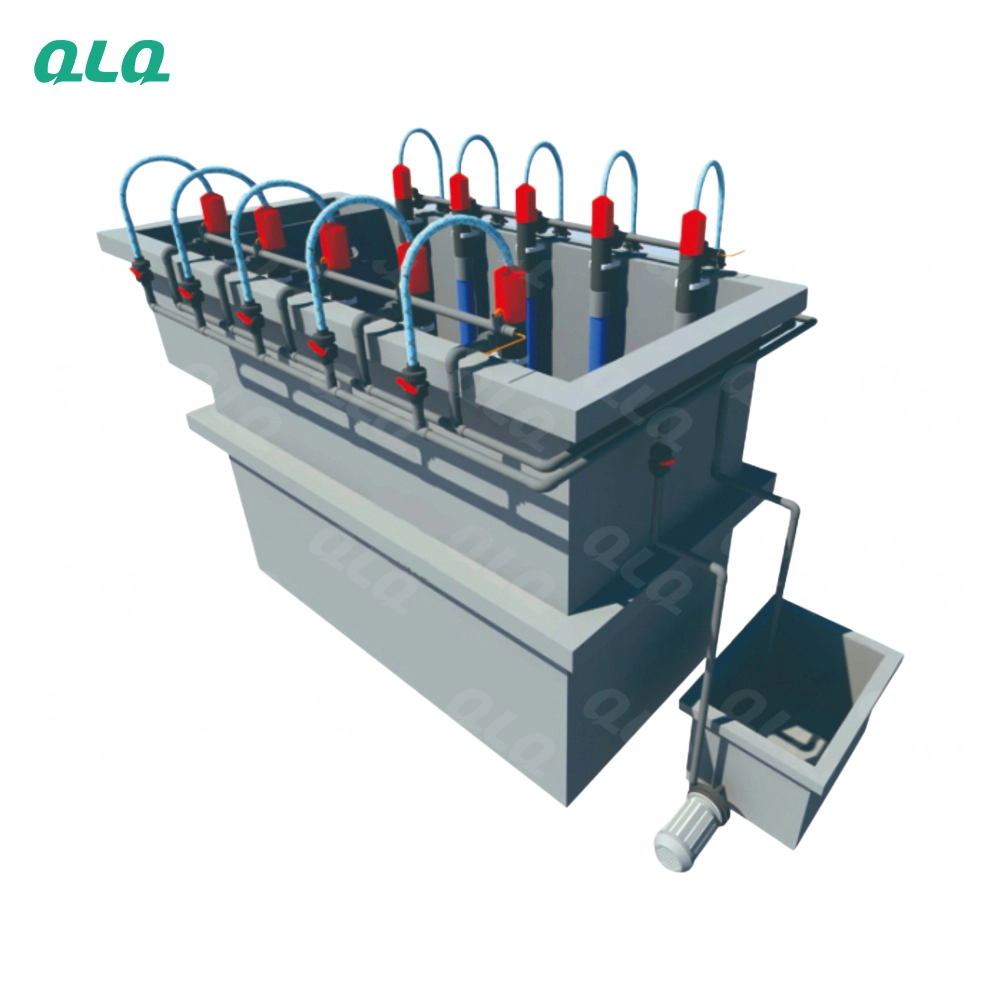
An e-coat bath fails slowly through poor turnover before it fails suddenly through contamination. Dead zones, weak filtration and temperature drift each shorten bath life, and the cost appears later as a premature dump.
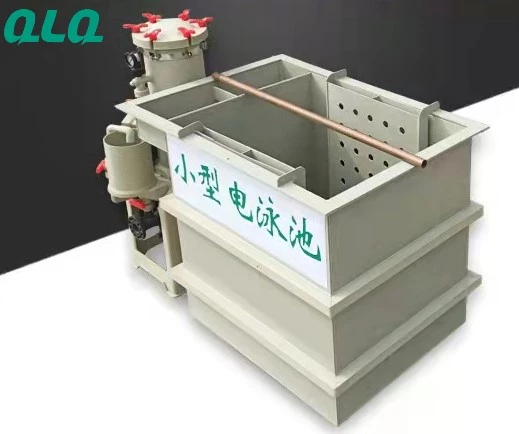
This senior guide covers bath turnover management: circulation rate and dead zones, filtration and UF balance, temperature zones across the tank, and the maintenance plan that extends bath life instead of planning a dump.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Ignoring dead zones | Sludge builds silently | Map flow across the tank |
| 2. Low turnover | Contamination accumulates | Check turnover per hour |
| 3. Temperature gradients | Film varies by zone | Measure tank zones |
| 4. Filtration undersized | Solids climb | Match filter to turnover |
| 5. UF flow ignored | Bath life shortens | Monitor UF with the bath |
| 6. Cleaning only the filter | Tank walls still foul | Schedule tank hygiene |
| 7. No flow map | Dead zone found too late | Map flow after changes |
| 8. Dump as default | Costly habit | Prevent with a plan |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Map circulation and find dead zones in the tank
- Maintain the turnover rate from the bath design
- Keep temperature even across all zones
- Monitor UF and filtration as one system
- Schedule tank hygiene to extend bath life
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Turnover management flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Bath life is decided by turnover long before analysis shows the damage.
- Tank hygiene belongs in the calendar, not in the dump decision.
- Never raise filter flow without checking UF balance.
- Never accept temperature gradients as normal for an old tank.
Working Data & Formula Notes
Turnover reference
Example values for e-coat turnover; confirm with your line design and supplier.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Turnover rate | Per bath design | Bath passes filter per hour |
| Temperature spread | Within 1-2 C | Across all tank zones |
| Filter pressure | Per filter spec | Rising pressure means service |
| UF flow | Per supplier | Balanced with drag-out |
| Hygiene cycle | Per tank design | Before foul zones build |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Turnover fault table
| Symptom | Cause | Response |
| Sludge in corners | Dead zones | Map and improve flow |
| Solids climbing | Low filtration | Check turnover rate |
| Film varies by load position | Temperature gradient | Measure and balance zones |
| UF pressure high | Membrane or flow issue | Service with the bath |
| Bath life shrinking | Poor turnover history | Tank hygiene plan |
Implementation Cases
Case 1 - sludge that never showed in analysis
Situation. A bath's analysis looked stable, but film quality slowly declined and the plant scheduled an early dump. A flow map found a large dead zone behind the return pipe where sludge had built up for months.
Approach. Circulation was redirected, tank hygiene scheduled, and the flow map became the reference for maintenance.
Outcome. The dump was cancelled, film quality returned, and bath life was extended well beyond the old cycle.
Case 2 - the temperature gradient that varied film
Situation. Parts coated on one side of the tank consistently showed different film from the other side. The bath analysis was identical, so the paint was blamed.
Approach. Temperature probes across the tank found a 4 C gradient caused by a weak heater zone. Heaters were rebalanced and a zone check added to the audit.
Outcome. Film variation stopped and the zone check is now part of the quarterly turnover audit.
Frequently Asked Questions
What is bath turnover?
How many times the bath volume passes through the filter system per hour.
Why map dead zones?
Sludge and bacteria build where flow never reaches, hiding from analysis.
How does temperature affect the bath?
Gradients change film across load positions and stress the chemistry.
Why monitor UF with the bath?
UF controls drag-out and solids; it is part of the same life system.
How often should filters be serviced?
On pressure and flow data, with the hygiene schedule.
When should I schedule tank hygiene?
On a cycle from the bath design, before fouled zones build.
Is a dump ever the answer?
Sometimes, but only after turnover and hygiene have been ruled out.
Who owns the turnover audit?
The senior bath owner, reviewed quarterly with the maintenance plan.
What Would You Like to Solve?
If your e-coat bath seems to age faster than it should, send us your tank layout, turnover rate and maintenance history. We can help build the flow map and hygiene plan that extend bath life and delay the dump decision.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.