

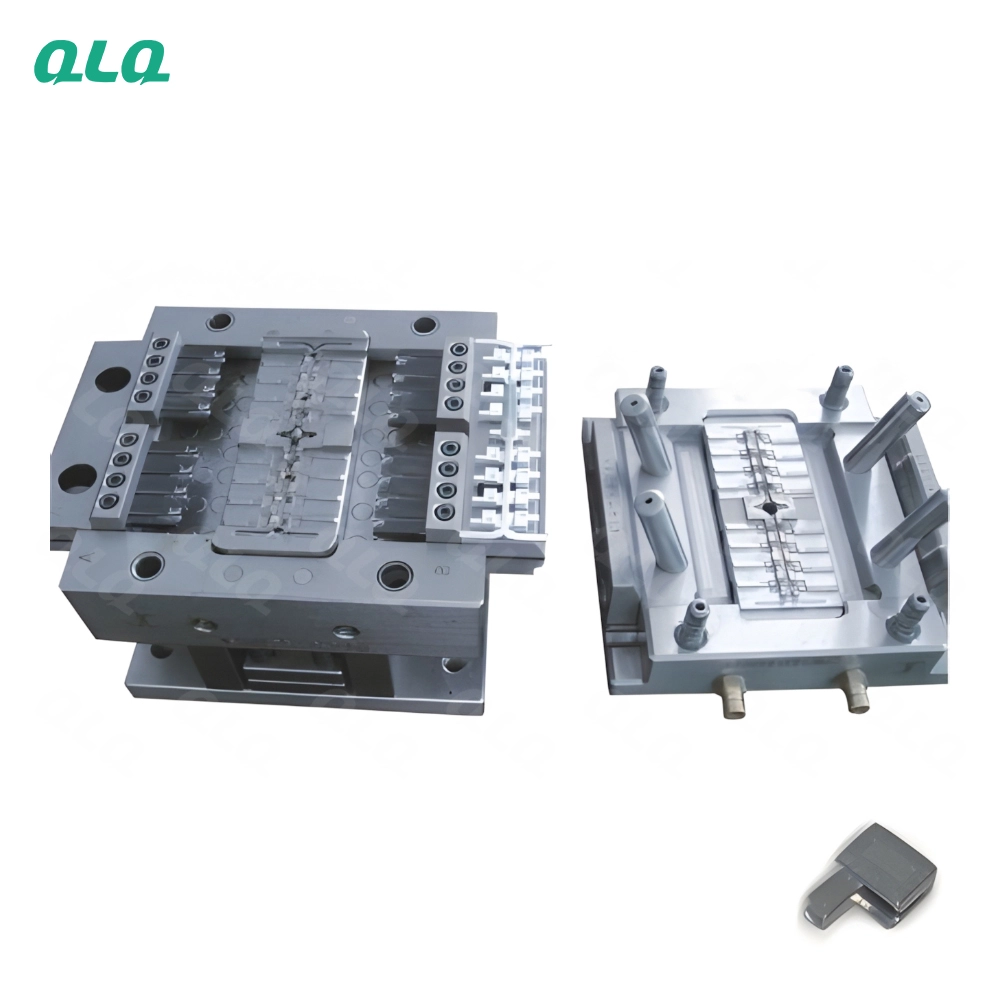
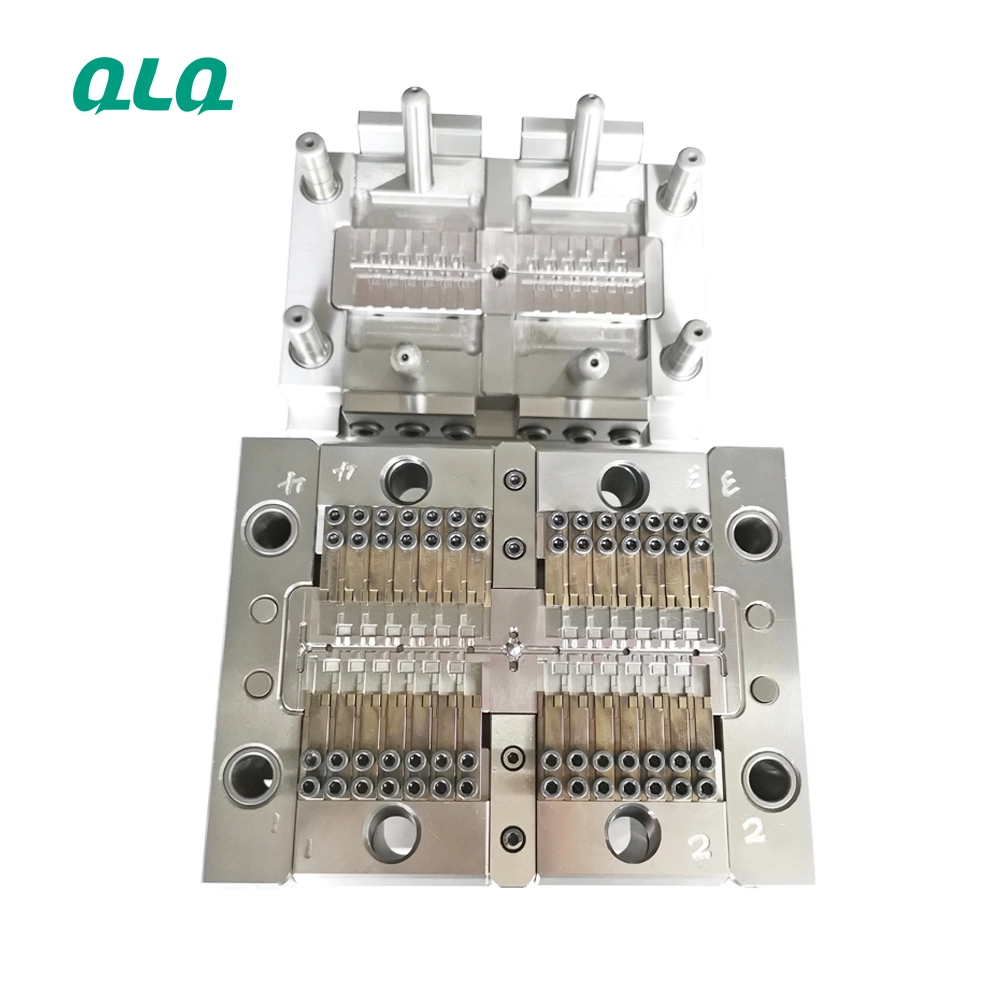
Zinc castings fail in finishing when their surface was decided at the die: a cold die gives a dull skin, a hot die gives sticking, and uneven temperature gives a patchwork surface that plating cannot hide.
This senior guide connects die thermal balance to casting surface quality and finishing performance, with temperature profiles, spray timing and evidence-based tuning.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Die temperature guessed | Surface varies | Map the zones |
| 2. Spray too early | Die shocks and cracks | Time after eject |
| 3. Spray uneven | Hot spots stay | Balance the nozzles |
| 4. Cold cavity surface | Dull skin | Raise local temperature |
| 5. Hot spots | Sticking and washout | Add cooling |
| 6. Thermal drift ignored | Patchwork surface | Log temperatures |
| 7. Surface blamed on polishing | Die cause | Check the die first |
| 8. No thermal map | Fixes blind | Map per cavity |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Map die temperature per cavity zone
- Time spray after ejection, before close
- Balance spray nozzles and cooling lines
- Hold 180-260 C typical per alloy
- Log thermal data with the batch
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Thermal balance flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Die temperature decides skin quality.
- Spray is part of thermal control, not just release.
- Never spray a closed die.
- Thermal couples need calibration.
Working Data & Formula Notes
Thermal data
Reference values for zinc die thermal control.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Die surface | 180-260 C typical | Cold dulls, hot sticks |
| Spray timing | After eject | Early spray cracks dies |
| Spray duration | Per zone | Uneven spray = hot spots |
| Cooling flow | Per circuit | Balanced cooling levels skin |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Thermal zone card
| Zone | Target C | Action |
| Gate area | Top of window | More cooling |
| Fill end | Mid window | Balanced |
| Deep rib | Lower | Check spray reach |
| Surface skin | Window | Verify finish |
Implementation Cases
Case 1 - dull skin fixed at the die, not the polish line
Situation. Castings needed extra polishing for a dull grey skin; the die ran cold at the fill end.
Approach. Cooling was rebalanced, spray was timed, and the zone map raised the fill-end temperature.
Outcome. Skin brightened and polishing time fell; the surface stopped hiding die faults.
Case 2 - sticking that started at a hot spot
Situation. Intermittent sticking and surface drag appeared on one cavity corner; the thermal map showed a hot spot.
Approach. A cooling line was added at the corner and spray timing was balanced.
Outcome. Sticking stopped and the drag marks disappeared from the cast surface.
Frequently Asked Questions
How does die temperature affect the surface?
Cold dies dull the skin; hot spots stick and drag; balance gives a clean finishable skin.
What temperature should the die run?
Typically 180-260 C at the surface for zinc, tuned per cavity zone.
Why time the spray?
Spraying after ejection and before close protects the die and controls temperature.
How do I map the die?
Use a thermal couple or pyrometer at each zone and record a map per cavity.
Why check spray coverage?
Uneven spray leaves hot spots that stick and drag the surface.
How do I fix a dull skin?
Raise local die temperature and confirm the surface responds before blaming polishing.
Should surface faults blame polishing?
No - check the die thermal map first; the skin is made in the die.
What do I log?
Zone temperatures, spray timing and the cast surface result per batch.
What Would You Like to Solve?
Send us your die zone map, spray settings and the surface complaint from finishing. We can help balance the thermal profile so the casting finishes cleanly.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.