
Scope of this guide
This intermediate guide goes into diagnosis: reading symptoms, isolating the variable that changed, and fixing it with data you can collect on the line.
Process: Resin Dripping. Figures in this guide are industry-standard starting ranges; confirm against your supplier TDS before locking settings.
Working ranges and control points
The table below is the daily reference for a dripping station. Set by the card, verify by the control point column.
| Parameter | Typical range | Control point | Watch out |
|---|---|---|---|
| Mix ratio | By resin kit (A:B) | Scale 0.1 g accuracy | Off-ratio never cures fully |
| Degassing | Vacuum 2–5 min after mix | No visible bubbles | Skipped step craters |
| Pot life | 20–60 min by kit | Discard at pot end | Thickened resin traps bubbles |
| Cure | 40–60 °C × 60–120 min | Profile per thickness | Thick pour exotherms |
| Bubble count QC | 0 visible > 0.3 mm | Light table per batch | Cold resin is viscous |
Diagnose It Fast: the intermediate view
Beyond the basic card, this is the layer that matters at your level:
| Symptom | Likely variable | Confirm by | First fix |
|---|---|---|---|
| Dull or hazy finish | Bath chemistry drift | Hull cell panel | Rebalance per test |
| Defects cluster on one rack position | Contact or current map | Position thickness map | Repair contact / re-map amps |
| Good-bad-good pattern | Loading or cycle drift | Time-stamped samples | Standardise load weight |
| Defect appears after maintenance | Work just done | Revert one change | Restore and re-verify |
Standard routine
- Warm resin to 25–30 °C for flow
- Scale A and B exactly; stir slowly 2–3 min
- Degas before pouring, not after
- Pour centre-out to let self-level
- Cure with profile, log oven load
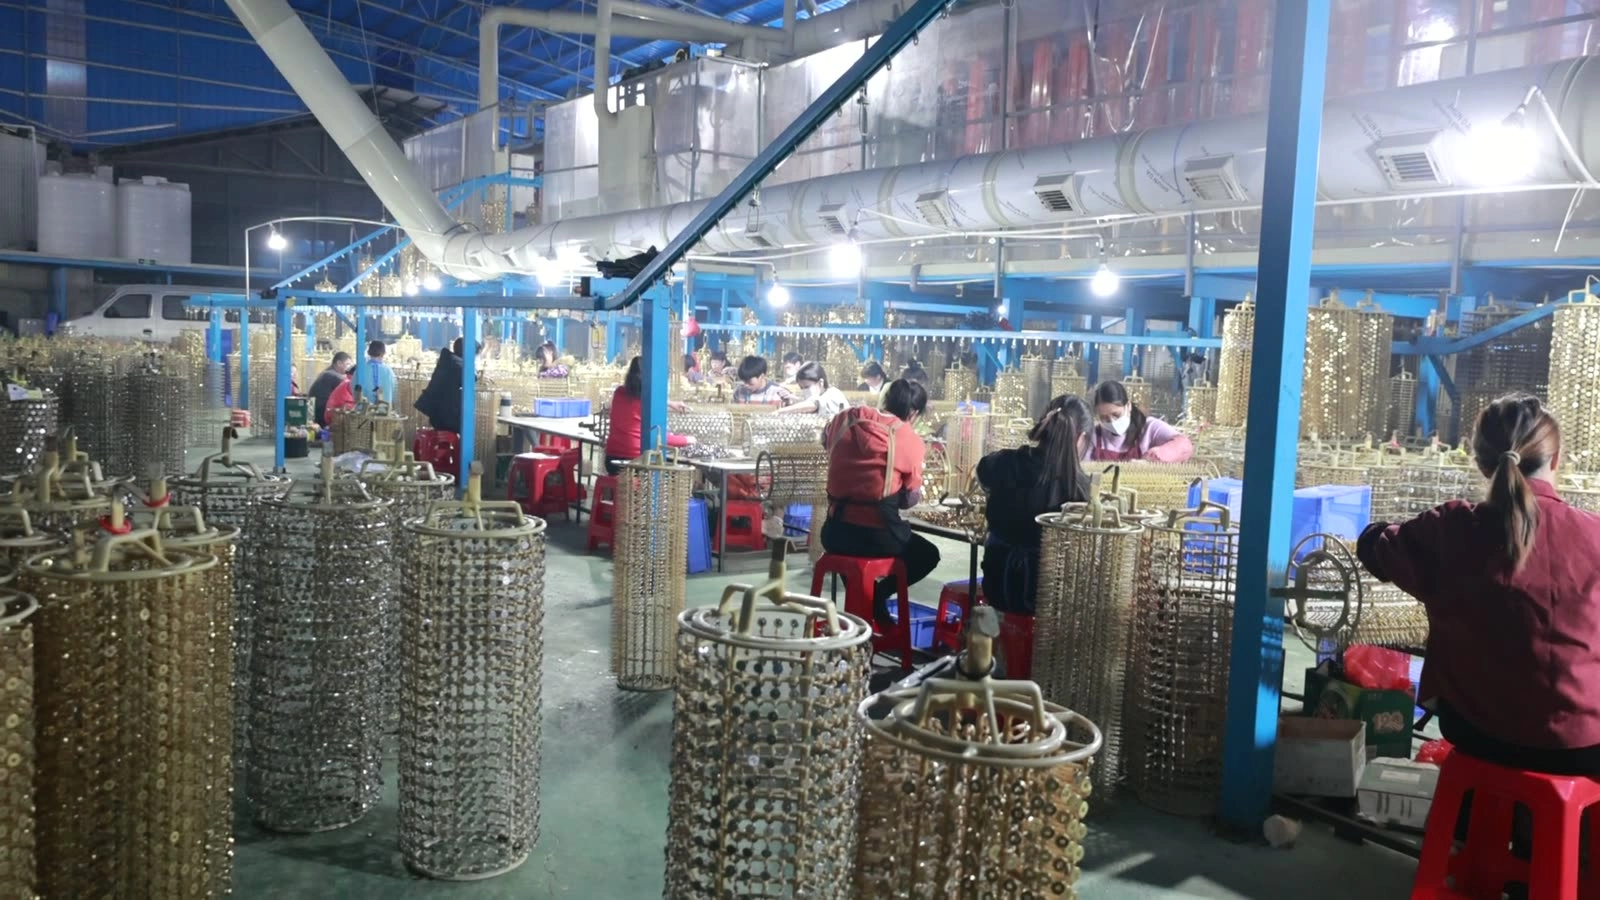
Engineer notes
- Stir fast and you whip bubbles in — slow folding wins
- Pot life shortens in summer; batch smaller
- Thick pours need stepped cure to avoid exotherm yellowing
- Dust-free covers over racks during gel
- Yellowing traces to over-heat or aged hardener
Safety: Uncured resin and hardener are skin sensitisers. Nitrile gloves, no latex, and barrier cream; ventilate the curing oven.
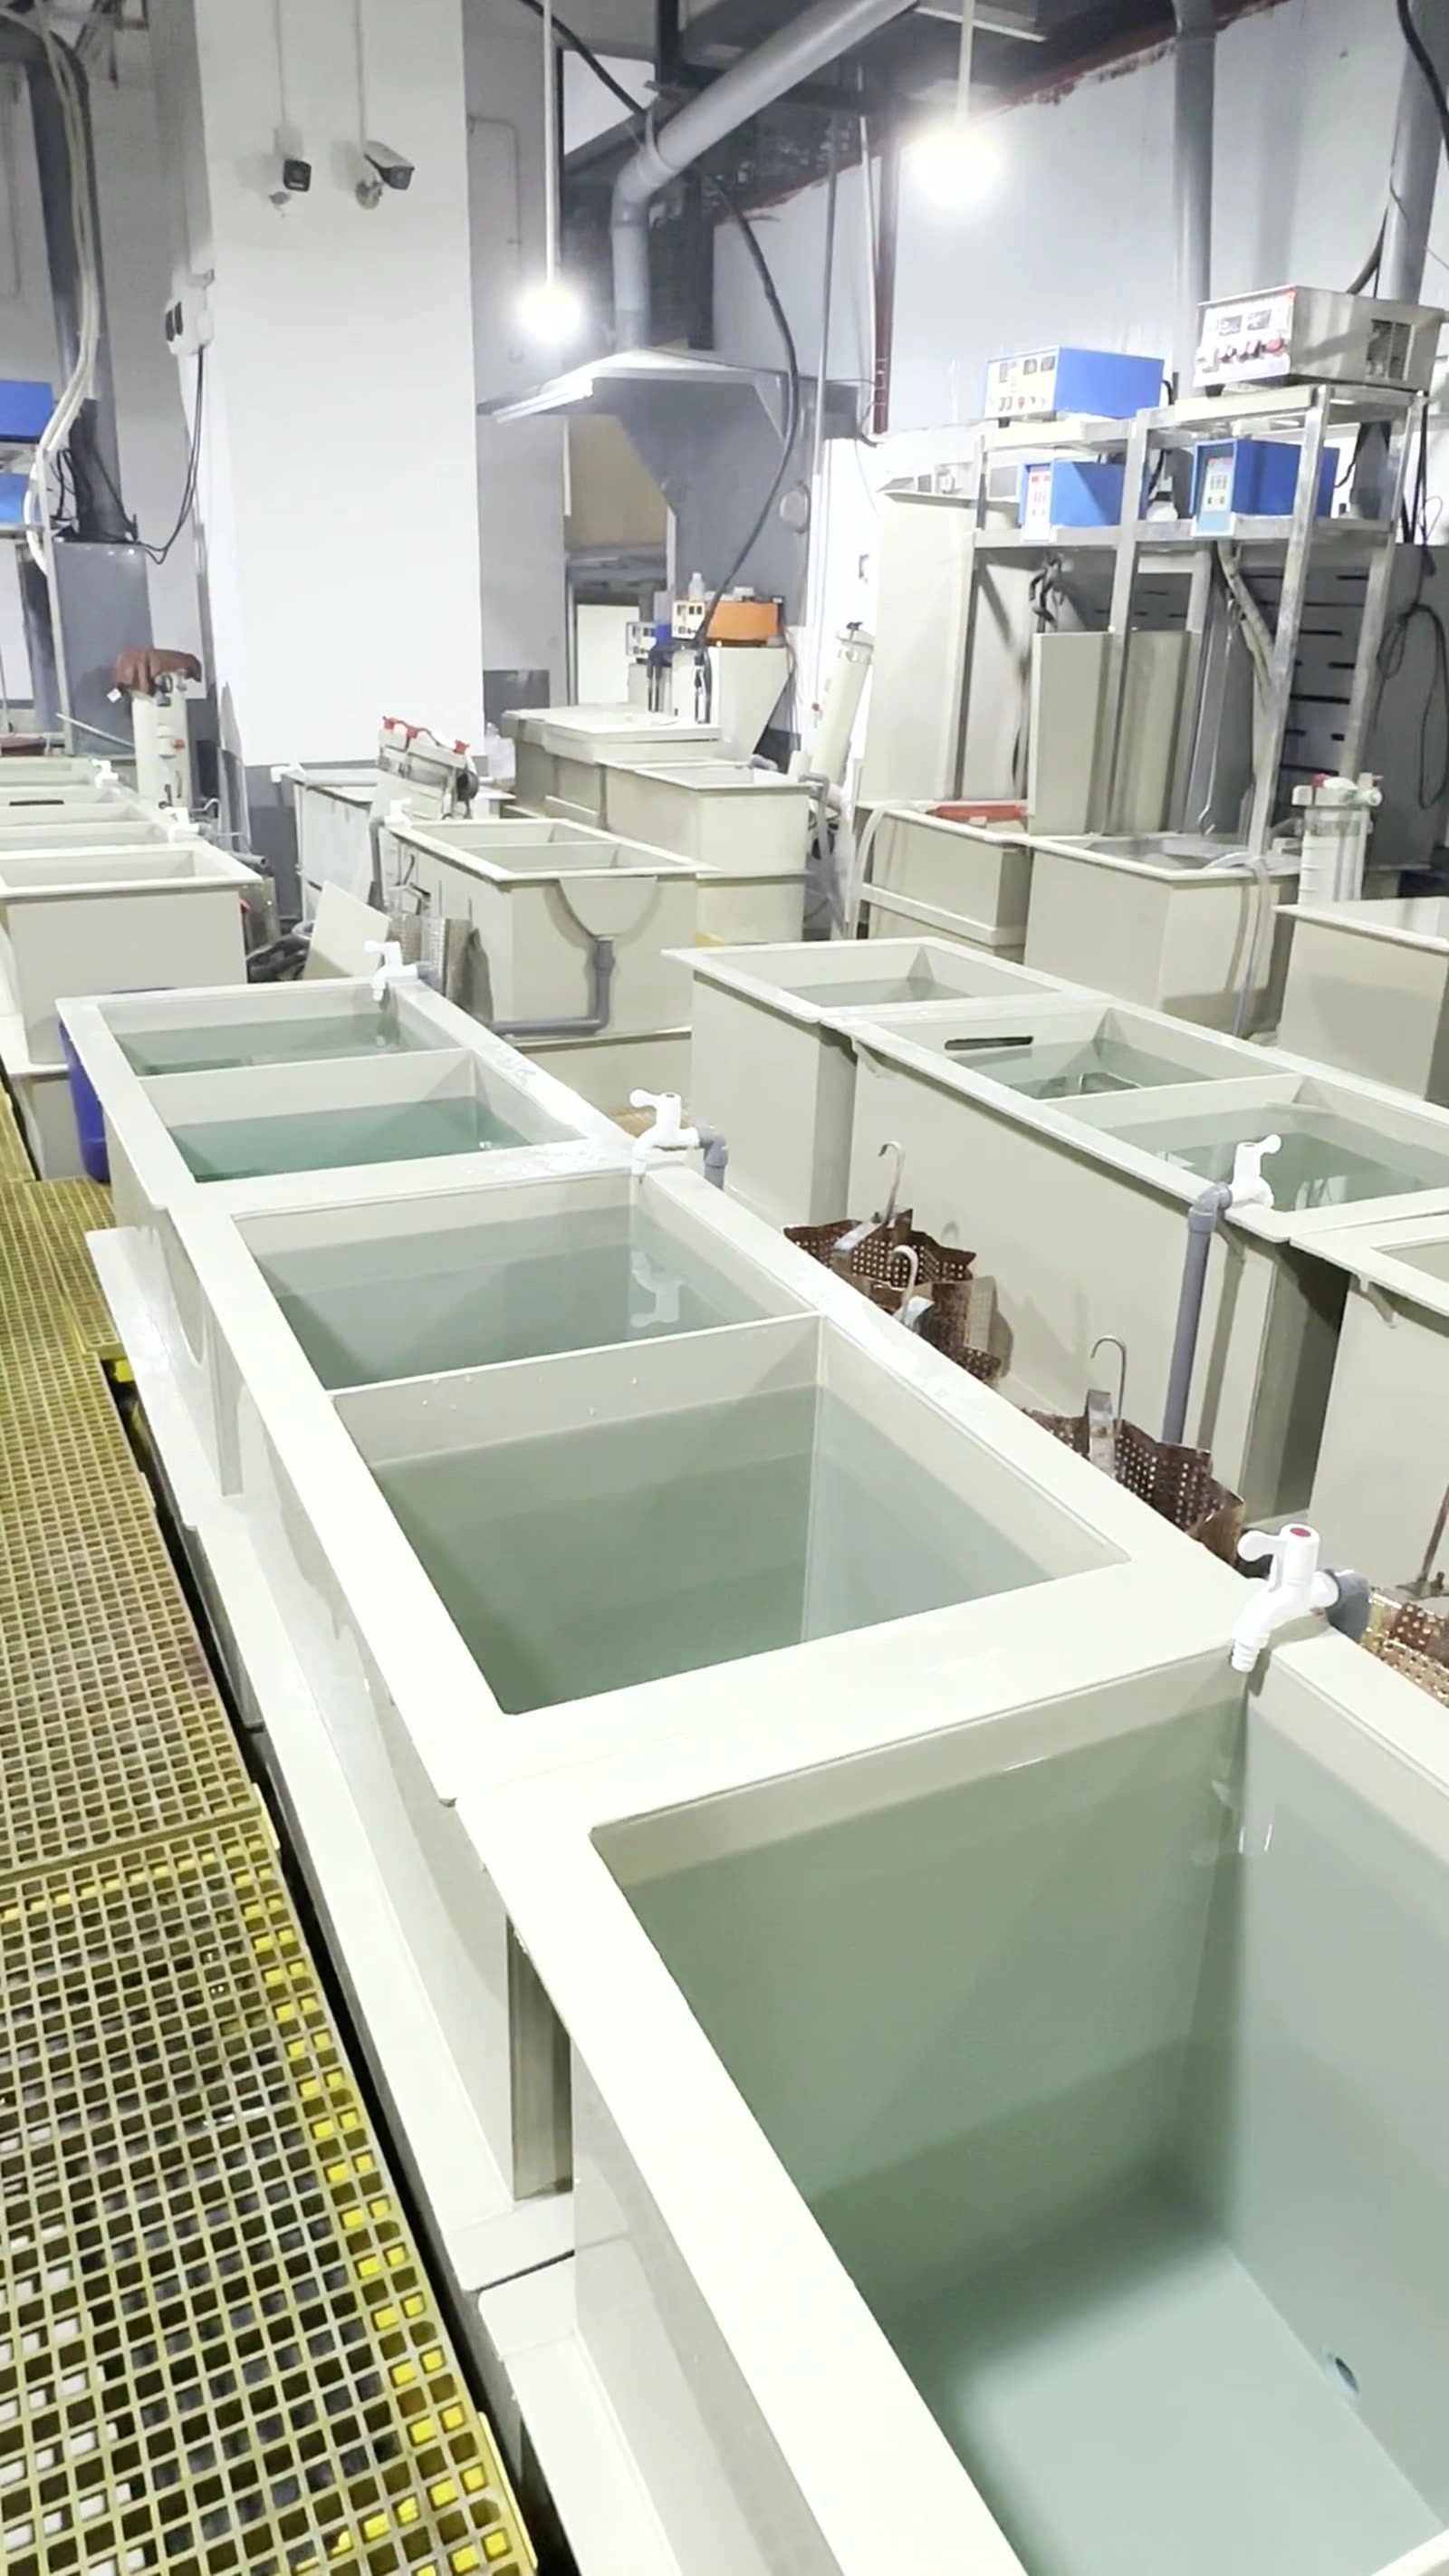
FAQ
Why do bubbles keep appearing after degassing?
Cold resin or over-fast stirring. Warm components and fold slowly; degas again if needed.
Can I speed cure with more hardener?
No — off-ratio leaves uncured resin. Follow kit ratio and raise temperature instead.
Why does the surface stay tacky?
Off-ratio mix or expired pot life. Scale exactly and mix fresh within pot life.