Professional Zinc Alloy Surface Finishing Solutions
Sodium Sulfide
Sodium Sulfide
Buat kode QR
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Sodium Sulfide (Na2S) is the workhorse sulfide donor of the finishing shop - a yellow to reddish-brown flake that hydrolyzes in water to a strongly alkaline solution rich in free S2- ions. In metal finishing it does three distinct jobs: it colors copper and brass into antique brown-black sulfide finishes (the raw chemical behind many proprietary antiquing concentrates), it purifies plating solutions by precipitating heavy metals, and it removes dissolved heavy metals from effluent as extremely insoluble sulfides. In QLQ's finishing plants it supports antique hardware lines for zipper sliders and belt buckles and keeps zinc and nickel process solutions free of copper and lead. Two commercial families are common: standard reddish technical flakes (Na2S ≥ 60%) and low-iron yellow flakes (Fe ≤ 0.005%) which are preferred when a clean, reproducible sulfide color is required - iron in the grade tints the sulfide film and shifts shade. Grades sold for paper pulping or mining flotation are not held to the impurity limits plating and effluent work need, so ask for the low-iron classification by name.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
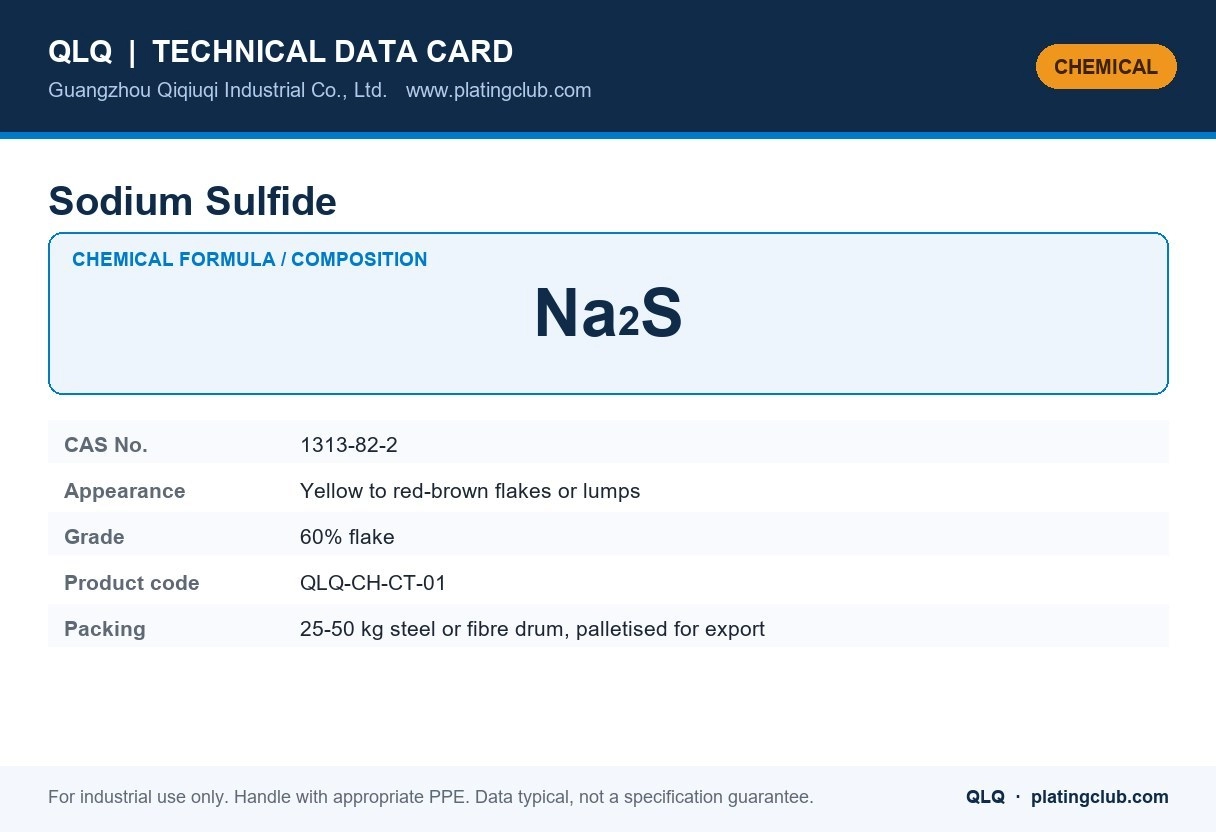
| Chemical name | Sodium Sulfide |
| Chemical formula | Na2S |
| CAS number | 1313-82-2 |
| Appearance | Yellow to red-brown flakes or lumps |
| Grade / type | 60% flake |
| Standard packing | 25-50 kg steel or fibre drum, palletised for export |
What it is and what it does. Sodium sulfide is the classic blackening and antiquing agent for brass, bronze and copper alloys, and it is also used as a component of some colouring and etching solutions.
- Yellow to red-brown flakes; it reacts with copper and silver ions to give the black sulfide film used in antiquing.
- Also used in the colouring of brass hardware and in the treatment of steel before some phosphate processes.
- Strongly alkaline and it releases hydrogen sulfide if acidified - never acidify a sulfide bath.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Brass and bronze blackening | 10-30 g/L at room temperature, 0.5-3 minutes |
| Antiquing for contrast | Short dips, then mechanical relief to highlight the raised areas |
| Rinse | Thorough cold rinse; the film is soft until fully dried |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Toxic with acids (H2S) + corrosive + irritant |
| Personal protective equipment | Goggles, nitrile gloves, dust mask; handle in a ventilated area |
| Spill / first aid | Collect dry; never acidify — hydrogen sulfide gas is released; treat residues as hazardous waste |
| Storage | Dry, sealed store, strictly away from acids; short storage time recommended because of gradual oxidation |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| Why does the colour come out uneven? | Usually an oil film or insufficient activation; degrease and activate the surface first. |
| How do I dispose of the bath? | Never acidify. Oxidise the sulfide with hypochlorite before sending it to the effluent plant. |
| Item | Typical Value |
|---|---|
| Chemical formula | Na2S (flake, hydrated commercial form Na2S·nH2O) |
| Na2S content | ≥ 60% (low-iron yellow flake), ≥ 30% (crystalline nonahydrate) |
| Appearance | Yellow to reddish-brown flakes with typical sulfide odor |
| Iron (Fe) | ≤ 0.005% (low-iron grade); standard grade higher |
| Water insolubles | ≤ 0.1% |
| Solution pH (50 g/L) | > 12 (strongly alkaline) |
| Standard packing | 25KG or 50KG woven bag with PE inner liner |
Where It Is Used in a Finishing Plant
Sulfide coloring is an immersion conversion reaction: S2- reacts with the copper or brass surface to grow a compact cupric-sulfide film whose shade runs from light chocolate to near-black as concentration, temperature or time increases. Because the film follows every contour, recessed detail darkens first and raised surfaces can be highlighted afterward - the classic antique relief look. The same sulfide chemistry does useful purification work: in alkaline and cyanide process solutions, a small test dose of sodium sulfide throws out copper, lead and cadmium as sulfide sludges that are then filtered, leaving the working metal untouched.
| Application | Typical working range | Result / note |
|---|---|---|
| Antique brown-black on copper & brass | 2-10 g/L make-up (start low), 20-45°C, 10-120 s immersion | Chocolate to black sulfide film; depth set by time, temperature and concentration |
| Purification of zinc / process baths | 0.1-0.5 g/L test dose added as 50-100 g/L solution | Cu, Pb, Cd precipitate; settle hot, filter, Hull-cell before production |
| Heavy-metal removal from rinse effluent | Dose matched to metal analysis, pH 8-10 | Sulfide sludges far less soluble than hydroxide sludges |
One warning carries over between all three uses: sulfide must never meet acid. Acidifying a sulfide solution liberates hydrogen sulfide gas instantly, so sulfide coloring tanks, purification additions and sulfide sludge lines are kept physically separate from acid dips and pickles.
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Appearance | Visual inspection of opened bags | Uniform dry flakes, no white carbonate crust, no caked lumps |
| Na2S assay | Iodometric titration of a weighed sample | ≥ 60.0% on the low-iron yellow flake grade |
| Iron content | Supplier COA, spot-check by ICP | Fe ≤ 0.005% for color work; high iron shifts shade muddy |
| Color trial | Fresh 3-5 g/L solution on clean brass panel, 30-60 s at 25°C | Even chocolate-to-black tone; no patchiness, no rainbow |
| Solution clarity | Dissolve 50 g in 1 L DI water | Clear yellow-amber solution; haze points to carbonate or insolubles |
How QLQ controls it: sulfide deliveries are quarantined until the assay and iron figure on the COA match the purchase order, and a small brass test panel is colored with the actual lot before any of it is released to the antiquing line. The lot number follows the drum into the tank record, so a shade complaint can be traced to a single delivery within a day. Only lots that pass all five checks above are accepted.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Patchy or streaky color | Residues or fingerprint soils on the part; solution exhausted or carbonate-loaded | Full alkaline clean + 5-10% sulfuric acid dip before coloring; replenish by titration; renew solution on a schedule |
| Color turns black too fast to control | Concentration or temperature too high | Dilute to 2-4 g/L, run at 20-25°C, shorten dip to seconds and extend by trial |
| Reddish or rainbow patches on brass | Dezincified surface from over-aggressive acid activation; alloy segregation | Shorten acid dip, add inhibitor or use 5% sulfuric only; re-polish and re-activate lightly |
| Film rubs off as dark powder | Over-immersion built a thick, loose sulfide layer | Reduce dip time; a thin dense film survives better; seal all sulfide work with clear lacquer |
| Bath smell or skin irritation in the shop | Acid drag-in reaching the sulfide tank or spills | Neutralize drag-in with a thorough rinse between acid and sulfide; ventilate; never let the two chemistries share a station |
| White crust on tank wall and fading solution | Air oxidation to thiosulfate and carbonate uptake | Keep the tank covered between runs; filter weekly; low-usage tanks are renewed, not patched |
Handling & Safety for the Plating Line
- Alkali burn risk: dissolved sulfide is a strong caustic (pH > 12). Wear splash goggles, neoprene or nitrile gloves and a rubber apron when opening bags, dissolving flakes or handling solutions.
- Hydrogen sulfide (H2S): contact with any acid - even acid drag-in on parts - liberates toxic H2S. Ventilate the sulfide area separately, never position acid dips upwind of it, and treat smell fatigue as a warning that exposure is already dangerous.
- Dissolving: add flakes to water with slow stirring and let the heat of solution dissipate; do not add to hot acid or hot water where boiling can spray caustic solution.
- Storage: keep bags sealed on dry pallets, away from acids, oxidizers and moisture. Damp or CO2-exposed sulfide develops a carbonate crust and loses assay.
- Spills and waste: do not wash sulfide into acid drains - that generates H2S in the sewer. Collect sulfide-bearing solutions and treat with iron salt or oxidize residual sulfide before discharge to meet local sulfide and metal limits.
- First aid: eye splash - flush 15 minutes with water and seek medical attention; skin - remove contaminated clothing and wash thoroughly; report all H2S exposures.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Behavior of sodium sulfide on this substrate | Recommended practice |
|---|---|---|
| Iron / steel small hardware | No sulfide color develops on bare steel - the film needs a copper-bearing surface | Copper- or brass-plate the steel first (acid copper 3-5 μm), then color; steel jigs stay clean but must be rinsed before reuse |
| Zinc alloy (sliders, buckles) | Alkaline sulfide attacks zinc rapidly and stains it grey without a controlled film | Protect with an acid or cyanide copper underlayer before any sulfide coloring |
| Copper / brass | The primary substrates - clean copper reacts to a dense chocolate-black sulfide film | Clean, light acid dip, color in 2-5 g/L solution, rinse, highlight if required, then clear lacquer |
| Stainless steel | Passive surface shows no visible reaction and is not colored | Use stainless only for racks and anodes in sulfide work; do not expect decorative color on it |
FAQ
| Question | Answer |
|---|---|
| Can sodium sulfide color steel parts directly? | No. The sulfide conversion film grows only on copper-bearing surfaces, so steel parts must be copper- or brass-plated first. |
| How is sodium sulfide different from a proprietary antiquing concentrate? | This is the raw, low-cost sulfide donor. Proprietary concentrates add wetting, buffering and stabilization so shade stays repeatable run to run. Shops that already control their own chemistry buy the flake and titrate it themselves; others prefer a concentrate. |
| Why is my antique shade different every morning? | Check three variables: sulfide concentration by titration, solution temperature, and immersion time. Carbonate buildup from air exposure also slows the reaction - renew the solution on a fixed schedule. |
| Can I use sodium sulfide to purify my zinc bath? | Yes, copper, lead and cadmium are precipitated as sulfides. Dose by test (0.1-0.5 g/L), never by guess - an overdose precipitates zinc and empties the bath of metal. |
| Does QLQ supply low-iron sodium sulfide with technical support? | Yes. Each lot ships with COA covering assay and iron, and QLQ engineers help with sulfide coloring recipes, purification dosing and effluent treatment for customers in 10+ countries. |
Setting up an antique line or a bath purification program? QLQ supplies low-iron sodium sulfide with COA and helps customers in 10+ countries size doses, build sulfide-safe tank layouts and train operators. Contact us with your bath analysis.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.