
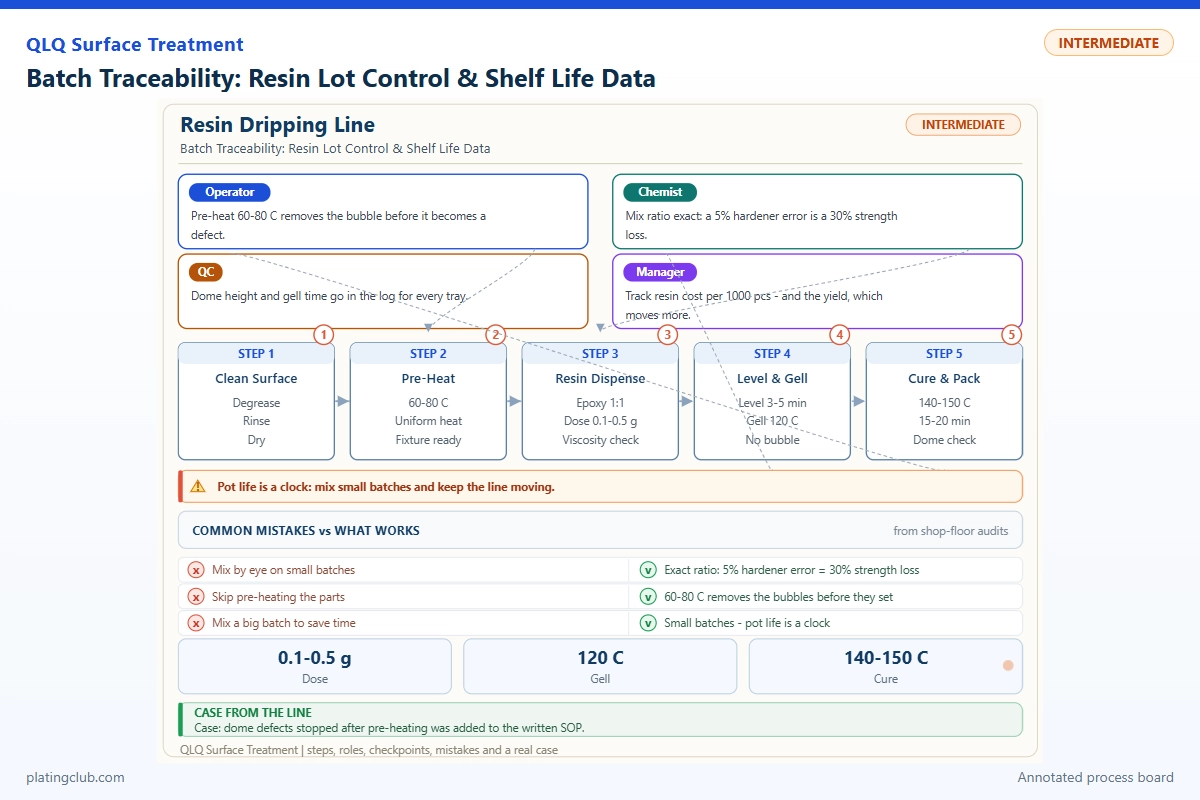
RESIN DRIPPING / SENIOR TECHNICAL PRACTICE
Batch Traceability: Resin Lot Control & Shelf Life Data
A resin dome on plated zinc-alloy bag hardware is a small coating with a large traceability burden. A soft surface, cloudy interface, or delayed edge lift may originate in the hardener container, metering circuit, plating rinse, cleaning operation, or loaded cure rack. Senior technicians need records that distinguish these causes, not merely a supplier lot number written beside the production order.
This guide covers two-component decorative resin dripping. Epoxy, polyurethane, silicone, and PVC processes are not interchangeable. The QLQ local equipment catalogue identifies separate silicone and PVC dispensing systems; it does not establish an epoxy recipe or shelf-life qualification. Do not transfer settings between those chemistries.
Evidence boundary: no authenticated QLQ resin-lot experiment or customer failure report was available for this article. Published supplier results below are reference data, not factory trial results. Proposed operating bands and investigation scenarios require site validation. Pending measurements are explicitly identified rather than replaced with invented values.
1. Build genealogy around the mixed batch
Give every container a unique identity even when several containers share one supplier lot. Record product code, A or B designation, supplier lot, container serial, manufacture date, labelled expiry, receipt date, seal condition, certificate reference, and storage location. Photograph damaged packaging before acceptance. Release each component independently; an acceptable A container does not release an unverified B container.
The mixed-batch record must join both container identities to the weighing record, operator, mixing start, mixer identity, recipe revision, and dispensing interval. Link that batch to hardware casting lot, plating order, cleaning record, tray positions, cure history, inspection results, and shipment carton range. Pigment or primer needs its own lot link if used.
A useful identifier is RD-20261011-S2-M003: process, date, shift, and mixed-batch sequence. This is an illustrative naming scheme, not an actual production lot. Never overwrite an identifier after rework. Create a child record that retains the original parent, disposition, and additional cure or cleaning operation.
Tank topping-up creates overlapping genealogy. Prefer an empty-and-clean changeover where practical. Otherwise log remaining mass, incoming mass, and the transition interval; quarantine the entire potentially mixed population if either lot fails. A software timestamp cannot locate the boundary accurately unless hose volume, tank mixing, and purge behaviour are known.
2. Working formulation and replenishment rules
The complete shop-floor formulation below uses a supplied two-part system; it is not a disclosed chemical synthesis recipe. Parts A and B already contain the manufacturer's proprietary ingredients. No solvent, pigment, accelerator, or defoamer is authorised in this baseline. Adding one requires a separately qualified formulation revision.
| Component | Range | Typical | Function | Replenishment |
|---|---|---|---|---|
| 308A-3S1 supplied main agent | 75.00 g fixed target per 100 g mix | 75.00 g | Resin component | Refill A circuit only with released, traceable material. |
| 308B-3S0 supplied curing agent | 25.00 g fixed target per 100 g mix | 25.00 g | Curing component | Refill B circuit separately; check its own expiry. |
| Added pigment, filler, solvent, water, or accelerator | 0 g in this baseline | 0 g | No additional function authorised | Never replenish a mixed cup or dilute ageing resin. |
| Total | 100.00 g target; measurement tolerance separately validated | 100.00 g | Complete dispensing mixture | Prepare a new batch with a new start time. |
The supplier specifies 3:1 by mass and 2.7:1 by volume. These are different metering instructions. The 75/25 split is calculated from the mass ratio. Use the exact product's approved ratio, not this example, for another resin. Source: 308AB-3S1 technical data sheet.
Check balance resolution against the smaller component. Separately collected A/B shots provide a ratio check only through a safe supplier-approved calibration method. Define relative ratio error as 100 × [(measured A/B ÷ target A/B) − 1]. A 1% relative ratio error is not the same as one percentage point of hardener concentration.
3. Shelf life is three clocks, not one date
Control unopened shelf life, opened-container service life, and mixed-resin working time separately. A container may remain inside its printed expiry while its opening history makes it unacceptable. Conversely, a cured product's service life is not the resin container's shelf life.
For 308AB-3S1, the sheet states six months in original packaging and recommends 15–25°C storage. Its 100 g pot-life reference is 50 ± 5 minutes at 25°C. It does not establish a universal opened-container allowance. Obtain written supplier guidance rather than assigning an arbitrary “30 days after opening” rule. Supplier storage and working-time reference.
Use the earliest applicable approved expiry across A, B, and other ingredients. First-expiring-first-out is more useful than receipt-date order. Do not recalculate a supplier expiry from receipt date. When storage exceeds a recommended band, preserve temperature and duration records and place the container on hold pending a documented assessment.
Requalification needs a written protocol and authorised disposition. A satisfactory hardness result alone does not justify extending expiry: appearance, adhesion, flow, and durability may behave differently. Never blend expired material into fresh material to conceal its age. Retain sealed component samples and cured witnesses under a retention schedule linked to customer and warranty obligations.
4. Trend normal bands against action thresholds
These are proposed commissioning controls, not universal resin specifications. Only the cited material-property values are supplier references. Approve the other bands through trials on the actual plated construction. Between a normal band and a stop threshold, investigate and increase sampling; crossing a stop threshold means holding affected output, not merely adjusting a display.
| Parameter | Normal fluctuation band | Danger / hold threshold | Response and basis |
|---|---|---|---|
| A/B mass-ratio relative error | Within ±1% of approved target | Outside ±2%, or identity uncertain | Proposed limits; stop and recalibrate both deliveries. |
| Component temperature during metering | 23–27°C around a 25°C qualification point | Below 20°C or above 30°C | Proposed process limits; condition sealed material and recheck flow. |
| Local relative humidity | 45–65% RH proposed | Above 75% pending investigation | Conservative site alarm; qualify humidity sensitivity independently. |
| A viscosity at 25°C | 550–750 mPa·s | Outside that reference range | Supplier reference; confirm instrument setup before material disposition. |
| Mixed viscosity at 25°C | 150–250 mPa·s at a fixed early sampling time | Outside the band at that same time | Supplier reference; compare equally aged samples, not fresh versus old cups. |
| Elapsed mixed-batch time | 0–30 minutes proposed production window | Above 40 minutes in the qualified 100 g setup | Internal safety margin, not a supplier pot-life guarantee. |
| Shot mass versus qualified target | Within ±3% | Outside ±5% | Proposed limits; hold since last verified shot and inspect profile. |
| Remaining shelf life | More than 30 days: planning preference | Label expiry reached, or opened-life approval absent | Thirty days is a scheduling trigger, not evidence of degradation. |
The cited viscosity ranges belong only to 308AB-3S1. Viscosity reference and measurement temperature. Do not introduce aqueous-bath pH limits into a nonaqueous resin record. Where humidity rises, separate condensation, interface contamination, and entrained air before deciding on degassing or heat treatment.
5. Experimental data: separate references from lot qualification
Published hardness can guide resin selection but cannot release a factory lot. The reference comparison below contains actual supplier-reported typical values; neither supplier discloses the underlying lot identities here. It is not a controlled head-to-head experiment.
| Material / sample status | Film or dome thickness | Hardness | Salt-spray result | Test condition |
|---|---|---|---|---|
| 308AB-3S1; supplier typical result | Not reported for hardness specimen | Shore A 58–72 | Not reported | Sheet references 25°C / 70% RH laboratory conditions; hardness cure age and specimen geometry unspecified. |
| 618AB-18; supplier typical result | Manual process describes approximately 2 mm; not identified as hardness specimen thickness | Shore A 70 ± 5 | Not reported | Sheet references 25°C / 65% RH typical testing; hardness-specific cure history unspecified. |
Sources: epoxy test results and polyurethane test results. Do not convert Shore A to Shore D or treat a reading through a thin dome onto metal as a valid bulk-hardness measurement.
| Trial group | Thickness result | Hardness result | Corrosion / adhesion result | Test condition |
|---|---|---|---|---|
| Fresh released A/B reference pair | Pending | Pending | Pending | Same plating lot; 25 ± 2°C; 50 ± 10% RH; five hardware coupons plus separate compliant hardness specimens. |
| Near-expiry A with reference B | Pending | Pending | Pending | Identical cleaning, target dose, cure schedule, measurement age, and agreed corrosion exposure. |
| Reference A with near-expiry B | Pending | Pending | Pending | Same conditions; trace each container's opening and storage history. |
| Near-expiry A/B pair | Pending | Pending | Pending | Same conditions; record individual values, mean, spread, photographs, and disposition. |
Measure dome height by optical profile or cross-section at agreed locations; distinguish centre height from minimum edge coverage. Prepare hardness specimens with the geometry and conditioning required by the selected method. Freeze cure age before comparison. Include bare plated controls to separate plating corrosion from resin-interface failure. Define corrosion exposure duration, scribing, edge masking, and pass criteria with the customer before testing. Salt-spray hours alone are not a service-life prediction.
6. Two investigation scenarios for senior technicians
Scenario A: softness follows one hardener container
This is a diagnostic scenario, not a documented customer case. Two trays share plating and cure conditions, but softness begins after a B-container change. Freeze shipment and reconstruct the exact transition population. Verify component identity and separate delivery masses first. Then compare retained reference A with old and new B using the experiment sheet. If the difference follows B under controlled conditions, retain both containers and request supplier investigation; do not compensate by increasing hardener.
Scenario B: edge lift follows a plating rack
This second scenario is also hypothetical. Several resin lots fail only on hardware from one finishing rack. Cross the suspect substrate against a released substrate using one verified resin pair. Preserve cleaning and rinse records, handling history, and surface photographs. A failure that follows substrate warrants interface investigation before resin rejection. Report measured adhesion and corrosion observations separately; neither visual clarity nor hardness proves substrate bonding.
7. Engineer Notes
- Scan both container IDs before weighing; block dispensing if either release status is missing.
- Check the balance with appropriate verification weights and save the check before the first batch.
- Collect separate component deliveries only through an approved procedure; record actual masses rather than pump settings alone.
- Start the mixed-material timer at first A/B contact, including mixer residence and production pauses.
- Label retained samples immediately with genealogy, cure start, rack position, and inspection age.
- After a lot change or prolonged pause, verify ratio, shot mass, and a cured witness before restarting unrestricted output.
- Use the current component SDS for gloves, ventilation, cleaning, and waste handling; do not choose solvents from a generic resin article.
8. Shift Checks
| Shift stage | Check item | Frequency | Acceptance standard | Record |
|---|---|---|---|---|
| Before shift | Container identity, expiry, release, seal | Every container and changeover | Correct approved A/B pair; no unresolved hold | Scans, opening history, release signature |
| Before shift | Balance, ratio, component temperature | Startup and recipe change | Verified instruments and validated operating bands | Check weights, shot masses, sensor IDs |
| During shift | Shot mass, mixed age, local conditions | Each batch; shot checks every 30 minutes and restart | No exceeded approved action limit | Time-stamped trend and output range |
| During shift | Profile, bubbles, substrate genealogy | First-off and every tray | Approved appearance and profile specification | Tray map, photographs, defect count |
| After shift | Cure history and witness tests | Each cure load at defined test age | Qualified cure and inspection requirements met | Temperature log, measured results, disposition |
| After shift | Container closure, mass reconciliation, WIP holds | Every circuit and open container | Sealed, labelled, reconciled; no unidentified output | Stock balance, waste, hold list, handover |
9. Technician questions to ask AI
These are suggested direct prompts, not quotations from authenticated customer messages.
“AI, my resin is still inside its expiry date, but the hardener was opened last month. Can I use it?”
Check the exact product's approved opened-container limit and exposure history. Printed shelf life does not automatically cover repeated opening. Without an authorised opened-life rule, hold the container and request written supplier guidance plus the appropriate qualification tests.
“AI, hardness is normal but resin edges lift after corrosion testing. Is the resin lot bad?”
Not necessarily. Compare the suspect substrate with a released substrate under one verified resin pair, and compare resin pairs on one substrate lot. Keep cleaning, thickness, cure age, and exposure conditions fixed. Hardness describes one property; it does not identify an interface failure's cause.
“AI, can I add fresh resin to an old mixed cup and reset the pot-life timer?”
No. Fresh material does not reverse the older fraction's reaction history. Stop using material beyond the qualified working window, dispose of it under the approved procedure, and prepare a new traceable batch. A new container label cannot reset chemical age.
10. What Would You Like to Solve?
For a focused engineering review, send the resin product codes, both lot IDs, expiry and opening dates, storage excursions, plated substrate construction, ratio checks, cure records, and actual test results to [email protected]. Identify the first affected tray and last known acceptable tray. For coordinated equipment, chemistry, and process support, see turnkey surface-treatment lines and technical support.
Local knowledge-base source: QLQ Obsidian Vault, equipment catalogue page 25, silicone and PVC dispensing sections. That source supports chemistry separation only; it does not supply the epoxy measurements above. Supplier references are product-specific, and factory release still requires completed, traceable qualification records.