Professional Zinc Alloy Surface Finishing Solutions
Copper Sulfate
Copper Sulfate
Luo QR-koodi
-
Estimated Delivery:Oct 02 - Oct 06
-
Free Shipping & Returns: On all orders over $75
Product description
Shipping & Return
Product Overview
Copper Sulfate (CuSO4·5H2O) - blue vitriol - is the main salt of the acid copper plating bath, the workhorse that lays down the level, bright copper underlayers under nickel-chrome on zinc die cast and steel, and the thick builds used in electroforming and rotogravure. In QLQ's finishing plants acid copper from copper sulfate produces the smooth undercoats that make zipper sliders and belt buckles look like jewelry instead of stampings. The commercial market sells many grades: plating grade (crystal, low iron and chloride, essentially free of organic residue), agriculture and feed grades, and even crude industrial material. Only the plating discipline matters here - copper sulfate is judged by what is not in it. Iron above a few hundred ppm dulls and hardens the deposit and slows the bath, chloride shifts the delicate chloride balance that proprietary brighteners need, and organic residue roughens and hazes. A bright acid copper bath is an additive machine with a narrow tolerance, and its fuel must be clean.
Product Identity (Encyclopaedia Card)
| Property | Value |
|---|---|
| Chemical name | Copper Sulfate |
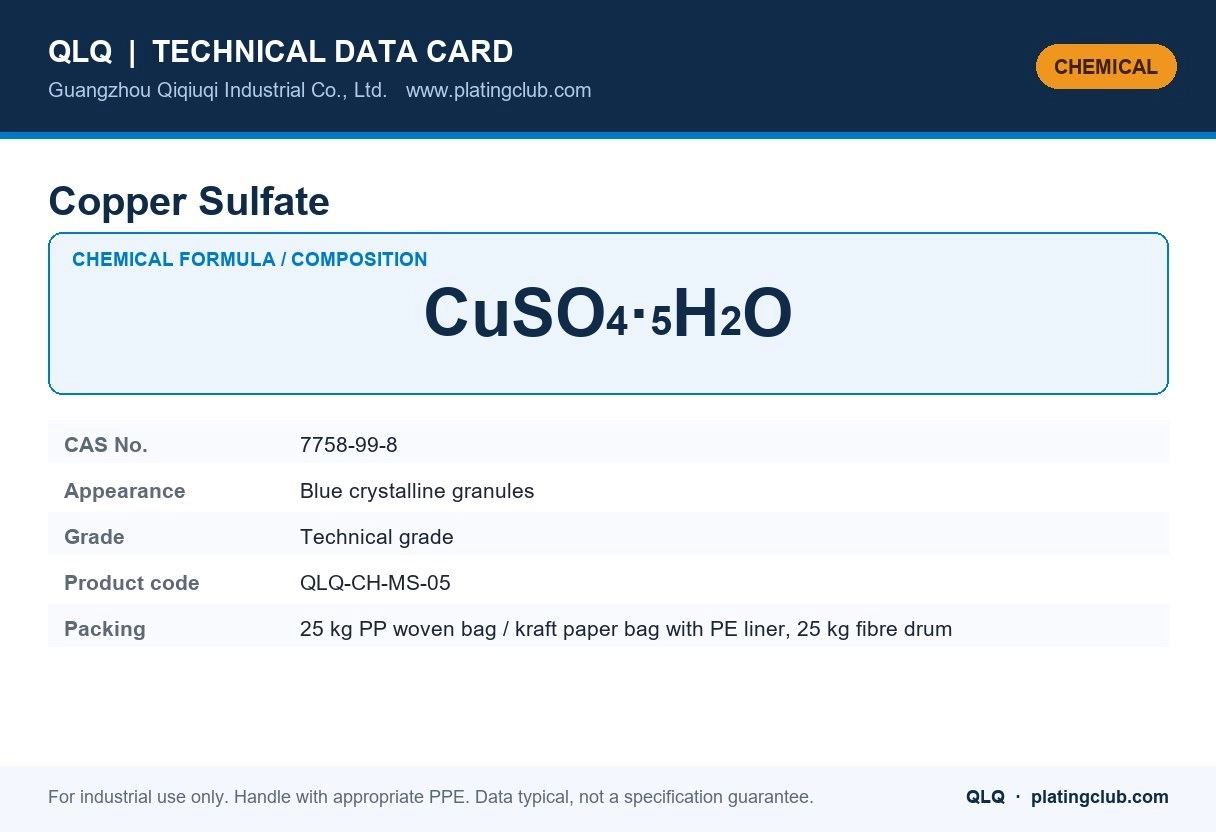
| Chemical formula | CuSO4·5H2O |
| CAS number | 7758-99-8 |
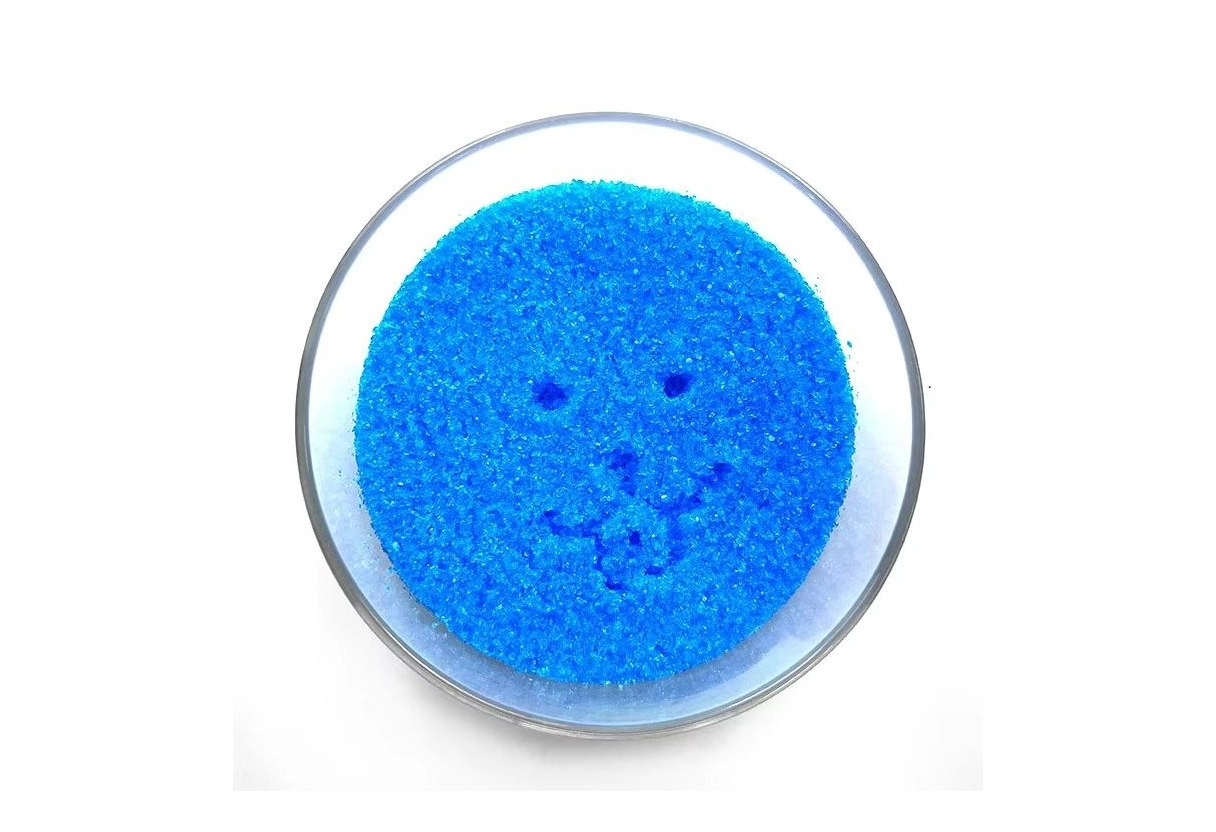
| Appearance | Blue crystalline granules |
| Grade / type | Technical grade |
| Standard packing | 25 kg PP woven bag or kraft paper bag with PE inner liner; 25 kg fibre drum |
What it is and what it does. Copper sulfate is the general technical grade copper salt used for acid copper plating, for making up copper anode films, for antiquing solutions and for copper recoating of damaged plating racks.
- The familiar blue crystal; the same substance as the pentahydrate product, offered here in the general technical grade and in a wider range of pack sizes.
- Used to prepare the copper complex for antiquing and for thin protective copper layers on steel before nickel.
- Copper ions are toxic to aquatic life, so spent solutions go to the effluent treatment plant and never to drains.
Typical Use in a Plating / Finishing Line
| Item | Typical guidance |
|---|---|
| Acid copper make-up | 180-250 g/L depending on the metal content required |
| Antiquing / colouring | As specified by the colouring formulation |
| Analysis | Copper by titration; iron contamination should stay below about 1 g/L |
Safety, Handling & Storage
| Item | Requirement |
|---|---|
| Hazard classification | Harmful / toxic (GHS06/08 depending on the metal) + skin sensitiser |
| Personal protective equipment | Nitrile gloves, goggles, dust mask, coverall; no eating or smoking in the work area |
| Spill / first aid | Sweep up dry, place in a labelled drum, rinse the area; do not discharge metal-bearing solution to drains |
| Storage | Dry, ventilated store, keep bags closed; segregate from acids, oxidisers and food; keep a COA and an MSDS with each batch |
| Transport | Classified and packed according to IATA/IMDG for the hazard class; UN number and packing group stated on the shipping documents |
Quality Documents Shipped With Every Batch
| Document | Comment |
|---|---|
| COA (certificate of analysis) | Provided with the shipment; batch traceable to the production date |
| MSDS (safety data sheet) | Provided with the shipment; batch traceable to the production date |
| Packing list | Provided with the shipment; batch traceable to the production date |
| Commercial invoice | Provided with the shipment; batch traceable to the production date |
| Certificate of origin on request | Provided with the shipment; batch traceable to the production date |
Buyer Questions We Answer Every Week
| Question | Answer |
|---|---|
| What is the difference from the pentahydrate listing? | Same substance; this grade is offered for general technical use rather than for plating-critical baths. |
| Does copper sulfate harm the wastewater plant? | Copper must be precipitated with hydroxide or sulfide in the treatment plant; it cannot be discharged as a metal ion. |
| Item | Typical Value |
|---|---|
| Chemical formula | CuSO4·5H2O (copper sulfate pentahydrate) |
| Copper (Cu) content | ≥ 25.0% (≈ 25.5% theoretical) |
| Appearance | Bright blue crystals, free-flowing, no efflorescence |
| Iron (Fe) | ≤ 0.005% |
| Chloride (Cl) | ≤ 0.001% (must not disturb bath chloride balance) |
| Water insolubles | ≤ 0.005% |
| Standard packing | 25KG woven bag with PE inner liner |
How It Works in the Bath (Acid Copper Chemistry)
Acid copper is a two-component electrolyte: copper sulfate supplies the metal ions that plate out, and sulfuric acid supplies conductivity and keeps the bath stable while suppressing the copper-ion concentration at the cathode so the deposit levels and brightens under the additive system. In the classic decorative bath the make-up is roughly 200 g/L copper sulfate and 60-80 g/L sulfuric acid, with 40-80 mg/L chloride and the supplier's brightener/leveler package; high-throw formulations used in PCB work invert the ratio (low copper, 180-220 g/L acid) to plate deep holes evenly. Air agitation and continuous filtration are not optional - acid copper is dead without them, because the brightener depends on strong, uniform solution movement. Anodes are phosphorized copper (about 0.03-0.06% phosphorus), which dissolve cleanly and leave a black film that holds back anode sludge instead of releasing particles that roughen the deposit.
| Component | Decorative rack bath | High-throw / PCB bath |
|---|---|---|
| Copper sulfate (CuSO4·5H2O) | 180-220 g/L | 70-100 g/L |
| Sulfuric acid | 60-90 g/L | 180-220 g/L |
| Chloride | 40-80 mg/L | 40-80 mg/L |
| Brightener / leveler / carrier | per supplier, maintained by analysis and Hull cell | |
| Temperature | 20-30°C | 20-28°C |
| Cathode current density | 2-6 A/dm² (with air) | 1-4 A/dm² |
The same salt serves the alkaline (cyanide) copper line only as a source for making up copper cyanide concentrate - it is never added to a cyanide bath directly, because acid salts liberate hydrogen cyanide gas in cyanide solution.
How to Check Quality Before Loading a Batch
| Check | Method | Pass Criteria |
|---|---|---|
| Appearance | Visual | Uniform bright blue; pale, white-spotted or dusty crystal signals efflorescence or contamination |
| Copper assay | Iodometric titration or AA | ≥ 25.0% Cu |
| Iron | COA figure or thiocyanate test | Fe ≤ 0.005%; iron dulls and hardens deposits |
| Chloride | Silver nitrate on a 10% solution | No precipitate beyond faint haze (Cl ≤ 0.001%) |
| Hull cell trial | Make up a lab bath with the lot; plate at 2-4 A | Bright range, leveling and color reproduced with standard additives |
How QLQ controls it: copper sulfate lots are quarantined until the copper, iron and chloride figures on the COA match the purchase order, and a Hull cell panel confirms the lot plates identically to the retained standard before it is released. The lot number goes into the make-up record, so a leveling or brightness change can be traced to the salt in a day.
Common Problems & Fixes (Workshop Table)
| Problem | Root cause | Fix |
|---|---|---|
| Rough, gritty copper deposit | Anode sludge or insolubles from the salt entering the bath | Check anode bags, filter to 5 μm, verify salt insolubles |
| Dull copper, poor leveling | Additive imbalance, chloride off-range, or iron contamination | Hull cell; analyze chloride and brightener; carbon-treat and rebuild; check salt iron |
| Burnt, powdery high-CD areas | Copper metal too low, acid too high, agitation weak | Raise copper sulfate to range; reduce acid; increase air agitation |
| Immersion deposit (pink flash) on make-up | Plating onto bare steel/zinc without a strike in acid copper | Apply cyanide copper or copper strike before acid copper; never acid-copper directly on steel |
| Bath loses brightness between shifts | Organics building from brightener breakdown | Carbon treat 2-5 g/L on schedule; continuous filtration; peroxide treatment if needed |
Handling & Safety for the Plating Line
- Health: copper sulfate irritates eyes, skin and airways; it is harmful if swallowed. Wear gloves, goggles and a dust mask when handling crystals and making up solution.
- Dissolving: copper sulfate dissolves readily in warm water (about 30-40°C) with stirring; do not boil. Acid is added to the diluted salt solution - never water into acid.
- Effluent: copper is tightly regulated in rinse water (typically ≤ 0.5-2 mg/L discharge limits). Collect spills and spent solutions as copper-bearing waste; do not hose to drain.
- Storage: keep bags sealed and dry. The pentahydrate effloresces in dry air and cakes in damp air - either way weighing accuracy suffers.
- Cyanide rule: never allow acid copper solution near cyanide baths or cyanide waste - mixing acid with cyanide liberates hydrogen cyanide gas.
What It Does on Iron, Zinc Alloy, Copper and Stainless Steel Parts
| Substrate | Role of the acid copper layer from this salt | Recommended practice |
|---|---|---|
| Iron / steel small hardware | Levels substrate defects before nickel so the final finish looks plated, not stamped | Use a cyanide or copper strike first - acid copper on bare steel gives non-adherent immersion deposits |
| Zinc alloy (sliders, buckles) | The classic die-cast route: copper seals the active zinc, acid copper levels, nickel-chrome decorates | Strike copper thin and bright, build in acid copper 8-15 μm, then nickel-chrome |
| Copper / brass | Leveling and brightening directly on copper alloys for decorative work | Clean and activate briefly; acid copper builds straight onto copper with full brightness |
| Stainless steel | Copper layers are applied after an adhesion strike when nickel-chrome must not touch stainless directly | Nickel strike (Woods) first, then acid copper; keep stainless racks out of the copper bath |
FAQ
| Question | Answer |
|---|---|
| Why can't I acid-copper directly on steel parts? | Acid copper deposits by displacement on steel - a loose pink immersion film instead of an adherent plate. A cyanide copper strike or a copper strike bath is the necessary bridge. |
| How much copper sulfate do I add when copper is low? | Raise 10 g/L of CuSO4·5H2O adds about 2.5 g/L of copper metal; confirm by titration and Hull cell rather than by arithmetic alone. |
| Is agriculture-grade copper sulfate acceptable? | No for bright work. Its iron, chloride and organic residues disturb the additive balance; plating-grade crystal is priced for that reliability. |
| Why does my acid copper need chloride when the salt spec says low chloride? | The two limits serve different purposes: chloride in the salt is an impurity risk to the balance you set, while 40-80 mg/L chloride deliberately added in the bath is an essential partner to the brightener. |
| Does QLQ supply plating-grade copper sulfate with support? | Yes. QLQ supplies copper sulfate with COA covering copper, iron and chloride, and engineers help with acid copper make-up, additive balance and troubleshooting. |
Acid copper rough, dull or not leveling? QLQ supplies plating-grade copper sulfate with COA and engineers who help customers in 10+ countries run decorative and high-throw copper lines. Contact us with your Hull cell panels.
Shipping cost is based on weight. Just add products to your cart and use the Shipping Calculator to see the shipping price.We want you to be 100% satisfied with your purchase. Items can be returned or exchanged within 30 days of delivery.