

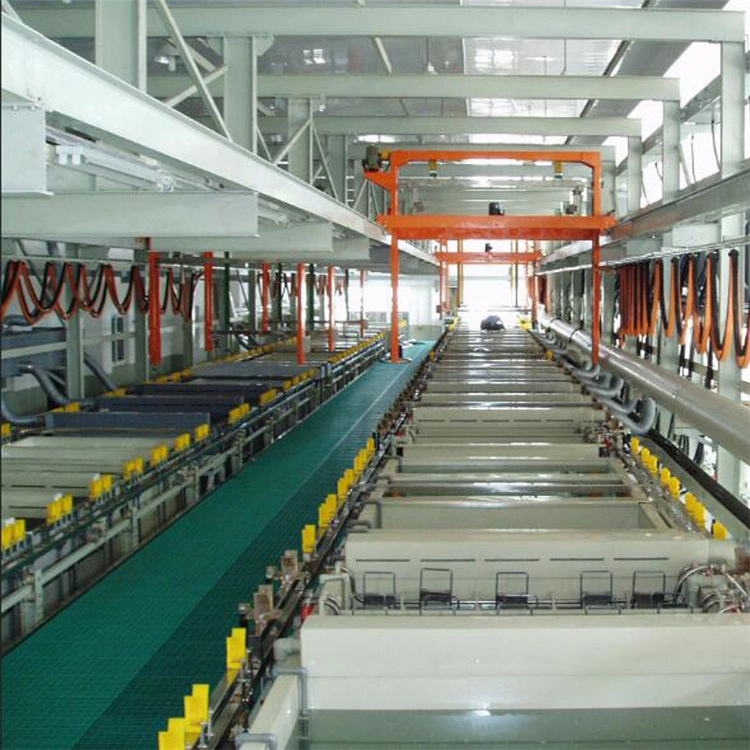
Rupture marks and orange peel appeared in the same batches, and the paint supplier found nothing in the bath. The fault sat at the interface between the bath and the UF rinse chain.
This senior guide traces that interface: drag-in, permeate quality, rinse staging and the logs that separate bath faults from rinse faults.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Bath only blamed | Interface missed | Sample bath and rinses |
| 2. Permeate never checked | Contaminated rinse | Measure conductivity per stage |
| 3. One rinse stage cut | Drag-in peaks | Keep the counterflow chain |
| 4. Permeate flow low | Rinse starvation | Check UF flux |
| 5. Temperature drift | Solvent and pH shift | Control bath temperature |
| 6. Solvent control ignored | Rupture on parts | Track solvent percentage |
| 7. Rinse water too cold | Poor wetting | Hold the rinse temperature window |
| 8. No cross-sample | Fault side hidden | Sample before and after each stage |
| 9. Logs not correlated | Cause unprovable | Correlate bath and rinse logs |
Best Practices
- Sample the bath and each UF stage in one go
- Track permeate conductivity per stage
- Keep the counterflow rinse chain intact
- Control bath temperature and solvent level
- Correlate bath and rinse logs daily
- Section and surface-check failed parts
Implementation Roadmap
| Step | Frequency |
|---|---|
| Cross-sample | Per fault event |
| Permeate check | Per shift |
| Rinse stage review | Weekly |
| UF flux check | Monthly |
| Log correlation | Daily |
Rupture and orange peel trace flow
- Sample - Bath and all rinse stages. (One sample hides the fault.)
- Measure - Conductivity, pH, solvent. (Specs differ per stage.)
- Correlate - Match faults to logs. (Unlogged data proves nothing.)
- Fix one - Rinse or bath variable. (Two changes unprovable.)
Rupture follows solvent or gas breakout at the film surface. | Orange peel follows surface tension and wetting faults.
Bath-interface and UF rinse data
Reference values for e-coat bath interface and UF rinse control.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Bath solids | 15-20% | Feed per consumption |
| Bath pH | 5.8-6.4 | Drift shifts the rupture window |
| Bath conductivity | 25-60 µS/cm | Per product target |
| Voltage | 120-250 V | High voltage plus solvent equals rupture |
| Rinse stages | 3-4 counterflow | First rinse removes drag-in |
| Permeate conductivity | Per stage target | Rising trend means contamination |
| Rinse temperature | Per product window | Cold water hurts wetting |
| Solvent content | Per product | Track and dose |
UF rinse chain check
| Stage | Check | Action |
|---|---|---|
| 1 (dip) | Drag-in heaviest | Maximize overflow |
| 2 (spray) | Conductivity trend | Adjust the flow |
| 3 (fresh) | Near feed quality | Change membrane if high |
| Permeate | Flux and quality | Clean or replace UF |
Case 1 - rupture and orange peel traced to a starved first rinse
Scenario. A line ran rupture and orange peel together for a month; bath analysis passed and the supplier offered a new resin, but the faults followed load position, not batch.
Action. Cross-samples showed the first UF rinse at three times the target conductivity; permeate flow had dropped and the first stage carried all the drag-in.
Result. The UF membrane was cleaned, permeate flow recovered, and rinse staging was restored; rework fell 30% and the bath stayed untouched.
Case 2 - a solvent spike from a weekend temperature drop
Scenario. An agricultural equipment plant saw ruptures every Monday batch; parts failed only after the weekend shutdown.
Action. The log correlated the faults to a 6°C bath temperature drop that shifted solvent balance; a weekend recirculation rule was added.
Result. Monday ruptures stopped; the temperature and solvent log now gates the restart.
Frequently Asked Questions
What is e-coat rupture?
A film break caused by solvent or gas breakout during deposition or cure, leaving crater-like marks.
Why rupture and orange peel together?
Both trace to surface and interface conditions - solvent balance, wetting and rinse quality.
Why suspect the rinse chain?
The bath interface includes drag-in; a contaminated rinse changes the film surface before cure.
How do I cross-sample?
Take the bath, each rinse stage and the last rinse in one sequence while the fault is present.
What does permeate conductivity mean?
It tracks contamination; a rising trend means the rinse carries bath or soil into the film.
Why keep three or four stages?
Counterflow stages dilute drag-in step by step; fewer stages peak the load.
How does temperature fit?
It shifts solvent and wetting; a cold weekend bath can push the system into the rupture window.
What about voltage?
High voltage with excess solvent widens rupture risk; check both together.
What is the fastest proof?
A cross-sample before any bath adjustment, with the fault positions mapped to the log.
When call the supplier?
After the interface is cleared - bath chemistry is the last suspect, not the first.
What Would You Like to Solve?
Describe your rinse stage counts, permeate numbers, fault positions and bath logs. We can help trace the interface and set the cross-sample routine.