

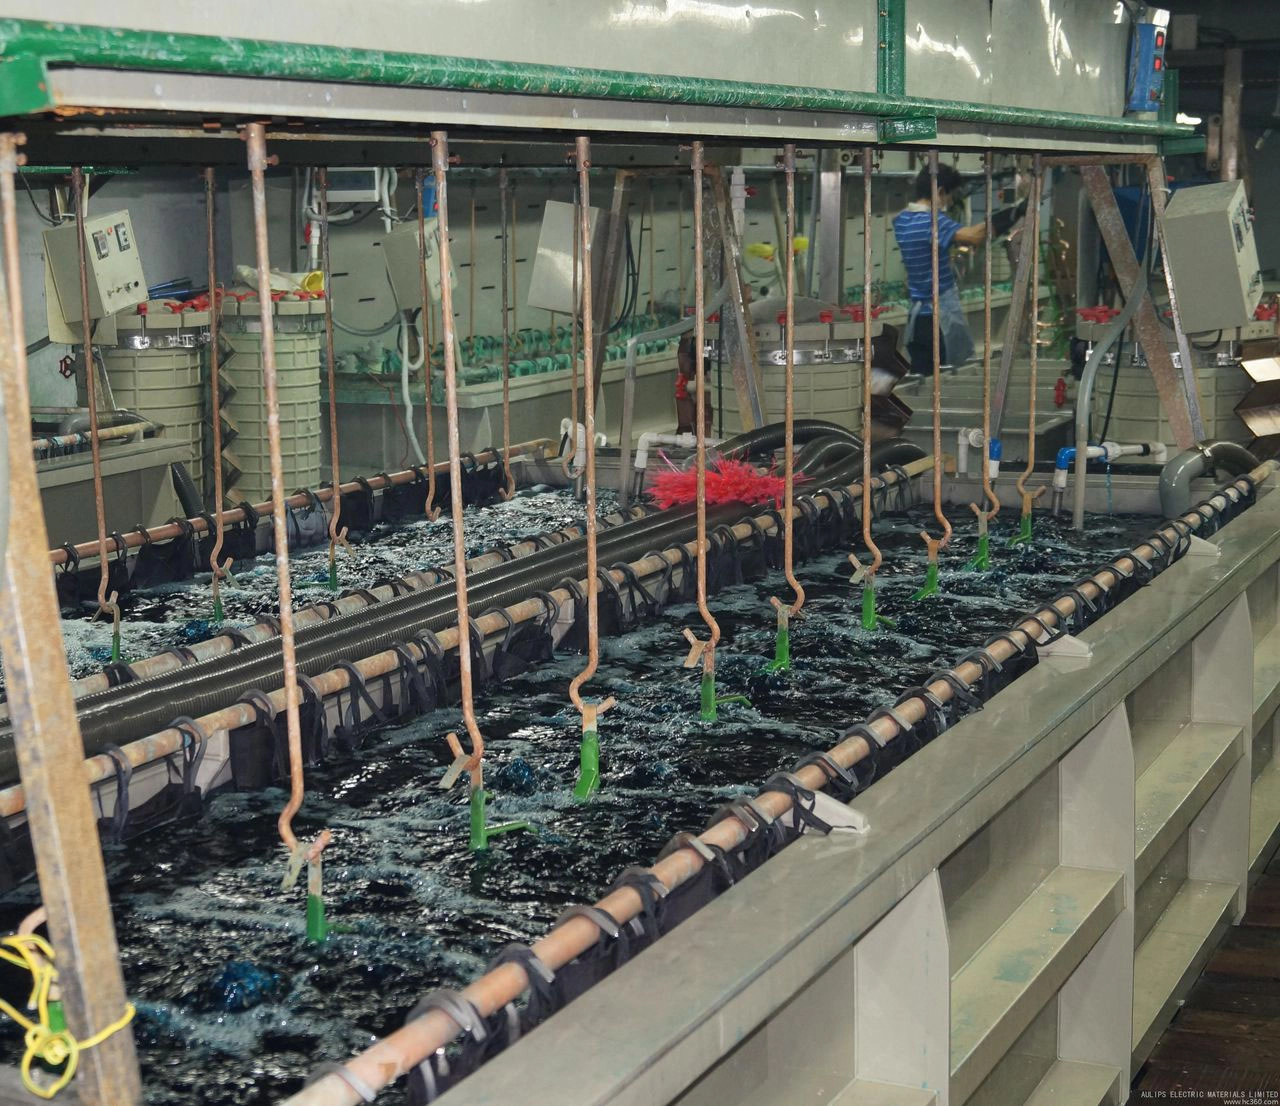
Adhesion failures moved from one plating line to another and back again over six weeks, and each line blamed the other's chemistry. Interface analysis showed an oxide film between the substrate and the deposit that formed during a 90-second dwell after degreasing.
This senior guide covers failure-interface analysis, dwell time control, conversion coating verification and the cross-process checks that stop adhesion faults from jumping lines.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Line blamed, not interface | Real fault stays hidden | Analyze the failed interface first |
| 2. Dwell time unmeasured | Oxide grows between stages | Cap dwell under 60 seconds |
| 3. Parts dried mid-line | Oxide forms on dry surface | Keep parts wet through stages |
| 4. Conversion coating unverified | Thin or missing film | Weigh coating per standard |
| 5. Crosshatch on one spot | Local fault missed | Test multiple locations |
| 6. Chemistry changed first | Process fault repeats | Check timing before chemistry |
| 7. No substrate history | Alloy change missed | Log supplier and lot |
| 8. Racks shared between lines | Faults travel on racks | Separate or clean racks per line |
| 9. Bake test skipped | Hydrogen fault hidden | Bake sample per spec |
Best Practices
- Analyze the failed interface before changing any chemistry
- Cap the dwell time between degrease and activation at 60 seconds
- Verify conversion coating weight per standard weekly
- Test adhesion at multiple locations, not one spot
- Log substrate supplier and lot with every batch
- Keep parts wet through the whole pretreatment chain
Implementation Roadmap
| Step | Frequency |
|---|---|
| Identify interface | SEM/EDX on failed sample |
| Measure dwell times | Per line, per stage |
| Verify coating weight | Weekly |
| Run bake and crosshatch | Per batch |
| Review cross-line data | Monthly |
Interface fault flow
- Analyze - SEM/EDX the failed interface. (Blame without data jumps lines.)
- Time - Dwell under 60 seconds. (Dried parts grow oxide.)
- Verify - Coating weight weekly. (Thin film fails adhesion.)
- Track - Substrate lot per batch. (Alloy changes repeat faults.)
Adhesion fails at the weakest interface, not the newest process. | An oxide film a few nanometers thick breaks adhesion completely.
Interface control data
Reference values for adhesion failure analysis across pretreatment lines.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Dwell after degrease | Under 60 seconds | Longer dwell grows surface oxide |
| Dwell to activation | Under 30 seconds | Dry parts need re-wetting |
| Zinc phosphate weight | 1.5-3.5 g/m2 | Below 1.5 fails adhesion |
| Iron phosphate weight | 0.3-0.8 g/m2 | Light film for painted parts |
| Crosshatch test | ISO 2409, grade 0-1 | Grade 2 or more equals reject |
| Bake test | Per spec, 200 deg C typical | Reveals hydrogen or moisture faults |
| Activation acid | 1-5% at 30-60 s | Weak acid leaves oxide |
| Interface scan | SEM/EDX at 2000x | Confirms the failing layer |
Adhesion test record
| Test | Standard | Accept |
|---|---|---|
| Crosshatch | ISO 2409 | Grade 0-1 |
| Bend test | ASTM D522 | No crack at radius |
| Bake test | Per spec | No blister after 200 deg C |
| Pull-off | ISO 4624 | Over 5 MPa |
Dwell time card
| Stage to stage | Limit | Check |
|---|---|---|
| Degrease to rinse | 60 s | Stopwatch audit |
| Rinse to activation | 30 s | Keep parts wet |
| Activation to conversion | 30 s | No dry spots |
| Conversion to final rinse | 60 s | Uniform film |
Case 1 - adhesion faults that jumped between two plating lines
Scenario. Adhesion failures moved between two lines every few weeks for six weeks; each line's chemistry was re-dosed and the fault returned on the other side, and the lab found no single bath out of range.
Action. SEM/EDX on the failed samples showed an oxide layer between substrate and deposit; stopwatch audits found a 90-second dwell after degreasing on both lines, and parts sat dry on the transfer. Dwell was capped at 60 seconds, parts kept wet, and racks were separated per line.
Result. The jumping pattern stopped; dwell time and substrate lot became logged items on both lines.
Case 2 - a supplier alloy change that looked like a bath fault in Turkey
Scenario. A plant in Turkey saw adhesion failures on the same product after a substrate supplier change; the bath was re-analyzed twice with no fault found.
Action. Lot tracking showed the new alloy had a different zinc-aluminum ratio; activation time was extended from 40 to 60 seconds and a new lot gate was added at incoming inspection.
Result. Failures stopped after the activation change; the incoming gate now flags alloy changes before production.
Frequently Asked Questions
Why do adhesion faults jump between lines?
The fault lives in a shared process or part flow, not in one bath; shared racks, dwell times and substrates travel between lines.
How do I find the real interface?
Analyze the failed sample with SEM/EDX at the interface; the failing layer shows which stage produced it.
What is dwell time and why does it matter?
Dwell is the pause between stages; a dry part grows oxide in seconds, and the oxide breaks adhesion.
What dwell limit should I enforce?
Under 60 seconds from degrease to rinse, under 30 seconds to activation, and keep parts wet the whole chain.
How do I verify the conversion coating?
Weigh a panel before and after phosphating; zinc phosphate should run 1.5-3.5 g/m2.
Which adhesion test should I trust?
Crosshatch ISO 2409 plus a bake test per spec; run both at multiple locations on the part.
Why check the substrate lot?
Alloy composition changes alter activation response; lot tracking turns a mystery into a known variable.
Can racks carry the fault?
Yes; a contaminated rack touches parts on every line, so separate or clean racks per line.
When should I change chemistry?
After interface analysis and timing audits show a chemistry cause; changing chemistry first hides the real fault.
What Would You Like to Solve?
Describe your line sequence, dwell times and the failed interface data; the dwell and coating gates here can be fitted to your line layout.