
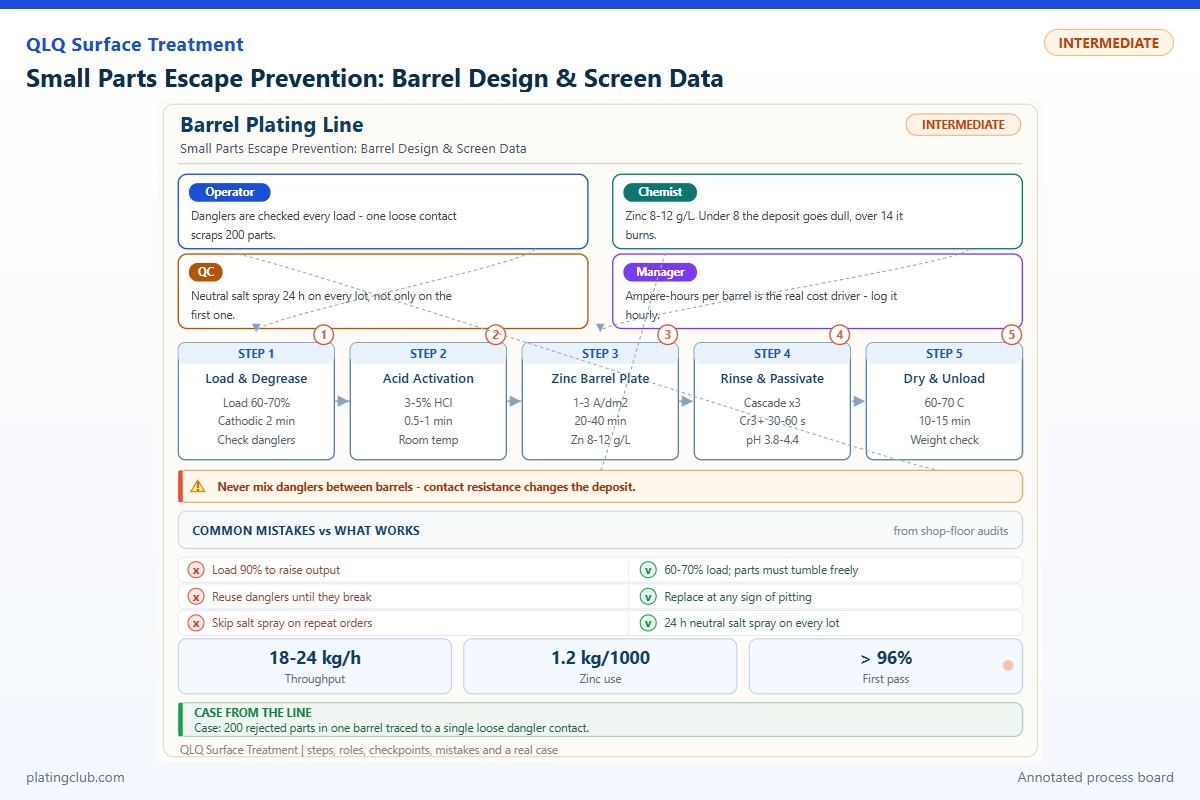
BARREL PLATING / MANAGEMENT ENGINEERING
Small Parts Escape Prevention: Barrel Design & Screen Data
Small-part escape is a containment failure, not simply a purchasing problem called “wrong mesh.” A spring plate can pass edge-first through a slot, a thin pull can lodge behind a liner, and a correctly sized screen can leak at its door. Management must control the entire containment boundary while preserving electrolyte exchange, electrical contact and unloading reliability.
This guide addresses small zipper components and comparable finishing hardware. Its release principle is straightforward: qualify the smallest incoming geometry against the largest opening the assembled barrel can develop in service. Then demonstrate that the retained load still receives acceptable coating. Zero visible losses during one trial is insufficient evidence of long-term capability.
Evidence boundary: QLQ knowledge-base operating ranges and published equipment data are identified below. Numerical screen examples are engineering calculations, not measured production results. No authenticated escape, coating-thickness or corrosion trial report was supplied; the experimental comparison table therefore explicitly leaves results pending.
1. Specify the escape geometry before ordering a screen
Collect parts from incoming lots, including tolerance extremes, burr-free samples and any legitimately flexible components. Record thickness, narrowest width, hole geometry and the orientation in which each part can enter an opening. Overall length is rarely the controlling dimension. For spring plates, include elastic deflection under representative tumbling contact without deliberately deforming good parts.
Inspect panels, doors, end plates, seams, shaft penetrations and cathode-entry arrangements as one system. Measure openings with calibrated optical equipment or suitable gauges; a mesh count alone does not specify clear aperture. Record both slot width and length. Use hot, wetted assembly checks where material expansion or liner movement can change gaps.
Manufacturer data illustrate available architectures: Tscherwitschke lists micro-part slots of 0.4 × 3.5 mm and replaceable sieve buttons, noting that sieve buttons provide less free surface than other perforation types. These are supplier examples, not QLQ specifications or proof that a 0.4 mm slot retains your part. See the manufacturer's perforation data.
| Boundary | Data required | Illustrative design check | Release evidence |
|---|---|---|---|
| Thin plate versus long slot | Minimum thickness and entry orientation | A 0.35 mm plate may enter a 0.40 mm slot edge-first | Worst-orientation wet challenge; no passage or wedging |
| Round perforation | Smallest passable projected geometry | A thickness measurement alone cannot establish passage through a round hole | Actual-part challenge across tolerance extremes |
| Square woven screen | Clear aperture a and wire width w | a = 0.30 mm; w = 0.20 mm; theoretical open area = 36% | Assembled aperture map and loaded coating trial |
| Door and liner seam | Maximum assembled gap, including distortion | Proposed gap ceiling must be below the validated passage geometry | Hot/wet measurement, latch inspection and seam challenge |
Square-screen open area (%) = 100 × [a / (a + w)]²
The 36% calculation excludes supports, overlapping seams and blockage. If one-quarter of the theoretical opening area becomes blocked, the remaining projected open area is 27%, before those other losses. This is a geometric estimate, not a prediction of flow. Measure drain time and coating performance rather than equating open area with guaranteed electrolyte renewal.
2. Choose containment without creating a plating bottleneck
A fine liner may stop escape while retaining sludge, increasing drag-out or shielding recesses. Unsupported liners can fold and create hidden pockets. Reinforcement may restore stiffness but reduce active area. Require chemical and temperature compatibility, mechanically captured edges, smooth internal transitions and accessible inspection surfaces; do not rely on adhesive alone for critical retention.
QLQ's local Barrel Plating note gives general operating ranges of 8–15 rpm, 30–50% volumetric loading and 0.5–3 A/dm². It also connects overloading with uneven deposits, excessive speed with collision damage and poor contact with missed plating. These are starting references, not universal settings for every barrel or electrolyte. The QLQ-BPM reference identifies a four-tank slider barrel machine; its note does not establish a certified minimum retained part size.
Assign a barrel identity, screen revision and qualified part-family list. Changing a latch, replacing a liner, introducing thinner stock or increasing load is a process change requiring review. Keep spare panels controlled by measured aperture, not by visual resemblance.
Two implementation scenarios to investigate
Thin spring plates: begin with edge-first passage and seam testing. If losses occur only after unloading, inspect the discharge interface and liner pockets before changing plating chemistry. These are diagnostic actions, not a reported customer outcome.
Small pull components: if a tighter liner eliminates losses but the coating minimum falls, compare drain time, current trace, contact condition and load turnover. Trial a supported higher-open-area construction while keeping retention geometry unchanged. Do not “solve” restricted exchange by raising current blindly.
3. Working formulation for a controlled nickel comparison
A containment trial needs stable chemistry. The table defines an additive-free Watts nickel reference electrolyte for engineering trials on a suitable prepared substrate. It is not a complete zinc-alloy pretreatment route, bright decorative nickel system or direct-on-zinc recommendation. Establish the approved undercoat and activation separately.
The salt ranges below follow the Nickel Institute's Nickel Plating Handbook. Typical values are selected trial targets within those ranges, not a QLQ proprietary formula. Proprietary brighteners and wetting agents are deliberately excluded; a production system requiring them must use its supplier's approved dosing schedule.
| Component | Range | Typical | Function | Replenishment |
|---|---|---|---|---|
| Nickel sulfate, NiSO4·6H2O | 240–300 g/L | 270 g/L | Main nickel source | Maintain soluble anodes; correct analyzed nickel deficit, accounting for nickel from both salts |
| Nickel chloride, NiCl2·6H2O | 30–90 g/L | 60 g/L | Supports anode dissolution and conductivity | Analyze chloride; dissolve calculated additions separately and recheck |
| Boric acid, H3BO3 | 30–45 g/L | 40 g/L | Controls near-cathode pH behavior | Analyze; add dissolved material for drag-out losses, not by ampere-hours alone |
| Deionized water | Balance to final volume | Final working volume | Solvent | Restore verified level before concentration correction |
| Diluted sulfuric acid; approved nickel carbonate for upward correction | As required by measured pH | No fixed dose | pH adjustment | Laboratory-guided incremental correction; mix, filter where required, then remeasure |
For 1,000 L, the selected make-up requires 270 kg nickel sulfate hexahydrate, 60 kg nickel chloride hexahydrate and 40 kg boric acid, brought to final volume after dissolution. Follow the approved mixing instruction and current SDS controls. Never transfer this acid nickel recipe into another bath merely because both processes use barrels.
4. Trend bands and intervention thresholds
The following are proposed internal trial controls, not experimentally proven failure boundaries. Validate them against the chemical supplier, machine limits and part drawing. The nickel trial temperature is chemistry-specific; it must not be confused with the QLQ general note's 20–45°C range for unspecified plating solutions.
| Parameter | Proposed normal band | Danger / hold threshold | Management response |
|---|---|---|---|
| Watts trial pH | 3.8–4.2 | Outside 3.5–4.5 | Hold trial; verify meter and chemistry before correction |
| Watts trial temperature | 50–55°C | Below 40°C or above 60°C, or any lower equipment limit | Stop trial; investigate heating and sensor agreement |
| Trial barrel speed | 8–10 rpm | Outside the qualified setting; above 15 rpm exceeds cited general range | Measure speed and inspect collisions or poor turnover |
| Settled volumetric load | 30–40% | Above 50%, or outside the qualified loading band | Split batch; verify contacts and bed movement |
| Average trial current density | 0.5–1.0 A/dm², subject to coupon qualification | Above qualified limit; 3 A/dm² is not an automatic allowable maximum | Hold and confirm actual part area and current distribution |
| Drain time against clean-screen baseline | Within ±10% | Increase above 20% | Inspect blockage and retained liquid before restart |
| Escape and unexplained inventory loss | Zero observed escapes; reconciled inventory | Any escape or unresolved count difference | Contain lot and inspect all boundary interfaces |
Record trends by part family, not as pooled averages. A stable tank pH cannot demonstrate stable solution conditions inside a congested barrel. Likewise, rectifier current can remain constant while local contact deteriorates.
5. Experimental comparison: retention and coating together
Run the baseline and candidate screens with matched incoming parts, load, preparation, chemistry and electrical program. Use at least three independent batches per construction and rotate trial order to reduce time-related bias. Do not intentionally operate a known-leaking barrel in production; establish the unsafe baseline in an isolated non-electrical containment test instead.
| Batch / specimen | Test condition | Escape count | Nickel thickness, µm | Adhesion / surface result | Drain time, s |
|---|---|---|---|---|---|
| A1–A3: currently approved screen | Same part lot; 35% load; 8 rpm; qualified reference electrolyte; fixed recorded ampere-hours | Pending measured count | Pending: minimum, mean, maximum on actual parts | Pending approved adhesion check and visual inspection | Pending measurement |
| B1–B3: finer supported screen | Matched to A; only screen assembly changed | Pending measured count | Pending: same sites, instrument and calibration | Pending; record wedging and collision marks separately | Pending measurement |
| C1–C3: alternate seam / door assembly | Matched to A; qualified aperture retained; boundary joint changed | Pending measured count | Pending: same sampling plan | Pending; inspect trapped parts after unloading | Pending measurement |
Measure actual-part coating at agreed critical locations using a validated method, with cross-section confirmation where geometry makes readings unreliable. A separately wired coupon does not reproduce intermittent barrel contact. Report specimen count, instrument uncertainty and the lowest individual reading; release against the customer drawing rather than an invented universal thickness.
If corrosion testing is required, compare the complete approved coating stack using the customer's specified method, duration and acceptance criteria. Do not infer salt-spray hours from nickel thickness. Hardness testing also needs a suitable deposit thickness and substrate-effect assessment; it is not a substitute for retention testing.
Observed escape rate = escaped parts / loaded parts. With zero independent events in n opportunities, approximate one-sided 95% upper bound = 3/n.
Thus zero escapes in 10,000 independent opportunities corresponds to about 300 ppm as an approximate upper bound, not demonstrated zero risk. Barrel observations are often correlated within a batch; repeated independent batches and maintenance challenges are essential.
6. Engineer Notes
- Isolate energy before opening, measuring or replacing any barrel component; never gauge a moving assembly.
- Challenge every seam with the smallest acceptable part in its easiest entry orientation, then repeat under approved hot/wet conditions.
- Measure a mapped set of apertures, including worn edges; retain photographs, maximum readings and gauge identification.
- Capture drain-time baselines with fixed liquid, temperature, loading and lift procedure; never compare unrelated drain cycles.
- Inspect and clean cathode contacts before screen comparisons so contact deterioration does not masquerade as a screen effect.
- Reconcile loaded, unloaded, sampled and recovered parts; weigh only with a validated counting method and its uncertainty.
- Quarantine torn liners and distorted doors; do not patch an unqualified opening and return it silently to production.
7. Shift Checks and ownership
| Shift stage | Check item | Frequency | Acceptance standard | Record |
|---|---|---|---|---|
| Before shift | Screen, seams, latch and barrel identity | Each barrel before use | Correct revision; no damage; all gauges within qualified limits | Operator checklist and aperture exception log |
| Before shift | Bath condition and contacts | Start-up and after correction | Approved chemistry bands; sound, clean contacts | Analysis sheet and maintenance signature |
| During shift | Load, speed and current trace | Every batch | Qualified program and stable turnover | Batch traveler with actual readings |
| During shift | Escape trap and drain time | Every unloading cycle | No escaped parts; drain time within qualified band | Count, location, drain time and disposition |
| After shift | Inventory reconciliation and hidden pockets | Each barrel and final batch | No unexplained loss or retained mixed parts | Reconciliation signed by shift lead |
| After shift | Wear trend and next-shift handover | Daily | Open actions assigned; unsafe barrels isolated | Maintenance queue and handover log |
Production owns counts and operating records; maintenance owns mechanical condition; process engineering owns chemistry and qualification; quality owns measurement and disposition. Management should review escape incidents, minimum coating thickness, rework and screen life together. Rewarding throughput alone encourages overloading and delayed replacement.
8. Technician-to-AI FAQ
These are example technician-style prompts, not authenticated customer quotations.
“AI, our holes are smaller than the part width. Why are parts still escaping?”
Check thickness and edge-first passage, not just width. Map door gaps, seams and cathode entries, including hot/wet distortion. Find the first escape location using an approved recovery arrangement, then challenge that boundary with actual tolerance-limit parts.
“AI, can I fit finer mesh and keep the same amps and cycle time?”
Not without qualification. Finer mesh changes exchange, drag-out and possibly contact behavior. Match trial conditions, compare minimum actual-part thickness and drain time, then approve a revised program only after retention and coating both pass.
“AI, we lost no parts in one batch. Can management approve the barrel?”
One batch is preliminary evidence. Repeat across independent batches, incoming geometry extremes and normal maintenance conditions. Reconcile inventory, document maximum openings and meet the drawing's coating criteria before issuing the qualified part-family release.
9. Source notes and next engineering step
Local QLQ sources: the Obsidian knowledge-base note titled “Barrel Plating” in the IMA product-knowledge section, and 03-Equipment Knowledge / Machine Compendium / 4Tank Slider Barrel Plating Machine.md (English filename; directory names translated here). These support the general operating ranges and QLQ-BPM identity, not an escape-performance guarantee. External references are linked beside their relevant technical claims.
What Would You Like to Solve?
Send the smallest part dimensions, current aperture and seam measurements, barrel revision, batch loading and any authenticated coating reports to [email protected]. Ask for a containment-and-coating qualification review. For the wider equipment, chemistry and process-support scope, see turnkey surface-treatment line planning.