
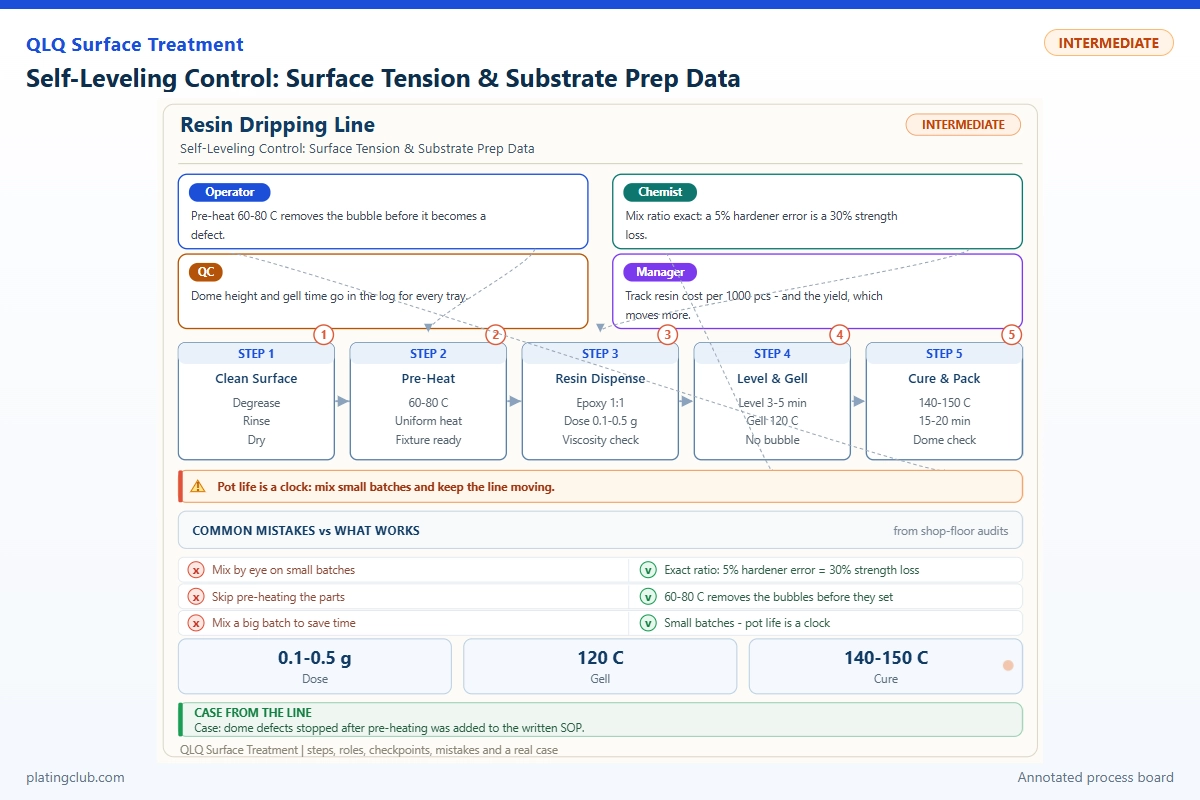
RESIN DRIPPING / MANAGEMENT
Self-Leveling Control: Surface Tension & Substrate Prep Data
A smooth resin dome is the result of compatible wetting, controlled flow and timely cure. On plated zinc-alloy bag hardware, reducing surface tension alone can replace craters with edge overflow. Management must control the complete interface: final metal finish, cleaning residue, resin condition, dispensing volume, fixture angle and elapsed time.
This guide addresses two-component epoxy doming, not PVC plastisol, silicone molding or an electroplating bath. Epoxy does not have a useful bath-pH operating window. The objective is a reproducible dome with sound adhesion, rather than the lowest possible liquid surface tension.
Evidence boundary: No verified QLQ coupon dataset, epoxy formulation or customer trial report for this topic was available in the reviewed knowledge base. The comparison table is an unexecuted experiment record; numerical operating bands are proposed qualification starting points, not measured production limits. Supplier data are separately identified.
1. Separate Wetting from Leveling Before Changing Chemistry
Wetting describes how resin contacts the substrate. Leveling describes how height differences decay before the network becomes too viscous to flow. A clean surface may wet correctly while an aged batch retains dispense marks. Conversely, fresh low-viscosity resin can level within a region yet retract from an oily spot.
Young's relation, gammaSV = gammaSL + gammaLV cos(theta), connects solid-vapor, solid-liquid and liquid-vapor interfacial tensions with the equilibrium contact angle. Real production surfaces are rough, heterogeneous and sometimes reactive; do not infer an absolute surface-energy value from one drop measurement.
For a thin-film disturbance, leveling time scales approximately with viscosity multiplied by disturbance wavelength to the fourth power, divided by surface tension and film thickness cubed. This simplified model is not a dome-design equation. It shows why reducing surface tension can improve spreading while slowing capillary smoothing, and why broad waviness persists longer than small dispense ridges.
Measure mixed-resin surface tension at a fixed temperature and elapsed time. Measure resin contact angle on a sacrificial coupon with the actual topcoat or plating finish. A water contact-angle measurement is useful for contamination trending, but it cannot substitute for resin wetting or predict cured adhesion.
2. Working Data & Formula Notes
A complete shop-floor mixing formulation can use a purchased matched resin and hardener; its proprietary constituent chemistry should not be reconstructed. The benchmark below uses Fong Yong E-1158-2/H-1158-2, not a QLQ-qualified hardware resin. Its published applications primarily concern labels and flexible substrates, so plated-metal adhesion needs independent qualification.
| Component | Range | Typical | Function | Replenishment |
|---|---|---|---|---|
| E-1158-2, Part A | Fixed 75.00 wt%; no formulation range authorized | 45.00 g | Resin component | Weigh into each new batch; never top up reacting material. |
| H-1158-2, Part B | Fixed 25.00 wt%; no formulation range authorized | 15.00 g | Matched curing component | Add once at the specified 3:1 mass ratio. |
| Additional leveling agent | 0 wt% for this benchmark | 0 g | Excluded to isolate substrate effects | No shop-floor additions; obtain supplier approval for a separate trial. |
| Solvent, pigment and filler | 0 wt% for this benchmark | 0 g | Excluded; preserve the complete supplied system | None. Do not dilute aged batches. |
The manufacturer lists Part A viscosity at 400–1,000 mPa·s and Part B at 70–120 mPa·s, both at 25°C. These are not mixed-resin viscosity values. Its pot-life reference is 30–40 minutes for 60 g at 25°C; full-cure references are seven days at room temperature or 120 minutes at 80°C, with Shore A hardness of 80–90. Shore A is not interchangeable with Shore D. Manufacturer processing and property reference.
For any approved 3:1 system, hardener mass equals resin mass divided by three. Control ratio error against this target, not against total mixture mass. Scrape the mixing vessel walls and bottom, transfer to a clean cup, and mix again using a validated low-air-entrainment procedure. Product-specific mixing instructions take precedence.
There is no replenishment method for partially cured resin. Record both component lots, masses, temperature and mixing start time. A larger batch may heat itself more rapidly; laboratory pot life does not authorize scaling up without thermal and dispensing trials.
3. Substrate Preparation That Preserves the Final Finish
Map the incoming surface stack before choosing a cleaner: zinc alloy, copper or nickel layers, decorative finish, lacquer and anti-tarnish treatment may each change adhesion. Approve cleaning on representative finished coupons. Do not use aggressive abrasion or acid activation on decorative surfaces without checking appearance, coating integrity and compatibility.
Use a validated cleaner, controlled rinse and complete drying where the finish permits wet cleaning. For solvent wiping, use only a supplier-approved solvent and a two-cloth method: one wetted cloth lifts contamination, and a separate clean cloth removes it before evaporation. Check solvent compatibility and ventilation; keep ignition sources away.
Handle dried parts with clean gloves and protect trays from polishing dust, silicone sprays and compressor oil. Compare water-break behavior only on surfaces where that test is appropriate: a deliberately hydrophobic lacquer may fail it even when clean. Establish a clean reference for each finish instead of imposing one universal wetting rule.
If plasma treatment is proposed, qualify treatment dose, delay before dispensing and adhesion after aging. More treatment is not automatically better. A process that improves initial spreading but damages the topcoat or changes color is not acceptable.
4. Normal Variation Bands versus Stop Thresholds
These engineering bands are screening settings for a controlled trial near 25°C. Replace them with validated limits for each resin, finish and geometry. Crossing a stop threshold means segregating affected trays and investigating; it does not prove a specific chemical cause.
| Parameter | Proposed normal band | Proposed danger / hold threshold | Response |
|---|---|---|---|
| Resin and substrate temperature | 23–27°C | Below 20°C or above 30°C | Condition material and parts; reassess usable dispensing time. |
| Hardener-dose error | Within ±1% of target B mass | Beyond ±2% | Hold batch; never correct by guessing after dispensing. |
| Mixed viscosity at matched temperature and age | 0.90–1.10 times qualified reference | Below 0.80 or above 1.25 times reference | Check temperature, ratio and reaction age. |
| Mixed-resin surface tension | Qualified reference ±2 mN/m | Departure greater than 4 mN/m | Repeat measurement; check contamination and lot change. |
| Actual-resin contact angle | Qualified reference ±5° at fixed read time | Increase greater than 10°, or visible retraction | Inspect preparation and finish identity before additive trials. |
| Substrate-to-dew-point margin | At least 3°C | Below 3°C | Hold dispensing until condensation risk is removed. |
| Fixture inclination | Within ±0.2° of approved orientation | Beyond ±0.5° | Reset fixture; inspect dome asymmetry. |
| Dispensed mass | Target ±3% | Beyond ±5% | Check nozzle, calibration and pressure stability. |
Trend by lot and shift, not only by pass/fail count. Repeated movement toward one boundary warrants action even before rejection occurs. Separate measurement variation from process variation through duplicate readings and instrument checks. Do not introduce silicone additives because a single dyne or contact-angle reading appears low.
5. Coupon Experiment and Batch Comparison Record
Unexecuted experimental matrix: The fields below require real measurements. No film thickness, corrosion hours, hardness or pass rate is being claimed. Use coupons from the same plating batch, randomize tray positions, and test at least five coupons per condition. Retain a bare plated control when evaluating corrosion.
| Coupon / batch | Test condition | Wetting / leveling data | Cured dome thickness | Hardness | Salt spray / adhesion |
|---|---|---|---|---|---|
| P0: incoming control | As received; 25 ±2°C; fresh mix; identical target mass | Record contact angle at 30 s; coverage and craters at 5 min | Pending: center and four edge points, mm | Pending: separate suitable plaque after complete cure | Pending: actual hours, defect locations and adhesion results |
| P1: approved cleaning | Validated clean/rinse/dry; otherwise identical to P0 | Same measurements and timestamps | Pending: mean, range and dome symmetry | Pending: same cure and test temperature | Pending: same exposure and evaluation rules |
| P2: preparation-delay challenge | P1 preparation; covered hold for 4 h before dispensing | Same measurements; document storage conditions | Pending: same positions and method | Pending: same plaque method | Pending: compare interface failure with P1 |
| P3: resin-age challenge | P1 preparation; dispense 15 min after mixing at 25 ±2°C | Record viscosity and surface tension at dispense time | Pending: inspect ridge persistence and edge height | Pending: complete cure before comparison | Pending: same exposure and evaluation rules |
Use optical profiling or a sectioned witness coupon when a magnetic thickness instrument cannot isolate resin above a multilayer plated substrate. Soft domes on thin metal do not provide valid bulk-hardness readings; prepare a specimen suitable for the selected method. Report the scale, specimen thickness and conditioning.
If the buyer requires neutral salt spray, agree on the applicable method, exposure duration, scribed versus unscribed condition and failure definition before testing. Record edge corrosion separately from under-resin blistering. Salt-spray hours are not a service-life conversion, and resin cannot repair porous or defective plating underneath.
6. Two Diagnostic Scenarios for Management
Scenario A: Craters Follow One Incoming Finish Lot
This is a diagnostic example, not a reported customer case. Fresh resin wets the approved reference coupon but retracts on one incoming lot. Quarantine that finish lot and run P0 versus P1 without changing resin. Ask whether polishing compounds, anti-tarnish chemistry or protective lacquer changed. If cleaning restores spreading, still verify adhesion after cure and aging; appearance alone cannot release the lot.
Scenario B: Domes Become Uneven Late in the Shift
This is also a diagnostic example. Wetting remains consistent, but end-of-batch coupons show ridges and asymmetric fill. Compare fresh and aged resin on identically prepared parts, then verify tray level and nozzle mass. If reaction age explains the drift, reduce batch size or introduce controlled metering. Do not add solvent or increase hardener to compensate; both actions create new chemistry variables.
7. Engineer Notes
- Photograph a fixed reference area under constant lighting at dispensing, five minutes and full cure; retain scale and coupon identity.
- Measure contact angle at a defined drop volume and read time; use sacrificial coupons so test fluids never contaminate saleable parts.
- Weigh ten consecutive shots into tared cups after setup; calculate mean and range before releasing the nozzle.
- Level the loaded fixture, not just the empty bench; check support points after tray changes.
- Label every mixed cup with start time and a validated discard time; prohibit mixing old material into fresh batches.
- Run substrate and resin changes independently. Keep an unchanged reference coupon in every qualification trial.
- Before releasing a corrective action, verify cured adhesion and appearance after the agreed exposure, then update instructions and train every shift.
8. Shift Checks and Traceability
| Shift stage | Check item | Frequency | Acceptance standard | Record |
|---|---|---|---|---|
| Before shift | Finish identity, cleaner and protected storage | Each incoming lot and setup | Approved route; no unauthorized finish change | Traveler, finish lot and preparation time |
| Before shift | Temperature, dew point and fixture level | Before first dispense | Within qualified bands | Environmental and fixture checklist |
| During shift | Component masses and batch age | Every mix | Approved ratio; before discard time | Resin lots, scale readings and timestamps |
| During shift | Shot mass and first-off dome | Setup, nozzle change and hourly | Qualified dose; no retraction or overflow | Shot-weight sheet and coupon photograph |
| During shift | Reference wetting and leveling | New resin or finish lot; after interruption | Within validated reference limits | Contact angle, viscosity and observation time |
| After shift | Tray cure status and segregation | Every retained tray | Complete approved cure; suspect trays held | Cure log and release signature |
| After shift | Yield, waste and outstanding corrective actions | Daily handover | Defects classified; unresolved lots identified | Handover board and action owner |
Management should review first-pass yield by finish lot, discarded resin mass per accepted part, and cure-space occupancy. Assign preparation control to the upstream finishing owner, dispensing control to the resin team, and release authority to quality. Shared ownership must not become undocumented responsibility.
9. FAQ: Technician-to-AI Questions
These are suggested technician prompts, not authenticated customer quotations.
“AI, our resin forms fish-eyes only on some plated parts. Should I add more leveling agent?”
First compare the suspect finish with a clean qualified reference using the same fresh mix. Local retraction points to surface heterogeneity, but confirm it experimentally. Review cleaner residues, silicone exposure and final protective coatings. Additive changes require supplier approval and separate adhesion testing.
“AI, the dome spreads well but spills over the edge. How do I stop it?”
Check shot mass, fixture inclination and boundary geometry before increasing viscosity. Excessive spreading may indicate incompatible surface treatment or additive loading. Compare the actual-resin contact angle with the approved reference. Adjust one variable at a time and verify cured edge coverage.
“AI, can good hardness and salt-spray results prove the substrate preparation is correct?”
No. Hardness primarily describes cure, while corrosion performance also depends on plating integrity and exposed edges. Verify adhesion with a suitable agreed method, inspect the failure interface, and compare preparation controls. A hard dome can still detach from contaminated lacquer.
10. What Would You Like to Solve?
Send the resin technical sheet, complete finish stack, dome dimensions, cleaning route and time-stamped defect photographs to [email protected]. Include fresh-versus-aged coupon results so the discussion can separate interface contamination from flow and cure problems. For coordinated upstream and downstream planning, review turnkey surface-treatment lines, equipment, chemicals and support.
Local scope source: QLQ knowledge-base machine-directory page 25 lists silicone mixing, vacuum and dispensing equipment. That catalog does not establish epoxy compatibility or validate this process. Source file: 03-Equipment Technology / Company Directory / Machine Directory / Page 25 (English rendering of the local filename). Confirm equipment wetted materials and metering performance for the chosen epoxy separately.