

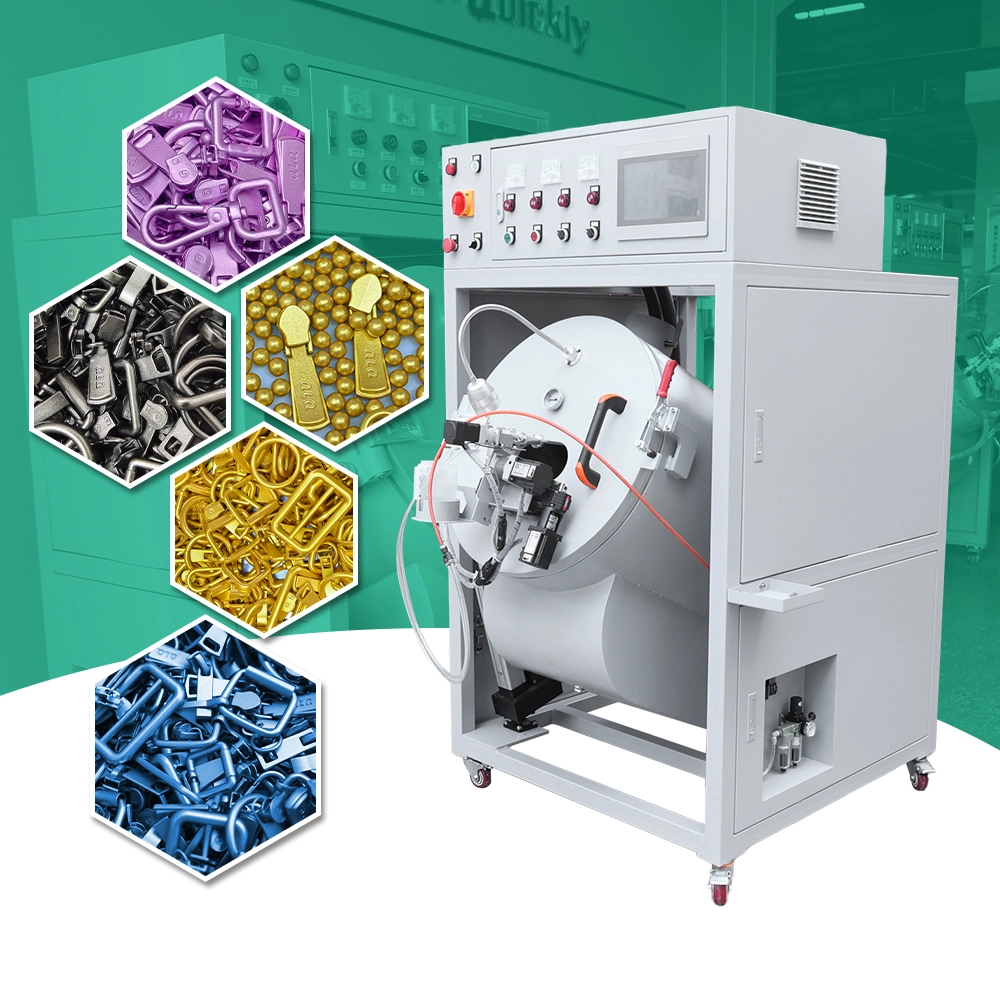
Zinc alloy bag hardware cures by metal temperature, not by oven timer. A dense rack in the middle of an oven can run 15 degrees cooler than a light rack at the edge, and the painter will not see it until hardness or solvent tests fail.
This senior guide covers cure profiling for rack painting: measuring part temperature by rack position, auditing rack density and oven airflow, and building a cure map that every product can use.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Curing by timer | Dense loads under-cure | Measure part temperature |
| 2. Probing one rack | Misses oven zones | Probe multiple positions |
| 3. Racks too dense | Air cannot reach centre parts | Open rack spacing |
| 4. Ignoring oven top-to-bottom gradient | Edges over-cure, centre lags | Map the full oven |
| 5. Changing paint for a thermal fault | Costly and ineffective | Profile before changing paint |
| 6. No audit after rack change | New density changes cure | Re-profile after changes |
| 7. Testing only by feel | Soft centre passes the thumb | Run hardness and solvent tests |
| 8. Same settings all seasons | Ambient air shifts the profile | Seasonal review |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Profile part temperature at multiple rack positions
- Control rack density so air reaches every part
- Audit the oven after any rack or airflow change
- Verify cure with hardness and solvent tests, not feel
- Keep a cure map per product family
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Rack cure profiling flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- The coolest part in the oven defines the batch, not the average.
- Every product family needs its own cure map because rack density changes thermal mass.
- Never over-cure edge parts to fix a cold centre; open the rack or extend dwell.
- Never profile with one rack type and apply the map to another.
Working Data & Formula Notes
Cure profile reference
Example values for a typical two-pack rack paint; confirm with your paint spec.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Metal temperature | Per paint spec | Start dwell when reached |
| Dwell time | Per paint spec | At metal temperature |
| Probe positions | 4-6 per oven load | Top, middle, bottom, sides |
| Rack gap | Per product map | Allows airflow between racks |
| Audit cycle | Quarterly | Plus after any change |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Cure fault location table
| Fault position | Likely cause | Response |
| Centre of oven | Rack density too high | Open spacing |
| Bottom of rack | Cold air pooling | Airflow or rack height |
| Top of rack | Over-cure | Check oven top gradient |
| Edge parts only | Radiation hot spots | Reduce temperature, extend time |
| Whole load fails | Oven set point or timer | Re-profile from zero |
Implementation Cases
Case 1 - the dense rack that under-cured
Situation. A plant filled an oven with dense racks of zinc frames to raise throughput. Hardness tests started failing on centre parts while edge parts over-cured.
Approach. Temperature probes showed the centre of the dense load never reached the paint spec. Rack spacing was opened and dwell time extended until the centre reached temperature.
Outcome. Cure passed across the whole load, and rack density became part of the product cure map.
Case 2 - the paint changed for a thermal fault
Situation. Repeated soft finishes led a team to switch to a slower paint at higher cost. The fault returned, and a senior profile found the oven had a cold bottom zone that no part temperature check had caught.
Approach. Airflow baffles were adjusted, probes confirmed the bottom zone reached spec, and the original paint was restored.
Outcome. The plant kept the original paint and the cure map now covers the full oven height.
Frequently Asked Questions
Why measure metal temperature?
Parts cure by metal temperature; oven air can be hot while dense parts stay cold.
How many probe points do I need?
Enough to cover the oven zones and rack positions, typically four to six.
How does rack density affect cure?
Dense racks block airflow, so centre parts heat slowly and under-cure.
Why test hardness and solvent resistance?
They confirm cure; the thumb cannot feel a soft centre.
When should I re-profile?
After any oven, rack or airflow change, plus a seasonal review.
Should I change paint for a cure fault?
No; profile first and fix the thermal cause.
What is a cure map?
A record of rack density, probe results and settings for one product family.
Who owns the cure map?
The senior process owner, reviewed with every oven change.
What Would You Like to Solve?
If cure faults persist on dense racks, send us your oven layout, rack density and paint cure spec. We can help build the profiling plan and cure maps that protect every part position in the oven.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.