

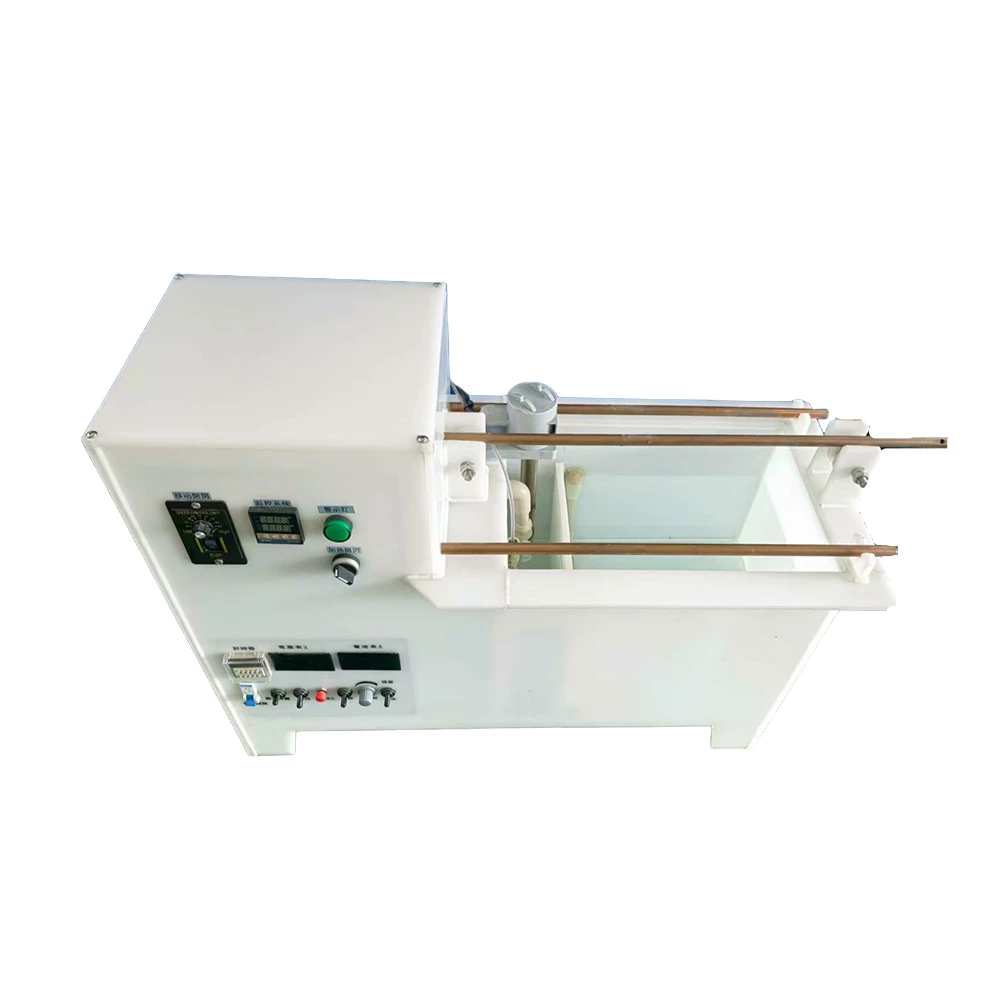
An e-coat line uses electricity in rectifiers, pumps and ovens, and water in rinses, DI makeup and UF. Both are silent costs that grow with every inefficient habit, and neither appears until the utility bill arrives.
This management guide covers e-coat energy and water efficiency: metering kilowatt-hours per square metre, controlling DI water cost, maximizing UF recovery, and the environmental scorecard that tracks all of it monthly.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No energy meter per line | Utility bill hides waste | Meter kWh per line |
| 2. DI water by habit | Cost invisible | Track per rinse stage |
| 3. UF bypassed | Drag-out lost to drain | Maximize UF recovery |
| 4. Rinses overfed | Water and treatment cost rise | Set flow by conductivity |
| 5. Oven half full | Energy per part doubles | Consolidate oven loads |
| 6. No environmental board | Waste continues unseen | Monthly scorecard |
| 7. Too many targets at once | Nothing improves | One target per quarter |
| 8. Savings not verified | Improvements fade | Re-measure after changes |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Meter energy and water per line, not per plant
- Track DI water by rinse stage
- Maximize UF recovery before adding makeup
- Set rinse flow by need and conductivity
- Review the environmental scorecard monthly
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Efficiency flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Efficiency targets must protect film quality; a kWh target can never break the cure.
- Water and energy share the same scorecard because they share the same process.
- Never cut rinse flow below the conductivity window.
- Never turn off UF to save electricity; the bath cost will be higher.
Working Data & Formula Notes
Efficiency data
Example metrics for an e-coat efficiency board; adapt to your line.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Energy | kWh per m2 coated | Includes rectifier, pumps, oven |
| DI water | Litres per m2 coated | Tracked by rinse stage |
| UF recovery | Drag-out returned % | Higher recovery cuts makeup cost |
| Rinse flow | Per conductivity | Minimum that holds quality |
| Review | Monthly | One target per quarter |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Efficiency scoreboard example
| Metric | Last month | Target | Status |
| kWh per m2 | 0.42 | 0.38 | Audit pumps |
| DI litres per m2 | 8.5 | 6.5 | Check rinse flow |
| UF recovery | 82% | 90% | Service UF |
| Oven load | 65% | 85% | Consolidate batches |
Implementation Cases
Case 1 - the rinse that used half the DI water
Situation. DI consumption on an e-coat line was far above the design rate. No stage was metered, so the whole line shared the blame.
Approach. Flow meters by stage showed one rinse running at double its required rate because a valve had been opened years earlier.
Outcome. The valve was reset to the conductivity window and DI use fell by 40% without any quality change.
Case 2 - UF bypassed to save a pump
Situation. A maintenance decision ran the line with UF bypassed to save electricity. Drag-out losses rose, makeup chemical use climbed, and bath stability suffered.
Approach. UF recovery was restored and the efficiency board added a UF recovery line so the saving was visible against the chemical cost.
Outcome. Chemical makeup fell, bath stability returned, and no future decision bypasses UF without a full cost review.
Frequently Asked Questions
What is the best energy metric?
Kilowatt-hours per square metre coated, tracked per line.
Why meter DI water by stage?
One overfed rinse can cause most of the waste; stage meters find it.
How does UF save money?
It returns drag-out chemistry to the bath instead of sending it to drain.
Can I cut rinse flow?
Only to the minimum that holds the conductivity window.
Why consolidate oven loads?
A half-full oven uses the same energy for fewer parts.
How do I set targets?
One target per quarter with a clear re-measurement after the change.
Should energy targets ever break quality?
No; every target must respect the film and cure windows.
Who reviews the scorecard?
The department manager with maintenance and quality data monthly.
What Would You Like to Solve?
If energy and DI costs on your e-coat line are invisible, send us your utility records, rinse layout and UF data. We can help build the per-line scorecard and recovery plan that cut cost without touching film quality.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.