
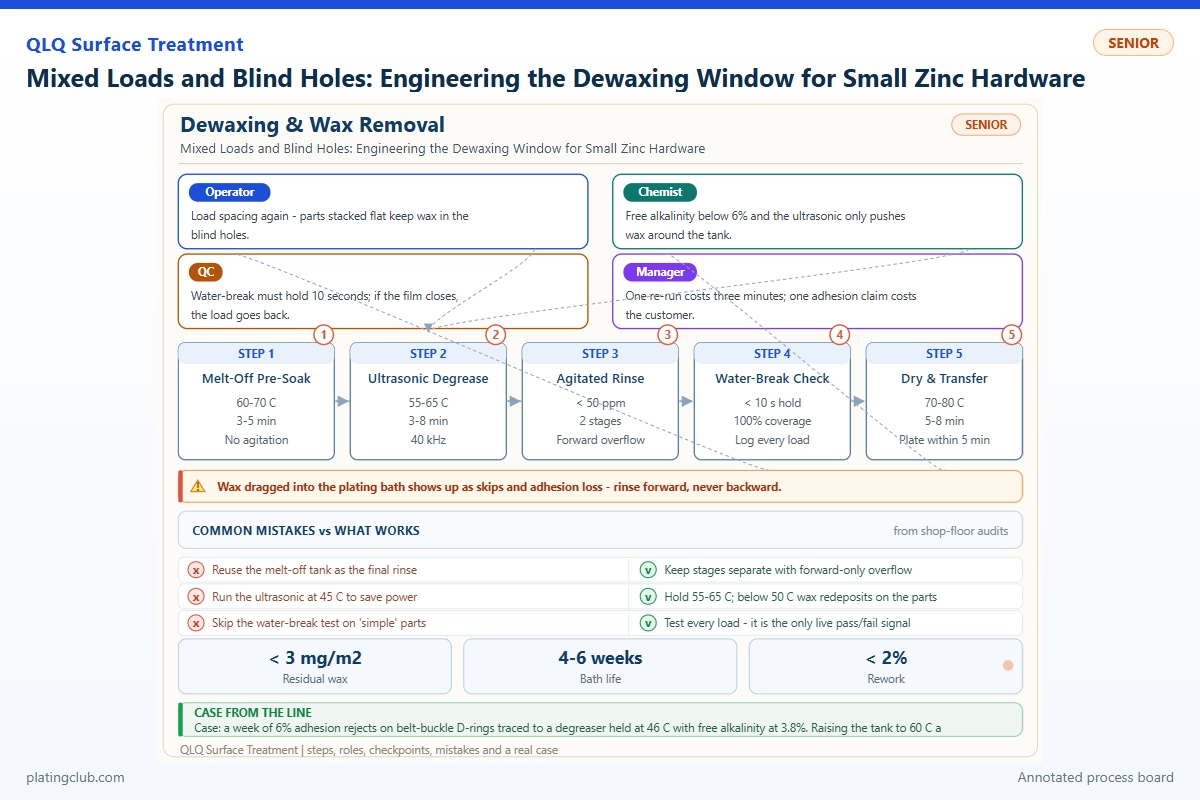
Small zinc hardware arrives in mixed batches: flat belt buckles next to deep D-rings with blind holes. One window must clean both. This is how senior staff engineer the load so the hardest geometry sets the cycle, not the average.
<= 60%
Load factor
sets the cycle
Hardest geometry
100% coverage
Blind-hole gate
Geometry classes and their dewaxing demand
| Class | Example | Demand | Cycle change |
|---|---|---|---|
| Open flat | Belt buckle plate | Easy, 3 min | None - use as the reference |
| Open 3D | D-ring | Moderate, 4-5 min | None |
| Blind hole | Clasp cavity | Hard, 6-8 min | Extend cycle; tilt the basket |
| Shielded thread | Screw boss | Hard, needs flow | Rotate parts at 50% cycle |
Basket and flow design rules
| Rule | Do | Do not |
|---|---|---|
| Load factor | Fill to 60% maximum | Brim-full baskets - shadows clean nothing |
| Orientation | Face cavities downward, angled 15-30 deg | Nest blind holes against each other |
| Spacing | One part thickness between layers | Stack flat parts face to face |
| Rotate | Turn the basket at half cycle for mixed geometry | Assume cavitation reaches sealed cavities |
Blind-hole validation (do once per new part)
| Step | Method | Pass |
|---|---|---|
| 1 | Dye the cavity with marker ink | Ink fully removed |
| 2 | Run the production cycle | Cavity free of ink, no residue |
| 3 | Water-break the cavity | Film holds 10 s |
| 4 | Cross-hatch after plating | No lift at the cavity lip |
Watch out
A cycle that cleans a flat buckle is not evidence for a clasp. Validate the hardest geometry in the load and let it set the clock.
Common mistakes and the fix
| ✗ Set cycle time from the easiest part | ✓ Let the blind-hole part set the cycle |
| ✗ Nest parts for volume | ✓ Nesting creates shadowed faces and trapped wax |
| ✗ Skip rotation for mixed loads | ✓ Rotation costs 30 seconds and saves whole batches |
| ✗ Validate on scrap that was already clean | ✓ Use real production parts with real wax |
What each role watches
| Operator | "Keep the basket within the marked load line and rotate at half cycle." |
| Chemist | "If rotation is impossible, raise alkalinity to the top of range and shorten bath life instead." |
| QC | "Own the blind-hole validation record per part number." |
| Manager | "Price mixed loads honestly: the hardest part sets the cost." |
From the shop floor
Case: a shop quoted mixed belt-hardware loads at the flat-part cycle time. Blind-hole clasps failed cross-hatch in one batch out of five. Rotating the basket at half cycle and adding two minutes gave a 100% pass rate at a 4% cost increase - far below the cost of the failures.
FAQ
Can I clean blind holes without rotation?
Sometimes, but only at reduced load and higher temperature. Rotation is cheaper and more reliable.
Does higher alkalinity fix shadowing?
No. Chemistry cannot reach a shadowed cavity; flow and orientation do.
How often should a new geometry be validated?
Once per part number, and again whenever the polishing compound or basket changes.
Where to go next
- Level guide for this trade: Dewaxing & Ultrasonic Cleaning — technician levels
- Other levels: Junior, Intermediate, Management
- Owner view: Process Overview for owners
- Supplier view: Chemistry & Supply · Find content by trade + level