

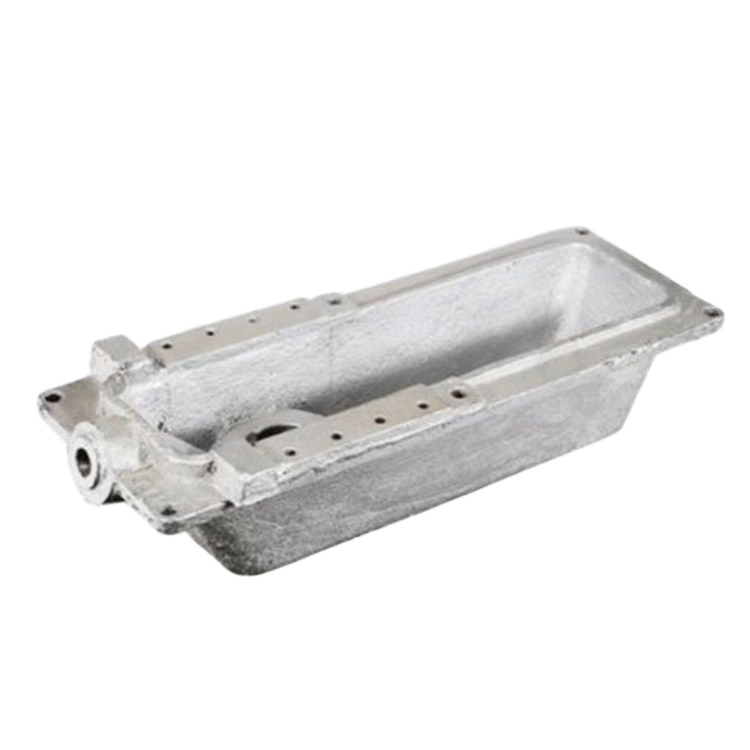
Sliders on one zinc line stuck in the die every afternoon between 2 and 4 pm while the morning ran clean. Cooling water leaving the die had climbed from 28 C to 41 C, and cavity surface temperatures differed by 35 C.
This intermediate case guide traces sticking to die thermal balance, cooling circuit condition and lube timing, and sets the checks that keep a die stable across a full shift.

Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Afternoon sticking accepted | Thermal drift untreated | Measure die temperature at noon |
| 2. Cooling lines scaled | Flow drops, die overheats | Clean and measure flow per channel |
| 3. Water delta ignored | Outlet at 41 C hides blockage | Log inlet and outlet per shift |
| 4. Lube sprayed only at start | Slides dry by afternoon | Set lube per shot or slide cycle |
| 5. Slides over-lubed | Residue and gas cause sticking | Use ratio and count per shot |
| 6. Cycle time stretched | Die cools between shots | Hold cycle within 0.5 s |
| 7. One cavity runs hot | Parts stick only there | Balance channels, check each cavity |
| 8. Ejector pins worn | Sticking blamed on heat | Check pin clearance 0.05-0.10 mm |
| 9. No noon check | Fault found at 3 pm | Pyrometer sweep at noon and 2 pm |
Best Practices
- Log cooling water inlet and outlet temperature every shift
- Keep cavity surface spread within 15 C
- Clean cooling channels on a fixed schedule
- Set lube spray to the part cycle, not to habit
- Run a pyrometer sweep at noon and 2 pm
- Hold cycle time within 0.5 s across the shift
Implementation Roadmap
| Step | Frequency |
|---|---|
| Log water delta | Every shift, inlet and outlet |
| Sweep die surface | Noon and 2 pm daily |
| Clean cooling lines | Monthly or per flow drop |
| Check lube ratio | Daily, per shot count |
| Review sticking log | Weekly, by cavity |
Thermal balance flow
- Measure - Water delta and cavity spread at noon. (Afternoon faults hide until 3 pm.)
- Balance - Clean lines, re-route flow. (Scale blocks heat removal silently.)
- Lube - Every shot or per slide cycle. (Dry slides stick; rich lube gases.)
- Hold - Cycle time and water log. (Drift repeats the same stuck parts.)
Sticking follows heat accumulation, not melt changes. | A 5-10 C water delta means the circuit is working.
Thermal balance data
Reference values for zinc die thermal control.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Die surface window | 180-220 C | Holds dimensional and finish stability |
| Cavity spread | 15 C max | Wider spread means uneven shrinkage and sticking |
| Cooling water delta | 5-10 C in to out | Above 10 C points to scale or low flow |
| Channel flow | 5-8 L/min per channel | Flow check beats temperature guessing |
| Lube spray | Every shot or per slide | Timing follows the heat load |
| Ejector pin clearance | 0.05-0.10 mm | Tight pins stick as the die heats |
| Cycle time hold | 0.5 s | Slow cycles cool the die between shots |
Afternoon sticking check card
| Check | Target | Action |
|---|---|---|
| Water inlet | 20-28 C | Chiller set point |
| Water outlet | Delta 5-10 C | Clean channel, raise flow |
| Cavity surface | 180-220 C | Balance channels |
| Cavity spread | 15 C max | Re-route cooling |
| Slide movement | Free by hand at 180 C | Lube and clean slides |
Cooling line maintenance
| Line | Schedule | Sign of trouble |
|---|---|---|
| Main channels | Monthly clean | Delta above 10 C |
| Slide lines | Per 20k shots | Sticking on one side |
| Chiller filter | Weekly | Flow drop across the line |
Case 1 - sticking stopped by rebalancing the cooling circuit
Scenario. Zinc alloy sliders stuck in the die every afternoon from 2 to 4 pm on one machine. The morning ran clean, the melt was in window, and operators sprayed extra lube as a workaround.
Action.
Result.
Case 2 - ejector pin marks that looked like a heat fault
Scenario. A plant running luggage lock frames found ejector pin marks and sticking on one corner every late shift; thermal checks read normal because the pins, not the die, were the problem.
Action.
Result.
Frequently Asked Questions
Why only in the afternoon?
Heat accumulates through the shift; cooling that copes at 10 am fails at 3 pm.
What does a 5-10 C water delta mean?
The circuit removes heat properly; a bigger delta means scale, low flow or a blocked channel.
How do I check thermal balance?
Log water inlet and outlet per shift and sweep the cavity surface with a pyrometer at noon.
Why do sliders stick?
Slides expand with heat, lube burns off, and clearances close; all three peak in the afternoon.
How often lube the slides?
Per shot or per slide cycle, not just at start; dry slides stick within an hour.
Can I spray more lube to fix it?
Temporarily, but rich lube leaves residue and gas; fix the cooling instead.
What cavity spread is acceptable?
Keep the surface within 15 C across the cavity; wider spread means uneven shrinkage.
Why clean cooling lines?
Scale is an insulator; a half-blocked line raises the outlet temperature without warning.
What about ejector pins?
Clearance should be 0.05-0.10 mm; tight pins stick and mark as the die heats.
What Would You Like to Solve?
Describe your sticking window, water temperatures and lube practice, and we can work through the thermal balance checks for your die.