

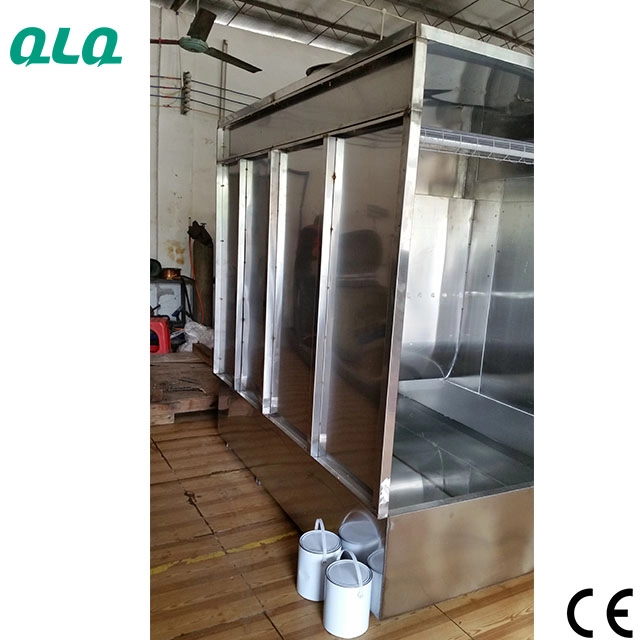
The same painter, gun and paint can give a different finish on opposite sides of a booth because airflow carries overspray and solvent away unevenly. Racks near the exhaust can dry-spray, while racks near the inlet stay wet longer and sag.
This intermediate guide covers the interaction between booth airflow and spray technique: reading air movement across the rack, adapting the pass plan, and the checks that make the booth part of the process instead of an unknown.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. One pass plan for the whole booth | Dry and wet zones plate differently | Adapt passes to air movement |
| 2. Spraying against the air | Overspray lands on the rack | Spray with the airflow direction |
| 3. Ignoring the exhaust side | Dry spray on far parts | Adjust distance and speed near exhaust |
| 4. Crowded rack blocks airflow | Overspray and solvent trap | Follow rack spacing rules |
| 5. No air movement check | Booth drift goes unnoticed | Check streamers each shift |
| 6. Long strokes in still zones | Sags on wet parts | Short controlled strokes |
| 7. Changing only the gun | Air problem returns | Fix the airflow before the gun |
| 8. Filter condition ignored | Airflow falls as filters load | Check filters on schedule |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Check air movement with streamers at rack height each shift
- Spray with the airflow, not against it
- Adapt stroke length and distance to the booth zone
- Keep rack spacing so air can pass through the load
- Include filter condition in the booth check
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Airflow-adapted spraying flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- Airflow turns a booth into a variable that can be planned.
- Filters are airflow; a loaded filter changes every zone.
- Never adjust the gun before checking the air movement.
- Never crowd racks so tightly that air cannot pass.
Working Data & Formula Notes
Booth reference
Working reference values for airflow-adaptive spraying; confirm with your booth manual.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Air velocity | Per booth spec | At rack height, not floor level |
| Spray direction | With airflow | Reduces overspray on the rack |
| Distance | Near exhaust: closer | Compensates for faster solvent drag |
| Stroke speed | Wet zone: steady | Prevents sags in still air |
| Zone check | Each shift | Catches filter and fan drift |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Zone adjustment guide
| Zone | Condition | Technique adjustment |
| Near inlet | Wet, slow dry | Steady stroke, slightly closer |
| Centre | Balanced | Standard card settings |
| Near exhaust | Dry, fast evaporation | Faster pass, shorter stroke |
| Below extraction | Strong vertical air | Adjust angle and speed |
| Blocked by rack | Poor circulation | Re-space racks first |
Implementation Cases
Case 1 - dry spray on the exhaust side
Situation. Parts on the exhaust side of a booth consistently showed dry spray while identical parts at the inlet were glossy. The painter adjusted the gun but the pattern stayed.
Approach. Streamer checks showed strong air at the exhaust side. The pass plan was changed there: shorter strokes, faster movement and slightly closer distance.
Outcome. Dry spray disappeared and the booth now has a zone map posted for each product.
Case 2 - sags that only appeared in one corner
Situation. Racks in one booth corner sagged on vertical faces while the rest of the booth passed. The painter blamed the paint until airflow checks showed a still-air pocket.
Approach. Rack spacing was opened and the corner pass used a lighter wet film with longer flash time before the second coat.
Outcome. Sagging stopped in the corner and the zone map was added to the shift handover.
Frequently Asked Questions
Why check airflow with streamers?
Air movement at rack height decides dry-spray and sag zones that are invisible from the floor.
Should I spray with or against the airflow?
With it; spraying against the air drives overspray onto the rack.
Why adapt passes by zone?
Near the exhaust paint dries faster; in still pockets it stays wet and sags.
Do filters affect the finish?
Yes; a loaded filter lowers airflow and changes every zone.
How often should I check the booth?
At least once per shift with streamers, plus after filter changes.
What do I do with a still-air corner?
Open rack spacing, shorten strokes and control the wet film.
Should I change the gun first?
No; check air movement first so the gun change is based on data.
Where should the zone map be kept?
Posted in the booth with settings for each product family.
What Would You Like to Solve?
If one side of your booth always finishes differently, send us your booth layout, filter schedule and product racking. We can help build the airflow zone map and the pass plans that make every position plate the same.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.