
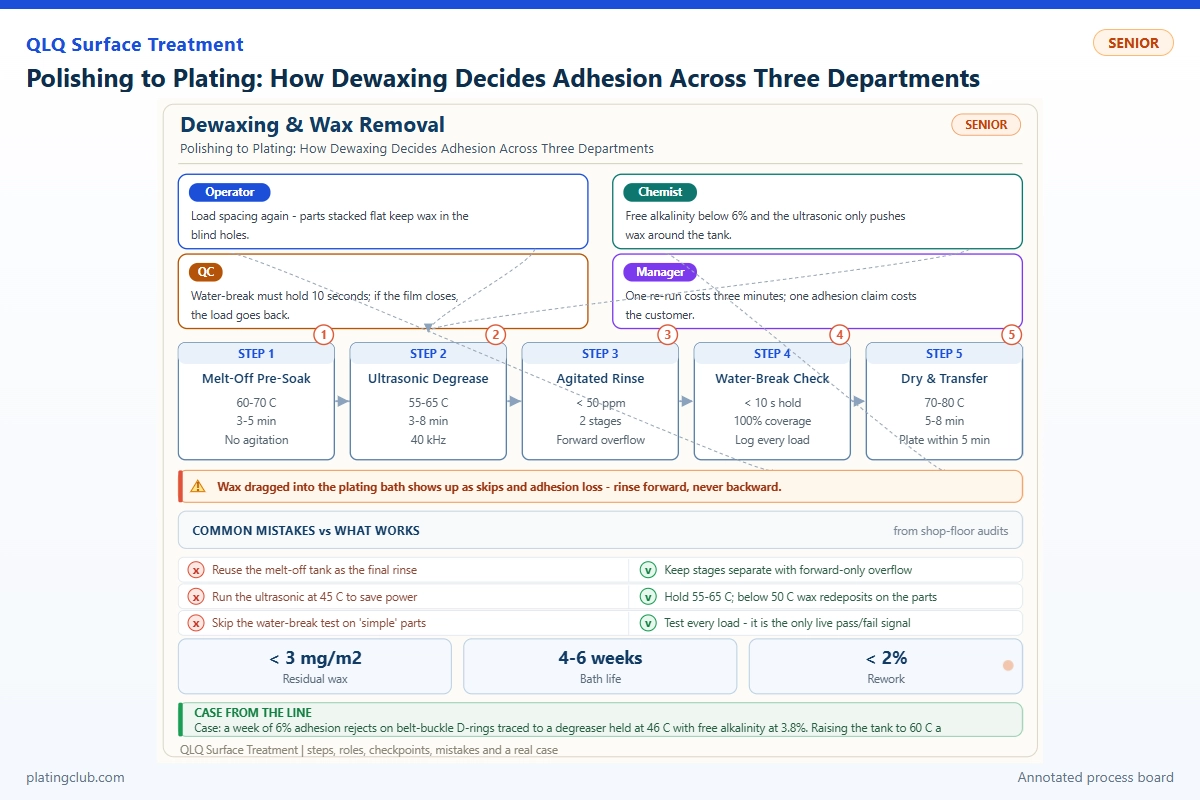
Adhesion is not decided in the plating bath. It is decided by the wax the polishing department chose, the dewaxing window that follows it, and the time the dried rack waits before plating. A senior technician owns all three numbers.
< 30 min
Handover time
0% cross-hatch lift
Shared metric
< 8 C
Window spread
Who sets which number (and what happens when it drifts)
| Department | Owns | Setting | Effect on plating |
|---|---|---|---|
| Polishing | Compound type | Stearate-based, <= 12% abrasive | Hard compound resists melt-off |
| Polishing | Finish time | 3-5 min per part | Over-buffing burns compound into the surface |
| Dewaxing | Tank temperature | 60-65 C | Below 55 C, redeposition begins |
| Dewaxing | Alkalinity | 7-8% free | Low alkalinity leaves a bonded film |
| Plating | Queue time | <= 30 min from dry | Long queues collect handling oils |
Shared window matrix (all three must be green)
| Condition | Polishing side | Dewaxing side | Plating side |
|---|---|---|---|
| Heavy compound | Reduce buffing pressure | Extend ultrasonic to 6-8 min | Add 1 extra rinse |
| Blind holes | Avoid filling cavities | Rotate parts mid-cycle | Check under-crown at QC |
| High humidity day | Shorter queue | Raise dry temp to 80 C | Shorter queue again |
| New part geometry | Pilot 50 pcs | Pilot tank run | Cross-hatch every batch |
Handover rules that survive shift changes
| Rule | Why | How it is checked |
|---|---|---|
| One rack, one ticket | Traceability from polish to plate | Ticket travels with the rack |
| Temperature logged every 2 h | Catches slow drift | Log initialled by dewaxing operator |
| Cross-hatch on every new part | Adhesion is geometry-specific | QC, with photo record |
| Queue timer visible | The 30-minute rule only works if seen | Digital clock on the rack stand |
Watch out
When a defect appears, resist the departmental instinct. Ask for the polishing compound batch, the dewaxing log and the queue time together - two of three will be in range, and the third is your answer.
Common mistakes and the fix
| ✗ Fix adhesion in the plating bath only | ✓ Adhesion starts upstream: check compound and dewaxing window |
| ✗ Change compound without telling dewaxing | ✓ A harder compound needs a longer melt-off or higher alkalinity |
| ✗ Allow unlimited queue time | ✓ Parts waiting collect oils and dust; 30 minutes is the working limit |
| ✗ Run pilots without QC gates | ✓ A pilot without a cross-hatch gate produces opinions, not data |
What each role watches
| Operator | "Rotate parts mid-cycle on complex geometries - cavitation does not reach sealed cavities." |
| Chemist | "Cross-check the degreaser after any compound change; dose needs may move 10-20%." |
| QC | "Own the cross-hatch gate and photograph every new geometry." |
| Manager | "Make the shared handover metric visible: one number on the wall beats three meetings." |
From the shop floor
Case: a line chased adhesion defects for three months across polishing, dewaxing and plating. The fix came from a single shared log: compound batches with higher stearate needed 8 minutes in the ultrasonic, not 4. The window matrix above is what ended the argument.
FAQ
How do I audit a handover quickly?
Pick one rack and ask for three documents: compound batch, dewaxing log for that hour, and the queue timestamp. Anything missing is your risk.
Should dewaxing report to polishing or plating?
Neither. It is a process stage of its own, with its own numbers and its own owner.
What is a realistic queue-time limit?
Thirty minutes from dry to plated for zinc hardware indoors; fifteen if the shop is humid or dusty.
Where to go next
- Level guide for this trade: Dewaxing & Ultrasonic Cleaning — technician levels
- Other levels: Junior, Intermediate, Management
- Owner view: Process Overview for owners
- Supplier view: Chemistry & Supply · Find content by trade + level