

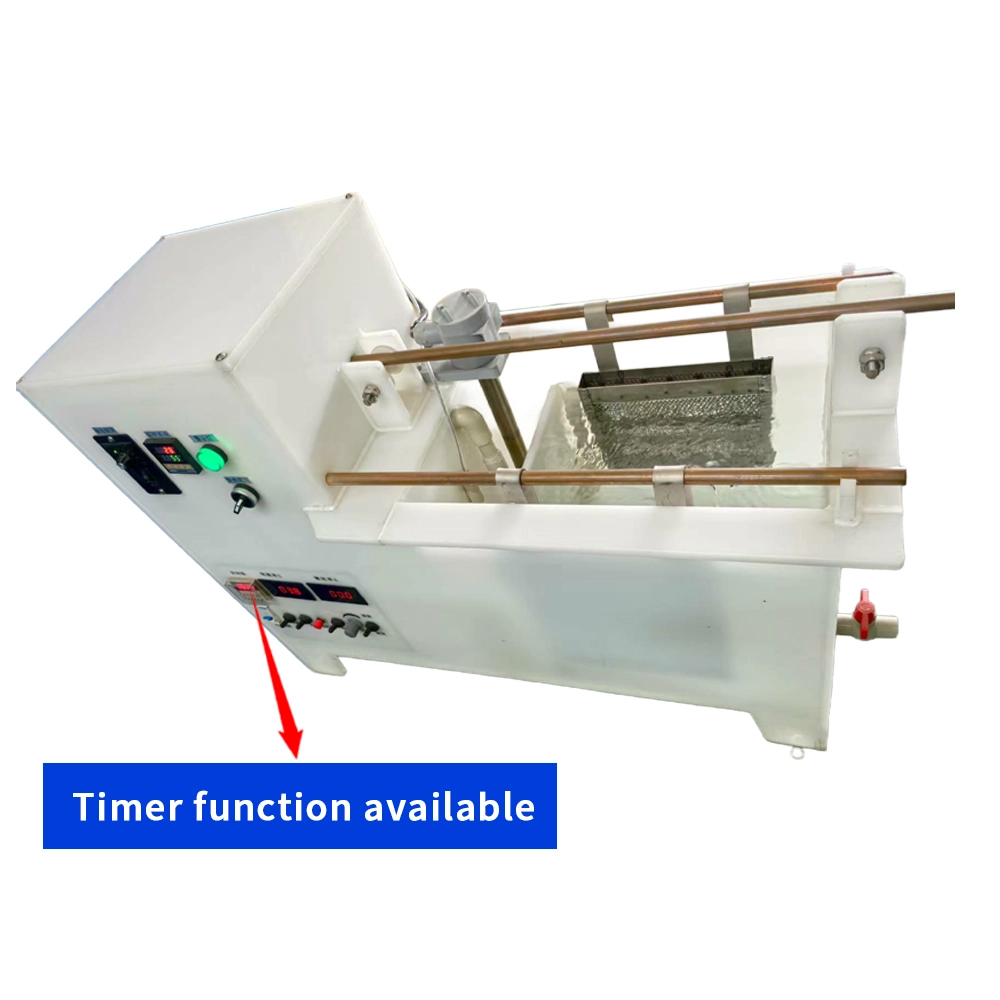
A plating plant cut unplanned downtime by a third in four months, without new machines. The change was planning: work orders, spare parts minimums and a maintenance calendar that people followed.
This case shows how maintenance management converts chaos into control: planning horizons, spare parts discipline, backlog rules and the metrics that prove the improvement.
Common Mistakes and How to Avoid Them
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. Maintenance only on failure | Downtime never falls | Shift to scheduled preventive work |
| 2. No work order system | Tasks vanish at handover | One order per task, one owner |
| 3. Spares bought after failure | Every breakdown waits | Set min-max stock with lead times |
| 4. Backlog grows unseen | Critical tasks slip | Review and cap backlog weekly |
| 5. Emergency parts at any price | Costs explode | Pre-stock the top 20 spares |
| 6. Preventive list from memory | Intervals drift | Write the calendar and audit it |
| 7. Downtime not measured | Improvement is invisible | Log every stop in minutes |
| 8. Technicians fight fires daily | Planning is impossible | Protect 30 percent of hours for planned work |
| 9. Stocked spares never used | Capital sits idle | Review stock against failure data quarterly |
Best Practices
- Run one work order per task with an owner and a due date
- Keep a weekly planning window and protect planned hours
- Set min-max spare levels from lead time and usage
- Review and cap the backlog every week
- Measure MTTR, MTBF and downtime percentage monthly
- Audit the preventive calendar against actual execution
Implementation Roadmap
| Step | Frequency |
|---|---|
| Review downtime and open orders | Daily |
| Plan next week's preventive work | Weekly |
| Review backlog and spares | Weekly |
| Update MTTR, MTBF and OEE | Monthly |
| Audit spare stock versus failure data | Quarterly |
Maintenance planning flow
- Measure - Downtime minutes per stop. (Unmeasured downtime cannot be managed.)
- Plan - Weekly window, protected hours. (Firefighting eats planning time.)
- Stock - Min-max from lead time. (Empty shelves cause long stops.)
- Review - Backlog, metrics, calendar. (Unreviewed plans decay into chaos.)
Unplanned downtime falls when preventive work is scheduled before failures. | Spare discipline is a management decision, not a storekeeper's job.
Maintenance management reference data
Reference values for maintenance planning on plating lines.
| Parameter | Reference | Why It Matters |
|---|---|---|
| Downtime target | Below 5 percent of run time | Well-planned lines run above 95 percent availability |
| OEE target | 85 percent or higher | Availability is the base layer |
| Planning horizon | 1 week fixed, 4 weeks rolling | Stable windows protect planned hours |
| Backlog cap | 2 weeks of work | Older tasks need review |
| Spare coverage | Top 20 parts by failure frequency | Covers most breakdowns |
| Min-max rule | Min equals lead-time usage times 1.5 | Prevents stockouts and idle capital |
| MTTR trend | Falling month over month | Faster repairs cut downtime |
Downtime before and after
| Month | Unplanned downtime (h) | MTTR (min) |
|---|---|---|
| Month 1 | 38 | 95 |
| Month 2 | 31 | 82 |
| Month 3 | 27 | 70 |
| Month 4 | 25 | 61 |
Spare parts min-max card
| Part | Min | Max | Lead time |
|---|---|---|---|
| Filter pump seal | 2 | 6 | 3 weeks |
| Rectifier fan | 1 | 3 | 5 weeks |
| Heater contactor | 1 | 4 | 4 weeks |
| Limit switch | 3 | 8 | 2 weeks |
Case 1 - downtime cut by a third in four months
Scenario. A plating plant logged 38 hours of unplanned downtime a month; technicians spent every day fighting breakdowns, and spares were bought after each failure.
Action. The manager introduced one work order per task, a weekly preventive window, min-max spares for the top 20 parts, and a daily downtime log.
Result. Unplanned downtime fell to 25 hours a month by month four, MTTR dropped from 95 to 61 minutes, and OEE rose to 87 percent.
Case 2 - a Mexican finishing plant's spare crisis
Scenario. A finishing plant in Mexico waited two weeks for a filter pump seal after every failure because spares were only ordered when the pump failed.
Action. Lead times were measured for the top 30 parts, min-max levels were set, and two local suppliers were qualified for critical seals.
Result. Average repair time for pump failures fell from 9 days to 1 day, and emergency freight costs dropped by 70 percent.
Frequently Asked Questions
How do I start cutting downtime?
Measure every stop in minutes, then plan preventive work in a weekly window; measurement comes first.
What is a work order system?
One written task with an owner, due date and result; it stops tasks from disappearing at handover.
Which spares do I stock?
The top 20 parts by failure frequency, with min-max levels based on lead time and usage.
What are min-max levels?
Minimum stock to cover lead-time usage and maximum to avoid idle capital; review quarterly.
How do I protect planning time?
Reserve about 30 percent of technician hours for planned work and let emergencies use the rest.
What metrics should I track?
Downtime percentage, MTTR, MTBF and OEE; review them monthly so improvements stay visible.
How much backlog is too much?
More than two weeks of work; older tasks need re-prioritization or they hide critical jobs.
How do I stop emergency buying?
Pre-stock critical spares and qualify a second supplier for each so lead times cannot hold the line hostage.
What is a realistic downtime target?
Under 5 percent of run time for a well-planned line; that supports an OEE of 85 percent or better.
What Would You Like to Solve?
Describe your current downtime numbers, spare situation and planning process, and share where the biggest single loss sits.