

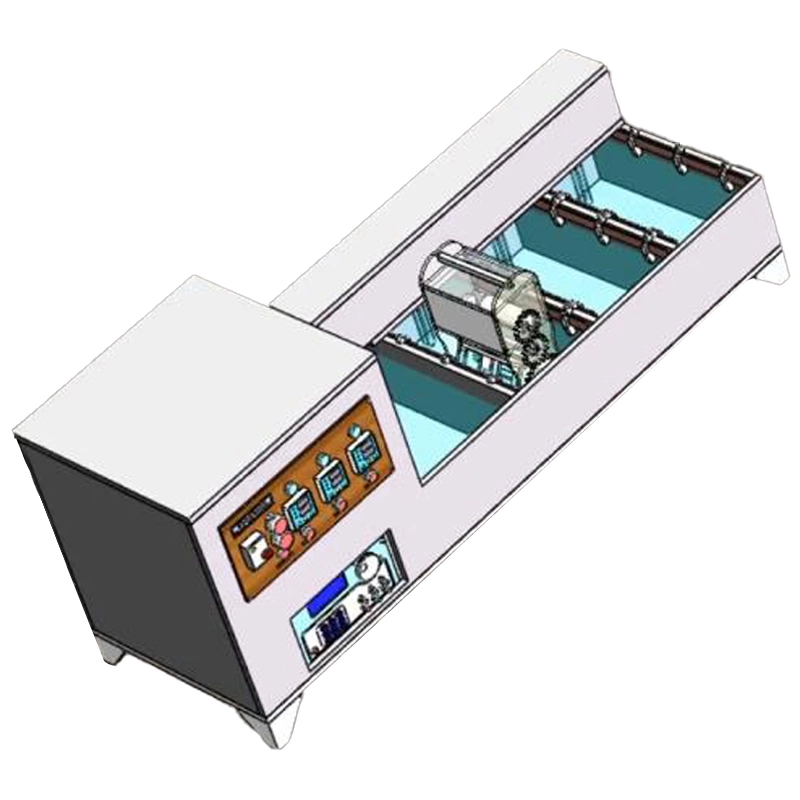
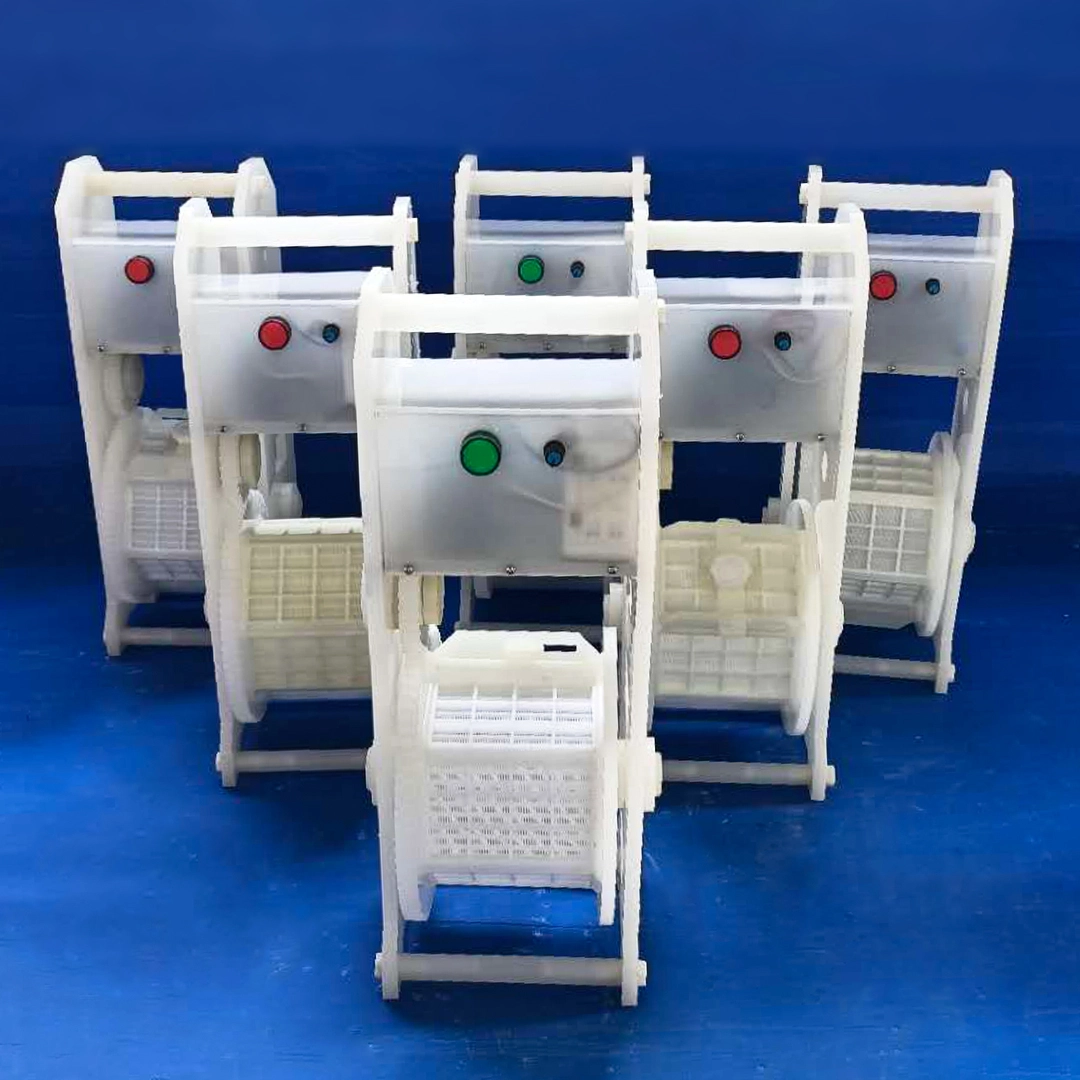
A barrel line is only as available as its weakest drum. When one barrel fails and there is no spare, the whole department loses capacity and every urgent order waits behind a repair.
This management guide shows how to run the barrel fleet like equipment, not furniture: spare barrel ratios, rotation schedules, load-count maintenance triggers, repair gates and the weekly cost review.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No spare barrel | One failure halts half the line | Keep 1 spare per 4-5 active drums |
| 2. Running a leaking drum | Chemical loss and rejects | Gate: stop at first leak sign |
| 3. No load-count log | Maintenance is guesswork | Count loads per barrel daily |
| 4. Danglers replaced only on failure | Thin deposits before failure | Rotate by load count |
| 5. Repairs delayed | Downtime becomes days | Set a same-day repair gate |
| 6. Every drum runs every product | Contamination and signatures mix | Assign drums by product family |
| 7. Spare barrel stored wet | Corrosion and worn seals | Store clean, dry and sealed |
| 8. No fleet cost review | Repair spend hides in general costs | Track cost per barrel-hour weekly |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Own the barrel fleet with a load-count log, not intuition
- Keep one spare barrel per four or five active drums
- Rotate danglers by load count before failure
- Assign drums to product families where possible
- Review fleet cost and downtime at the weekly meeting
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Fleet management flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- The fleet plan converts maintenance from reaction to schedule.
- Spare barrels are capacity insurance, not a luxury.
- Never let an urgent order keep a damaged barrel running.
- Store spare drums clean and dry, never half-filled.
Working Data & Formula Notes
Fleet planning data
Example planning ratios to adapt to your line size and product mix.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Spare ratio | 1 spare per 4-5 drums | Balances cost against downtime risk |
| Dangler service | 150-250 loads | Depends on product and current |
| Drum deep service | 800-1200 loads | Seals, bearings and interior |
| Leak gate | Immediate stop | Repair before the next load |
| Cost target | Track per barrel-hour | Makes the plan measurable |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Barrel fleet review sheet
| Item | Owner | Trigger |
| Dangler rotation | Line technician | Load count reached |
| Drum deep service | Maintenance | 800-1200 loads |
| Leak repair | Maintenance | Immediate stop-use |
| Spare readiness | Shift leader | Weekly check |
| Fleet cost review | Department manager | Weekly meeting |
Implementation Cases
Case 1 - the plant with no spare barrel
Situation. A nine-drum line carried no spare. When one drum cracked its door seal, the plant ran at seven drums for two days while urgent orders were re-planned around the gap.
Approach. Management bought two spare drums, numbered the fleet and introduced a load-count log so service happened on schedule instead of after failure.
Outcome. Barrel-related downtime fell by two thirds, and urgent orders no longer wait on repairs.
Case 2 - danglers replaced only when rejects appeared
Situation. Contact rejects were rising on one product. The team kept changing chemistry until a load-count check showed the barrel had passed 400 loads since its last dangler service.
Approach. A rotation schedule was set at 200 loads per barrel, with the count logged by shift and reviewed weekly.
Outcome. Contact-related rejects stopped, and the department saw a measurable first-pass yield gain within a month.
Frequently Asked Questions
How many spare barrels do I need?
About one spare for every four to five active drums on the line.
When should danglers be serviced?
At a set load count, typically 150-250 loads for standard programs.
Why assign drums to product families?
It keeps plating signatures clean and prevents cross-contamination.
How do I track load counts?
Log every load per barrel on the shift card; review weekly.
What is a repair gate?
A defined fault that stops the drum from running until repair is complete.
How should spares be stored?
Clean, dry and sealed, ready to install.
How do I measure fleet cost?
Track repair, spare and downtime cost per barrel-hour.
Who owns the fleet plan?
One department owner who reviews counts and costs weekly.
What Would You Like to Solve?
If you want a barrel fleet register, load-count form or rotation schedule for your line, tell us your drum count and typical loads per shift. We can help set spare ratios, service triggers and the weekly review format.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.