

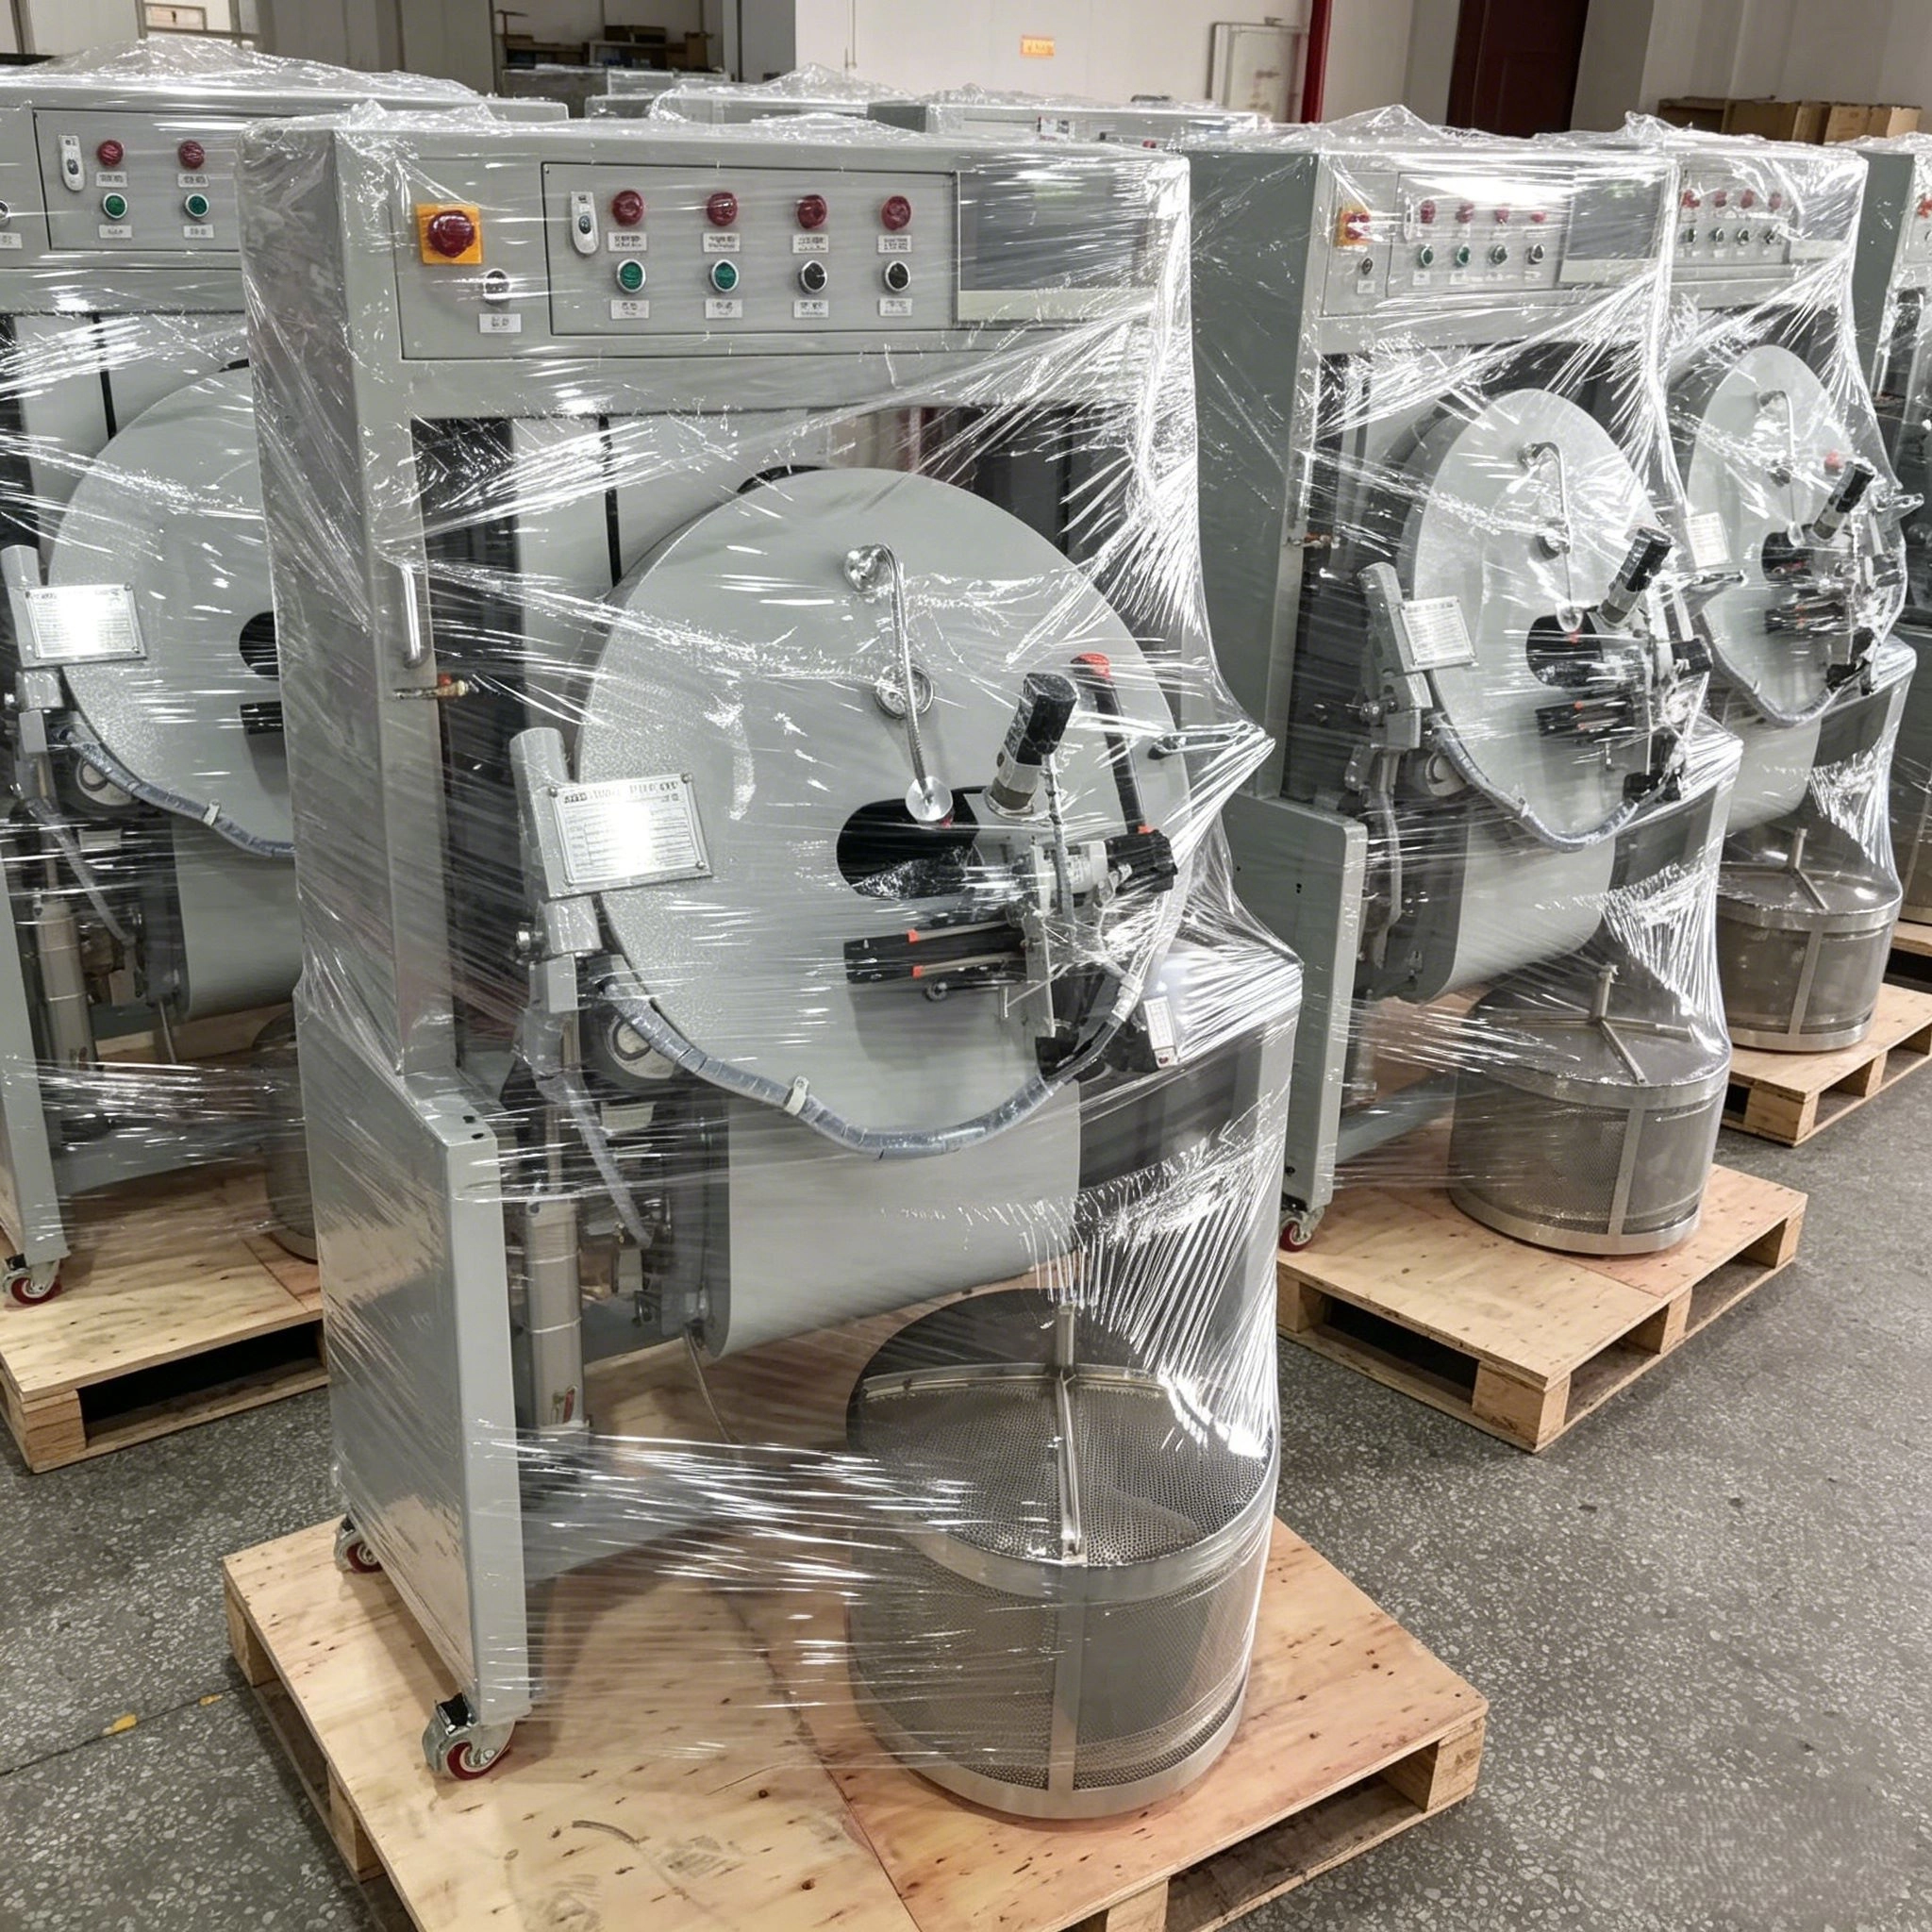
A part that weighs twice as much needs a different recipe even when the paint is the same. Batch recipes written for one part geometry stop working the moment the part changes, and intermediates who tune by memory repeat the same trial and error every week.
This intermediate guide covers batch recipe cards for tumble painting: grouping parts by weight and geometry, setting spray time, drum speed and load, and building a recipe card that any trained operator can follow.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. One recipe for every part | Heavy parts thin, light parts stick | Group parts by weight and geometry |
| 2. Spraying in one long pass | Paint pools and coverage skips | Use short spray windows |
| 3. Overloading light parts | They weld together in the drum | Lower load for light parts |
| 4. Copying another drum's recipe | Different drum, different result | Verify per drum |
| 5. No mid-cycle check | Fault found after full cure | Sample at mid-cycle |
| 6. Card changed by memory | No record of what worked | Update cards with data |
| 7. Ignoring drum speed | Too fast flings paint, too slow pools | Set speed per part group |
| 8. Batch weight guessed | Recipe settings are wrong from the start | Weigh every batch |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Group parts by weight and geometry before writing recipes
- Set load, speed and spray windows per group
- Run a mid-cycle coverage check on every recipe change
- Update recipe cards only after verified batches
- Keep recipe cards visible at the drum
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Recipe card flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- A recipe card turns a skilled guess into a repeatable process.
- Part grouping is the difference between tuning once and tuning every batch.
- Never run a new part group without a mid-cycle sample.
- Never change spray time and drum speed in the same trial.
Working Data & Formula Notes
Recipe reference
Example grouping values for tumble painting; confirm with your paint and drum supplier.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Light parts | Below 10 g | Lower load, short spray windows |
| Medium parts | 10-50 g | Standard load and windows |
| Heavy parts | Above 50 g | Higher load, longer windows |
| Fine springs | Special group | Slowest drum, lightest load |
| Mid-cycle check | At 50% of spray time | Catch faults while fixable |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Recipe card example
| Part group | Load kg | Drum speed | Spray windows |
| Light sliders | 8-10 | Slow | 3 x 8 s |
| Medium buckles | 12-15 | Medium | 4 x 10 s |
| Heavy D-rings | 18-22 | Medium fast | 5 x 12 s |
| Fine springs | 5-6 | Slowest | 2 x 6 s |
Implementation Cases
Case 1 - heavy parts that never covered
Situation. A plant ran D-rings with the same spray recipe as light sliders. The rings came out patchy because the heavier load buried parts and the spray window was too short.
Approach. Parts were grouped by weight, and a new recipe card for heavy parts used a larger load allowance and longer spray windows with a mid-cycle check.
Outcome. D-ring coverage passed on the first full batch and the card was approved for production.
Case 2 - the card changed by memory
Situation. An experienced operator shortened the spray time one afternoon to catch up. The next operator copied the new timing and thin batches followed for a week.
Approach. Recipe cards were made the only authority, with a change request note whenever an adjustment was proposed and verified.
Outcome. Thin-batch rejects stopped and recipe changes now require a verified trial before the card is updated.
Frequently Asked Questions
Why group parts by weight?
Heavy parts need more spray time; light parts need a lighter load to avoid sticking.
What is a recipe card?
A written set of load, drum speed, spray windows and cure settings for one part group.
Why check mid-cycle?
Coverage problems are visible at the middle of the spray cycle, before cure.
How long should spray windows be?
Short bursts with pauses, sized per part group; timing comes from verified batches.
Can I use one recipe for two drums?
No; drum geometry changes the result, so verify per drum.
What if the batch is heavier than the card?
Split the batch; never run above the recipe load.
Who may update a card?
Only after a verified trial; memory-based changes drift the process.
Where should cards be kept?
Visible at the drum so every operator uses the same settings.
What Would You Like to Solve?
If your tumble painting still relies on operator memory, send us your part list, weights and current settings. We can help build the grouping table and recipe card format that make every batch repeatable.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.