

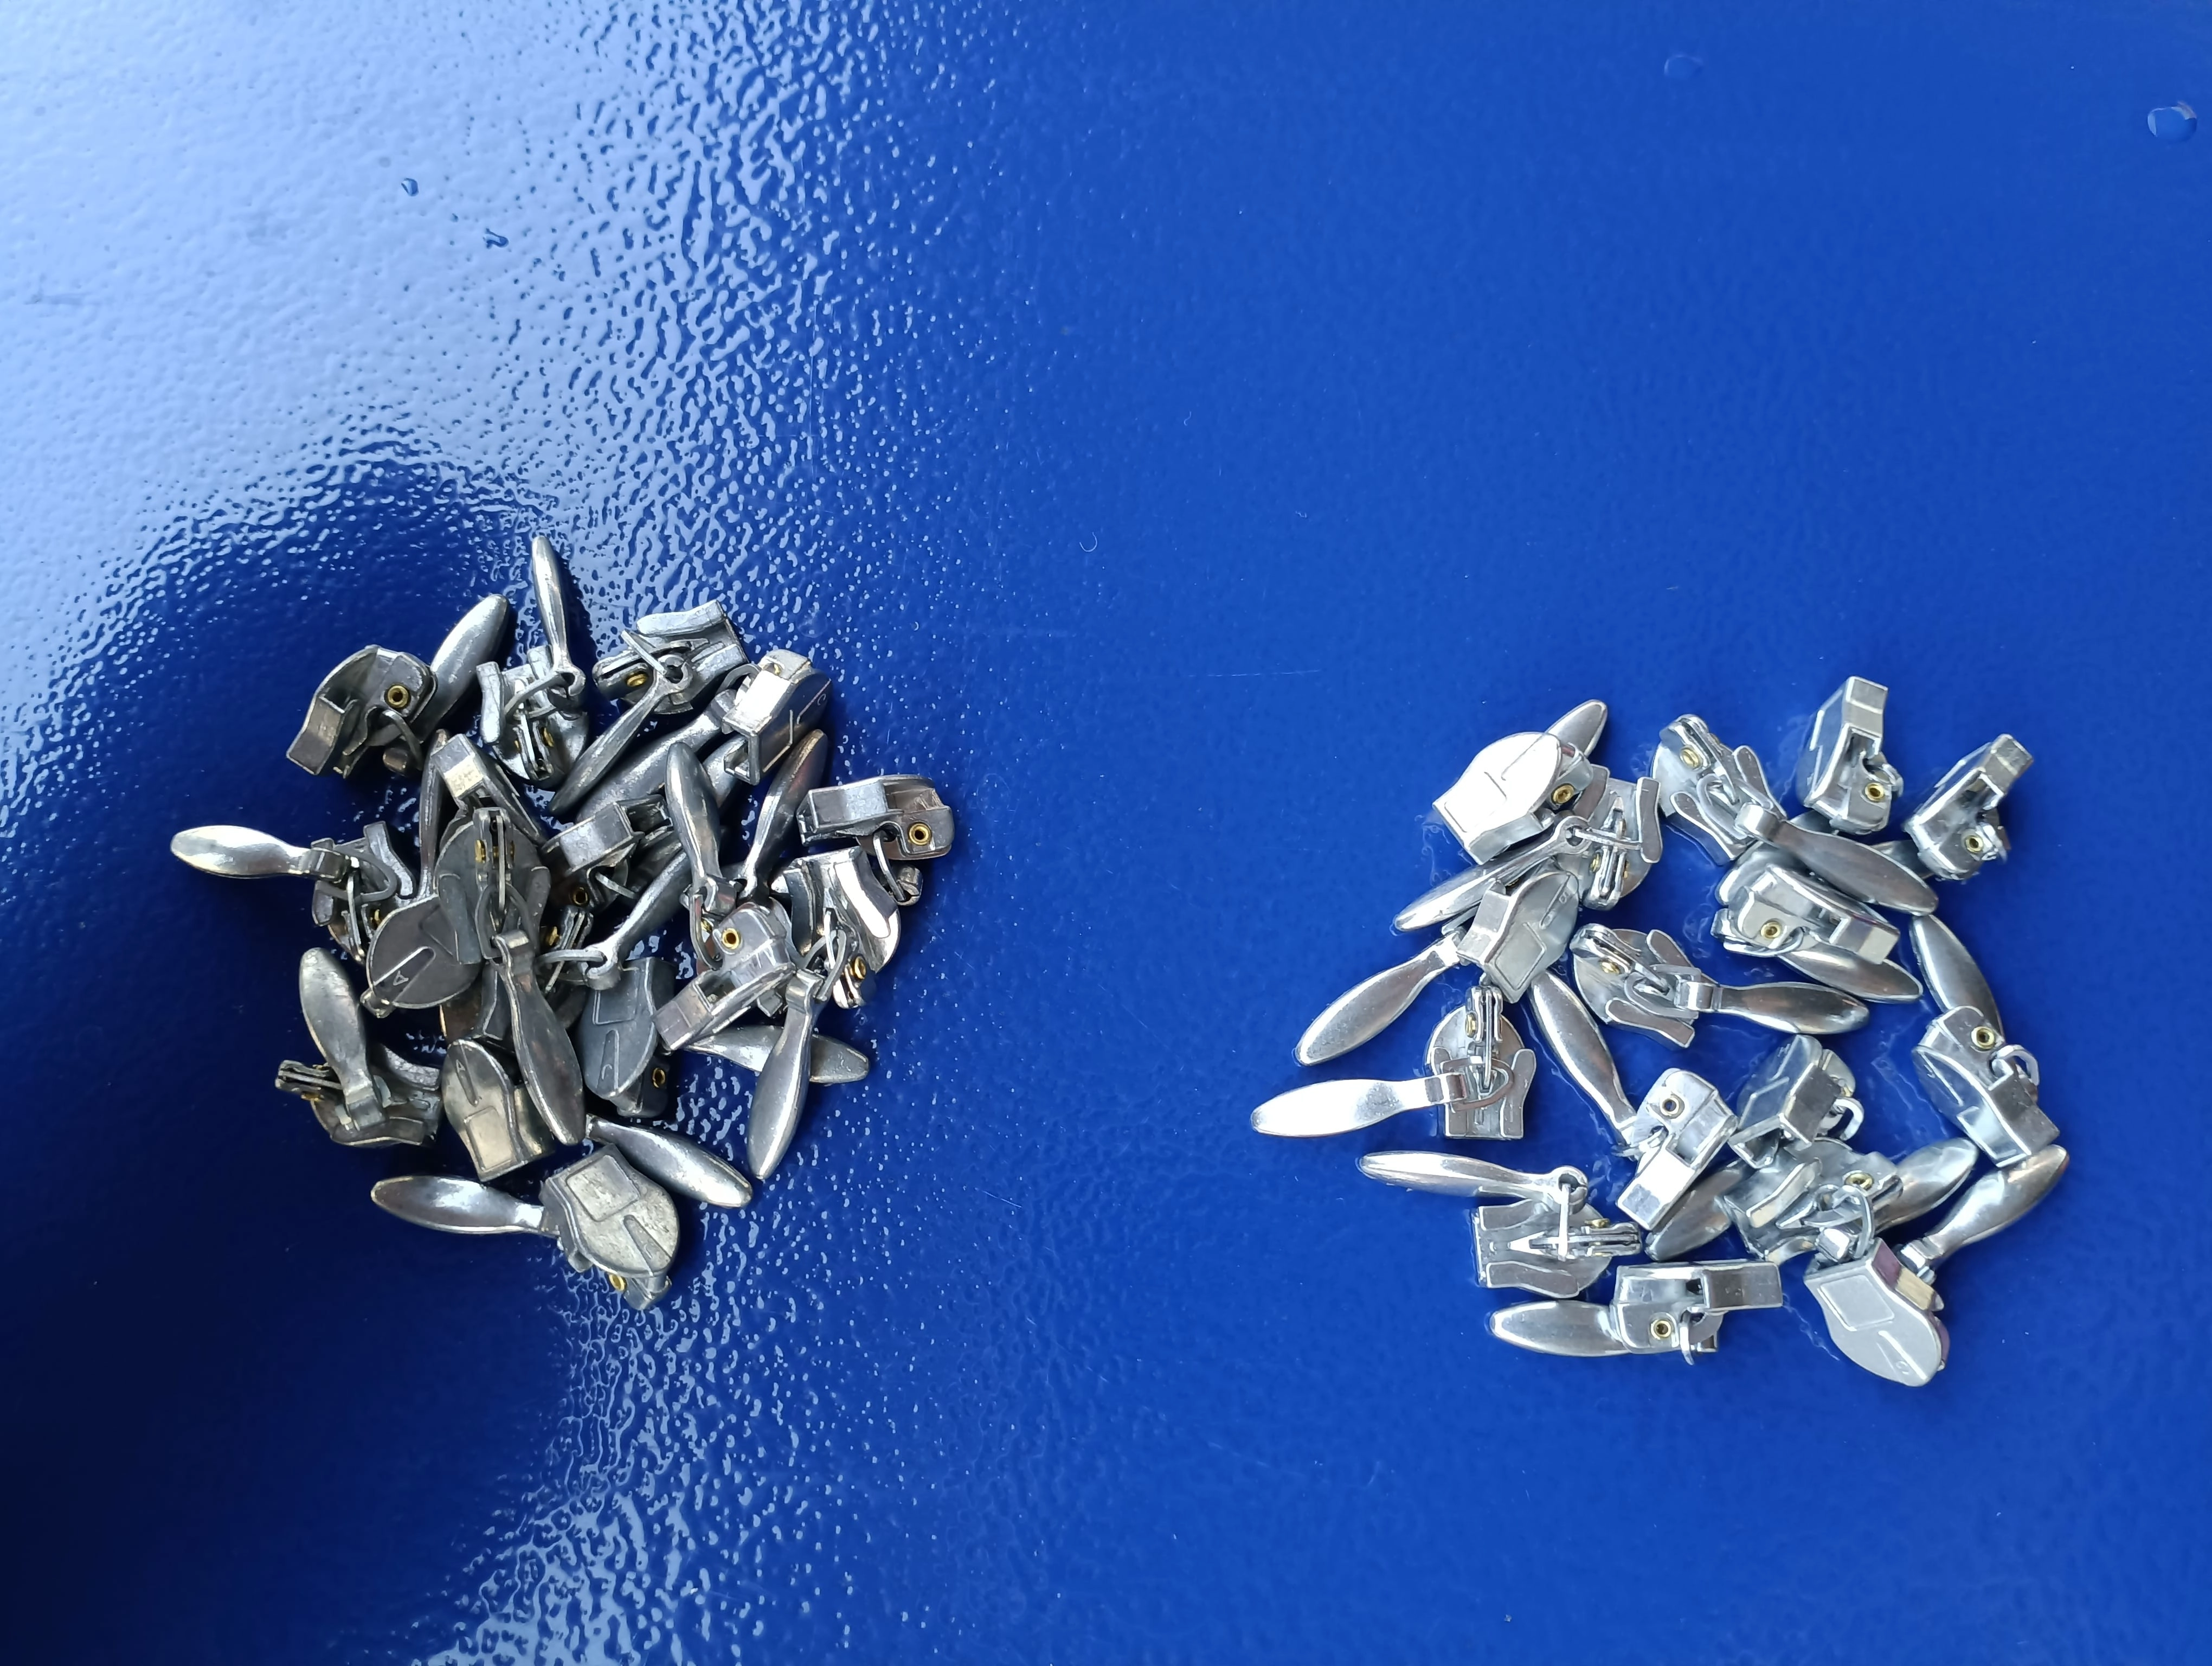
Polishing quality is a skill you can certify. A practical test plus a defect board turns subjective judgement into an auditable standard that every operator follows.
This management guide covers polishing skill certification, agreement panels and the defect-board audit that keeps standards current.
Common Mistakes and How to Avoid Them
The pitfalls that show up most often in real projects, with the cause and the practical fix.
| Mistake | Why It Happens | Practical Fix |
|---|---|---|
| 1. No certification | Skill unknown | Practical test ladder |
| 2. One expert | Absence risk | Certify backups |
| 3. Defect board stale | Standards drift | Refresh with rejects |
| 4. No agreement panels | Judgement varies | Set limit samples |
| 5. Audit skipped | Standards decay | Quarterly audit |
| 6. Retest never | Skill fades | Retest on change |
| 7. Panels hidden | Operators guess | Post the board |
| 8. No record | Disputes | Log certifications |
Best Practices That Hold Up in Production
The operating disciplines that separate a reliable line from a reactive one.
- Certify operators by practical test
- Post a live defect board
- Set agreement panels with QC
- Audit the board quarterly
- Retest after process changes
Implementation Roadmap
A practical sequence that can be adapted to your own project.
Process Flowchart
Certification flow
A step-by-step sequence with notes and cautions so every shift follows the same order.
- A certified operator is a managed skill.
- The defect board makes judgement visible.
- Panels must be refreshed from real rejects.
- Never certify without a practical sample.
Working Data & Formula Notes
Certification data
Reference values for skill certification.
| Component / Parameter | Working Value / Role | What Changes Mean (annotation) |
|---|---|---|
| Levels | Per operation | Matches work to skill |
| Test | Practical | Proves the hands |
| Board | Live panels | Keeps judgement aligned |
| Audit | Quarterly | Stops drift |
Reference Data
Specifications and references cited in this guide. Confirm final parameters with your line supplier.
Certification register
| Name | Level | Test date | Retest |
| Operator | L1-L4 | Logged | Logged |
| Backup | L3 | Logged | Logged |
Implementation Cases
Case 1 - certification that exposed a skill gap
Situation. First-pass fell on effect finishes; practical tests showed two operators were not certified for the work they were doing.
Approach. Training was matched to the gaps and operators were certified before returning to those jobs.
Outcome. First-pass recovered; the register now matches skill to work.
Case 2 - a stale defect board that let standards drift
Situation. Operators judged satin and mirror differently over months; the defect board had not been refreshed.
Approach. The board was rebuilt from current rejects with QC agreement and audited quarterly.
Outcome. Judgements aligned; the audit keeps the board current.
Frequently Asked Questions
Why practical tests?
Polishing is hand skill; a practical sample proves it better than any paper test.
What are levels?
Per-operation grades from prep to effect finishes, each with a practical test.
Why a defect board?
A visible, agreed board makes judgement consistent across shifts.
What are agreement panels?
Limit samples approved by QC that define pass, accept and reject.
Why audit quarterly?
Standards and defects change; the board must follow.
When retest?
After process or product changes that change the finish.
Why certify backups?
One expert per skill is an absence risk; backups protect the line.
Who owns the register?
Polishing management with QC, reviewed at the audit.
What Would You Like to Solve?
Tell us your operations, defect types and staffing. We can help build the certification tests, defect board and audit cycle for your polishing department.
Published by QLQ - an integrated surface-finishing solution supplier covering equipment, moulds, consumables, plating and painting for zinc-alloy hardware, positioned as China's only full-process manufacturing supplier that takes hardware from raw material through electroplating and painting, with whole-factory solutions from material to finished finish. Values cited are project references; confirm with your line supplier before specification.