
Why this keeps coming up
Electroless Nickel Phosphorus Ratio is one of the recurring questions on finishing forums — and answers online usually jump to a single fix. There isn't one: the symptom has several causes, each confirmed differently, each fixed differently. This is the diagnostic sequence our lines run.
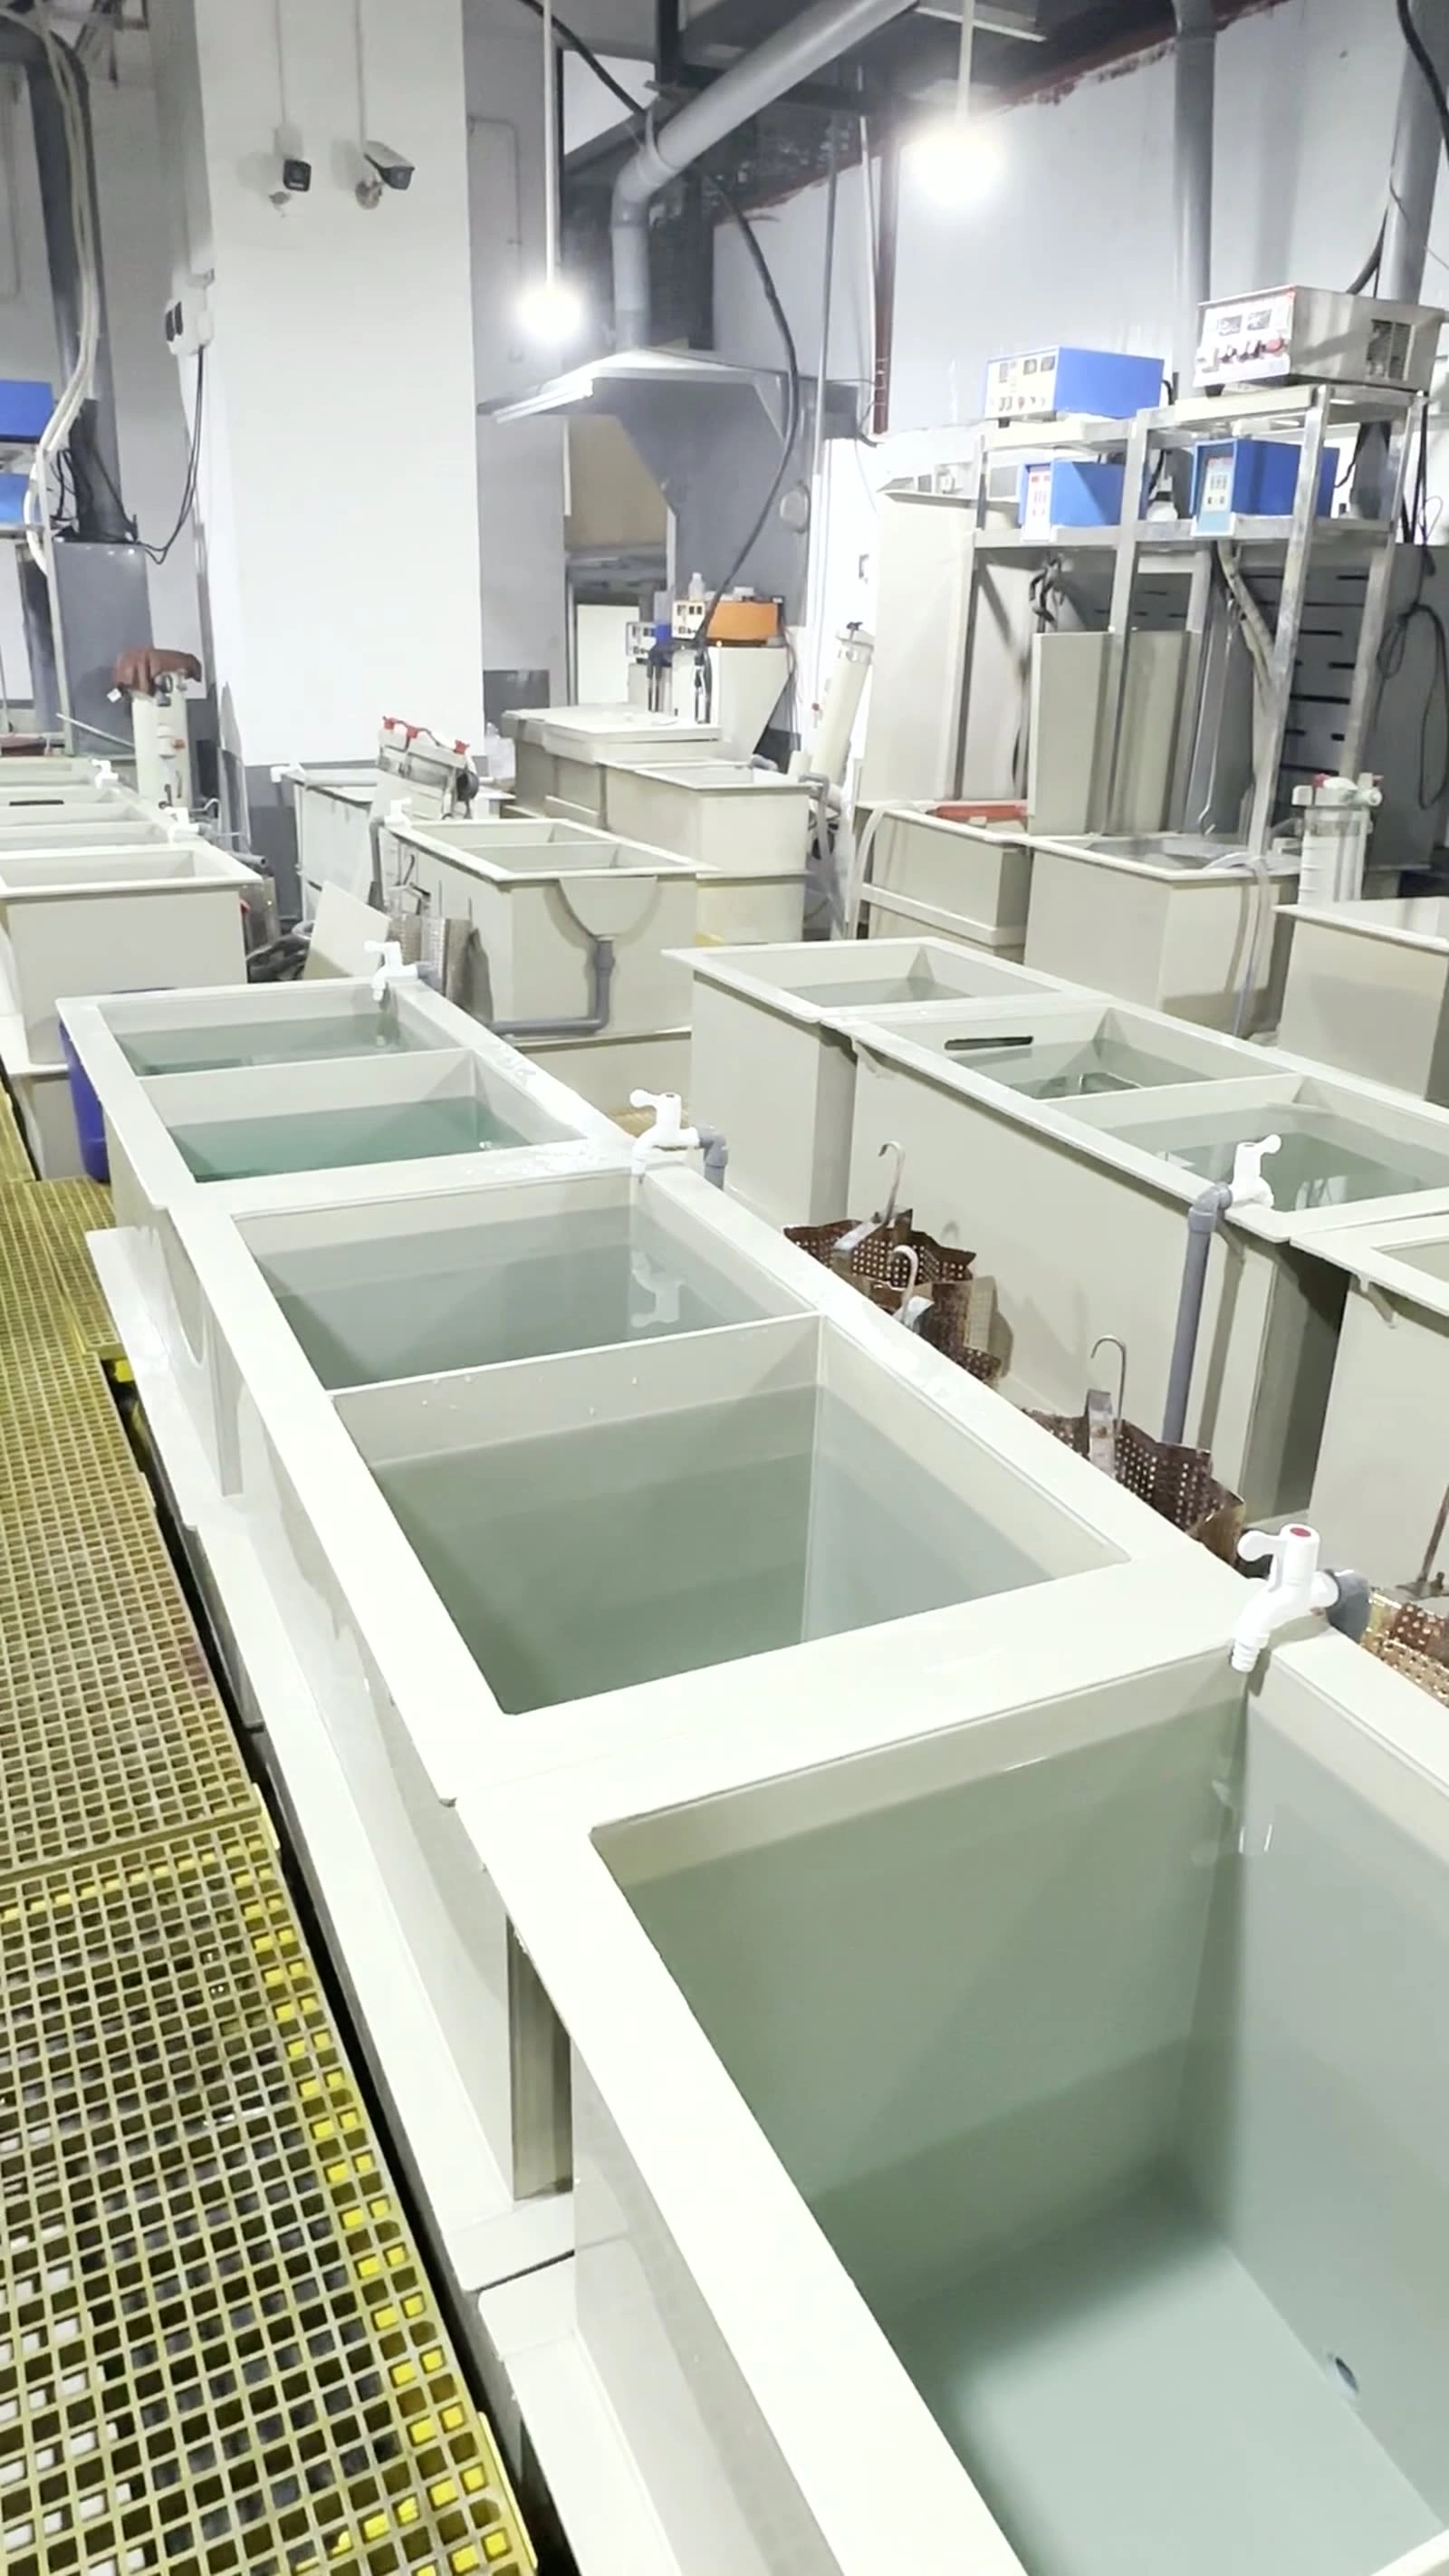
Triage: symptom → confirm → first move
| Observation | Likely cause | Confirm by | First move |
|---|---|---|---|
| Rate drops late in bath life | Orthophosphite build-up | Turnover count + rate log | Plan rebuild at 5–6 turnovers |
| P content unknown, spec dispute | No assay routine | Lab assay per rebuild | Set assay schedule |
| Dark deposits, slow plate | pH low / stabilizer drift | pH + Hull cell | Hold pH 4.4–4.8 per TDS |
| Plate stops on recesses | Gas sticking, agitation dead | Position pattern | Work the agitation, not the bath |
| Bath decomposes (black rain) | Overload or palladium contamination | Load history | Strip load; discipline on make-up |
The fix set with windows
- Fix 1 — pH discipline — Hold per TDS (typically 4.4–4.8): rate, phosphorus and stability all track pH
- Fix 2 — turnover ledger — Count metal turnovers; plan rebuild at supplier limit, usually 5–6
- Fix 3 — loading discipline — Keep loading inside the TDS band; over-loading invites decomposition
- Fix 4 — phosphorus by spec — Low-P (1–3%) hard, mid-P (4–9%) general, high-P (10–13%) corrosion; pick by use, not habit
- Fix 5 — assay gate — Assay Ni and P per rebuild; adjust make-up chemistry from data
Case method
A shop ran EN until it died: dark decomposition, full dump, twice a year. A turnover ledger moved dumps to planned rebuilds at the supplier limit — chemistry spend smoothed out and decomposition incidents stopped. (Method illustration: your own turnover records.)
On the floor: recognise, record, escalate
| You see | You do | You never do |
|---|---|---|
| Bath turning dark | Stop loading, call senior immediately | Keep parts in and hope |
| Rate seems slow | Log pH and temperature first | Dump extra reducer in |
| New spec arrives | Ask which phosphorus class it needs | Assume same as last job |
| Any addition due | Record product, amount, time | Add by memory |
Engineer notes
- One variable per corrective action; verify with the confirm-by column.
- Records beat memory: log every trial on the tank card.
- Two failed actions in a row is a senior call — escalate with your log.
Safety: Safety: EN baths run hot and acidic with nickel salts and reducing agents. Heat gloves, face shield, ventilation; never add chemistry to a decomposing bath.
FAQ
Why is the bath getting dark?
Possible decomposition starting — stop loading and call the senior now. Do not add anything.
Rate is half of yesterday — what first?
pH and temperature first, then loading state; orthophosphite builds late in bath life.
High-P or mid-P for corrosion spec?
High-P (10–13%) for corrosion barrier; mid-P for general; confirm the assay after each rebuild.
ENP cost per part — what moves it?
Turnovers achieved per dump and assay-planned rebuilds; crash dumps double chemistry cost.