
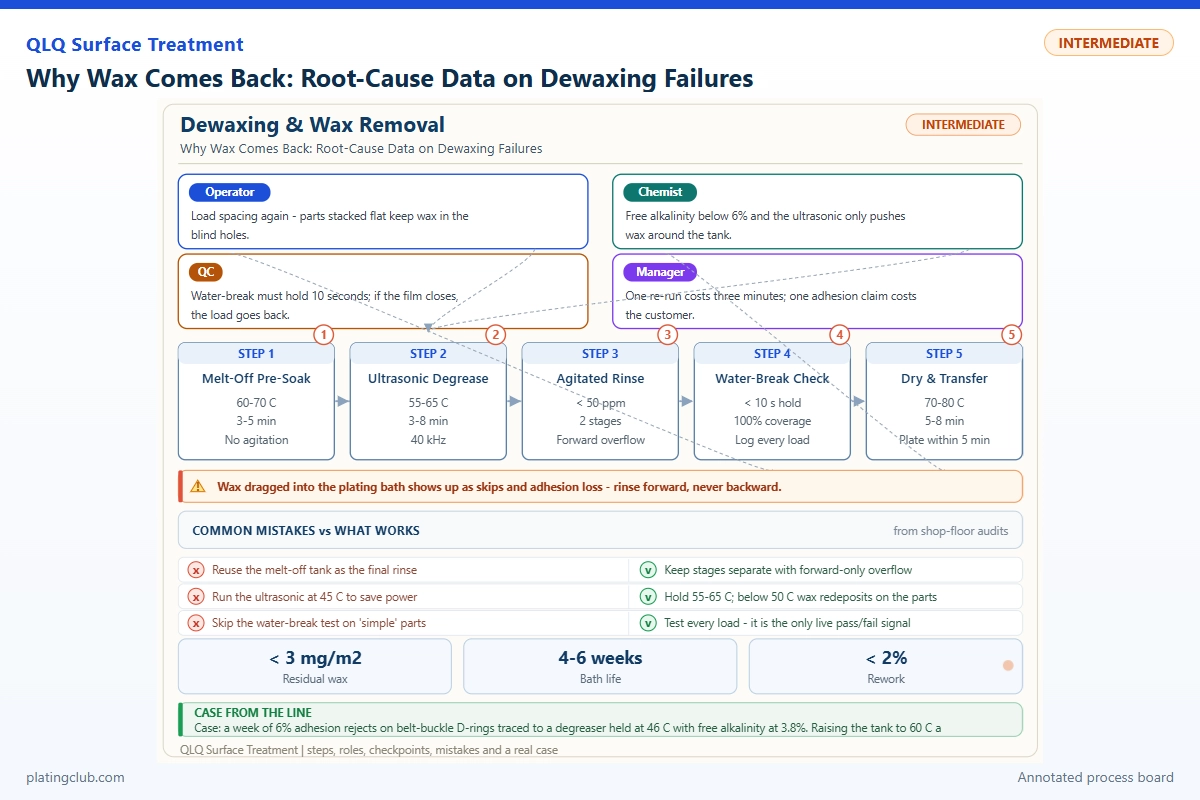
'The parts were clean' is not a diagnosis. Wax-related defects come from four different places, and each leaves a different fingerprint on the part. This is how to tell them apart in under ten minutes and fix the right one.
< 10 min
Diagnosis time
< 1.5%
Repeat rate target
4-6 weeks
Bath life
Four failure modes and their fingerprints
| Mode | Fingerprint | Where to look first | Corrective action |
|---|---|---|---|
| Redeposition | Uniform dull film, strongest low on the part | Bath temperature, free alkalinity | Raise to 60 C, rebuild to 7.5% |
| Carry-over | Defects clustered near rack contact points | Rinse stages, drip time | Add drip time, forward-only overflow |
| Rinse chemistry | Water-marks, hazy patches after drying | Final rinse conductivity | Keep < 50 ppm, DI final stage |
| Mechanical shadowing | Clean top faces, dirty undersides | Load factor, basket design | Reduce to 60%, rotate parts mid-cycle |
Five-day data set from a small-hardware line
| Day | Tank C | Free alkali % | Water-break | Adhesion rejects |
|---|---|---|---|---|
| Mon | 61 | 7.6 | Pass | 0.4% |
| Tue | 59 | 7.1 | Pass | 0.6% |
| Wed | 54 | 5.9 | Fail (11 s) | 2.8% |
| Thu | 52 | 5.4 | Fail | 4.1% |
| Fri | 62 | 7.4 | Pass | 0.5% |
Lab checks that settle arguments
| Check | Method | Limit | Frequency |
|---|---|---|---|
| Residual wax | Solvent extract on a sample | < 3 mg/m2 | Weekly |
| Rinse conductivity | Hand meter at the final stage | < 50 ppm | Every shift |
| Bath loading | Oil/soap split in a sample jar | <= 2% by volume | Weekly |
| Adhesion | Cross-hatch + tape | 0% lift | Every batch of a new part |
Watch out
The Wednesday-to-Thursday pattern above is not operator error: it is a tank drifting below 55 C. Fix the tank, and the rejects follow within one shift.
Common mistakes and the fix
| ✗ Blame the polishers for the wax | ✓ Measure the bath first - the fingerprint tells you which stage failed |
| ✗ Rebuild the tank every time | ✓ Try a top-up and skim first; full rebuilds cost water and heat |
| ✗ Judge cleanliness by sight | ✓ Use residual-wax numbers; the eye misses 3 mg/m2 |
| ✗ Skip the drip time to speed the line | ✓ Drag-out is the second-largest cause of cross-contamination |
What each role watches
| Operator | "Record tank temperature every two hours, not once a shift." |
| Chemist | "Trend free alkalinity; a steady slide means the load is dirty, not the chemistry." |
| QC | "Keep a photo board of each fingerprint - it trains judgement faster than any document." |
| Manager | "Ask for the five-day trend, not a single reading." |
From the shop floor
Case: a shop rebuilt its degreaser every Friday 'to be safe' and still lost 3% to adhesion. The trend sheet showed temperature falling through the week; a covered tank and a 60 C set point removed the problem and cut rebuilds to once every five weeks.
FAQ
How fast does a degreaser drift?
With a well-operating skimmer, 0.2-0.4 percentage points of free alkalinity a day in single-shift work. A drop of 1.5 points in a day means high soil load.
Do I need a DI final rinse?
For zinc hardware heading into plating, a DI final stage is the cheapest insurance against water-marks and hazy gold.
Is residual wax measured on the part or in the bath?
On the part. Bath analysis tells you the tank state; the part tells you what the customer will see.
Where to go next
- Level guide for this trade: Dewaxing & Ultrasonic Cleaning — technician levels
- Other levels: Junior, Senior, Management
- Owner view: Process Overview for owners
- Supplier view: Chemistry & Supply · Find content by trade + level